Engineered for automotive trim, plastic sub-assemblies, electronic enclosures, and metal-to-metal high-torque cold-joining.



Evaluating structural integrity, mechanical yield performance, and insertion dynamic metrics across automated Tier-1 assemblies.
Cross recess drive systems (Phillips Type H and Pozidriv Type Z) balance driver bit engagement with deliberate cam-out thresholds. In high-speed robotic screwdriving, our precision cold-heading dies ensure driver recess tolerances within ±0.015 mm, mitigating premature cam-out, bit wear, and micro-particle contamination inside cleanroom assembly zones.
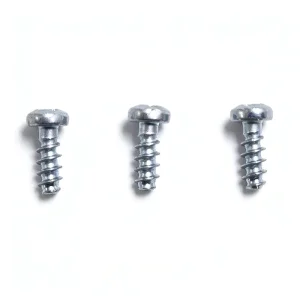
Unlike conventional machine screws requiring pre-tapped female threads, specialized thread geometries—such as our 30° flank angle PT profiles—displace thermoplastic substrate elastically rather than tearing it. This drastically reduces radial hoop stress, eliminates boss cracking in low-ductility polymers, and maximizes back-out resistance during thermal fluctuation.
The international industrial hardware market is rapidly transitioning toward consolidated procurement. Global OEMs demand tier-one Chinese factories capable of offering end-to-end traceability, verified surface passivations meeting REACH/RoHS3 imperatives, and integrated supply resilience capable of buffering raw material and currency volatility.
Cross recess self-tapping fasteners serve as foundational structural hardware across demanding sectors where vibration, thermal shock, and chemical exposure dominate.
Miniature cross recess self-tapping screws (M1.2–M3.0) secure delicate PCB substrates, shielding frames, and structural heat dissipation housings. Using high-ductility 304/316 stainless steels, these micro-fasteners resist galvanic corrosion and strip-out within ABS, Polycarbonate, and glass-filled PBT housings under rapid robotic placement.
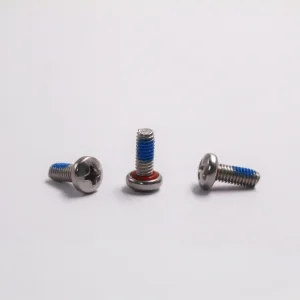
Compliant with stringent IATF 16949 production standards, our fasteners secure wire harnesses, dashboard fascia modules, lighting clusters, and lithium battery sensor rails. Pre-applied nylon locking compounds or under-head sealing elastomer washers neutralize loosening under severe continuous harmonic resonance.
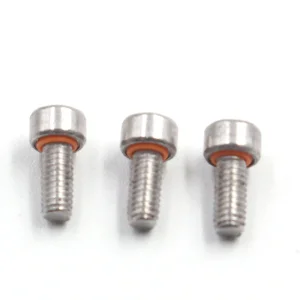
Energy storage system (ESS) cabinets and junction control boxes demand unyielding outdoor ingress protection. Our IP67/IP68 rated sealing cross recess fasteners combine cold-headed captive flanges with molded fluorosilicone O-rings, providing dual sealing and structural anchoring that resists water, atmospheric salt spray, and dielectric fluid leakage.
Vertical manufacturing integration delivers rapid tooling cycles, zero-compromise metallurgy, and dynamic capacity scaling for Fortune 500 supply chains.
Operating inside Guangdong and Central China manufacturing corridors allows direct partnership with world-class wire-rod drawing mills. Whether processing AISI 1022A carbon steel for carburized case-hardening or SUS 304/316 austenitic stainless steels, spectroscopic composition validation occurs before batch allocation.
Continuous mesh-belt carburizing furnaces impart critical hardness differentials: achieving minimum surface hardness of HV 450–750 for swift sheet penetration while preserving a resilient core hardness of HV 270–390 to prevent catastrophic hydrogen embrittlement or shear failure under dynamic structural flex.
High-speed rotary glass plate vision sorters verify every critical dimension—recess depth, thread angle, head concentricity, and total length—at rates exceeding 800 parts per minute. Defective parts are pneumatically ejected, locking down incoming quality for fully automated assembly stations.
| Parameter | Type AB (Thread Forming) | Type B (Blunt Point) | PT Thread (Thermoplastics) | Tri-Lobular / Taptite Compatible |
|---|---|---|---|---|
| Target Substrates | Sheet steel < 2.5mm, Plywood | Die-cast Zinc, Extruded Al | ABS, PP, PA66, PBT, Polycarb | Structural Steel, Ductile Castings |
| Flank Angle | 60° Standard ANSI/DIN | 60° Truncated Crest | 30° Low-Radial Stress | 60° Tri-Lobular Cross Profile |
| Driving Method | Phillips / Pozidriv Cross | Phillips / Combination Slot | Cross Recess / Torx Hybrid | Deep Cross Recess Type H/Z |
| Surface Hardness | HV 450 min. (Carburized) | HV 450 min. (Carburized) | Through-Hardened or Passivated | HV 550 min. (Case Hardened) |
| Prevailing Friction | Moderate (Continuous thread) | Low running friction | Ultra-low (Reduces boss hoop strain) | Low dynamic driving torque |
Anticipating next-generation micro-electronics assembly and automotive decarbonization requirements through metallurgical innovation.
Transitioning from hexavalent to zero-chrome trivalent zinc passivations, organometallic thin-film zinc flake finishes (Geomet/Magni), offering 1,500+ hours neutral salt spray resistance without acidic acid risk.
Scaling multi-station wire cold formers down to M0.8 and M1.0 sizes. Accommodates surgical micro-devices, AR/VR smart optics assemblies, and miniaturized drone sensor gimbals requiring extreme lightweighting.
Combining cross recess geometric foundations with subtle anti-stripping radial locks. Ensures smart brushless electric nutrunners capture precise angle-torque curves for complete Industry 4.0 data logging.
Implementing green wire annealing and low-emission closed-loop lubrication systems. Reduces embedded carbon footprints across large-scale export batches to Europe, Japan, and North America.
International trade requirements demand uncompromising material testing and transparent documentation at every milestone.
We provide complete Production Part Approval Process (PPAP) documentation, including Process FMEA, Control Plans, Gage R&R studies, and International Material Data System (IMDS) declarations for Tier-1 automotive assemblies.
Our bilingual application engineers offer remote DFM (Design for Manufacturability) consulting, recommending pilot hole diameters, optimal thread pitches, and tightening torques tailored directly to your molded CAD part models.
From bonded warehousing in Shenzhen, Ningbo, and Shanghai to FOB, CIF, or DDP delivery directly to European and American assembly plants, we manage rigorous moisture-barrier packaging and barcoded traceability.
Targeted answers covering cold heading tooling, pilot hole design, metallurgical grades, and custom OEM manufacturing.
While both feature a cruciform cross drive, the Pozidriv recess has parallel internal flank ribs that eliminate the deliberate cam-out taper engineered into standard Phillips screws. Pozidriv permits higher driving torque with less required operator end-load, whereas Phillips helps prevent thread over-tightening in soft sheet metal.
Hydrogen embrittlement is prevented by strictly controlling electroplating pickling times and transferring fasteners to continuous baking ovens within 4 hours of surface finishing. Fasteners are de-embrittled at 200°C–220°C for 4 to 8 hours depending on tensile strength grade, followed by destructive torque testing per ISO 10683.
Yes. We custom-roll specialized PT thread geometries with 30° or 40° included thread angles and expanded thread pitch. This design reduces internal boss expansion forces by up to 50%, preventing burst bosses in brittle plastics like 30% glass-filled PA66 or Polycarbonate.
Standard metric sizes in stock ship within 48 hours. Custom CNC or cold-headed fasteners manufactured from 2D/3D client prints typically carry an MOQ of 20,000 to 50,000 pieces depending on wire gauge, with tooling fabrication and sample sign-off completed in 10–14 days and full mass production in 3–4 weeks.
Precision-manufactured mechanical components produced to international standards (DIN, ISO, JIS, ASME) and custom client drawings.





Submit your 2D engineering drawings (PDF/DWG) or 3D STEP models. Receive a detailed Design for Manufacturability (DFM) review and volume pricing estimate within 24 hours.
