

Precision engineered fasteners produced concurrently with our industrial hex keys, torx drivers, and custom socket systems to ensure zero cam-out and zero recess rounding.


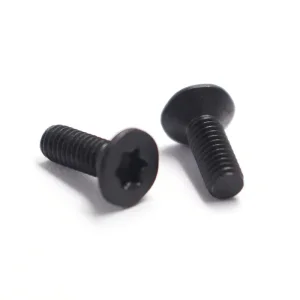
In advanced high-vibration assemblies, hex keys (Allen wrenches) are critical transmission interfaces. Discover how modern metallurgical manufacturing eliminates socket round-out, premature torsional shear, and contact stress corrosion.
Standard hex keys comply with DIN 911, ISO 2936, and ASME B18.3. Modern high-torque applications demand tight flank-to-flank tolerances (h9–h11 across flats) to maximize surface contact and prevent concentrated notch stresses at socket corners.
Sub-tier tooling suffers from over-hardening, yielding catastrophic brittle failure under impact loading. Premium industrial hex keys demand continuous induction tempering to retain a ductile shock-absorbing core paired with an HRC 58–62 wear-resistant surface shell.
Automotive, aerospace, and energy manufacturers require unified procurement. By synchronizing hex key tooling tolerances with precision custom socket screws, OEMs eliminate assembly line slippage, drive stripping, and joint preload discrepancies.
From silicon-alloyed S2 shock-resisting tool steel to non-magnetic austenitic stainless steels, review our metallurgical options tailored for critical torque retention and harsh environmental exposure.
| Alloy Grade | Hardness Range | Torsional Yield Point | Corrosion Shielding | Recommended Industrial Applications |
|---|---|---|---|---|
| Premium S2 Tool Steel | HRC 58 – 62 | Exceeds DIN/ISO by +45% | Manganese Phosphate / Hard Chrome | Robotic assembly lines, automotive assembly plants, automated production cells |
| Chrome Vanadium (Cr-V / 6150) | HRC 52 – 56 | Standard ISO 2936 baseline | Satin Nickel / Zinc Electroplate | General machinery maintenance, consumer tool sets, plant repair operations |
| AISI 304 / 316 Stainless | Work-Hardened / HRC 32–38 | Engineered for non-magnetic joints | Native Passivation (ASTM A967) | Medical robotics, semiconductor cleanrooms, offshore wind telemetry housings |
| Alloy 8660 (Ni-Cr-Mo) | HRC 56 – 60 | High fatigue endurance limit | Black Oxide with Anti-Corrosion Seal | Heavy industrial gearboxes, wind turbine hub assemblies, railway rolling stock |
Yu-Huang Electronics (Dongguan) Co., Ltd. leverages a multi-site manufacturing footprint across southern and central China, providing high vertical integration from coil drawing to final export packing.
Unlike trading houses that subcontract critical stages, our 20,000 m² facilities handle spheroidizing annealing, multi-stage cold extrusion, ball-end CNC machining, mesh-belt vacuum heat treatment, and surface plating under one rigorous IATF 16949 audit trail.
Production is load-balanced across our primary Dongguan headquarters and regional manufacturing branches in Shaoguan and Wuhan. This multi-plant strategy buffers regional supply bottlenecks, ensuring on-schedule delivery for global tier-1 assemblers.
We engineer non-standard dimensions, extended-reach shafts, ball-end configurations up to 30-degree entry angles, security tamper-proof pins, and specialized flag handles within 7–10 days using dedicated CNC tool-and-die workshops.
Industrial hex keys and matched socket hardware operate across demanding conditions—from automotive assembly floors to cleanroom instrumentation. Here is how our components perform in high-reliability applications.
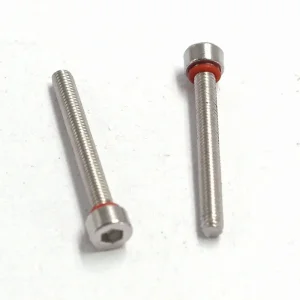
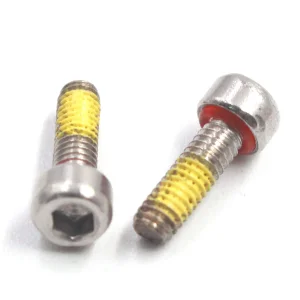
Automotive radar brackets and inverter modules require precise torque limits without micro-burr generation. Our cold-forged hex wrenches and captive sealing screws deliver uniform clamp loads without damaging pre-applied threadlock coatings.
High-current electrical connections require regular field retorquing. We supply zinc-nickel plated hex wrenches and stainless steel fasteners certified to withstand 720+ hours of neutral salt spray (ASTM B117), preventing galvanic corrosion in marine and desert solar parks.
Cleanroom mechanisms require non-galling, non-magnetic stainless steel hex keys and custom ball plungers. Controlled ultrasonic solvent cleaning and Class 100 packaging eliminate hydrocarbon particulate contamination.
Our smart factory investments improve precision, material tracking, and low-carbon metallurgical processes to meet Industry 4.0 requirements.
Automated optical grading checks 100% of hex key drive dimensions and chamfer angles at line speed, reducing defect escapes to under <5 PPM.
Transitioning high-torque keys to controlled bainitic structures, increasing dynamic impact toughness by 35% compared to standard quench-and-temper martensite.
Sub-millimeter laser annealing encodes production lot numbers, raw material heat numbers, and exact torque specs directly onto tool shafts for critical aerospace and EV applications.
Employing green electric annealing furnaces and closed-loop trivalent chromium passivation to eliminate hexavalent chrome and reduce carbon footprint per unit by 28%.
Every production lot is documented from incoming wire coil to dispatch. Our internal laboratories verify dimensions, metallurgy, and performance before release.
We provide complete Production Part Approval Process (PPAP) documentation, including Design Failure Mode and Effects Analysis (DFMEA), Process Control Plans (PCP), and Gage R&R studies for automotive and industrial OEMs.
Our on-site QA lab features computer-controlled torsional test benches, Rockwell and Vickers microhardness indenters, and ASTM B117 salt spray chambers to verify corrosion performance on every production lot.
All surface coatings, anti-rust oils, and pre-applied patches comply with EU RoHS 2.0 (2011/65/EU) and REACH (EC 1907/2006). Comprehensive SGS test reports are archived for 10 years to support downstream regulatory audits.
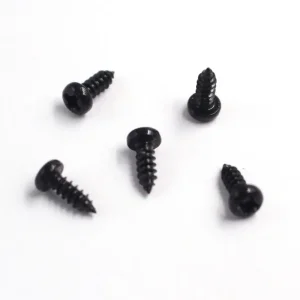
Standard and custom cold-headed fasteners manufactured alongside our hex key product lines, providing OEM buyers with integrated procurement and certified fitment.

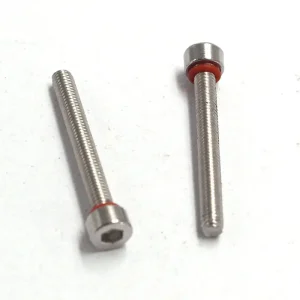


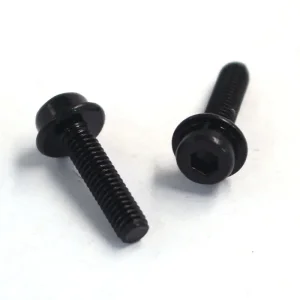
Detailed technical answers to common queries raised by corporate procurement heads, lead tool designers, and supply chain managers.
Send your CAD drawings, sample requirements, or bill of materials to our application engineering team. Receive an engineering analysis, feasibility review, and factory-direct quote within 24 hours.
Request Direct Factory Consultation