
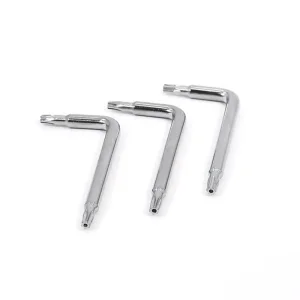
OEM Stainless Steel Torx Hex Key Wrench Manufacturer, Factories
Explore Wrench Specs
Direct integration of precision-profile wrenches and pairing drive screws engineered to mitigate cam-out, ensure repeatable preload clamping, and streamline high-volume production lines.


In modern automated and semi-automated production lines, high-stress assembly operations often fail not because of tensile bolt failure, but due to interface degradation. When high-speed pneumatic drivers mate with sub-standard L-keys, hexagonal wrenches, or Torx profiles, minute dimensional discrepancies introduce severe cam-out, radial bit rounding, and micro-fissuring.
Discrepancies exceeding ±0.02mm between wrench across-flats (AF) and socket recesses create localized contact stresses that exceed the plastic yield threshold of stainless steel fasteners, inducing instant metal sliver shedding in cleanrooms.
Unplanned line stops resulting from stripped Torx pins or rounded Allen key sockets generate crippling operational expenditures in automotive battery-pack integration and high-volume electronics housing operations.
Tier-1 procurement directives increasingly require captive manufacturing protocols, wherein wrench tools and high-spec fasteners are engineered, cold-headed, and calibrated from identical metallurgical masters.
Precision L-keys, ball-end hex drivers, and tamper-resistant Torx wrenches must be calibrated against sector-specific structural constraints. Below is how our engineered wrenching solutions are deployed globally.
Non-magnetic, passivated SS316 and insulated Torx keys engineered to prevent stray electrostatic discharge during prismatic cell installation, retaining clean anti-galling profiles across repetitive torque operations.
Micro-wrenches down to 0.7mm across-flats calibrated for sub-millimeter opto-mechanical brackets. Zero burr retention guarantees zero FOD (Foreign Object Debris) in cleanroom electronics enclosures.
Heavy-duty, manganese-phosphated Cr-V hexagonal keys engineered with ball-end flexibilities up to 25° angles, permitting field maintenance engineers access to deep recessed engine flanges and casting dies.
True supply chain resilience requires eliminating subcontracting delays. Operating across 20,000 m² of specialized production plants, YH Fastener centralizes the entire tool-and-fastener lifecycle.
Direct volume agreements with certified steel mills guarantee certified billets of S2 shock-resistant steel, Cr-V (6150), and austenitic SS304/SS316 with complete chemical composition traceability.
Over 180 multi-station cold heading machines and dedicated tooling rooms allow high-speed drawing conversion into bespoke chamfered L-keys and custom fastener drives within 48-72 hours.
Atmosphere-controlled mesh-belt furnaces maintain consistent quenching conditions, preventing surface decarburization and achieving uniform core-to-surface grain hardness without embrittlement.
High-speed laser sorting tables screen each output batch for dimensional flatness, head height, drive depth, and surface inclusions at speeds of 600 units per minute prior to dispatch.
Full compliance with international mechanical norms including DIN ISO 2936 (Hex keys), DIN EN ISO 10664 (Hexalobular/Torx), and ASME B18.3. Custom modifications engineered upon request.
| Profile Specification | Material Grade | Surface Hardness | Yield Torque Target | Corrosion Passivation | Primary Industrial Sector |
|---|---|---|---|---|---|
| Metric Hex L-Key (DIN ISO 2936) | Chromium-Vanadium (Cr-V 6150) | HRC 52 - 56 | ≥125% of DIN Norm | Black Oxide / Matt Chrome | Industrial Machinery Assembly |
| Torx / Hexalobular (T5 to T60) | S2 Shock-Resistant Alloy Steel | HRC 58 - 62 | ≥140% of ISO Standard | Titanium Nitride / Phosphate | Consumer Electronics & Robotics |
| Cleanroom Austenitic Keys | AISI 304 / 316 Stainless Steel | HB 190 - 230 (Work Hardened) | High Toughness / Anti-Snap | Electropolished Passivation | Biomedical, Marine, Photovoltaics |
| Tamper-Proof Pin-Torx & Hex | AISI 8660 Nickel-Chromium Steel | HRC 56 - 60 | Zero Pin Deflection Spec | Electrophoretic Black E-Coat | Telecommunications & Transit |
| Spherical Ball-End Hex Driver | Modified Cr-Mo (SCM435) | HRC 54 - 58 | 25° Off-Axis Load Certified | Satin Zinc / Nickel Plating | Automotive Jigs & Ergonomic Tools |
Fastening systems are transforming from passive mechanical linkages into smart, sensor-monitored, and self-documenting assembly interfaces designed for automated manufacturing 4.0.
Application of micro-crystalline diamond PVD coatings to wrench tips to dramatically elevate friction coefficients, completely eliminating contact slip on rounded fasteners.
Development of quick-indexing magnetic hex and Torx tool cartridges designed specifically for SCARA and 6-axis collaborative robotic assembly arms with automatic wear feedback.
Embedded micro-transponders inside industrial wrench bodies to automate tool accounting, calibration monitoring, and FOD prevention in flight-critical assembly lines.
Direct metal laser sintering (DMLS) combined with CNC five-axis finishing to create ultra-lightweight hollow-truss wrenches for field equipment and mobile defense assemblies.
International trade requirements necessitate comprehensive verification. YH Fastener equips global engineering teams with direct digital validation and rigorous export certifications.
For automotive tier-suppliers, we furnish full Production Part Approval Process documentation, including PFMEA, control plans, Gage R&R, and initial process capability (Cpk ≥ 1.67) studies.
Third-party testing via SGS/TUV confirms zero restricted hazardous substances or uncertified raw materials across all plating chemistries, including hexavalent chrome-free zinc finishes.
Dedicated technical liaisons and multilingual fastener application engineers facilitate video tool evaluations, joint clamping simulations, and on-site factory audit verifications within 24 hours.
Precision-manufactured machine screws, anti-vibration locking systems, spring detents, and specialized industrial bolts direct from our cold-heading and CNC lines.
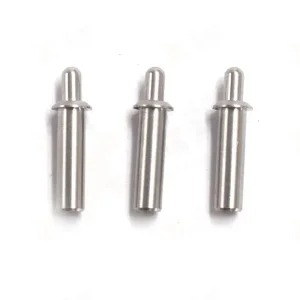
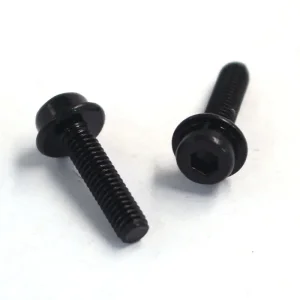
In-depth technical answers addressing dimensional verification, alloy selection, coating adhesion, and global shipment validation protocols.
We overcome cam-out by manufacturing the driving key and the fastener socket using integrated gauge suites. Instead of relying on disparate ISO baseline charts, our engineers calculate micro-tolerances for both mating parts simultaneously, ensuring 100% flank contact, zero reaming, and optimal torque transfer under high pneumatic drive speeds.
For high-cycle industrial environments, we recommend premium S2 modified tool steel heat-treated to HRC 58-62. S2 provides superior impact shock resistance compared to standard Cr-V 6150, resisting micro-torsional shear when pneumatic drivers strike automated seating points in automotive assembly.
Yes. Our in-house engineering and tooling facility in Dongguan specializes in custom profile geometry. We accept STEP, IGES, and DWG models to develop precision cold-forming dies or wire-EDM tooling within 48 to 72 hours, backed by full CMM coordinate measuring reports and sample runs.
We provide multiple finish options: black oxide (24–48h NSS), electro-zinc plating with trivalent passivation (96–240h NSS), zinc-nickel alloy plating (720–1000h NSS without red rust), and electropolished passivation on austenitic SS304/SS316 for offshore, marine, and medical environments.
Our Quality Assurance system strictly complies with IATF 16949 standards. For every batch shipment, we generate full material traceability certificates (EN 10204 Type 3.1), salt spray corrosion logs, micro-Vickers hardness reports, torque-to-yield graphs, and full PPAP Level 3 documentation.
Standard catalog hex keys, spring plungers, and standard machine screws typically dispatch from warehouse inventory within 3 to 5 business days. Custom cold-headed production orders run on average 15 to 22 business days, supported by express air freight or consolidated ocean containers to over 60 countries.