Engineered cold-formed fasteners featuring IP67/IP68 self-sealing elastomer rings, vibration-proof thread profiles, and anti-tamper head drive geometries.





Analyzing the macro-economic forces, intellectual property protection imperatives, and critical safety regulations driving the double-digit expansion of anti-tamper fastening systems worldwide.
In modern industrial engineering, mechanical security at the physical fastener interface is no longer an afterthought—it represents the primary barrier against catastrophic liability, intellectual property theft, warranty fraud, and lethal electric shocks. As global original equipment manufacturers (OEMs) roll out interconnected smart infrastructure, distributed energy systems (such as EV battery packs and residential energy storage), high-density 5G telecommunication networks, and automated utility metering, the vulnerability of public-facing mechanical enclosures has surged into an executive-level risk calculation.
Historically categorised under niche mechanical hardware, the global market for security screws and tamper-resistant fasteners is undergoing an unprecedented paradigm shift. Industrial design authorities estimate that by 2030, tamper-evident and anti-theft hardware will account for more than 18% of all high-tensile machine screw installations across mission-critical sectors. The transition from common slotted or standard Phillips recesses to proprietary security geometries is being propelled by three converging industrial vectors:
With electric vehicle architectures escalating from 400V to 800V and beyond, non-authorized entry into battery enclosures or inverter housings poses immediate fatal electrocution hazards. Tamper-evident fasteners function as active life-safety protocols.
ISO 6469-3 IEC 60664 UL 2580High-value industrial electronics, edge AI compute modules, and specialized robotics contain proprietary PCB topologies and firmware. Security screws prevent unauthorized physical probing, chip harvesting, and unlicensed hardware extraction.
IP Protection Warranty Integrity Custom RecessesSmart meters, railway signalling enclosures, highway surveillance units, and municipal solar lighting arrays face constant vandalism and metal scrapping risks. Specialized one-way and pin-drive fasteners drastically curb maintenance overhead.
Vandal Proof DOT Infrastructure Smart GridsA deep mechanical analysis evaluating drive torque transfer capacity, cam-out mitigation, tamper-resistance index, and automated assembly line compatibility across leading drive architectures.
Selecting the optimal security screw geometry requires balancing three competing engineering variables: the Tamper Resistance Index (TRI), the Torque Transmission Capability (TTC) without recess shear, and the Assembly Speed / Automated Driver Integration (ADI). Using incorrect geometries often yields stripped recesses, damaged drive tooling, or inadequate clamp load in production environments.
| Drive Geometry Typology | Mechanical Engagement Mechanism | Torque Transfer Efficiency | Tamper Resistance Index | Field Serviceability & Tooling Control | Ideal Application Sectors |
|---|---|---|---|---|---|
| Pin-in-Torx (Security Star) | 6-lobe spline with a solid central cylindrical post preventing standard Torx key insertion | Very High (92% - minimal cam-out force required) | Medium (Consumer bits readily available) | High (Standard security bit sets available for field technicians) | Automotive sub-assemblies, electronic enclosures, mass transit interiors |
| Pin-in-Hex (Tamper Hex Socket) | Standard 6-point hexagonal broach with solid central blocking core | Medium-High (Susceptible to flank rounding at high torques) | Moderate (Available in industrial maintenance kits) | High (Readily deployed across HVAC and industrial plants) | Machinery guarding, commercial lighting, elevator access panels |
| One-Way / Sentinel (Clutch Head) | Cammed slotted profile allowing clockwise insertion; driver slides off counter-clockwise | Medium (Requires high axial down-force during install) | Extremely High (Permanent; requires destructive removal/drill) | Zero (Designed purely for permanent one-off installation) | Prisons, detention locks, public park signage, architectural security grilles |
| Spanner / Snake-Eye (Two-Hole) | Two opposing cylindrical blind pilot holes machined into smooth rounded head | Low-Medium (High torque will sheer driver locator pins) | High (Flat face prevents grip by pliers or common tools) | Controlled (Dual-prong bits require exact center-to-center pitch) | Architectural ironmongery, luxury retail fixtures, marine aesthetics |
| Tri-Wing / Tri-Groove | Three radial slotted wings converging on an offset or triangular hub | High (Radial engagement distributes torsional stress evenly) | High (Requires specialized aircraft/electronics driver bits) | Restricted (Commonly deployed with registered tool crib logs) | Aerospace cockpits, defense hardware, flagship gaming consoles |
| Proprietary / Multi-Lobe Asymmetrical | Custom patented spline curves with non-standard flank angles and variable center pins | Maximum (Engineered to withstand class 10.9/12.9 yield torque) | Maximum (Zero commercial bit availability globally) | Strictly Restricted (Driver keys serialized and restricted to OEM) | EV High-Voltage battery modules, smart meter metrology, weapon systems |
In high-throughput automated production, driver cam-out (the upward slipping of the driver bit from the fastener recess under torsional load) leads to damaged component surfaces, premature driver bit fatigue, and non-conforming pre-load tensions. Cross-recess and slotted drives inherently convert radial torque into axial ejection force due to tapered flanks. Conversely, Pin-in-Torx and Multi-Lobe Asymmetrical drives feature a 15-degree to near-zero drive flank angle, redirecting nearly 100% of driver output into rotational clamping force. This allows high automated RPM installations without stripping the internal security post.
How state-of-the-art multi-station cold heading, vertical tool and die integration, and automated optical laser sorting deliver peerless total cost of ownership (TCO) without quality compromise.
When international procurement directors evaluate security screw manufacturers, competitive advantage is dictated by three pillars: manufacturing throughput speed, die tooling innovation, and zero-defect quality control. Situated in Dongguan, Shaoguan, and Wuhan, YH Fastener’s manufacturing plants leverage the world’s most dense hardware industrial cluster, delivering precision-engineered parts with rapid prototype-to-mass-production turnarounds.
Utilizing high-speed 5-die and 6-die progressive cold-heading machines capable of cycling 200–350 parts per minute. Continuous grain-flow alignment provides up to 30% greater tensile and fatigue strength compared to machined alternatives, while generating virtually zero scrap material.
Zero Waste High Grain Density Class 8.8–12.9Proprietary punch and die manufacturing within our own CNC toolroom enables custom tamper-proof drive prototypes in just 3 to 5 business days. Tungsten carbide wire EDM tooling guarantees pin concentricity within ±0.015mm over production runs of several million units.
Micro-Tolerances 5-Day Tooling Custom DiesEvery security screw batch passes through high-speed glass-plate 360-degree optical sorting machines. Automated vision algorithms inspect pin height, recess depth, thread pitch integrity, and head diameter at 600 pieces/min, eliminating line-jamming burrs.
<10 PPM Defect Rate 100% Vision Check Robotic Feed ReadyWhere failure is not an option: Exploring specialized security fastener configurations engineered for harsh thermal, chemical, and mechanical operating realities across global markets.
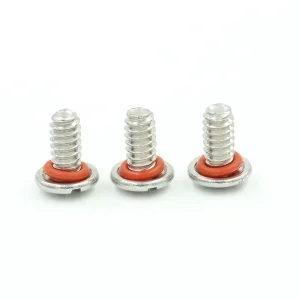
Lithium-ion battery top covers require dual functionality: extreme tamper prevention to protect against unauthorized service shocks, and IP67/IP68 hermetic sealing against moisture and road brine. Integrated silicone O-ring under-head designs ensure zero water ingress up to 5 bar pressure while pin-Torx drives restrict opening to certified battery recycling technicians.
IP68 Immersion Under-head O-Ring SS316 / Class 8.8Electricity, gas, and municipal water smart meters are primary targets for magnetic interference and physical current shunting. Miniature M2 to M3.5 stainless steel security pan-head screws with custom tri-lobe or pin-recess profiles prevent revenue diversion, safeguarding billions of kilowatt-hours across European, North American, and Asian power distribution grids.
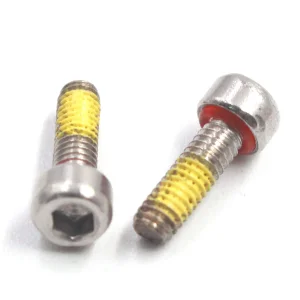
Anti-Tamper Revenue Micro-Diameters M1.6-M3 Corrosion ProofPayment terminal casings must comply with strict PCI-PTS (Payment Card Industry PIN Transaction Security) hardware physical tamper standards. Captive security fasteners embedded with internal break-away heads or pre-applied locking micro-encapsulated adhesive ensure that any attempt to drill or force open card reader mechanisms triggers hardware self-erasure.
PCI-PTS Compliance Nylon Patch Locking Anti-Drill SteelsFrom micro-dot laser cryptographic engraving to self-locking hybrid polymers, review the pioneering innovations transforming static screws into smart, tamper-evident assets.
The fastener industry is rapidly transcending basic metallurgy. As industrial ecosystems adopt digital twin models and strict ESG circular economic directives, security screws are developing advanced multi-functional capabilities:
Direct part marking via femtosecond UV laser pulses directly onto the fastener head surface. Each security screw carries an encrypted 2D data-matrix containing batch chemistry, heat treat batch number, and authentication certificates, directly readable via automated assembly vision systems.
Anti-Counterfeiting Digital Passport Laser EngravingTransitioning beyond traditional hex-chrome finishes to organic multi-layer micro-layer zinc flake finishes (Geomet, Dacromet) that eliminate hydrogen embrittlement risks in high-tensile 10.9/12.9 security fasteners while offering 1500+ hours salt spray defense.
Zero Embrittlement REACH Compliant Zinc Flake FinishFusing metal cold-formed screws with bonded elastomeric O-rings (Fluorosilicone, EPDM, Viton) seated within specialized under-head undercut grooves. This completely negates the requirement for secondary manual liquid sealants or discrete washers on the assembly floor.
Under-cut Grooving Zero Assembly Labor Pressure TightA vendor-evaluation framework designed for Supply Chain Directors and Quality Engineering Leads to de-risk fastener sourcing contracts, guarantee material traceability, and enforce strict PPAP protocols.
Procurement professionals managing international supply chains cannot afford fastener field failures. A broken screw head or a stripped drive recess inside an automotive inverter can paralyze an entire assembly plant, racking up hundreds of thousands of dollars in line-stoppage costs. When vetting security screw manufacturers, tier-1 industrial enterprises apply rigorous qualification criteria:
| Audit Parameter | Standard Baseline Requirement | YH Fastener Manufacturing Guarantee | Risk Mitigation Value to OEM |
|---|---|---|---|
| Quality System Certification | ISO 9001:2015 General Baseline | IATF 16949:2016 + ISO 14001:2015 fully audited automotive compliance across all workshops | Ensures rigorous continuous improvement, error-proofing (Poka-Yoke), and standardized FMEA management |
| Production Part Approval (PPAP) | Level 1 or Level 2 standard submissions | PPAP Level 3 Full Documentation: Control plans, gauge R&R, IMDS reports, dimensional checks | Guarantees complete process readiness and dimensional compliance prior to high-volume shipment release |
| Raw Material Chemistry & Origin | Generic mill test reports | 100% Traceable Steel Billets with optical emission spectrometer chemical composition verification | Eliminates risk of hydrogen embrittlement, unexpected cold-working cracking, and material substitution |
| Drive Recess Concentricity | ANSI / DIN standard runout (±0.08mm) | High-Precision Cold Heading (±0.02mm) centered pin alignment verified via optical shadowgraph | Guarantees smooth automatic robotic feeder insertion without bit cam-out or cross-threading damage |
| Hydrogen Embrittlement Relief | Ambient post-plate de-embrittlement bake | Mandatory 200°C–220°C 4–8 Hour Bake cycle monitored via automated digital thermal loggers | Prevents catastrophic delayed delayed fracture on Class 10.9/12.9 high-strength carbon steel fasteners |
Comprehensive technical guidance addressing torque ratings, galvanic corrosion prevention, tooling management, and non-standard custom manufacturing capabilities.
The insertion of an axial anti-tamper security pin reduces the contact cross-sectional surface area of the driver bit by roughly 10% to 18% compared to standard open recesses. However, because our cold heading dies maintain strict zero-degree flank angles and precision broached lobes (particularly in Pin-in-Torx profiles), radial torque transfer remains exceptionally efficient. We engineer our Class 8.8 and 10.9 security fasteners with sufficient recess depth to permit full seating torque without shearing the pin. For ultra-high torque applications, we recommend asymmetrical multi-lobe drives or deep socket configurations.
YH Fastener operates an auditable, restricted-tooling manufacturing protocol for OEM partners requiring proprietary tamper-proof security. We develop unique asymmetrical head profiles with customized key paths that are legally and contractually protected. Driver bit tooling is produced strictly in-house, serialized, and distributed solely to authorized OEM maintenance channels or verified logistics hubs, eliminating illicit secondary distribution across retail markets.
Direct metallic coupling between austenitic stainless steel (AISI 304 / 316) and cast aluminum alloys (such as ADC12 or A380) triggers aggressive galvanic corrosion when exposed to electrolyte solutions like moisture or road salt. To prevent this, YH Fastener provides three engineered solutions: 1) Non-conductive under-head elastomeric O-rings/washers that break electrical contact; 2) Micro-encapsulated organic barrier coatings (fluoropolymer / PTFE finishes); or 3) Specialty zinc-nickel plated alloy steel screws tailored to match the electrochemical potential of the aluminum mating component.
Because YH Fastener maintains a complete in-house CNC wire EDM die-sinking and heading toolroom in Dongguan, our prototype tooling lead-time is typically 5 to 7 working days from drawing sign-off. First Article Inspection (FAI) reports with physical samples are dispatched immediately via express air freight. Once approved, high-speed multi-station mass production runs deliver between 500,000 and 5,000,000 units within 15 to 22 working days, supported by flexible global shipping terms (FOB, CIF, DDP).
Self-sealing security screws combine a tamper-evident head drive with an engineered groove machined directly into the under-head bearing area. A high-grade silicone, Viton, or Buna-N O-ring is seated in this groove. When torqued to specification, the elastomeric ring is compressed metal-to-metal into a 360-degree hermetic seal (IP67/IP68 rated) that prevents fluid or vacuum egress while simultaneously absorbing high-frequency mechanical vibration and preventing accidental screw back-out.
Explore our specialized range of anti-loosening spring plungers, precision metric machine fasteners, and custom multi-head self-tapping assemblies engineered for rigorous global OEM specifications.
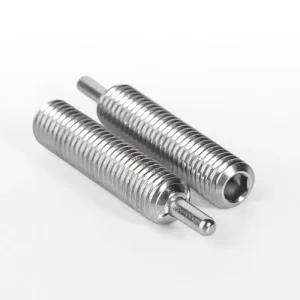
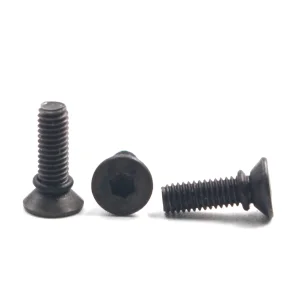
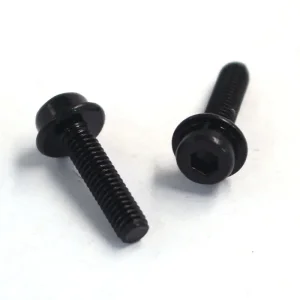

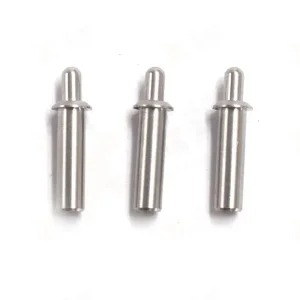
Whether you require high-volume standard Pin-Torx fasteners, IP67 self-sealing O-ring machine screws, or customized proprietary security tooling developed from CAD step files, YH Fastener delivers end-to-end metallurgical expertise with 30 years of certified IATF 16949 / ISO 9001 precision manufacturing.
