Zero-defect cold heading, micro-threading, and automated optical sorting
Review our highest-volume production items deployed across Tier-1 OEM electronic chassis, marine-grade sealing assemblies, and vibration-proof robotic control cabinets.

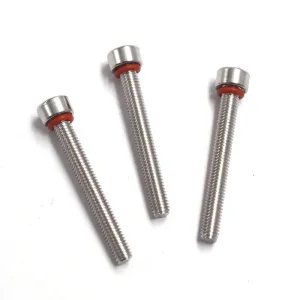
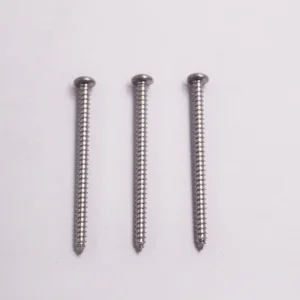
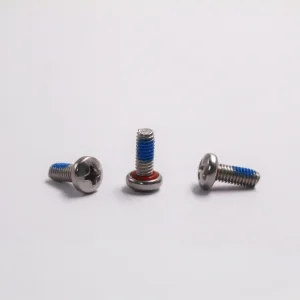
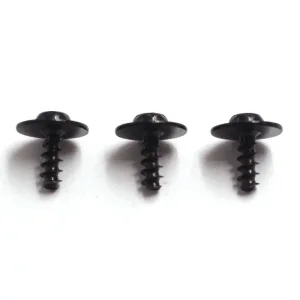

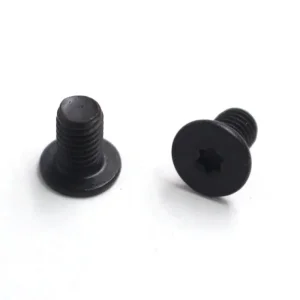
The modern manufacturing paradigm is shifting away from standardized bulk fasteners toward highly specialized, multi-functional fastening hardware. Fasteners are no longer passive clamping elements; they now serve as hermetic seals, electrical conductors, thermal dissipate paths, and active anti-tamper barriers.
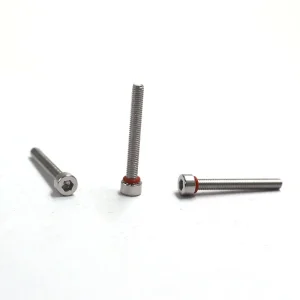
As electrical components move from sheltered cabins to exposed chassis and harsh marine environments, fasteners must prevent fluid and particulate migration. Integrated under-head silicone, fluorosilicone, and EPDM O-rings engineered into cold-headed undercut grooves provide permanent seals under variable thermal expansion cycles without extrusion failure.
Vibration-induced back-off in high-frequency electric drivetrains has made traditional spring washers obsolete. Pre-applied micro-encapsulated anaerobic adhesives (DIN 267-27) and fused 360-degree polyamide/blue nylon patches (DIN 267-28) generate constant prevailing torque, preventing catastrophic loosening across extreme temperature boundaries (-50°C to +150°C).
Engineering thermoplastics such as glass-filled PA66, PBT, and PPS demand optimized 30-degree flank thread geometry (PT Screws) rather than standard 60-degree machine threads. This reduces radial bursting stresses by over 38%, minimizes core boss crack hazards, and maximizes clamp-load retention during rapid automated robotic driving cycles.
International OEM procurement directors and supply chain engineers evaluating Chinese manufacturing facilities require verification that extends far beyond baseline commercial quotes. Structural reliability is governed by quantifiable metallurgical parameters and certified process controls.
| Evaluation Vector | Critical Engineering Metric | YH Fastener Manufacturing Standard | Impact on Assembly Life |
|---|---|---|---|
| Metallurgical Integrity | Wire rod grain structure, decarburization depth | 100% certified austenitic SS304/316 & alloy wire rod | Prevents head shearing and fatigue stress fracturing under cyclic shock. |
| Dimensional Consistency | Thread pitch diameter, recess depth (Cpk ≥ 1.67) | Keyence laser multi-axis optical sorters (0 PPM target) | Guarantees jam-free automatic bowl feeder and robotic pick-and-place lines. |
| Surface Engineering | Coating thickness (μm), Cr6+ free passivation | Eco-friendly trivalent zinc, zinc-nickel alloy, black Geomet | Exceeds 720 to 1,500 hours neutral salt spray testing without red rust formation. |
| Vibration Resistance | Prevailing torque retention under Junkers testing | Nylon patch 360-degree fusion, DIN 267 compliant patch | Precludes joint relaxation and electrical disconnect in automotive powertrains. |
| Traceability & Auditing | Lot numbering, raw mill test report, PPAP Level 3 | Full digital tracking from billet heating to final sealed packaging | Full regulatory audit defense for aerospace, medical, and defense contracts. |
In robotic screw-driving cells running 0.8-second cycle times, a single dimensional burr or deformed drive recess causes expensive line downtime. YH Fastener integrates multi-camera visual sorting machines that verify drive recess concentricity, thread pitch linearity, and total length at speeds up to 1,200 parts per minute.
High-tensile fasteners (Class 8.8, 10.9, 12.9) exposed to electroplating pickling acid risk catastrophic delayed brittle fracture. Our facility executes immediate post-plating thermal baking protocols (200°C–230°C for 4 to 8 hours) strictly compliant with ISO 4042 to ensure thorough atomic hydrogen expulsion.
Direct-from-factory partnerships eliminate multiple layers of distributor margins. Consolidated tooling runs, internal wire-drawing facilities, and integrated secondary operations (nylon patching, washer captive assembly) provide sustainable 18% to 32% landed cost reductions for Tier-1 supply chains.
From extreme subsea environments to high-voltage automotive power electronics, precision fasteners are customized to match substrate metallurgy, torque tension constraints, and galvanic corrosion boundaries.
Lithium-ion pack enclosures demand fasteners that maintain electromagnetic shielding (EMI), prevent coolant leakage, and withstand severe vibration testing. Our custom PT carbon-steel and SS304 screws with captive sealing washers deliver certified IP68 water sealing and constant clamping torque across the entire battery lifecycle.
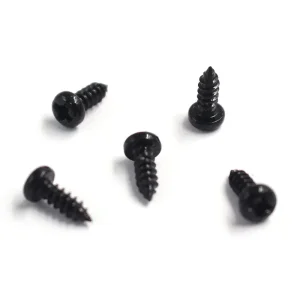
Precision PCB mounting and aluminum die-cast housings require ultra-fine threads (M1.4 to M4) with tight dimensional tolerances to prevent stripped threads and metal debris contamination. Our Phillips pan head machine screws feature Class 6g/6h thread tolerances and micro-passivation for cleanroom assembly readiness.
5G base station antennae, solar inverter junctions, and outdoor industrial control boxes face continuous UV exposure, wind shear, and corrosive salt air. Our specialized sealing bolts and anti-loosening nylon patch screws eliminate gasket degradation and prevent moisture siphonage via the internal thread roots.
Navigating global industrial compliance mandates requires a rigorous testing infrastructure. YH Fastener operates fully equipped in-house physical and chemical testing laboratories verifying full compliance with worldwide statutory and environmental frameworks.
Our multi-facility manufacturing plants in Dongguan, Shaoguan, and Wuhan enforce closed-loop statistical process control (SPC). Every custom run supports complete APQP documentation, FMEA analysis, control plans, and PPAP Level 3 submissions (dimensional results, material certs, salt spray reports).
In full compliance with EU Directive 2011/65/EU (RoHS 3) and Regulation (EC) No 1907/2006 (REACH SVHC list), our plating and raw materials are tested regularly using X-ray fluorescence (XRF) and ICP-OES spectrometers to guarantee zero trace contamination of lead, mercury, cadmium, or hexavalent chromium.
To insulate international clients against freight fluctuations and port disruptions, YH Fastener facilitates Vendor-Managed Inventory (VMI) agreements, safety buffer stocking programs, and flexible DDP/FOB/CIF shipping logistics serving OEM plants across North America, Europe, Japan, and Southeast Asia.
Our dedicated engineering laboratory continuously refines cold forming dynamics, micro-alloying, and smart sensor integration to meet the higher strength-to-weight ratios and intelligence demands of tomorrow's industrial assemblies.
Transitioning aerospace-grade titanium (Gr2/Gr5) and cold-formable 7075 aluminum into high-speed heading processes to achieve 45% mass reduction in airborne and humanoid robotic joints without yielding tensile capacity.
Implementing zinc-flake plus inorganic nano-ceramic topcoats yielding 2,000+ hour neutral salt spray resistance with controlled frictional coefficients (μ = 0.10 - 0.15), eliminating galling in automated power tools.
Direct AI-assisted inline tool-wear detection inside multi-station cold headers, adjusting heading dies in sub-micron increments before dimensional drift occurs, securing near-zero process scrap.
Embedding micro-piezoelectric thin films under bolt heads to monitor live clamping preload and micro-loosening in critical energy infrastructure, communicating via RFID/NFC protocols during maintenance audits.
Engineered for high mechanical shear, IP67 enclosure seal, and anti-tamper security
Review our precision application hardware engineered for waterproof electronic enclosures, automotive EV battery housings, and high-strength machinery framing.
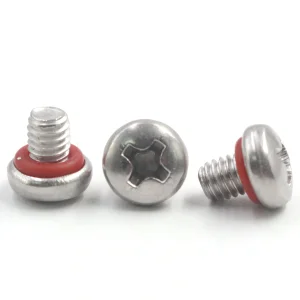


Detailed technical responses formulated by senior application engineers addressing fastener fatigue life, torque calibration, sealing mechanics, and global export qualification.
Standard fasteners with flat washers squeeze the elastomer outward, resulting in premature tensile pinching, extrusion rupture, and loss of seal. Our precision sealing screws incorporate a cold-headed annular undercut groove beneath the screw head. During assembly, the elastomeric O-ring (silicone, Buna-N, Viton, or fluorosilicone) flows into the constrained groove, experiencing strictly controlled volumetric compression (typically 25% to 30%). This isolates the O-ring from direct sliding friction while achieving complete hermetic sealing across the threaded boundary capable of withstanding internal pressures up to 100 psi.
Traditional thread-cutting or standard self-tapping screws use a 60° profile angle designed for ductile sheet metals. When driven into brittle or viscoelastic plastics (e.g., glass-filled PA, ABS, PBT), a 60° thread induces severe outward radial burst forces that crack boss structures. In contrast, specialized PT screws employ a narrow 30° thread flank angle and an enlarged pitch. This geometry reduces radial expansion stress by over 38%, allows maximum plastic displacement between threads, dramatically enhances pull-out resistance, and facilitates multiple disassembly-reassembly cycles without stripping the plastic core.
Helical split lock washers function only under static preloads; once dynamic cyclic vibration or transverse shock exceeds the joint clamp force, split washers flatten, gouge joint seating faces, and often act as a bearing slip surface that accelerates fastener back-out. In comparison, fused nylon patches (DIN 267-28) apply a permanent prevailing torque by deforming elastically against internal mating thread flanks. This creates a metal-to-metal wedge contact on opposite flank faces that remains dampening and self-locking even if initial bolt tension experiences relaxation due to thermal expansion.
Every production run engineered by YH Fastener is supported by complete traceability and quality documentation conforming to ISO 9001 and IATF 16949 requirements. Standard deliverables include Raw Material Mill Test Certificates (spectrometric chemical composition and mechanical tensile verification), Initial Sample Inspection Reports (ISIR / Full Dimensional Cpk studies), Plating Thickness & Salt Spray Test Reports (ASTM B117), and formal Automotive PPAP Level 3 documentation dossiers upon program qualification.
Send our technical team your 2D CAD engineering prints (.dwg, .pdf) or 3D step files (.step, .igs). Our application engineers will evaluate cold-heading manufacturability, recommend optimal materials and surface treatments, and deliver a comprehensive DFM review within 24 hours.
