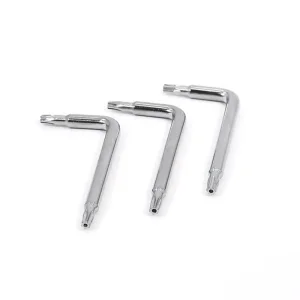
Directly integrated with cold-forged L-type Torx key production lines, our precision screw series provides matched recess tolerances to eliminate cam-out, lower radial slippage, and optimize robotic torque transmission.




As automated tightening, higher preloads, and lightweight alloys dominate modern mechanical joints, standard internal hex (Allen) and cross-recess drives increasingly fall short of critical yield requirements. The 6-lobe Torx design (ISO 10664) represents an engineered paradigm shift.
Conventional hex keys exert force at a 60° contact angle, causing substantial radial outward pressure that rounds female recesses. An L-type Torx key functions with a drive angle close to 15°, practically eliminating cam-out forces, reducing operator fatigue, and preserving recess geometry across repetitive service cycles.
Modern public infrastructure, 5G enclosures, and high-value consumer electronics demand unauthorized disassembly prevention. Custom ODM L-keys feature precision-drilled center apertures engineered to mate seamlessly with security Torx pin fasteners, maintaining high torsional rigidity while deterring field tampering.
The asymmetric 90° geometry of the L-type key provides dual application modes: the long arm delivers extended reach into recessed chassis recesses, while the short arm provides maximum mechanical advantage for initial thread breakaway or final precision seat torquing.
Sourcing L-type Torx wrenches independently from matching machine screws routinely results in tolerance stack-up errors. When the key’s lobe radius exceeds fastener recess tolerance by as little as 0.015 mm, point loading replaces area loading, causing premature brittle fracture under high torque. Yu-Huang's integrated manufacturing pairs tool profile tooling with internal fastener heading punches for guaranteed 100% surface engagement.
Tier-1 automotive contractors, consumer electronics conglomerates, and industrial equipment builders are transforming how manual service wrenches are specified. Off-the-shelf consumer hand tools are no longer acceptable for high-liability assemblies.
In high-density optical transceiver modules, hearing aids, surgical robotics, and smartphone gimbal assemblies, fastener diameters drop below M1.2. Global procurement teams demand ultra-micro ODM L-keys forged from specialized vacuum-degassed alloy steels to achieve torsional resistance without plastic deformation down to T1 micro-profiles.
Electric Vehicle (EV) battery packs and charging infrastructure mandate maintenance tools that prevent accidental short circuits. Sourcing programs increasingly require dual-compound insulated dipped coatings (IEC 60900 compliant) over hardened chrome-vanadium L-keys, tested to withstand 10,000V AC dielectric proof tests.
Aerospace ground equipment and cleanroom semiconductor machinery demand complete lot traceability. Every L-key is laser-etched with batch numbers, dimensional sizes, and manufacturer identifiers, enabling immediate failure-mode isolation within ISO-certified quality tracking databases.
| Torx Size (ISO 10664) | Point-to-Point (mm) | Recommended Max Torque (N·m) | Standard Material Alloys | Hardness Range (HRC) | Common Industrial Applications |
|---|---|---|---|---|---|
| T1 – T4 | 0.90 – 1.28 | 0.10 – 0.45 | High-Carbon S2 / Tool Steel | 58 – 62 HRC | Smart wearables, micro-optics, drones |
| T5 – T8 | 1.42 – 2.31 | 0.75 – 2.60 | Alloy S2 / SVCM / Cr-V | 56 – 60 HRC | Consumer laptops, SSD housings, automotive radar |
| T9 – T15 | 2.50 – 3.27 | 3.80 – 7.70 | Chromium-Vanadium (6150) | 54 – 58 HRC | Automotive interiors, lighting, medical gear |
| T20 – T30 | 3.86 – 5.52 | 10.5 – 37.0 | Forged Cr-V / S2 Industrial | 52 – 56 HRC | EV battery modules, machine tools, solar mounts |
| T40 – T60 | 6.65 – 13.25 | 54.0 – 380.0 | Heat-Treated SNCM / Cr-Mo | 50 – 54 HRC | Heavy mechanical fixtures, structural chassis, wind power |
Operating from an advanced 20,000 m² industrial footprint spanning Dongguan, Shaoguan, and Wuhan, Yu-Huang Electronics (YH Fastener) bridges the gap between precision toolmaker craftsmanship and automated mass production.
Every batch of Cr-V 6150, S2 tool steel, and SUS304/316 wire rod undergoes X-ray fluorescence (XRF) and spark emission spectrometry to confirm carbon, silicon, and molybdenum ratios before processing.
Multi-stage automated cold-heading and high-precision CNC bending work cells form standard and custom-length L-key geometries without micro-cracking at the 90° stress concentration corner.
Continuous mesh-belt furnaces with nitrogen-protected carburizing control atmosphere composition, preventing surface decarburization while securing uniform bulk hardness (up to 62 HRC) and optimal toughness.
Automated high-speed CCD vision sorting machines measure profile run-out, corner radius, chamfer depth, and key drive lobes with sub-micron precision, enforcing true zero-defect 0-PPM quality delivery.
Deep metallurgical & fastener manufacturing experience since 1998.
Synchronized facilities across Dongguan, Shaoguan, and Wuhan, China.
Torque threshold, dimensional, and salt-spray testing before dispatch.
Trusted by OEMs across North America, Europe, Japan, and Southeast Asia.
From cleanrooms to corrosive outdoor environments, customized L-type Torx keys and matching precision fasteners are formulated to meet rigorous thermal, mechanical, and regulatory standards.
In high-vibration battery tray lids, electric drive units, and ADAS sensor modules, engineers specify tamper-resistant Torx Plus® and security Torx screws paired with matched L-keys. Tight lobular tolerancing ensures factory and service technicians deliver specified clamping force without damaging under-head sealing gaskets.
Vacuum wafer handling equipment requires non-magnetic, particle-free fastening systems. YH manufactures electropolished SUS316 stainless steel L-keys and captive Torx screws that resist chloride stress corrosion, produce zero zinc flaking, and undergo ultra-pure ultrasonic degassing washes before cleanroom vacuum packaging.
Remote radio units (RRUs) installed on cell towers face coastal salt-fog, torrential rains, and temperature swings from -40°C to +85°C. YH supplies specialized L-type wrenches and anti-galling Torx fasteners treated with multi-layer Dacromet and Geomet coatings exceeding 1,000 hours of neutral salt spray testing (ASTM B117).
An industrial-grade Torx L-key must balance extreme surface hardness (to deter lobe rounding) with high core toughness (to avoid sudden brittle fracture under shock over-torquing).
Alloyed with silicon, manganese, molybdenum, and vanadium, S2 steel provides superior elasticity and impact resistance. Hardened to 58–62 HRC, S2 is our recommended substrate for heavy-duty assembly lines, robotic maintenance kits, and high-frequency manual cycling.
The global benchmark for mechanical integrity, Cr-V achieves balanced tensile strength and cost efficiency. Suitable for large commercial OEM tool sets, consumer product maintenance kits, and standard industrial maintenance tools conforming to DIN ISO 2936 and ISO 10664.
Choose from black manganese phosphating for enhanced oil retention and zero hydrogen embrittlement; satin micro-matte chrome for wear resistance; black zinc plating for aesthetics; or physical vapor deposition (PVD) Titanium Nitride (TiN) coating for severe abrasive wear environments.
Comprehensive engineering guidance addressing common procurement inquiries, technical calculations, certifications, and customization parameters.
True ODM suppliers like Yu-Huang operate dedicated wire drawing, cold-heading, heat-treating, and CNC bending infrastructure in-house. This gives buyers direct engineering control over steel metallurgy, dimensional arm-length ratios, custom chamfer angles, laser engraving, and custom-toleranced star profiles rather than relying on pre-packaged commodity inventory with unverified metallurgy.
Yes. In addition to standard short-arm and extra-long arm configurations, our programmable CNC wire-bending centers can produce custom 100° or 110° clearance angles, extended stubby configurations for ultra-shallow enclosures, ball-end Torx profiles for 25° off-axis entry, and dual-drive configurations (e.g., standard Torx on long arm, Tamper-Resistant pin hole on short arm).
High-strength steels hardened above 40 HRC are susceptible to hydrogen embrittlement during acid pickling and electroplating. YH implements automated mechanical descaling and strictly adheres to post-plating hydrogen bake-out protocols (200°C–220°C for 4 to 8 hours within 1 hour after electroplating) verified through sustained load testing per ISO 15330.
Our facilities operate under ISO 9001, ISO 14001, and IATF 16949 automotive quality management certifications. Every production shipment is accompanied by complete inspection documentation, including 3.1 Material Test Reports (chemical analysis & tensile data), hardness test charts, dimensional CMM/optical reports, and RoHS/REACH SVHC declarations.
We supply custom turn-key packaging solutions for global retail tool brands and equipment inclusion kits. Capabilities include fiber laser etching of logos and sizing codes directly on wrench shanks, custom-molded color-coded plastic clip holders, ballistic nylon rollout pouches, and automated heat-shrink polybagging with custom customer barcodes and GS1 DataMatrix tags.
Rapid tooling prototyping for custom L-type Torx wrenches typically completes in 5 to 7 working days. For standard raw material diameters in Cr-V or S2, production MOQs range between 1,000 and 5,000 units depending on size, while custom exotic alloys or miniature sizes below T4 are confirmed individually upon drawing review within 24 hours.
Expand your assembly bill of materials with our precision machine screws, thread-forming fasteners, and custom drive accessories engineered in strict dimensional alignment with our ODM Torx key line.