

Engineered for vibration-damping, environmental isolation, and micro-tolerance performance. Factory-direct supply produced through automated multi-station cold heading.

Operating across 20,000 m² of modern, multi-site cold heading, high-speed thread rolling, and cleanroom automated sorting facilities in Dongguan, Shaoguan, and Wuhan.
Evaluating grain flow continuity, recess stability, and anti-galling chemistry in austenitic stainless steel machine screws under severe cyclic loading.
Unlike machined fasteners that shear austenitic grain structures, multi-die cold heading re-orients the metallurgical flow lines unbroken around the pan radius. This eliminates stress risers where fatigue failure typically initiates under high pre-loads.
Austenitic stainless steels rely on a chromium-rich passive film (Cr₂O₃) that naturally self-heals in atmospheric oxygen. Our automated immersion lines employ validated citric or nitric acid passivation cycles (ASTM A967 compliant) to dissolve embedded free-iron microparticles.
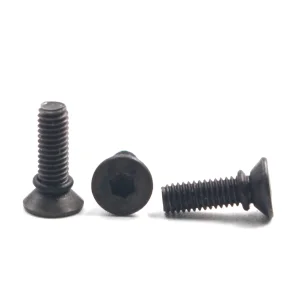
Whether utilizing Phillips, Torx (six-lobe), or custom tamper-proof drives, the tool geometry during high-speed punch formation enforces critical penetration depths. This controls tool cam-out and drive degradation during semi-automated robotics tightening.
Direct comparative reference data for custom stainless steel alloy selection in precision machine screw design according to ISO 3506-1 and ASTM guidelines.
| Material Designation | Yield Strength Rp0.2 (MPa) | Tensile Strength Rm (MPa) | PREN Rating | Primary Industrial Use-Case |
|---|---|---|---|---|
| AISI 304 / A2-70 | 450 min. | 700 min. | 18.0 - 20.0 | Consumer Electronics, Indoor Telecommunications, Standard Enclosures |
| AISI 316 / A4-70 | 450 min. | 700 min. | 23.0 - 25.0 | Marine Electronics, Chemical Processing, Exterior EV Enclosures |
| AISI 316L (Low Carbon) | 400 min. | 650 min. | 23.0 - 25.0 | Welded Assemblies, Medical Instrumentation, Ultra-Pure Process Lines |
| Duplex UNS S31803 | 650 min. | 800 min. | 32.0 - 35.0 | High-Chloride Environments, Heavy Petrochemical, Structural Naval |
Integrating multi-stage cold-heading cells, multi-camera laser sorting, and full traceability architectures to insulate international supply chains against disruption.
With three synchronized manufacturing facilities situated in Dongguan, Shaoguan, and Wuhan, internal capacity balance shields high-volume procurement programs from regional bottlenecks or raw material supply halts.
Eliminate line-stopping assembly anomalies. Our continuous automated inspection glass tables identify thread pitch aberrations, head concentricity runout, micro-burrs, and plating variations at rates topping 800 parts per minute.
Every barrel of cold-heading wire rod is tagged with raw mill heat chemistry records. From spheroidizing annealing to final thread rolling and passivation, full documentation packets (PPAP Level 3 available) follow all batch deliveries.
Precision pan-head screws operate as essential mechanical linkages across mission-critical equipment frameworks globally.
Battery management systems (BMS), inverter chassis assembly, and sensor mounts demanding IATF 16949-grade quality and continuous electrical isolation.
Non-magnetic, anti-galling surgical enclosure screws and internal diagnostic assemblies compliant with rigorous sterilization washdowns.
5G small-cell installations and IP67 weather-shielded junction boxes secured via integrated elastomeric sealing machine screws.
Micro-diameter M1.2 to M3 pan-head fasteners with pre-applied threadlockers for internal motherboard, display, and camera retention.
Forward-looking innovations addressing emerging requirements across smart automation, weight reduction, and extreme environmental exposure.
Replacing traditional wet oils with micro-encapsulated MoS₂ or PTFE dry coatings directly bonded to 316-grade threads. Eliminates assembly line contamination while stabilizing clamp-load scatter to ±5%.
Proprietary modified-recess pan heads designed specifically for rapid magnetic and vacuum vacuum-assist positioning in 6-axis collaborative robotic assembly cells.
R&D scaling for sustainable, high-manganese nitrogen-stabilized stainless grades that deliver 1.5x the tensile strength of conventional 304 without compromising ductility or chemical passivity.
Ensuring legal, chemical, and operational clearance across tier-1 multi-national supply chain audits.
All plating finishes, anti-vibration patches (such as blue nylon or polymide resins), and basic wire stock are batch-tested via ICP-OES to guarantee zero banned phthalates, lead, or hexavalent chromium.
For automotive and mission-critical OEM accounts, we deliver Process Flow Diagrams (PFD), Process Failure Mode and Effects Analysis (PFMEA), Control Plans, Gage R&R, and Dimensional Results per AIAG manuals.
Supporting DDP, CIF, and FOB structures with flexible bonded warehouse inventory programs (VMI/Kanban) to insulate long-lead international transit timelines against sudden volume surges.
Explore our complementary engineered configurations including non-standard sealing components, brass materials, and high-tensile carbon hardware.


Practical technical advice written by our application engineers for global sourcing managers and hardware mechanical designers.
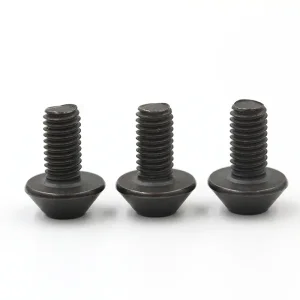
Pan-head profiles feature a substantially broader, flat under-head contact surface compared to button or round head equivalents. This configuration spreads tightening clamp loads evenly across a wider surface area without requiring independent flat washers, minimizing deformation on softer mating substrates like aluminum castings and engineered plastics.
Thread galling occurs when friction breaks down protective chromium oxide films under high contact forces. We implement controlled anti-friction surface treatments—including dry micro-wax films, PTFE coatings, pre-applied chemical microencapsulated patches, or controlled dissimilar hardness grades (pairing A2-70 screws with A4-80 nuts).
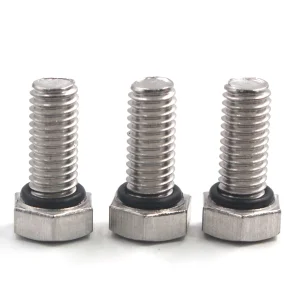
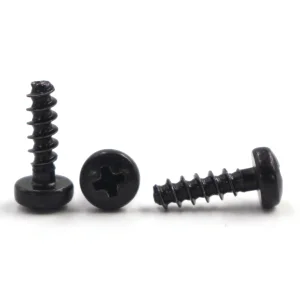
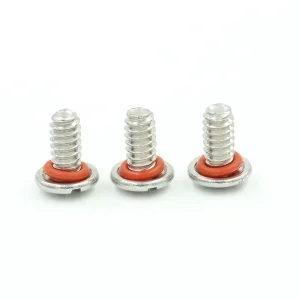
Beyond standard metric ISO (coarse and fine pitch), our precision rolling dies accommodate specialized thread forms including TP trilobular threads for direct thread-forming in plastic housings, High-Low alternate threads, self-tapping styles AB/B, captive relief shanks, and self-sealing recessed undercuts for silicone O-rings.
We supply a complete Design for Manufacturability (DFM) assessment, tooling cost estimates, and unit pricing within 24 hours of receiving formal CAD files (2D PDF/DXF or 3D STEP). Rapid physical prototyping via in-house tooling shops typically delivers verified first-article samples in 7 to 10 working days.