Direct factory manufacturing of IP-rated self-sealing fasteners, tamper-proof security drives, and vibration-proof machine screws designed for severe outdoor installations.


Outdoor electronic and electrical enclosures face simultaneous stresses: thermal expansion differentials, electrolytic oxidation, dynamic wind shear, and high-pressure water ingress. Our engineering framework eliminates premature joint degradation.
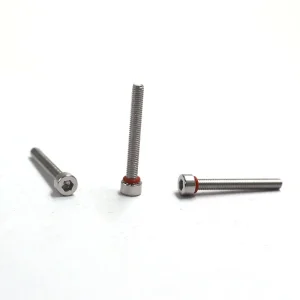
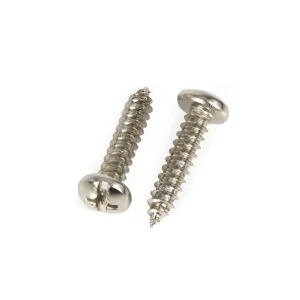
Standard screw threads allow micro-pathway fluid leakage via helix gaps. Our precision-engineered self-sealing screws feature an integrated under-head annular groove containing a vulcanized elastomeric O-ring (Silicone, Viton, EPDM, or Nitrile). When tightened to specified torque, the elastomeric element undergoes controlled 30% compression, delivering a reliable 360-degree seal rated up to IP67, IP68, and IP69K.
Mating austenitic stainless steel fasteners (A2-70 / SUS304 or A4-80 / SUS316) directly into extruded or die-cast aluminum enclosure cabinets triggers aggressive bimetallic galvanic decay in coastal or saline environments. We formulate specialized inorganic barrier films, zinc-nickel plating (12-16% Ni fraction), or fluoropolymer Dacromet/Geomet barriers to neutralize anodic dissolution.
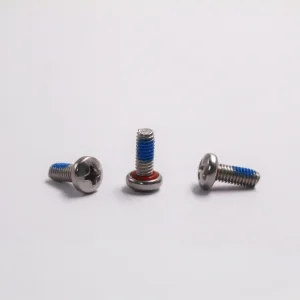
Environmental temperature cycling between -40°C and +85°C produces differential contraction across plastic and aluminum substrates, generating bolt preload relaxation. By bonding engineered polyamide (nylon) patches or micro-encapsulated anaerobic adhesives (DIN 267-27) directly across active thread engagements, our assemblies resist continuous multi-axis vibration.
| Alloy & Grade | Yield Strength (MPa) | Salt Spray Resistance (NSS) | Operating Temperature | Primary Outdoor Enclosure Application |
|---|---|---|---|---|
| Austenitic SUS304 / A2-70 | 450 - 600 | 400 - 600 Hours (Passivated) | -196°C to +400°C | Standard industrial NEMA 4 enclosures, general telecommunications, metering boxes. Cost-Effective |
| Marine Grade SUS316 / A4-80 | 600 - 800 | 1,200 - 2,000 Hours | -196°C to +500°C | Offshore wind control boxes, coastal 5G active antenna units, chemical processing facilities. Pitting Resistant |
| Duplex 2205 (S32205) | 650 - 850 | > 3,000 Hours (Severe Marine) | -50°C to +300°C | Subsea junction boxes, splash-zone maritime monitoring, harsh industrial acid environments. High Yield |
| Alloy Steel + Geomet 500B | 800 - 1040 (Class 10.9) | 1,500 Hours (No Red Rust) | -50°C to +260°C | Structural mounting brackets for utility-scale solar PV combiner boxes, transformer casings. High Tensile |
Yu-Huang Electronics Dongguan Co., Ltd. (YH Fastener) combines 30 years of cold-heading tooling expertise with over 20,000 m² of modern manufacturing floor space, eliminating intermediate broker margins and production latency.
Founded on high-precision precision cold heading, thread rolling, and tooling innovation.
Distributed across three strategic plants in Dongguan, Shaoguan, and Wuhan, China.
Full automated multi-sensor optical sorting ensuring zero-defect feeding on robot lines.
Long-term partnerships across North America, Germany, Japan, Scandinavia, and Australia.
Unlike simple trading entities, our facility maintains a dedicated mold-making workshop. We produce carbide cold-heading punches, multi-station transfer dies, and thread-rolling cylindrical dies in-house. Rapid prototype validation runs within 5-7 working days from drawing sign-off.
Our plants feature automated O-ring groove undercutting, continuous controlled-atmosphere heat treatment belt furnaces, nylon patch dispensing lines, and rotary washing stations to ensure surgical cleanliness before automated camera sorting.
Direct raw material allocation from tier-1 steel mills (Baosteel, Walsin Lihwa). Every incoming coil is inspected for chemical composition (spectrometer), decarburization, and inclusion ratings, with complete EN 10204 Type 3.1 certification per production batch.
Tier-1 industrial equipment and automotive electronics OEMs require stringent verification prior to vendor approval. Our quality management system matches high-demand international compliance protocols.
Full APQP management methodology with Production Part Approval Process (PPAP) Level 3 documentation, including Process FMEA, Control Plans, Gage R&R, and dimensional layout studies.
Zero hazardous chemical threshold. Fastener plating and passivations comply strictly with EU RoHS Directive 2011/65/EU and REACH SVHC lists. Direct IMDS (International Material Data System) submission ready.
High-speed glass turntable optical inspection machines measure thread pitch diameter, total shank length, recess concentricity, and under-head washer seating to guarantee automated assembly feed reliability.
Vendor Managed Inventory (VMI) frameworks and regional safety buffers (Shenzhen / Hong Kong forwarding hubs) ensure just-in-time dispatch with zero supply disruption across global production schedules.
From remote telecom antenna arrays to high-voltage solar energy storage containers, our specialized fasteners perform where equipment replacement costs make joint failure unacceptable.
Pole-mounted active antenna units (AAUs) and remote radio heads (RRHs) face intense wind-induced harmonic resonance and solar UV radiation. Fastener solutions: Stainless steel captive sealing screws with bonded blue nylon patches to prevent panel drop while preventing internal electronics water exposure.
Utility-scale photovoltaic combiner enclosures and battery energy storage system (BESS) racks operate in extreme desert conditions with daily 40°C temperature shifts. Fastener solutions: Class 8.8 and SUS304 pan head machine screws with non-conductive dielectric sealing washers.
Public-facing high-power charging kiosks require anti-vandalism defense combined with dustproof sealing (NEMA 3R / IP54+). Fastener solutions: Pin-in-Torx security tamper-proof screws, matched hardened L-keys, and captive stainless steel panel fasteners for maintenance doors.
Wayside railway switching boxes withstand continuous ground vibration from passing freight trains. Fastener solutions: SEMS combination screws with captured Belleville conical spring washers to maintain continuous axial bolt clamping force without relaxation.
Desalination units, harbor telemetry, and offshore oil platform instrumentation enclosures face constant salt aerosol. Fastener solutions: Molybdenum-bearing SUS316 and Duplex 2205 fasteners treated with electro-polishing and proprietary passivating films.
Micro-enclosures for air quality sensors, surveillance hubs, and municipal water monitors demand compact thread-forming PT screws for engineered plastics (Polycarbonate, ABS-PC blends) that prevent boss cracking under field weathering.
Next-generation outdoor hardware is evolving beyond simple passive mechanical joining toward multi-functional sealing, lightweight composite integration, and automated assembly optimization.
Rather than relying solely on manually inserted rubber gaskets or separate liquid threadlockers on the factory line, manufacturers are shifting to dry-to-the-touch micro-encapsulated coatings (e.g., precote 30, Scotch-Grip). Upon threading into mating tapped holes, internal capsules rupture and initiate room-temperature anaerobic cure, establishing simultaneous mechanical locking and 10 bar fluid barrier sealing.
Cold-welding (galling) remains the bane of automated stainless steel fastener installation in automated outdoor housing lines. Novel MoS2 (Molybdenum Disulfide) and PTFE-doped inorganic thin-film dry lubricants eliminate thread friction spikes, enabling precise clamp force torque control at rapid assembly speeds without cross-threading or seizing.
Telecommunications operators and utility companies increasingly mandate captive fastener assemblies on outdoor equipment doors. Using cold-headed reduced shanks and matching press-fit panel grommets, our captive screws stay permanently retained to the outer panel during opening, preventing hardware drops in gravel, grass, or snow during technician site maintenance.
Answers to detailed technical inquiries from engineering leads, quality auditors, and global supply managers.
Self-sealing screws integrate a precision cold-headed undercut groove located directly beneath the fastener head. An elastomeric silicone or fluorocarbon (Viton / FKM) O-ring is fitted into this annular cavity. When the fastener is seated against a flat enclosure surface and tightened to specified torque, the elastomeric ring is compressed within the controlled cavity boundaries. This eliminates lateral elastomer extrusion, filling all micro-voids between the fastener shank, clearance hole, and housing surface to block moisture, dust, and hydraulic pressure up to IP68 immersion levels.
When pairing stainless steel screws (austenitic 304/316) with cast aluminum enclosures (e.g., A380, ADC12), an electrochemical galvanic couple forms in the presence of conductive moisture. To prevent accelerated aluminum corrosion, we recommend: 1) Applying an inorganic zinc-nickel (12-16% Ni) conversion coating or Geomet 500 coating on high-strength steel fasteners, which exhibits neutral electrode potential against aluminum; 2) Utilizing passivated SUS316 fasteners fitted with non-conductive dielectric nylon/polyamide isolation washers; or 3) Employing pre-applied sealants that form a continuous insulating barrier along the thread flank.
Every shipment is delivered with comprehensive quality documentation, including: EN 10204 Type 3.1 Mill Test Certificates for raw wire chemistry; Full Dimensional Inspection Reports (CMM & optical projector data); ASTM B117 Neutral Salt Spray Test Reports; Plating Thickness XRF verification; RoHS & REACH Compliance Declarations; and, where agreed for automotive programs, complete PPAP Level 3 documentation packages (IMDS, Control Plan, PFMEA, Gage R&R, and Capability Studies with Cpk > 1.67).
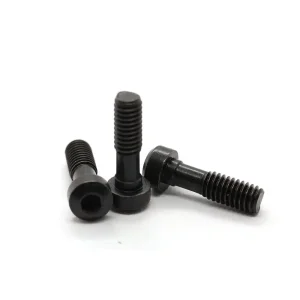
Captive screws feature an unthreaded relief shank between the threaded portion and the head, paired with a captive retainer washer, snap-in ferrule, or threaded retaining bushing on the enclosure cover. When technicians unscrew the cover for routine filter changes or wiring servicing, the fastener releases from the internal frame but remains mechanically secured to the door panel. This eliminates the risk of dropped screws falling into high-voltage switchgear or lost in outdoor terrain.
Yes. Our in-house engineering team works directly with STEP, IGES, SolidWorks, and 2D DWG/PDF drawings. We review tolerance stack-up, thread forming standards, cold-heading grain flow feasibility, and surface treatment requirements. With internal mold fabrication, sample prototypes are delivered in 7 to 10 working days, followed by rapid multi-station cold heading tool scaling for full-volume production runs.
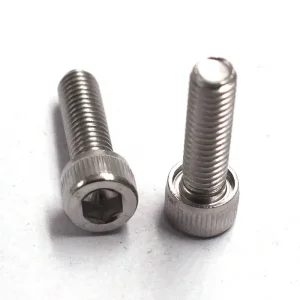
Explore our specialized heavy-duty machine bolts, anti-vibration nylon patched screws, and knurled manual adjustment fasteners designed for industrial machinery and electronic equipment enclosures.




Submit your 2D engineering drawings (tolerances, head styles, drive recesses) or 3D models. Our senior cold heading application engineers will review mold feasibility, recommend corrosion-resistant platings, and provide an official quotation accompanied by DFM insights.
