Explore our cold-headed, roll-threaded SEMS and captive washer hardware built for defect-free automated robotic handling and vibration-proof structural resilience.




A comprehensive engineering analysis on the transition from traditional split-component fastening to high-speed pre-assembled washer architectures across automated manufacturing lines.
In high-throughput industrial manufacturing, assembly efficiency, joint integrity, and ergonomic takt time dictate competitive advantage. SEMS screws (derived from "pre-asSEMbled" washer fasteners) have revolutionized modern manufacturing by permanently capturing one, two, or three free-spinning washers onto the blank shank prior to the cold thread-rolling operation. As global discrete manufacturers face compounding labor shortages and aggressive cycle-time targets, the integration of pre-assembled washer units removes manual secondary handling, eliminates missing washer assembly failures, and establishes consistent clamp preload distributions across mass-produced assemblies.
Operating from our modern 20,000 m² manufacturing footprint across Dongguan, Shaoguan, and Wuhan, Yu-Huang Electronics Dongguan Co., Ltd. (YH Fastener) stands at the forefront of this fastening evolution. Backed by IATF 16949, ISO 9001, and ISO 14001 certifications, our engineering teams produce wholesale SEMS screws engineered for demanding duty cycles. Whether damping harmonics in electric vehicle (EV) battery power rails or establishing hermetic IP68 enclosures in 5G telecommunication arrays, our combination fasteners are optimized for automated robotic pick-and-place feeders and micro-dispensed robotic drivers.
By eliminating individual washer sorting, indexing, and manual placement, automated and manual assembly stations achieve upwards of a 42% decrease in assembly cycle duration, yielding direct operational expenditure savings.
Captured spring, conical, external tooth, or flat washers make it physically impossible for line workers or automated machinery to omit vital load-spreading or lock elements, ensuring 100% compliant bolted joint assemblies.
Specially engineered unthreaded washer seating gaps prevent washer shingling and jam-ups in vibratory bowl feeders, magnetic blow-feed screwdrivers, and six-axis articulated assembly robotics.
Understanding the critical manufacturing threshold: How thread displacement retains loose components without inducing stress concentrations or metallurgical embrittlement.
The manufacturing mechanics of a SEMS fastener represent a precision sequence of metallurgical forming. First, precision alloy or stainless wire rod undergoes high-speed cold heading to form the screw head, drive recess (Phillips, Torx, Hex Socket, or Tamper-Proof), and pre-thread shank blank. The diameter of this blank is engineered to an exact tolerance (referred to as the basic pitch diameter blank, $d_{k}$).
Next, loose, loose-tolerance washers (stamped, heat-treated, and deburred) are mechanically loaded onto the unthreaded screw shank. The assembly passes through high-precision flat or rotary thread-rolling dies. As the dies cold-form the helical thread ridges, material is displaced radially outward. Because the major thread diameter ($d$) becomes significantly larger than the inner hole diameter of the washer ($d_{w}$), the washer becomes permanently captive on the shank while remaining entirely free to spin freely between the under-head radius and the thread crest.
Continuous wire induction feeding into multi-station cold headers. High-speed progressive punch forming establishes structural head profiles and dense unbroken grain boundaries.
Automated optical dial tables slip single or compound washer sets (e.g., flat + spring washer combinations) onto the shank blank precisely beneath the under-head fillet.
Cold plastic deformation creates rolled threads. Diametric expansion permanently captures the washer, preventing escape while preserving axial rotational clearance.
Continuous mesh-belt neutral hardening and tempering (Class 8.8, 10.9, or 12.9) ensures uniform core tensile strength paired with mandatory post-plate baking for hydrogen de-embrittlement.
| Washer Combination Type | Kinematic Action & Function | Primary Industrial Sector | Engineering Standards |
|---|---|---|---|
| Screw + Single Plain Flat Washer | Distributes clamping surface stress over soft substrates (plastics, stamped aluminum). | Automotive Trim, Consumer Enclosures | DIN 6902, ISO 10644 Type A |
| Screw + Helical Split Spring Washer | Imparts constant dynamic axial spring rebound force against low thermal vibration. | General Machinery, Rail Subsystems | DIN 6905, ASME B18.13 |
| Screw + Double Washer (Flat + Spring) | Combines broad surface load redistribution with persistent cyclic vibration locking. | Automotive Powertrain, Industrial Drives | DIN 6907, JIS B1188 |
| Screw + External / Internal Tooth Washer | Teeth bite through non-conductive surface coatings to provide guaranteed grounding continuity. | EV Battery Management, Telecommunications | DIN 6908, ISO 10644 Type B |
| Screw + Conical Belleville Washer | Delivers massive axial pre-load retention across heavy cyclic thermal expansions. | Renewable Inverters, Switchgears | DIN 6796 Integration |
Targeted engineering solutions deployed worldwide to overcome harmonic loosening, galvanic corrosion, and environmental ingress.
In high-voltage EV battery pack enclosures, high-frequency road excitations cause conventional joint decay. YH Fastener supplies Class 10.9 Zinc-Nickel plated Torx SEMS screws with captured conical spring washers that maintain continuous tension on copper busbars and composite thermal barrier plates without relaxing over 300,000 km lifecycle testing.
Miniature M1.4 to M3 stainless steel SEMS screws configured with non-marring captive delrin or passivated 304 washers safeguard delicate multi-layer printed circuit boards. The spinning washer eliminates rotational head-galling against delicate solder masks and conductive PCB grounding pads during automated spindle driving.
Terminal grounding requires low contact resistance under severe temperature fluctuations. SEMS combinations featuring phosphor-bronze or brass toothed lock washers bite through anodized or powder-coated cabinets, providing uninterrupted earth conductivity and avoiding catastrophic thermal arc hazards.
How automation, lightweighting materials, and strict environmental mandates drive fastener engineering breakthroughs.
Modern production cells demand screw tolerances below 0.03 mm. YH Fastener uses 100% optical camera sorting stations to inspect thread pitch, under-head runout, and washer retention dynamics, delivering 0-defect feeding across high-speed driver heads.
Compliance with RoHS, REACH, and California Proposition 65 requires the complete elimination of hexavalent chromium. We apply trivalent zinc (clear, yellow, black) and electroplated zinc-nickel finishes delivering over 1,000 hours of neutral salt spray resistance (ASTM B117) without red rust.
As transportation pivots toward carbon fiber and engineered polyamides, standard metal fasteners induce micro-cracking. Our custom wide-flange SEMS screws distribute compressive clamping force broadly, preventing matrix delamination under full torque.
To eliminate post-assembly chemical threadlocker dispensing, YH Fastener equips SEMS units with 360° microencapsulated chemical patches (DIN 267-27) or pre-applied polyamide patches, locking the threads mechanically and chemically simultaneously.
A strategic overview of emerging manufacturing paradigms that will redefine mechanical joint integrity over the coming decade.
Developing ultra-miniature, stress-sensitive piezoelectric thin-film coatings directly onto the washer interface. These smart washers broadcast real-time residual clamping force data over near-field telemetry, informing automated smart-factory quality control platforms of loose bolts before mechanical breakdown occurs.
Deploying specialized vacuum continuous-conveyor de-embrittlement ovens coupled with alkaline non-electrolytic zinc flake coatings (such as Geomet and Magni). This eliminates acid-pickling atomic hydrogen penetration during finishing on high-tensile fasteners (Class 10.9 & 12.9).
Partnering with Tier-1 steel wire rod mills utilizing electric arc furnace (EAF) processing powered by renewable energy. Paired with closed-loop cold-heading oil recycling and computer-modeled progression dies, our manufacturing waste approaches zero scrap.
Custom metric & imperial screws manufactured to strict international standards (DIN, ISO, ASME, JIS) for global wholesale and OEM production requirements.


Expert guidance addressing the technical, metallurgical, and supply-chain queries of engineering procurement managers and quality auditors.
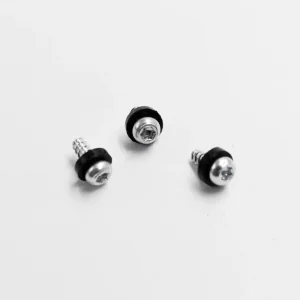
A SEMS screw features a washer that is slipped onto the unthreaded shank blank before thread rolling. During thread rolling, the cold displaced outer diameter of the thread expands beyond the inner diameter of the washer. This captures the washer permanently on the fastener shank without welding or crimping, permitting free axial rotation while eliminating washer omission risks during rapid assembly line cycles.
Washer binding or "shingling" inside vibratory feeding tracks happens when the inner chamfer of the washer locks into the thread runout or under-head fillet. YH Fastener engineers precision relief neck under-head grooves and exact unthreaded shank length dimensions, ensuring the washer spins smoothly without canting or jamming high-speed automatic blow-feeders.
Our comprehensive production system across our 20,000 m² facilities in Dongguan, Shaoguan, and Wuhan operates under strict compliance with ISO 9001 (Quality Management), ISO 14001 (Environmental Systems), and IATF 16949 (Automotive Quality Management). Every production lot is fully documented with complete material test reports (MTR) and dimensional inspection protocols.
Yes. Our in-house tooling division designs custom cold-heading dies and thread-rolling tooling from customer 2D prints (AutoCAD/PDF) or 3D CAD files (STEP/IGES). We accommodate bespoke head geometries, specialized drive recesses (Torx Plus, tamper-resistant pin-in-Torx), custom washer profiles (double-washer Belleville combinations), and micro-sizes down to M1.0.
High-tensile carbon and alloy steels are susceptible to atomic hydrogen absorption during electro-cleaning and acid pickling. YH Fastener mandates immediate post-plating thermal baking within 4 hours of electrodeposition at 200°C–230°C for a minimum of 8 to 24 hours. Alternatively, we utilize zinc-flake dip-spin coatings that entirely bypass acidic processing.
Rapid prototyping and custom die tooling are completed within 7 to 10 working days, followed by PPAP Level 3 documentation and first article sample submission. Following sample approval, mass production batches run across multi-station cold headers with lead times typically ranging from 15 to 25 calendar days, supported by global export shipping logistics to over 60 countries.
