Direct factory batch engineering with high yield rates and custom thread geometry.
Modern mechanical design demands flush surfaces, high clamp force, and elimination of pre-tapped tapping steps across metal and composite assemblies.
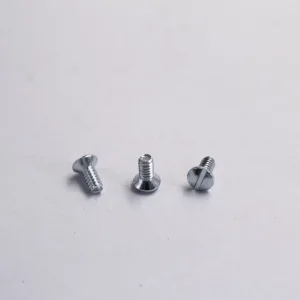
Countersunk self-tapping screws (Flat Head, DIN 7982, ISO 7049, ANSI B18.6.4) feature precision 90° or 82° conical heads designed to seat entirely flush with the mating surface. In high-speed automated manufacturing, eliminating surface protrusions reduces aerodynamic drag, prevents mechanical interference with moving components, and ensures aesthetic uniformity across exterior consumer electronics and automotive fascias.
Global tier-1 OEMs classify countersunk self-tapping fasteners into Thread Forming (Type AB, Type B, PT geometry) and Thread Cutting (Type F, Type 1, Type 23). Thread-forming designs displace metal or thermoplastic without creating chips, preserving material grain structure for superior pull-out resistance, while thread-cutting screws feature integrated flute geometries that clear chips in ductile cast metals and thick-gauge structural sheet metal.
Procurement engineers are transitioning from standard carbon steel with generic zinc plating toward case-hardened alloy steels (SAE 1022, 10B21) and cold-worked austenitic stainless steels (SUS304, SUS316). Strict environmental regulations (RoHS, REACH) require advanced trivalent passivations, zinc-nickel coatings with sealing topcoats, and micro-encapsulated thread-locking patches to resist cyclical vibration without thread galling.
Comparative analysis of standard configurations across major international norms for high-volume manufacturing lines.
| Standard / Type | Head Angle | Common Materials | Drive Recesses | Yield Tensile (MPa) | Primary Industrial Use |
|---|---|---|---|---|---|
| DIN 7982 / ISO 7049 | 90° Conical | Case Hardened 1022, SUS304 | Phillips (PH), Pozi (PZ), Torx (TX) | 450 – 750 MPa | Sheet metal enclosures, HVAC, white appliances |
| ANSI B18.6.4 (Type AB) | 82° Countersunk | Carbon Steel, Austenitic SS | Phillips, Slotted, Square (Robertson) | 600 – 900 MPa | North American chassis, electrical junction boxes |
| PT Thread Flush Head | 30° Flank / 90° Head | Alloy Steel 10B21, SCM435 | Torx Plus, Six-Lobe Tamper-Proof | 800 – 1050 MPa | Automotive thermoplastic trims, battery pack casings |
| Type F Cutting Countersunk | 90° Head w/ Flute | Carburized Low Carbon Steel | Hex Socket, Torx, Combined Slot | 700 – 950 MPa | Die-cast aluminum, zinc housings, heavy metal gauge |
Wire rod spheroidizing annealing eliminates internal stresses, optimizing cold-forging heading without head shearing.
High-speed automatic headers form the countersink angle and internal drive socket under closed-loop dimensional laser monitoring.
Continuous mesh-belt furnace carburizing ensures a hardened exterior case (min. 450 HV) alongside a tough, ductile core (240–390 HV).
Solving high-stress clamping, electrical grounding, and thermal shock issues across modern verticals.
Used extensively in instrument panel mountings, battery thermal management housings, and aluminum structural frames. Countersunk self-tapping screws eliminate the cost of welding weld-nuts or installing brass inserts. Utilizing zinc-nickel (Zn-Ni) coatings, they survive 1,500 hours of Neutral Salt Spray testing and cycle reliably through temperature extremes ranging from -40°C to 125°C.
Miniaturized M1.2 to M2.5 countersunk self-tapping fasteners provide clean, zero-interference closure for smartphone unibodies, laptop chassis, and IoT sensor arrays. Rolled with ultra-narrow lead tolerances, they achieve clean drive performance in polycarbonates (PC) and ABS resins without cracking bosses, preventing costly cosmetic rejection.
In server cabinets and 5G base station outdoor housings, flush countersunk profiles allow sliding rack equipment to glide freely without snagging screw heads. Precision-serrated underside head variants provide high-reliability ground continuity across anodized aluminum panels, actively mitigating electromagnetic interference (EMI).
High-frequency vibratory environments necessitate micro-encapsulated polyamide pre-coatings or Torx Plus drives that transfer high insertion torque without camming out or stripping the internal recess. This ensures long service maintenance intervals in automated conveyor systems and robotic end-effectors.
How Yu-Huang Electronics (YH Fastener) minimizes Total Cost of Ownership (TCO) for global supply chains.
For high-speed automated feed systems, a single deformed screw head can trigger costly assembly downtime. YH Fastener deploys glass-disk optical sorting systems utilizing multi-angle high-resolution CCD cameras, verifying pitch diameter, thread lead, head concentricity, and recess depth at speeds up to 1,200 ppm with defect rates under 15 PPM.
High-tensile case-hardened carbon steel fasteners subjected to electroplating processes face catastrophic delayed fracture from atomic hydrogen diffusion. Our IATF 16949-regulated heat-treatment protocols mandate immediate baking at 200°C–230°C for 4 to 8 hours within 1 hour post-acid-pickling and plating, verified by sustained stress test validation.
We provide complete material test reports (MTR), raw wire chemical assays, micro-Vickers hardness gradient maps, and Production Part Approval Process (PPAP) Level 3 documentation. Every batch carries an internal lot code linking back to raw heat batch, die tooling logs, and operator shift records.
Direct technical resolutions addressing design, torque specification, and coating performance.
Full-spectrum fastening portfolio for global electronic, automotive, and automation manufacturers.