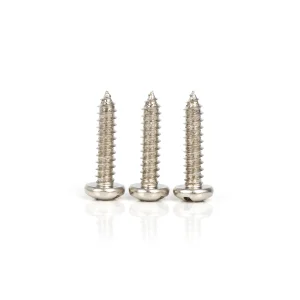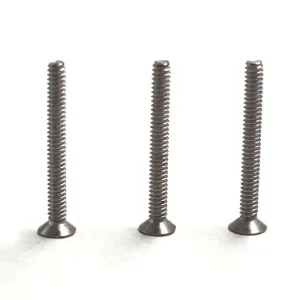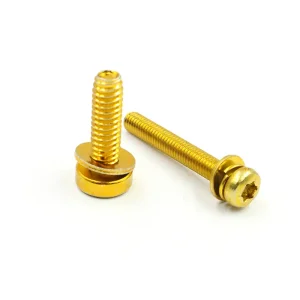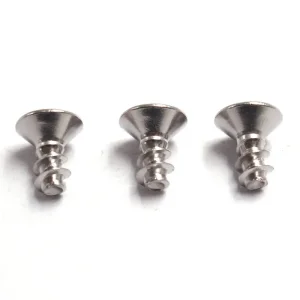
Standard, metric, and tailor-engineered captive, tapping, and machine fastening hardware directly exported from our Dongguan, Shaoguan, and Wuhan smart production centers.
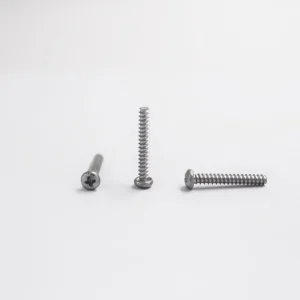
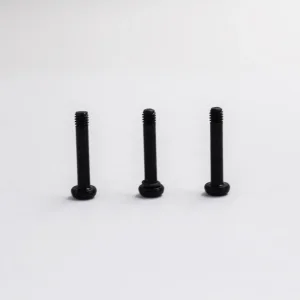
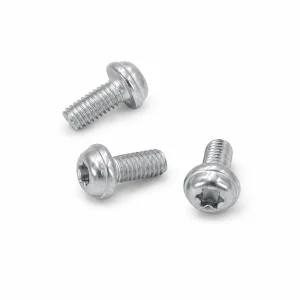
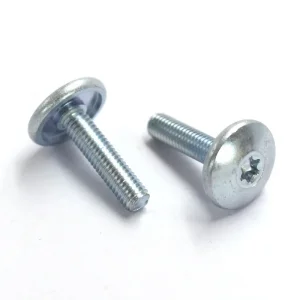

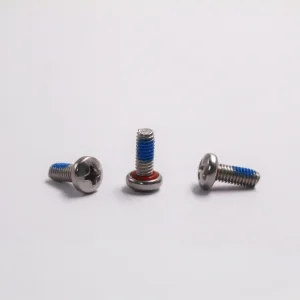

Countersunk captive screws solve dual challenges in high-density assembly: preventing fastener loss (FOD mitigation) while delivering a perfectly flush aerodynamic or mechanical profile.
Standard flat countersunk heads (82°, 90°, or 100°) seat directly flush with outer sheet metal panels. In high-speed airflow or sliding drawer rack enclosures, this eliminates turbulence, mechanical snagging, and operator glove interference.
By cold-heading or turning an unthreaded shank segment with an outer diameter narrower than the thread minor diameter, our screws remain captured in an outer retained hole via retainer washers, snap rings, or swaged grommets without coming loose during field servicing.
Manufactured using cold-worked 304 and 316 austenitic stainless steels or vacuum heat-treated alloy steels, our roll-threaded surfaces exhibit surface finishes below Ra 0.4 μm, minimizing galling even after repetitive high-cycle pneumatic disassembly.
Examine standard production metrics designed for rapid customization and OEM qualification protocols.
| Nominal Thread Size | Typical Shank Under-Cut Ø | Head Angle Standard | Material Options | Surface Treatment | Vibration Resistance |
|---|---|---|---|---|---|
| M2.0 – M2.5 | 1.45 – 1.80 mm | 90° / 100° Low Profile | SUS304 / Brass C3604 | Passivated / Gold-Plated | Class 4.8 / Micro-patch |
| M3.0 – M3.5 | 2.10 – 2.50 mm | 90° DIN 965 / 82° ANSI | SUS304, 316 / 1018 Steel | Bright Zinc / Black Trivalent | Nylon Strip (DIN 267-28) |
| M4.0 – M5.0 | 2.90 – 3.80 mm | 90° / 82° Countersunk | 316Ti / SCM435 Alloy | Electroless Nickel / Geomet | Prevailing Torque Patch |
| M6.0 – M8.0 | 4.50 – 6.10 mm | DIN 7991 Standard Head | Grade 8.8 / 10.9 Alloy Steel | Zinc-Nickel Alloy / Dacromet | Under-Head Serration / Sems |
How engineering sectors across Europe, North America, and the Asia-Pacific optimize maintenance safety using countersunk captive hardware.
In data center server blades (North American Open Compute Project), sliding clearances are tight down to millimeters. Countersunk captive screws prevent module snagging during hot-swap routines while ensuring no detached hardware drops into energised backplanes.
Under IATF 16949 standards across European and Asian EV OEMs, flat-mount captive fasteners are integrated into lightweight composite cover plates, avoiding contact with low-clearance vehicle chassis while preventing runaway loose screws in battery modules.
Precision machine safety guards demand zero downtime during routine blade, laser lens, or calibration maintenance. Captive screws enable technicians to unscrew lids rapidly without dropping fasteners into oily, rotating tool pathways.
Integrated upstream wire drawing, in-house tooling creation, and multi-facility footprint insulate tier-one procurement programs from global volatility.
By operating our mother facility in Dongguan alongside regional production sites in Shaoguan and Wuhan, YH Fastener controls wire preparation, high-speed multi-die cold heading, optical sorting, and automated packing completely in-house. This three-node structure protects buyers from regional logistics interruptions while offering continuous 24/7 capacity.
Access to direct raw material partnerships (Yongxing Stainless, Baosteel) reduces raw wire input costs. Combined with proprietary progressive cold-forming tooling that eliminates material loss compared to pure CNC turning, our high-volume output reduces per-piece costs by up to 35% without sacrificing tight DIN/ISO tolerances.
From automated robotic line picking to environmentally sustainable passive passivation films, see where captive hardware engineering is heading.
Optimizing head recess geometry (Torx Plus® & HexStik) to facilitate high-speed cobot feeder alignment and avoid cross-threading in lights-out assembly lines.
Full migration to high-performance zinc-aluminum flakes and chrome-free thin-film finishes with zero wastewater emission and 1,500+ hour salt-spray durability.
Expanding captive screw cold-forming into Grade 5 Titanium (Ti-6Al-4V) for next-generation satellite solar arrays and commercial aerospace drones.
Laser micro-engraving 2D DataMatrix batch identification codes directly on the captive head to fulfill digital twin product lifecycle demands.
Every overseas shipment is backed by verified metallurgical documentation, RoHS/REACH compliance certifications, and localized sales engineers.
For automotive tier suppliers, we furnish complete Production Part Approval Process (PPAP) documentation packages including Control Plans, FMEA, Gage R&R, and IMDS material submissions.
We eliminate customs friction through established DDP (Delivered Duty Paid) shipping to European and American hubs, accompanied by flexible buffer-stock inventory management for fast pull-down replenishment.
Our sales engineering team directly reviews CAD drawings (.STEP, .DWG, .IGES) and returns detailed DFM (Design for Manufacturability) suggestions within 24 hours to streamline initial prototyping.
Everything technical procurement teams need to know regarding tolerances, retention washers, tooling, and minimum quantities.
Metric countersunk captive screws generally conform to the DIN/ISO standard of 90 degrees (such as DIN 965 or DIN 7991 geometries). In contrast, imperial fasteners manufactured to ANSI/ASME standards feature an 82-degree angle (or occasionally 100 degrees for aerospace and ultra-thin electronics sheet metal). YH Fastener produces custom heading dies for 82°, 90°, and 100° heads according to OEM blueprints.
Retention is achieved through a reduced unthreaded shank underneath the threaded tip. After passing the screw through a countersunk clearance hole in the outer panel, a retaining washer (e.g., nylon retaining ring, stainless split ring, or press-fit grommet) is slipped onto the undercut section from the reverse side. The threaded lead prevents the washer from backing off, securing the fastener permanently to the panel during servicing.
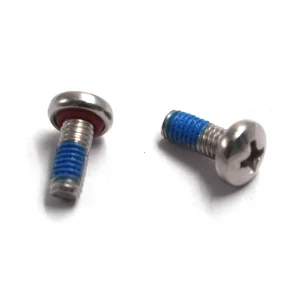
Yes. We frequently apply blue or red polyamide nylon patches (DIN 267-28 standard) directly onto the lead thread. This adds prevailing torque to lock into internal threads, protecting high-vibration applications in automotive electronics, military handhelds, and engine management enclosures.
For custom cold-headed parts, our standard prototyping MOQ starts from 10,000 to 50,000 pieces depending on wire size and head complexity. Tooling and prototype samples take roughly 7 to 12 days. Full mass-production runs are usually finished within 20 to 25 business days, with urgent air-shipment batches accommodated for fast-track product builds.
Discover matching custom screw architectures, plungers, and specialty self-tapping solutions from our complete manufacturing lineup.