

Direct manufacturer supply for automated robotic assembly cells, mission-critical electrical enclosures, and chassis hardware.


A technical assessment of joint reliability, prevailing torque metrics, and robotic automation assembly efficiency.
In high-throughput original equipment manufacturing (OEM), the fastening node represents not merely a static joint, but a critical failure point under continuous dynamic shear, vibrational harmonic oscillation, and thermal expansion cycles. SEMS screws—derived from the German phrase "schrauben-und-scheiben-vormontiert" (pre-assembled screw and washer)—solve an intrinsic vulnerability in industrial assembly: human error and robotic feeder jams caused by manual or separate washer placement. When combined with an indented hexagon or hex washer head geometry, Custom Hex SEMS Screws deliver maximum mechanical advantages across clamping force distribution, torque-to-tension linear consistency, and high-speed automated drive tooling retention.
From an empirical mechanical engineering standpoint, the cold-heading formation process of a custom hex SEMS fastener requires severe metallurgical controls. The washer element—whether a helical spring lock washer (ASME B18.21.1 / DIN 127), internal/external conical tooth washer (DIN 6798), or square-cone Belleville tensioning disc—must be positioned onto the screw blank prior to thread rolling. As the threading dies form the major and pitch diameters through plastic deformation rather than chip cutting, the thread outer diameter (OD) expands beyond the inner diameter (ID) of the washer, permanently capturing it beneath the hex bearing surface with completely free rotational movement. This free rotation is crucial: during final torque rundown, the captured washer acts as a thrust bearing, preventing galling or marring of sensitive mating surfaces (such as painted enclosures, magnesium structural frames, or PCB ground rings) while ensuring that applied driver torque directly converts into clamp tension rather than frictional head dissipation.
Custom hex SEMS screws equipped with integrated conical spring (Belleville) washers absorb the micro-vibrations and thermal expansion mismatches between die-cast aluminum housings and battery terminal copper busbars, safeguarding uncompromised electrical conductivity and preventing thermal runaway.
With captive double washers (flat and helical split lock) held rigidly perpendicular to the axis, our hex SEMS screws eliminate loose part skewing inside pneumatic blow-feed tubes and magnetic screw-driving spindles, lowering MTBF in high-volume electronic device manufacturing.
Utilizing high-tensile 304/316 austenitic stainless steel and custom zinc-nickel electroplating (providing over 1,200 hours of ASTM B117 salt spray protection), hex SEMS fasteners withstand rigorous marine and tropical weathering while securing outdoor microwave transceiver chassis grounding paths.
Synthesizing next-generation metallurgy, digitalization in cold heading, and cross-border supply chain resilience.
While Western OEMs in North America and Western Europe increasingly seek supply redundancy through nearshoring or regional diversification, the high-precision cold-heading sector remains inextricably anchored to China's dense industrial ecosystem. The production of complex custom hex SEMS screws demands not merely isolated cold-heading machines, but a hyper-integrated cluster comprising specialized steel draw-bench plants, bespoke tooling die makers, heat treatment salt-bath operators, eco-certified electroplaters, and optical sorting automation integrators. YH Fastener (Yu-Huang Electronics Dongguan Co., Ltd.), operating out of a 20,000 m² advanced manufacturing footprint spanning Dongguan, Shaoguan, and Wuhan, harnesses this supply chain concentration to deliver custom prototypes within 5-7 days and production scalability exceeding 25 million fasteners monthly.
Comprehensive design limitations, washer combinations, and metallurgical classifications.
| Dimensional / Mechanical Parameter | Standard Specification Range | Custom OEM Capability | Primary Industrial Utility |
|---|---|---|---|
| Nominal Thread Diameter | M2.0 to M12 (#2-56 to 1/2"-13) | Micro-diameters down to M1.4, custom pitches | Consumer Electronics, Industrial Enclosures |
| Head Geometries | Hex Flange, Indented Hex, Hex Washer | Combination Hex + Phillips / Slot / Torx recess | Dual-drive assembly, high-torque robotic tools |
| Captive Washer Variations | DIN 127, DIN 6798, DIN 6902, Flat DIN 125 | Double washer (Split + Flat), Conical Disc, Wave | Electrical ground-piercing, constant spring preload |
| Raw Materials | Carbon Steel (1018, 1022), Alloy (10B21, 40Cr) | Stainless 304, 316, 316L, 410, Brass, Phosphor Bronze | Marine corrosion resistance, high-tensile Grade 8.8/10.9 |
| Surface Finishes & Coatings | Bright Zinc, Black Zinc, Yellow Zinc, Nickel | Zinc-Nickel (15% Ni), Geomet, Magni, Electrophoresis Black | Automotive chassis, EV battery, outdoor PV installations |
| Thread Profiles | ISO Metric (Coarse/Fine), Unified UNC/UNF | Trilobular (PT / Taptite Thread-Forming), Type F | Direct insertion into cast aluminum or thermoplastics |
Navigating strict regulatory hurdles with complete PPAP documentation and international technical assistance.
Full support for the automotive supply chain with Part Submission Warrants (PSW), Failure Mode and Effects Analysis (FMEA), Process Flow Diagrams, Control Plans, and international material data system (IMDS) submissions for Tier-1 assembly acceptance.
Strict operational enforcement of environmental safety mandates. All raw materials, passivates, and lubricants undergo regular third-party SGS laboratory testing, ensuring non-detectable levels of heavy metals, polybrominated biphenyls, and PFAS chemistry.
To insulate international purchasers against ocean freight volatility and port congestion, we offer Vendor Managed Inventory (VMI) arrangements, blanket order scheduling, and strategic warehouse buffer stocks across European and North American logistics hubs.
Engineered cold-headed fasteners manufactured under IATF 16949 standards for critical mechanical assemblies.
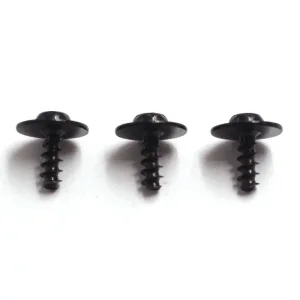



Expert insights regarding clamping torque, washer tooth retention, and cold-heading tooling economics.
An indented hex head features an inner depression formed during heading to save mass, but has an unshielded hex perimeter. A hex washer head incorporates an integral circular flange formed beneath the hex flats, offering a broader bearing surface area. When adding a free-spinning captured SEMS washer, an indented hex head allows the independent washer to manage total surface contact and spring tension without increasing head height, whereas a hex flange can be combined with internal tooth washers for dual-stage electrical ground bitings.
The washer is slipped onto the cold-headed unthreaded screw blank, which possesses a shank diameter roughly equal to the pitch diameter. The screw then passes through high-speed flat or cylindrical thread rolling dies. As the dies displace the cold steel to raise the outer thread ridges, the crest diameter becomes significantly larger than the inner hole diameter of the washer, permanently locking the washer between the screw head and the threaded portion while preserving complete axial rotational freedom.
Yes. Double-washer SEMS screws (often conforming to JIS B1188 or custom OEM drawings) are standard production components in our facilities. In this configuration, a flat washer is assembled closest to the workpiece to protect fragile surfaces from gouging, while a split helical or wavy spring washer is positioned directly beneath the hex head to exert continuous axial tension and prevent vibrational backing off.
High-strength carbon and alloy steels (hardness > 320 HV) are sensitive to atomic hydrogen absorption during acid pickling and electro-galvanizing. Our standardized quality protocol requires that all heat-treated SEMS fasteners undergo immediate de-embrittlement baking at 200°C–220°C for a minimum of 4 to 8 hours within 4 hours of plating completion, followed by rigorous stress-durability testing under 75% ultimate tensile load for 48 hours without fracture.
For fully bespoke hex SEMS geometries requiring new heading punch sets and thread rolling dies, initial tooling fabrication and prototype sampling (with 3D dimension inspection reports) require 5 to 7 working days. Commercial production lead times range between 2 to 3 weeks. Production MOQs typically start at 50,000 pieces depending on thread diameter (e.g., micro M2 vs heavy industrial M8), with blanket delivery schedules supported.
Robotic automated assembly lines cannot tolerate missing washers, bent shanks, or flash burrs. YH Fastener runs 100% optical sorting inspection utilizing multi-sensor high-resolution CCD cameras on transparent glass rotating platters. This process verifies washer presence, washer free-spin clearance, thread pitch accuracy, head height, and drive recess integrity at inspection speeds exceeding 800 parts per minute, ensuring a field defect rate under 15 PPM.