Direct from our Dongguan, Shaoguan, and Wuhan facilities—engineered to meet strict DIN, ISO, ANSI, and customer-specific blueprint tolerances.



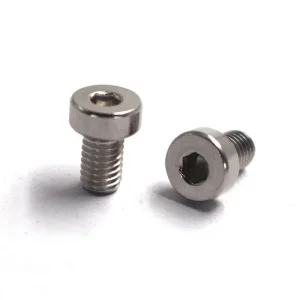
How the demands of electrification, high-vibration robotics, and microminiaturization are transforming headless threaded fastener engineering.
Traditional set screws relied strictly on point penetration (cup, cone, or knurled cup points) against a drive shaft. Modern ODM applications require 360-degree engineered nylon patches, micro-encapsulated anaerobic adhesives (DIN 267-27 compliant), or brass/nylon tipping to achieve repeatable prevailing torque without galling precision shaft ground surfaces.
With electronic devices, optical modules, and surgical gear downscaling rapidly, the market requires M0.8 to M2.0 set screws capable of sustaining precise torque limits without socket stripping. Multi-stage cold-heading tooling paired with high-concentricity hex and Torx-Plus® drive recesses ensures maximum driving tool engagement.
From aerospace thermal cyclings to subsea saltwater operations, standard 304/316 grades are increasingly supplemented by specialized alloys. Titanium Gr. 5, Inconel 718, and precipitation-hardened steels (17-4PH) ensure exceptional shear capacity and zero magnetic interference in cleanroom or sensor-dense enclosures.
Addressing the core risks identified by VP-level procurement and supplier quality managers (SQEs) during volume onboarding.
Procurement teams demand predictable clamp loads across high-speed automatic feeder bowls. Variations in thread lead-in chamfers or microscopic plating thickness (e.g., uneven zinc flake deposition) result in costly line stoppages. Our factory integrates automated optical sorting machines (sorting speed > 800 pcs/min) to filter out dimensional deviances > 0.01mm.
For high-tensile set screws (Grade 10.9, 12.9, 45H), improper acid pickling or delayed post-electroplating de-embrittlement baking triggers spontaneous catastrophic cracking under load. YH Fastener strictly executes standardized 200°C–220°C baking processes up to 8-24 hours depending on fastener hardness class.
Global Tier-1 manufacturers require documented production validation before bulk shipment. We provide full Production Part Approval Process (PPAP) documentation packages including Control Plans, Process FMEA, Gage R&R, Material Test Reports (EN 10204 3.1), and IMDS registrations.
Engineered locking solutions designed for complex mechanical joints under extreme thermal and mechanical stresses.
Joint assemblies subject to constant acceleration and rapid reversal suffer from vibration loosening. We engineer micro-diameter locking set screws with flat/dog points paired with Polyamide 11 patches. This configuration protects motor splines and maintains zero axial backlash throughout millions of continuous operational cycles.
Under-hood vibration, engine thermal spikes (-40°C to +150°C), and road de-icing salts present harsh operational environments. We produce alloy steel 45H set screws coated with thin-film zinc-nickel alloy (12-16% Ni content), guaranteeing 1500+ hours to red rust without thread pitch diameter swell that causes cross-threading.
Sub-micron optical alignment calls for zero-backlash positioning. We manufacture ultra-fine pitch set screws (0.25mm to 0.35mm pitch) featuring mirror-polished carbide or brass contact pads, eliminating galling against titanium optical mirror housings while preventing alignment drift.
Minimizing supply chain fragility through multi-plant production redundancy and comprehensive global certifications.
With our headquarters and main production plant located in Dongguan and specialized branch factories operating in Shaoguan and Wuhan, YH Fastener delivers cross-facility load balancing. If regional disruptions occur, cold heading and thread rolling capacity shifts seamlessly across our 20,000 m² combined plant footprint.
All incoming wire materials and surface treatments undergo strict screening for hazardous substances under EU RoHS 2011/65/EU and REACH (SVHC list). We provide full chemical assay certificates confirming lead-free brass formulations (< 0.1% Pb content) and transparent supply chains for global environmental audits.
Our sales engineering units operate in parallel with North American and European design cycles. By sharing 3D STEP files or CAD blueprints, clients receive complete Design for Manufacturability (DFM) feedback, tooling cost estimations, and optimized coating recommendations within 24 hours.
Investing in intelligent inline sensing, cold-forming micro-tooling, and sustainable carbon-neutral metallurgy.
Implementation of real-time acoustic emission sensors across multi-die cold-heading presses enables detection of internal crystal shear defects and micro-cracks during high-speed wire forming, preventing defective parts from progressing downstream to thread-rolling stages.
Development of proprietary bio-based prevailing torque coatings rated for up to 10 reinstall cycles without loss of initial locking efficiency. These eliminate volatile organic compounds (VOCs) during industrial oven curing while delivering reliable DIN 267-15 compliance.
Redesigning the socket chamfers and point radius transitions to accommodate centrifugal bowl and pneumatic blow-feed insertion systems operating at cycle times under 0.8 seconds per fastener, preventing socket misalignments in smart lights-out production lines.
Explore additional high-demand components engineered in-house with full metallurgical test reports.


In-depth technical answers addressing point selection, prevailing torque standards, and custom manufacturing parameters.
We manufacture six primary point styles: Cup Point (standard high-grip holding force for semi-permanent shaft mounting), Flat Point (prevents damage to precision ground shafts where frequent repositioning is required), Cone Point (provides permanent locking by penetrating into a pre-machined countersunk hole), Dog/Half-Dog Point (engages with internal shaft keyways or slots to transmit rotary motion while allowing axial float), Knurled Cup Point (exceptional rotational slip resistance under severe cyclical vibration), and Soft-Tipped (Nylon or Brass) (absorbs micro-chatter and guarantees zero cosmetic or dimensional deformation of sensitive mated components).
A nylon patch (prevailing torque type under IFI-124 / DIN 267-28) provides purely mechanical friction against the internal female threads. It is reusable up to 5 times, resists hydraulic oils and engine fuels, operates reliably across -50°C to +120°C, and requires zero cure time during automated assembly. Conversely, micro-encapsulated adhesive (reactive chemical locking under DIN 267-27) shears open during thread engagement, polymerizing into an airtight thermoset seal. It offers significantly higher breakaway torque but is strictly single-use and requires 24 hours for full cure.
Yes. Utilizing specialized multi-station precision cold headers and high-accuracy Swiss CNC lathes, we mass-produce miniature locking set screws down to M0.8. Drive systems include deep-engagement Hexagon Sockets, Torx (6-Lobe), and Torx-Plus® recesses. These high-torque geometries dramatically diminish cam-out forces and drive-strip risks when torqued by automatic precision electric screwdrivers.
For high-hardness alloy steels (≥ Class 45H / 10.9 / 12.9), we recommend Zinc-Nickel Electroplating (Zn-Ni 12-16%) paired with controlled de-embrittlement baking (minimum 8 hours at 200°C–220°C within 4 hours of plating), or non-electrolytic Zinc Flake coatings (Geomet®, Magni, Dacromet). Zinc flake eliminates acid pickling and electro-deposition currents altogether, offering zero hydrogen embrittlement risk while exceeding 1000 hours of neutral salt spray exposure per ASTM B117.
Standard engineering drawings receive comprehensive DFM feedback and formal quotation within 24 hours. Rapid custom prototyping with dedicated tooling typically requires 10 to 15 business days including First Article Inspection Reports (FAIR). Bulk production turnaround ranges from 3 to 4 weeks depending on thread patch requirements and post-forming heat treatment cycles. Stock programs (VMI / JIT consignment) are supported via our global freight forwarders.
