Engineered for automated insertion lines, anti-crossthreading integrity, and permanent grounding contact. Select from our production-verified ODM machine screws, SEMS hardware, and countersunk fasteners.


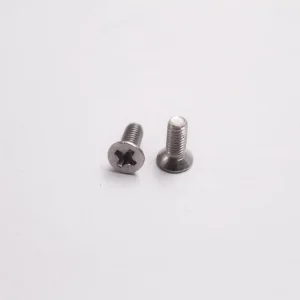
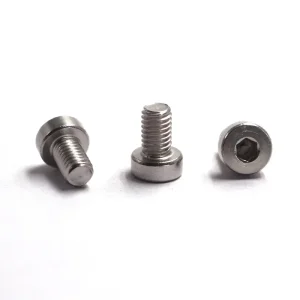
In modern automated manufacturing, cabinet assembly screws have transitioned from passive hardware into mission-critical structural components governing electromagnetic compatibility (EMC), thermal cycling stability, and automated throughput.
With the exponential boom in AI compute clusters, 19-inch and 21-inch Open Compute Project (OCP) server racks require zero-play assembly hardware. Fasteners must withstand constant acoustic vibrations generated by 12,000+ RPM cooling fans while maintaining micro-ohm electrical grounding resistance to eliminate stray static discharges across server motherboards.
Medium- and low-voltage distribution cabinets (IEC 61439 compliant) operate under harsh electrodynamic stresses during short-circuit surges. Standard fasteners experience catastrophic thread stripping or preload relaxation. Advanced SEMS screws featuring hardened helical conical spring washers maintain clamping forces exceeding 85% of initial yield across 20-year operational horizons.
The adoption of collaborative robots (cobots) in modular casework and electronics manufacturing has rendered conventional Phillips machine screws obsolete on automated lines. Fastening designs must feature deep Torx or Torx Plus geometries, precision dog-point lead chamfers, and balanced shank runout to prevent cam-out, bit slippage, and crossthreading at drive speeds over 1,200 RPM.
Operating across our primary 20,000 m² modern manufacturing hub in Dongguan alongside strategic production branches in Shaoguan and Wuhan, YH Fasteners eliminates Tier-2 subcontractor margins. We control the complete metallurgy lifecycle: raw alloy wire drawing, multi-station cold heading, high-speed thread rolling, computerized continuous atmosphere heat treatment, electroplating, and micro-encapsulated adhesive patching.
Decades of die-design specialization translating CAD models into high-volume tooling within 5 to 7 days.
IATF 16949 compliant zero-defect policy tailored for high-speed robotic screwdriving lines.
Different industrial cabinet enclosures demand distinct physical and chemical attributes. We engineer fasteners tailored specifically to base-metal hardness, thermal expansion, vibration spectra, and ingress protection ratings.
| Application Scenario | Recommended Fastener Configuration | Core Material Grade | Surface Treatment | Key Engineering Benefit |
|---|---|---|---|---|
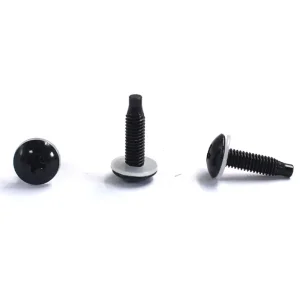
| 19-Inch Data Center Server Racks | M5/M6 Pan Head SEMS with Pilot Dog Point & Serrated Washer | AISI 1022A Case Hardened / SS304 | Black Zinc Plated / Passivated | Eliminates crossthreading; punctures anodized coatings to create direct Faraday chassis grounding. |
| Outdoor NEMA 4X / IP67 Enclosures | Hex Socket / Torx Pan Head with Molded Silicone O-Ring | Stainless Steel 316 / A4-70 | Electropolished / Passivated | Gas-tight and liquid-tight seal up to 10 bar pressure; immune to coastal salt-fog corrosion. |
| High-Voltage Switchgear & Busbars | Hex Head High-Torque Screw with Conical Belleville Washer | Alloy Steel Class 8.8 / 10.9 | Trivalent Zinc Yellow Cr3+ | Compensates for thermal expansion gaps caused by electrical peak resistance heating cycles. |
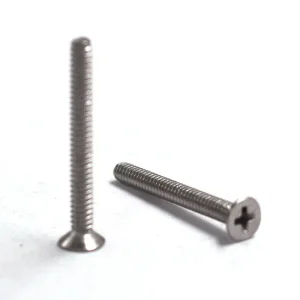
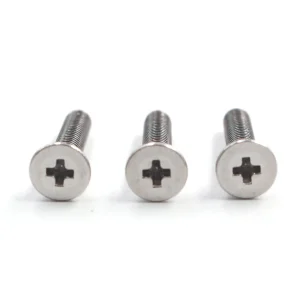
| Architectural & Modular Metal Casework | Countersunk Flat Head 82° / 90° with Torx Drive | Carbon Steel C1018 / SS302 | Zinc Nickel Black / Dacromet | Zero-protrusion flush profile ensuring zero interference with dynamic drawer slides and cabinet hinge rails. |
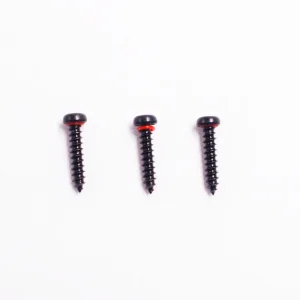
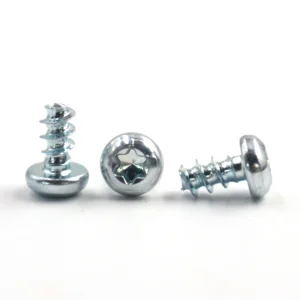
| Thermoplastic Junction & Control Boxes | PT Thread-Forming Screws with 30° Profile Flank Angle | Austenitic 304 / Case Carbon Steel | Bright Nickel / Trivalent Blue Zinc | Minimizes radial bursting stress in ABS, Polycarbonate, and Nylon boss structures while maximizing strip-out torque. |
Specially compounded wax and dry-film lubricants applied to austenitic stainless steel fasteners to prevent localized friction cold welding during pneumatic nutrunner driving.
360° or 180° polyamide (nylon) patches permanently fused to the external threads provide repeatable prevailing torque per DIN 267-28 for up to 5 re-use cycles.
Reduced unthreaded shanks that mechanically latch into sheet metal panel knockouts, ensuring service technicians never drop loose screws into energized cabinets.
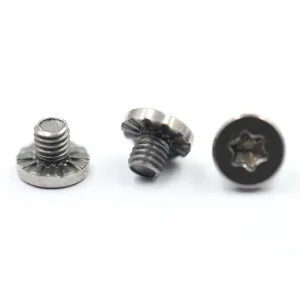
Internal/external tooth captive lock washers aggressively bite through non-conductive polyester powder coatings to achieve mandatory zero-resistance grounding.
As commercial smart cabinetry integrates IoT sensors, Edge AI servers, and modular sustainability mandates, industrial fasteners are evolving to meet extreme mechanical benchmarks.
With stringent global compliance standards like EU RoHS, REACH, and California Prop 65 banning heavy metals and volatile organic compounds (VOCs), our foundry has pioneered micro-layer zinc flake and silane sol-gel coatings. These surface treatments deliver extraordinary corrosion barrier performance (1,500+ hours neutral salt spray resistance) without hydrogen embrittlement hazards commonly found in electroplated high-tensile steels.
Traditional cabinet assembly required tapping holes in extruded aluminum or punched sheet steel—a process that introduces conductive metal debris hazardous to PCB assemblies. Our specialized trilobular thread-rolling screws (Taptite style) plastically flow mating sheet metal threads without cutting, delivering superior torsional break-loose resistance and eliminating secondary chip clearance operations.
Telecom utility cabinets deployed in open urban environments face persistent tampering and copper theft risks. We manufacture precision security screws equipped with pin-in-Torx, triangular socket, and one-way unidirectional drive heads. Matched high-durability installation keys ensure rapid authorized service while stopping vandalism in field-installed municipal infrastructure.
When global Tier-1 OEMs audit YH Fasteners for multi-million piece annual assembly contracts, their engineering and sourcing teams evaluate our facilities against four rigorous verification pillars.
Direct partnerships with certified domestic steel mills (such as Baosteel and Xingtai). Every master coil arrives with heat lot numbers, spectroscopic chemical composition certificates, and metallographic grain-size verification.
We calculate real-time Cpk/Ppk metrics across heading and thread-rolling stations. Critical dimensions—including major diameter, pitch diameter, thread lead, and under-head fillet radius—consistently maintain Cpk > 1.67.
Our in-house metrology lab utilizes computerized Schatz torque-tension test benches to generate accurate clamp force curves, nut-factor friction coefficients (μ), and ultimate yield points under dynamic assembly speeds.
For all high-tensile (Class 8.8, 10.9, 12.9) carbon steel fasteners subjected to acid pickling and electroplating, baking ovens execute mandatory 4 to 8 hour de-embrittlement cycles at 200°C–220°C strictly within 4 hours of plating.
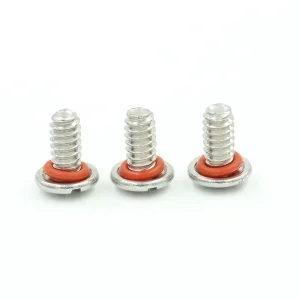
Engineered for extreme operating environments requiring hermetic O-ring isolation, plastic boss thread-forming, and specialized visual surface coatings.
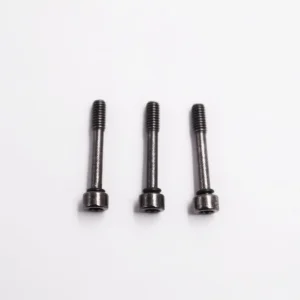
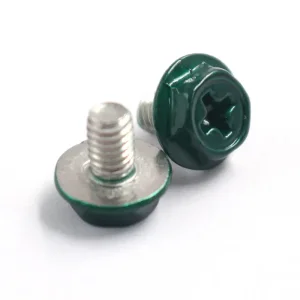

Detailed answers covering thread geometry, galvanic isolation, automated insertion torque specifications, and factory ODM customization parameters.
On high-speed automated assembly lines, magnetic or vacuum screwdriving spindles feed fasteners into tapped sheet-metal rack posts at angles that may deviate 2° to 5° from normal alignment. Standard sharp-lead machine screws will cross-thread immediately, destroying the extruded nut threads and triggering line shutdowns.
Our ODM cabinet assembly screws feature engineered unthreaded pilot points (dog points or conical leads) per DIN 78 / ISO 4753. The smooth cylindrical lead self-aligns the fastener within the tapped core hole before the first leading thread makes contact. This ensures true 90-degree thread engagement every time, dropping assembly crossthread rejection rates to below 0.002% on automated lines.
Achieving a reliable, reusable IP67/IP68 seal requires far more than slipping a loose O-ring under a conventional screw head. If a standard flat fastener is tightened, the rubber ring will squish outward, pinch, split, and lose sealing pressure.
YH Fasteners machines a cold-headed precision annular undercut (groove) directly beneath the head. The undercut volume is calculated to match the compressed volume of the silicone, Buna-N, or Viton O-ring with 25% to 30% controlled deformation. When torqued, the metal head makes direct flush contact with the enclosure panel, preventing over-compression while locking the elastomer within a 360-degree hermetic seal rated for submersion and high-pressure washdowns.
Thread galling (friction cold-welding) occurs when stainless steel fasteners are driven into stainless steel tapped holes or cage nuts under high speed. Friction shears off the protective chromium oxide layer, causing microscopic crystal asperities to fuse instantly and seize the joint completely.
To eliminate galling in critical stainless cabinet assemblies, we apply factory-engineered dry micro-coatings: anti-friction waxes, fluoropolymer dispersions, or thin-film molybdenum disulfide (MoS2). These solid lubricants reduce the thread friction coefficient to a uniform 0.10–0.15 range. This allows smooth automated torque driving up to 1,500 RPM without metal pickup, galling, or stripped driver bits.
In electrical cabinets and distribution switchboards, loose parts pose a severe safety hazard: an accidentally dropped loose lock washer falling across a high-voltage busbar can cause an explosive short-circuit arc flash during commissioning or maintenance.
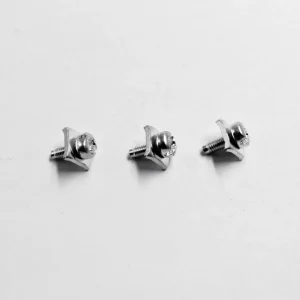
SEMS screws solve this risk fundamentally. Washers (conical spring, external tooth grounding, square terminal, or flat) are placed onto the blank shank before thread rolling. During rolling, the thread crest expands past the washer's inner diameter, making the washer permanently captive yet free to rotate freely. This slashes assembly handling labor by 40%, ensures the correct specified washer is never forgotten, and eliminates the risk of stray conductive washers falling into live electrical cabinets.
Our in-house die and tool design engineering department in Dongguan operates dedicated wire-EDM, mirror spark erosion, and CNC grinding centers. Upon customer approval of 2D/3D part drawings:
For outdoor telecom base stations, 5G pole cabinets, and coastal traffic controllers, standard decorative electro-zinc coatings fail within months. We engineer two proven metallurgical solutions depending on structural load needs:
1. Marine-Grade Austenitic Stainless Steel (A4 / SS316): Passivated via nitric-acid or citric-acid chemical baths to build an ultra-pure chromium oxide barrier that withstands indefinite exposure to marine salt fog.
2. Advanced Trivalent Zinc-Nickel Plating (12-15% Ni): Applied to high-strength carbon steel screws, yielding an electro-plated alloy barrier that withstands over 1,500 hours of continuous neutral salt spray (ASTM B117) with zero red rust, entirely free of Hexavalent Chromium (Cr6+).
