Direct factory supply of cold-forged and precision-rolled machine screws engineered to match standard and customized pre-tapped threads.
How the shift toward automated multi-axis torque assembly and lightweight substrates defines next-generation mechanical fastening.
Modern robotics demand tight lead thread chamfers and lead-in radii (typically conforming to 6g tolerance bands) to eliminate cross-threading in pre-tapped holes during high-RPM automatic blow feeding.
Pre-tapped cast aluminium, magnesium, and brass structures require strictly defined thread engagement lengths (1.5d to 2.5d). Our precision thread rolling guarantees zero burrs, reducing joint friction variables by 35%.
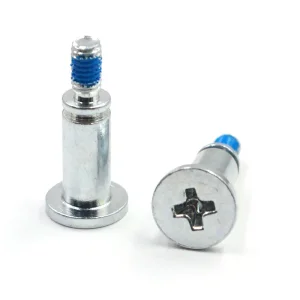
In high-vibration automotive power modules and aerospace actuators, pre-tapped holes can experience rapid pre-load loss. We engineer integral micro-encapsulated chemical patches and engineered thread flanks to ensure lasting resistance.
Enterprise procurement teams in North America, Europe, and Asia require verified consistency across every delivery tier.
Automated assembly rigs fail if seating torque fluctuates. We control surface treatments and lubricant friction coefficients (μ = 0.12–0.18) with strict SPC tracking.
Mill test certificates (EN 10204 3.1) are standard. Full chemical spectrum and metallographic inspections ensure clean raw wires for SUS304, SUS316, and Alloy Steels.
Complete Production Part Approval Process deliverables for automotive and medical clients, including DFMEA/PFMEA, control plans, and IMDS registration.
Direct door-to-door delivery pipelines with automated safety stock warehousing across key international freight hubs in Europe, the Americas, and APAC.
A comprehensive engineering comparison guide for selecting appropriate joining technologies across mission-critical assemblies.
| Evaluation Parameter | Pre-Tapped Hole Screws (Machine Threads) | Self-Tapping / Thread Forming Screws | Engineering Selection Advantage |
|---|---|---|---|
| Disassembly & Maintenance | Unlimited service cycles without degrading female threads. | Limited cycles; risk of stripping virgin thread walls. | Pre-Tapped is optimal for field service panels. |
| Internal Joint Stress | Even load distribution across engagement flank surfaces. | High residual hoop hoop-stress in boss structures. | Pre-Tapped eliminates boss cracking in delicate alloys. |
| Debris & Contamination | Zero debris generation during automated engagement. | Micro-chips generated during initial thread forming. | Pre-Tapped is required for cleanroom & optics. |
| High-Speed Insertion | High-RPM capability with zero tool-tip thermal buildup. | Requires torque monitoring to avoid excessive heat/friction. | Pre-Tapped streamlines assembly takt-time. |
| Sealing Reliability | Superior under-head clamping for O-rings and gasket interfaces. | Uneven seating torque can compromise seal contact geometry. | Pre-Tapped guarantees hermetic sealing integrity. |
Manufactured under verified IATF 16949 and ISO quality architectures to protect your downstream assembly line.
Every product is fully compliant with EU RoHS 2.0 (Directive 2011/65/EU) and REACH (EC 1907/2006) chemical limits, accompanied by full third-party laboratory documentation (SGS/TÜV).
State-of-the-art multi-camera vision sorting systems inspect 100% of critical dimensions—including pitch, major diameter, recess concentricity, and thread lead-in—down to 10 PPM standards.
Comprehensive 2D blueprints (PDF/DWG) and native 3D CAD models (STEP/IGES) supplied within 24 hours of technical scoping, facilitating immediate digital twin integration.
Aligning screw manufacturing capabilities with next-generation requirements in lightweight structures and connected hardware.
Expanding direct cold-heading processes for Grade 5 Titanium (Ti-6Al-4V) and A286 high-temp superalloys to slash payload mass in aerospace and robotics without trading shear performance.
Developing ultra-thin, hexavalent-chromium-free zinc-flake and ceramic layers under 5μm thick, providing over 1500 hours of neutral salt spray endurance with no thread pitch interference.
Integrating identification micro-markings directly into head geometry to enable automated tool vision tracking and real-time clamping data logging in Industry 4.0 production cells.
Key technical insights on specifications, lead times, and engineering parameters.
Pre-tapped hole screws possess blunt, parallel machine threads (typically 6g or 4h tolerances) configured to mate directly into an internally pre-threaded hole (such as 6H) without generating cutting debris or displacing substrate material. In contrast, thread-cutting screws feature notched flutes designed to carve new mating threads during drive-in.
We deploy three engineering solutions: pre-applied micro-encapsulated chemical adhesives (e.g., 3M, Scotch-Weld), mechanical resilient nylon locking patches (360° or 180° radial application), and integrated free-spinning or captive conical/spring washers (SEMS designs).
For custom non-standard fasteners requiring custom tooling, sample prototypes are delivered within 7 to 10 working days. Standard mass production MOQs begin at 10,000 to 50,000 units depending on diameter (M1.0 through M12), with pilot-run accommodations for prototyping.
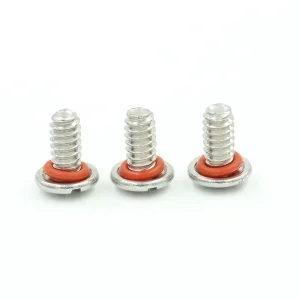
Yes. Our precision cold-forged sealing screws feature engineered under-head grooves that hold silicone, fluorosilicone, or Viton O-rings captive. Upon tightening, the elastomer achieves uniform radial compression without extrusion, preventing moisture or pressure leaks.
Explore our specialized threaded fasteners, manufactured with strict optical control for precision equipment.