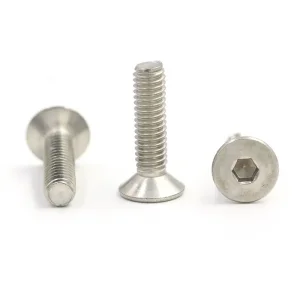
Direct from manufacturing lines: engineered machine fasteners delivering micro-tolerance cold forging, automated sorting, and multi-industry compliance.
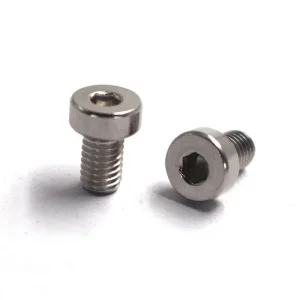
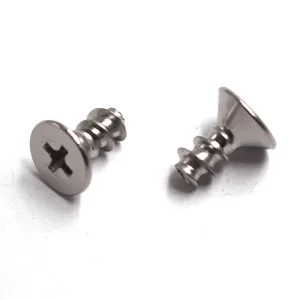

Evaluating under-head bearing pressure, drive torque stability, cold header metal flow, and tribological properties across micro and macroscopic assembly joints.
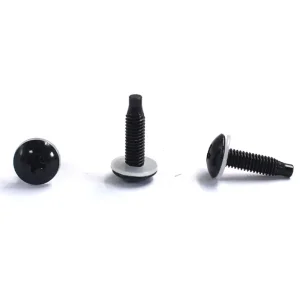
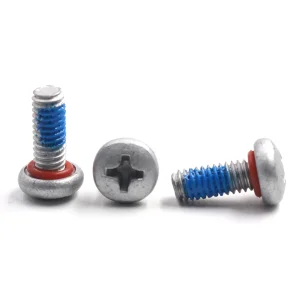
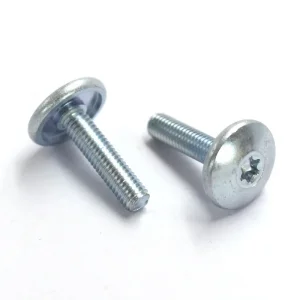
The pan head profile features a flat underside bearing surface coupled with low, rounded peripheral contouring. This geometry creates wide, uniform clamping force distribution across structural substrates without countersinking requirements, minimizing micro-cracking across plastics, stamped aluminum, and printed circuit boards.
Engineered per ISO 4757 & DIN 7985 standards, our cross-recess geometry maintains cold-formed wall taper angles that optimize bit-to-recess seating. The design balances bit grip and deliberate slip tolerances at high rotational speeds, protecting motor spindles during high-speed torque runs.
Rather than thread machining or single-stroke stamping, our multi-die cold formers redistribute the raw wire's crystallographic lines along the head contour into the shank. This eliminates internal micro-voids, increasing dynamic fatigue resistance by up to 38% over cut-thread hardware.
Across global industrial sectors, pan-head machine screws operate as key structural linkages, dampening harmonic vibrations and sealing electrical environments.
Within battery management systems (BMS), onboard charging modules, and sensory sensor housings, fasteners must withstand constant lateral G-forces and temperature fluctuations from -40°C to +150°C. We deploy high-tensile alloy steel and SS304 pan-head screws with 360° blue nylon patches or under-head vulcanized EPDM washers, maintaining preload stability under sustained road vibration.
Micro-electronic enclosures require tight shank-to-pitch concentricity to eliminate PCB track stress during installation. Our M1.6–M4 miniature pan-head machine screws undergo strict de-magnetization and clean passivation, preventing ionic surface contamination and ESD interference within cleanroom production lines.
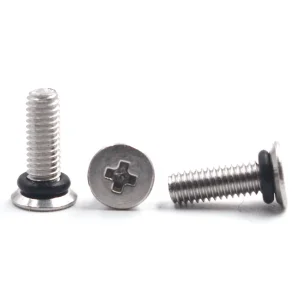
For IP67- and IP68-rated enclosures, fluid penetration along fastener threads poses risk of electronic failure. By cold-forming integrated under-head annular recesses, our pan-head sealing screws encapsulate silicone or fluoropolymer O-rings without pinching, creating a fluid barrier that withstands up to 50 bar internal pressure.
Navigating raw-material shifts, automated assembly line tolerances, and modern supply chain dynamics across international manufacturing centers.
Global wire rod markets face price fluctuation across austenitic stainless grades (AISI 304/316) and alloy bases (SCM435, 10B21). We hedge these dynamics via strategic mill-direct partnerships across Shaoguan and Wuhan, providing consistent material grading alongside verifiable heat, melt, and lot numbers.
High-volume robotic pick-and-place lines feed screws through pneumatic tubes. Minor heading flash, slot burrs, or thread malformations can halt multi-million-dollar lines. Our 360° laser optical sorters isolate diameter, pitch, and drive concentricity at 800 parts/min, maintaining near-zero assembly downtime.
European and North American buyers increasingly require low-carbon fastener supply chains under CBAM directives. We run closed-loop cold-heading lubricant recycling, low-energy induction heat treatment, and chrome-free surface lines (RoHS/REACH verified), balancing structural performance with sustainability.
Meeting multi-market compliance demands through strict metallurgical traceability, verified clean chemistry, and production audit procedures.
Full PPAP Level III documentation packages: Process FMEA, Control Plans, Dimensional Results, Material Certifications, and IMDS registration for automotive integration.
Certified chemistry containing zero heavy metals, lead, or SVHC contaminants. Surface electroplating and passivation layers pass 720-hour neutral salt spray tests per ASTM B117 without white or red rust.
With three manufacturing locations across Dongguan, Shaoguan, and Wuhan, we balance high-volume cold heading across multiple facilities, mitigating localized supply bottlenecks.
Direct application engineering access: 2D drawing review, step-file clearance verification, thread-class validation (6g / 6H / Class 2A/2B), and pilot sample fabrication in under 7 business days.
| Property / Characteristic | DIN 7985 / ISO 7045 Reference | JIS B 1111 (Pan Style) | YH Precision Custom Engineered Line |
|---|---|---|---|
| Head Diameter Tolerance | h14 Standard Window | ±0.15mm Nominal | Controlled to ±0.03mm (Automated Feeding Tier) |
| Drive Recess Concentricity | ≤ 0.15mm Radial Runout | ≤ 0.12mm Radial Runout | ≤ 0.05mm High-Speed Bit Alignment |
| Tensile Strength Options | Class 4.8 / 8.8 (Carbon Steel) | Class 4.8 / SCM435 | Class 4.8, 8.8, 10.9, 12.9, SS304, SS316, A2-70, A4-80 |
| Salt Spray Resistance (NSS) | 48–96h (Standard Clear Zinc) | 72h (Yellow Chromate) | Up to 1,000+ Hours (Trivalent + Sealer / Geomet Zinc Flake) |
| Anti-Loosening Functionalization | Split Ring / Star Washer Only | None Standardized | Pre-Applied Polyamide 360° Patch / 180° Strip / SEMS Captives |
Targeted engineering case studies demonstrating customized pan-head machine screws operating under real-world assembly constraints.
Challenge: Outdoor aluminum telecommunication housings suffered galvanic corrosion and moisture seep through thread pathways, degrading sensitive RF equipment.
Solution: Custom SS316 Phillips pan-head screws engineered with an integral under-head vulcanized EPDM seal ring, paired with a ceramic-reinforced passivation bath that passed 1,200 hours NSS exposure.
Challenge: Cooling fan harmonic resonances induced rotational loosening in traditional M3 standard fasteners, leading to intermittent ground continuity faults.
Solution: Transitioned to M3 Class 8.8 heat-treated pan-head screws treated with a micro-encapsulated anaerobic pre-applied adhesive patch, sustaining a continuous prevailing breakaway torque above 0.8 Nm over 500 thermal duty cycles.
Challenge: Automated sorting nozzles in sterile lab gear experienced occasional drive-camout metal shavings, threatening bio-sample integrity.
Solution: Redesigned Phillips recess geometry to deep-engagement Phillips/Slot combination profiles with electropolished SS304 surfaces, eliminating tool stripping and keeping bit engagement consistent at lower driver feed pressure.
Where cold forming meets digital manufacturing: tracking smart sensor integration, nanostructured coatings, and circular metal recovery initiatives.
We are integrating piezoelectric acoustic and pressure transducers inside cold-heading dies to monitor tool wear per strike. This allows machine controllers to flag micro-fissuring or tool chipping within milliseconds, preventing non-conforming fasteners from reaching downstream sorting bins.
Torque-tension scatter often leads to stripped threads or loose joints. Our advanced finishing research applies molybdenum disulfide and fluoropolymer-doped nano-coatings to ensure an exact friction coefficient window (µ = 0.08–0.14), keeping clamping forces repeatable under robotic air-tool assembly.
By leveraging batch traceability via 2D matrix codes etched onto lot shipping cartons, industrial clients can verify raw-material scrap origins. We prioritize suppliers utilizing >85% recycled scrap-based electric arc furnace (EAF) wire rods, shrinking the carbon footprint per fastener shipped overseas.
Engineered responses addressing procurement queries regarding head styles, recess geometry, thread pitch selection, and custom batch tooling.
Pan-head profiles feature a lower, broader head with a flat under-bearing surface designed to sit flush on mating materials, maximizing clamping distribution without countersinking. In contrast, button heads feature higher-profile rounded crowns often paired with hex drives, while traditional round heads have higher spherical profiles and narrower bearing bases that increase localized contact pressure.
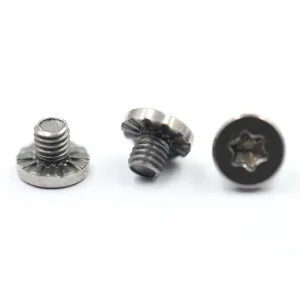
Cam-out happens when driver bits slip upwards from excessive torque or tool misalignment. We limit this by holding cold-heading punch dies to high optical tolerances, maintaining exact wall angles and sharp recess radiuses. We also supply custom bit-matched Phillips-indented, Phillips-slot combination, or Torx-drive pan alternatives for high-torque robotic lines.
We forge coarse pitch (UNC / Metric Standard) and fine pitch (UNF / Metric Fine) configurations per ISO 965 and ASME B1.1 standards. For plastics and ductile cast metals, we also manufacture custom PT-style thread geometries that lower radial expansion stress, preventing boss burst failures in polycarbonate or ABS enclosures.
Yes. Our in-house engineering and tooling centers build custom cold-heading dies directly from STEP, IGES, or 2D technical drawings. We accommodate unique shank steps, extended under-head radiuses, captive washer assemblies (SEMS), custom lead-in dog points, and custom head-stamped lettering.
High-tensile carbon and alloy steel screws (Class 8.8, 10.9, 12.9) absorb atomic hydrogen during acid pickling and electroplating baths. We apply strict de-embrittlement baking at 200°C–220°C for 4 to 12 hours immediately following plating, verified through sustained load testing per ISO 15330 to eliminate delayed brittle fracture risks.
Explore non-standard head styles, anti-vibration coatings, and modular SEMS combination screws tailored for diverse industrial assemblies.