Engineered cold-formed fasteners with captive washers, sealing seals, and anti-vibration coatings deployed globally across e-mobility, industrial electronics, and automation systems.


Analysis of dynamic joint mechanics, automated high-speed assembly integration, and the replacement of discrete washer-bolt systems across modern discrete manufacturing.
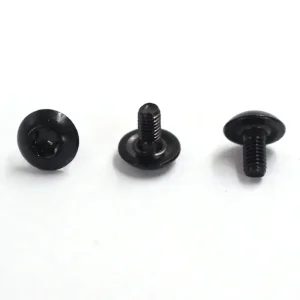
In modern industrial manufacturing, the humble threaded fastener has transformed from a purely static passive retention component into an active, highly engineered subsystem. Combination screws—universally classified in precision engineering as SEMS screws (derived from the German pre-assembled machine screw assembly methodology)—integrate one or more pre-assembled free-spinning washers permanently retained by a rolled thread profile whose major diameter exceeds the inner diameter of the washer.
Historically, high-volume production facilities suffered severe systemic bottlenecks caused by separate manual or vibratory bowl-feeding of loose flat washers, helical split-ring lock washers, and Belleville conical spring discs. This split-stage operation frequently resulted in missing components, uncalibrated preload forces, unbalanced friction coefficients, and catastrophic vibrational loosening in the field. Custom OEM combination screws eliminate this operational risk at the architectural level.
Technical Axiom: The captive integration of specialized washers prior to the cold thread-rolling process guarantees 100% mechanical containment, establishes a repeatable friction torque ratio (±0.015 μ), and slashes assembly-line cycle times by up to 42% on automated continuous lines.
Consolidating discrete washer feed chutes and separate bolt torquing stages cuts cycle duration down to sub-1.2 second pick-and-drive intervals in automated robotic cells.
Eliminates missing spring or flat washers—a failure mode responsible for 34% of field torque relaxations in heavy mechanical vibrations and automotive chassis units.
Engineered captive contact washers evenly disperse dynamic clamp preload, eliminating embedment yielding, localized brinelling, and plastic shear across delicate aluminum or composite substrates.
Washer outer diameters, free-spin clearance angles, and head configurations are calibrated to prevent jamming inside pneumatic blow-feed tubes and magnetic pick-and-place end-effectors.
Rigorous quality expectations enforced by Fortune 500 procurement teams spanning Tier-1 automotive, consumer technology, and industrial electrical assemblies.
Global original equipment manufacturers require strict Advanced Product Quality Planning (APQP). Every custom SEMS production order is backed by full Production Part Approval Process (PPAP Level 3) documentation:
Modern high-speed robotic insertion lines cannot tolerate a single deformed fastener or thread flash. Hand-sorting is completely obsolete. Global contracts mandate 100% automated high-speed multi-camera laser/optical glass disc sorting:
Cross-border supply chain security requires rigorous material pedigree tracking and international environmental stewardship under EU and global standards:
How cutting-edge industrial automation, continuous digital telemetry, and vertical integration establish global cost and quality supremacy.
The global fastener landscape has experienced a profound shift from distributed, fragmented sub-contracting toward heavily integrated, automated manufacturing clusters centered in Dongguan, Guangdong. In conventional fastener manufacturing, wire drawing, cold heading, washer assembly, thread rolling, heat treatment, and surface electroplating often took place across five independent sub-suppliers—introducing severe supply chain latency, moisture-induced hydrogen embrittlement risks, and unpredictable lot-to-lot dimensional variations.
Under our China Factory 4.0 framework, the entire production lifecycle of an OEM combination screw is consolidated within automated, digitally monitored facilities spanning over 20,000 square meters. High-speed multi-station cold heading machines integrate automated washer feeding tracks directly into the thread rolling cycle, forming rolled threads that permanently lock custom-stamped washers in continuous operations operating at over 280 units per minute.
In-house carbide tooling fabrication allows custom head recess stamping (Torx Plus, Phillips/Slot combos, Tamper-proof pins) with micron-level alignment dies.
Rapid iterative prototyping delivers production-grade PPAP tooling within 7 to 10 working days, reducing automotive launch timelines by over 60%.
Computerized mesh belt furnace lines with real-time carbon potential monitoring (Cp control within ±0.02%) eliminate surface decarburization and core brittleness.
Strict post-plating hydrogen de-embrittlement baking cycles (200°C to 220°C for 4 to 12 hours) prevent delayed catastrophic brittle shear failure on Grade 8.8, 10.9, and 12.9 fasteners.
Sensors track header impact tonnages in real time. Any die chipping or wire diameter irregularity triggers instantaneous machine halting before out-of-spec batches generate.
Automated optical sorting arrays record 100% of dimensional profiles to central SPC servers, guaranteeing complete batch traceability across 60+ export markets.
Comprehensive engineering reference for selecting tensile classes, washer kinematics, and protective micro-coatings tailored to hostile operational environments.
| Base Alloy / Material | Combination Configurations | Tensile / Hardness Range | Protective Finish / Passivation | Primary Industrial Sector |
|---|---|---|---|---|
| Austenitic Stainless (SS 304 / A2-70) | Flat Washer + Wave Spring Washer | Tensile: 700 - 850 MPa Hardness: HRB 85 - 95 |
Electrochemical Passivation, Cleanroom Ultrasonic Degreasing | Medical Devices Food Tech |
| Marine Stainless (SS 316 / A4-80) | Captive Fluorosilicone / EPDM O-Ring | Tensile: 800 - 950 MPa Hardness: HRB 90 - 100 |
Citric Acid Passivation / PVD Black Coating | Outdoor Enclosures Marine Solar |
| Medium Carbon Alloy (AISI 1022A / 10B21) | External Tooth Serrated Washer + Flat | Class 8.8 / 10.9 (Heat Treated) Core Hardness: HRC 32 - 39 |
Trivalent Clear/Yellow Zinc (8-12μm), 96h Red Rust Salt Spray | Power Switchgear HVAC |
| Case-Hardened Carbon Steel | Belleville Conical Washer (DIN 6796) | Surface Hardness: HV 550 - 680 Core: HRC 28 - 36 |
Zinc-Nickel Alloy Plating (>1000h Salt Spray to ASTM B117) | EV Battery Modules Chassis |
| High-Conductivity Copper-Brass Alloy | Square Saddle Clamp Terminal Washer | Yield: 250 - 400 MPa High Electrical Conductivity |
Tin Plated (Sn), Silver Plating (Ag) for Low Contact Resistance | Circuit Breakers Terminal Blocks |
Targeted mechanical configurations engineered to solve extreme vibration, hermetic sealing, and high-frequency thermal expansion challenges.
Challenge: Heavy thermal cycling during rapid DC supercharging creates dynamic thermal expansion differences between aluminum busbars and copper terminals, causing gradual bolt preload decay.
SEMS Solution: Class 10.9 Torx pan combination screw with captive Belleville conical spring washers. The engineered spring deflection curve maintains continuous clamp pressure across -40°C to +125°C.
Challenge: Outdoor junction boxes, radar radomes, and marine telecommunications units suffer fluid ingress at threaded mounting interfaces subjected to high wind load and UV radiation.
SEMS Solution: Pan head stainless steel 304/316 combination screw integrated with captive molded silicone/EPDM O-rings. When torqued, the undercut head geometry compresses the seal without radial tear-out.
Challenge: High-speed servo motors and robotic joint gearboxes experience continuous multi-axis resonant vibration, inducing fast back-out of conventional threaded fasteners.
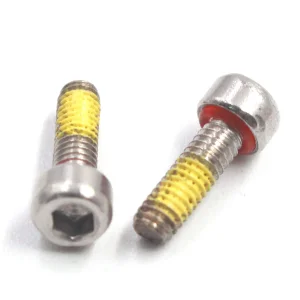
SEMS Solution: Combination screw equipped with captive dual spring-lock washers plus micro-encapsulated threadlocker patch (nylon or reactive chemical acrylic), preventing self-loosening under harmonic shock.
Challenge: Multi-conductor stranded cable connections in high-vibration industrial cabinet distribution boards demand zero resistive heating and low contact resistance.
SEMS Solution: Tinned cross-recessed machine screw with square saddle clamp washer featuring anti-spread bottom ribs, firmly locking stranded wires without fraying or localized current hotspots.
Preventative engineering practices addressing the five primary root causes of mechanical failure in dynamic threaded joints.
Root Cause: High-strength carbon steel (>HRC 32, Class 10.9+) absorbs atomic hydrogen during acid pickling or electroplating, initiating sub-critical delayed cracking under sustained tensile stress.
Mitigation: Mandatory dry mechanical descaling or baking at 210°C within 2 hours of electroplating for a minimum duration of 8 hours, verified through destructive stress-rupture qualification tests.
Root Cause: Surface microscopic roughness asperities on unhardened washer faces yield and plastically flatten post-torquing, causing loss of clamping preload without any rotational back-off.
Mitigation: Cold rolled threads combined with thoroughly through-hardened flat and conical washers to equalize surface stress distribution below the substrate yield point.
Root Cause: Pairing standard zinc-plated carbon steel screws with bare aluminum enclosures initiates severe anodic sacrifice in the presence of conductive moisture.
Mitigation: Implementation of zinc-nickel alloy coatings with specialized inorganic nano-sealers, insulating nylon washers, or custom austenitic 316 stainless steel assemblies.
Key technical, manufacturing, and procurement inquiries answered by our senior application engineering directors.
Complementary precision thread-forming screws, positioning spring plungers, and non-standard industrial fasteners manufactured across our 3 Chinese plants.