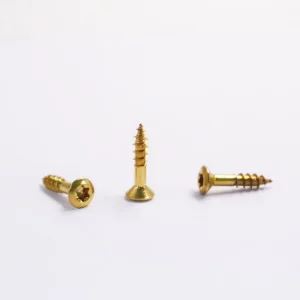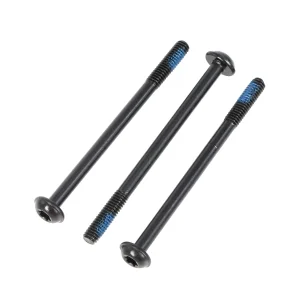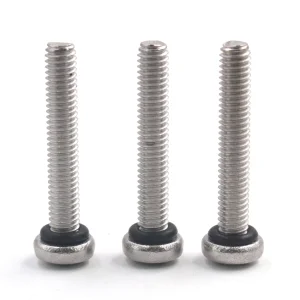
Direct from our audited production lines: heavy-duty hex assemblies, pre-coated self-sealing fasteners, and vibration-proof retaining screws engineered for harsh vehicular duty cycles.


As the automotive sector transitions toward software-defined vehicles (SDVs), multi-material battery chassis, and distributed 800V e-axles, the baseline mechanical criteria for hex fasteners have evolved beyond basic clamp load.
Next-generation vehicle platforms demand ultra-high-tensile fasteners (Property Class 10.9 and 12.9) that mitigate weight penalties without compromising clamping integrity. By applying micro-alloyed boron steels (20MnB4, 32CrB4) and proprietary multi-stage cold header drawing, we achieve higher yield strength-to-density ratios, allowing design teams to downsize thread diameters (e.g., transitioning from M12 to M10) without clamp loss.
High-voltage battery module enclosures and battery management system (BMS) busbar junctions require custom hex flange screws featuring both physical isolation and controlled grounding. Our engineering roadmap encompasses functionalized organic and inorganic ceramic-filled hybrid coatings that withstand dielectric breakdown voltages up to 2,500V DC while maintaining stringent friction coefficients (μtot = 0.10–0.16).
Combating severe resonance across chassis, steering knuckles, and powertrain assemblies requires active thread engagement technologies. Our roadmap integrates advanced mechanical micro-encapsulated anaerobic adhesives (DIN 267-27) and 360° pre-applied polyamide patches (DIN 267-28), eliminating bolt loosening caused by transverse vibrational fatigue under Junker test protocols (DIN 65151).
Deploying tailored fastening topologies across body-in-white (BIW), battery pack seals, interior structural cockpits, and extreme powertrain thermal boundaries.
Hex washer head bolts engineered with captive molded EPDM or fluorosilicone gaskets guarantee permanent barrier seals against moisture, electrolytic vapors, and particulate intrusion, fully satisfying IP67 and IP69K waterproof washdown mandates.
High-integrity Class 10.9 hex flange bolts paired with integrated serrations prevent relative displacement across control arm and suspension linkage joints. Designed with controlled radii transitions to resist shear stresses and rotational fatigue.
Combining compact washer geometries with non-standard pan and hex head designs. Optimized for swift robotic feeding with optical sorting tolerances held to <20 PPM for rapid automated module assembly.
Corrosion-resistant A2/A4 stainless and zinc-nickel plated hex fasteners delivering over 1,500 hours of neutral salt spray (ASTM B117) resistance without white or red rust, even in sub-frame locations exposed to severe road de-icing salts.
Leveraging the robust industrial cluster of Dongguan, Shaoguan, and Wuhan to deliver verified capacity, real-time closed-loop quality tracking, and comprehensive cost resilience.
High-speed 5-die and 6-die cold formers operate at rates up to 300 pieces per minute. By optimizing grain boundary orientation through near-net-shape continuous plastic deformation, we achieve superior fatigue endurance compared to conventional machining.
Human manual inspection cannot guarantee zero-defect parameters for automated robotic assembly lines. Our 360-degree glass plate vision sorting tables utilize multi-camera optical laser arrays to inspect threads, head diameters, pitch, and recess depth with zero escapes.
Spanning over 20,000 m² across Dongguan, Shaoguan, and Wuhan facilities, our footprint buffers against localized raw material volatility and energy disruptions, guaranteeing uninterrupted delivery schedules for cross-continental OEM programs.
Every custom fastener batch is reinforced by rigorous auditing methodologies, international environmental certifications, and localized engineering support.
| Audit Dimension | Standards & Methodologies | Technical Verification Scope | Procurement Deliverable |
|---|---|---|---|
| Quality System | IATF 16949 / ISO 9001:2015 | APQP Stage Gate reviews, FMEA risk assessments, full SPC lot control | PPAP Level 3 Dossier (Control Plan, PSW) |
| Mechanical Property | ISO 898-1 / SAE J429 / ASTM A574 | Proof load, tensile strength, core micro-hardness (Vickers / Rockwell), elongation | EN 10204 3.1 Mill Inspection Test Report |
| Corrosion & Plating | ISO 9227 / ASTM B117 / DIN 50021 | Neutral Salt Spray (NSS), cyclical humidity chamber tests, X-ray plating thickness gauge | Salt Spray Environmental Test Log (>1,000h) |
| Environmental Safety | RoHS 2011/65/EU / REACH (EC 1907/2006) | Hexavalent chromium-free passivation, SVHC screening, VOC emission testing | IMDS Material Data Sheet Submission |
| Hydrogen Embrittlement | ISO 15330 / ASTM F1940 | Baking relief verification (200°C+ within 4h of plating), sustained load test | De-embrittlement Certification of Conformity |
Empowering automotive mechanical procurement engineers with comprehensive design envelopes, surface plating options, and precision drive types.
Carbon Steel (10B21, 1022A, 1035, 1045), Alloy Steel (40Cr, 35CrMo, 42CrMo), Stainless Steel (AISI 302, 304, 316, 410), and Aerospace-grade Titanium alloys upon custom inquiry.
External Hexagon, Hex Flange (Smooth/Serrated), Hex Socket (Allen), Torx (Six-Lobe), Security Tamper-Resistant Pin-in-Hex, Indented Hex Washer, and Low-Profile Cap Heads.
Geomet, Dacromet, Magni, Eco-friendly Zinc Nickel Plating (Clear/Black Passivation), Hot Dip Galvanizing, Mechanical Zinc, Phosphate Coating, and Electrophoretic E-Coat.
Micro-encapsulated Threadlocker, Polyamide Patch 90°–360°, Pre-assembled Sems Free-spinning Flat/Spring Washers, Captive Overmolded O-rings, and Under-head Ribs.
Direct answers to core inquiries regarding lead times, testing protocols, custom tooling development, and compliance workflows.
For high-tensile fasteners (core hardness exceeding 320 HV), electroplating triggers hydrogen atom penetration. We enforce mandatory de-embrittlement baking at 200°C–230°C for a minimum of 4 to 8 hours within 4 hours post-acid activation and electroplating, validated via ISO 15330 pre-stress testing.
Standard PPAP Level 3 submissions include: Part Submission Warrant (PSW), Design Records, Process Flow Diagram, Process FMEA, Control Plan, Measurement System Analysis (MSA), Dimensional Results (Full CMM Report), Material & Performance Test Records, and IMDS confirmation.
Yes. Our in-house tooling shop fabricates custom cold heading dies and header punches for non-standard flange widths, undercut neck radii, and integrated captive washers according to 2D/3D customer models with rapid 10-day prototyping timelines.
We calibrate friction coefficient (μ = 0.12–0.18 per VDA 235-101) by introducing proprietary topcoats and torque-tension control sealers, ensuring repeatable clamp loads without galling during automated screwdriving on robotic production lines.
All finished lots pass multi-camera glass rotary sorting stations checking: pitch uniformity, head crack defects, shank straightness, recess depth, and plating continuity. Target defect levels can be customized to under 10 PPM upon OEM agreement.
Standard custom cold-headed production MOQs typically range from 50,000 to 100,000 units depending on thread diameter. Prototype sample runs require 7–12 working days, with mass production runs completing in 3 to 4 weeks.
Explore our broader manufacturing capabilities spanning parallel-thread machine screws, modular spring plungers, locking patch hardware, and outdoor weather-proof sealing assemblies.