Direct from Yu-Huang Electronics (Dongguan, Shaoguan, Wuhan plants) engineered to ISO, DIN, ANSI, and JIS engineering standards.


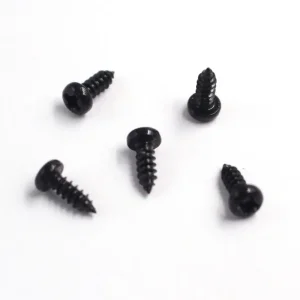

Evaluating the technical capabilities, raw material integration, and high-speed cold-heading capacity of Chinese supply chains.
From raw coil sourcing (1018, 1022A, SUS304, SUS316) to spheroidized annealing and chemical pickling, China's Pearl River Delta and Yangtze manufacturing corridors guarantee consistent metallurgical homogeneity, preventing shear failures during high-torque driving.
Equipped with 4-die and 5-die cold headers capable of holding micron-level tolerances (±0.02mm). Tooling profiles for cross recesses conform strictly to ISO 4757 / JIS B 1012, significantly eliminating screwdriver cam-out and bit wear.
Industrial factories implement real-time SPC (Statistical Process Control), eddy current sorting, and optical sorting gates to deliver zero-defect PPM levels across automotive electronics, smart metering, and automated robotic systems.
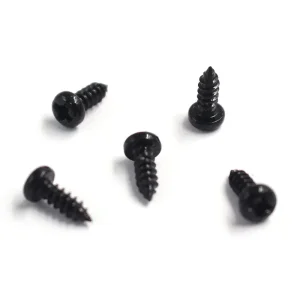
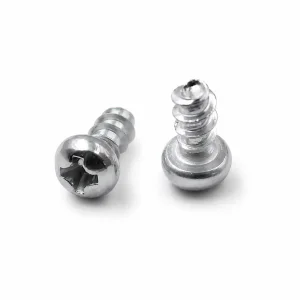
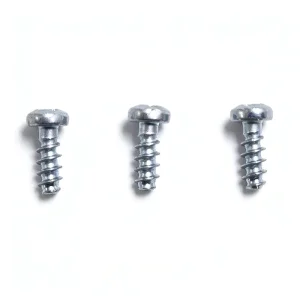
Parametric analysis across standard sheet metal (Type A/AB) and thread-cutting profiles (Type F/BT) compliant with DIN 7981, ISO 7049, and ANSI B18.6.4.
| Nominal Size | Major Thread Ø (d) | Head Diameter (dk) | Head Height (k) | Phillips Drive No. | Torsional Strength (Min. N·m) | Applicable Substrates |
|---|---|---|---|---|---|---|
| M2.2 (No. 2) | 2.10 – 2.24 mm | 4.00 – 4.20 mm | 1.55 – 1.80 mm | #1 Cross Recess | 0.45 N·m | Micro-plastics (ABS/PC), Thin PCB Shields |
| M2.9 (No. 4) | 2.79 – 2.90 mm | 5.30 – 5.60 mm | 1.95 – 2.20 mm | #1 Cross Recess | 1.50 N·m | Electronics Chassis, Instrument Consoles |
| M3.5 (No. 6) | 3.35 – 3.53 mm | 6.54 – 6.90 mm | 2.35 – 2.60 mm | #2 Cross Recess | 2.80 N·m | Cold-Rolled Steel Sheet (<1.2mm), Extruded Aluminum |
| M4.2 (No. 8) | 4.04 – 4.22 mm | 7.84 – 8.20 mm | 2.75 – 3.05 mm | #2 Cross Recess | 4.50 N·m | Automotive Interior Trims, HVAC Ductwork |
| M4.8 (No. 10) | 4.62 – 4.80 mm | 9.14 – 9.50 mm | 3.25 – 3.55 mm | #2 Cross Recess | 6.50 N·m | Structural Metal Framing, PV Solar Inverters |
| M5.5 (No. 12) | 5.28 – 5.46 mm | 10.37 – 10.80 mm | 3.65 – 3.95 mm | #3 Cross Recess | 10.00 N·m | Heavy Enclosures, Outdoor Telecommunication Cabinets |
A transparent look at the multi-stage manufacturing workflow in our 20,000 m² facilities.
Incoming carbon steel or austenitic stainless wire (SUS304/316) is verified using optical emission spectrometry. Raw material undergoes automated wire drawing and spheroidization to eliminate micro-cracking.
High-speed cold-heading machines deform the metal along unbroken grain structures. Pan heads are formed alongside precision Phillips recesses matching ANSI/JIS gauges to maximize bit torque transfer.
Precision thread dies roll rather than cut threads, yielding superior thread surface integrity, refined shear strength, and burr-free tapered lead threads (Type AB, B, or F points).
Continuous mesh belt furnaces deliver case hardening (carburizing and tempering) to achieve surface hardness above 450 HV and core toughness between 270–390 HV, ensuring penetrative tapping into unthreaded steel.
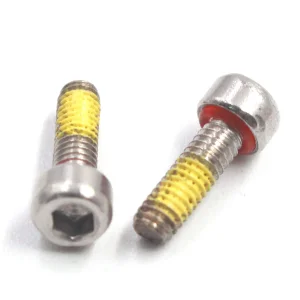
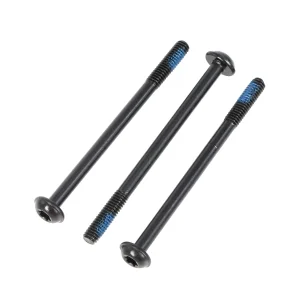
Surface treatments include environmentally compliant trivalent zinc, zinc-nickel plating (withstanding 1000+ hours neutral salt spray testing), passivated stainless finishes, and pre-applied nylon patches for anti-loosening.
High-speed optical inspection machines evaluate 100% of fastener lots for thread pitch, head concentricity, recess depth, and plating defects before automated batch packing with full lot traceability.
Addressing systemic engineering challenges across automotive electronics, consumer hardware, renewable energy, and industrial infrastructure.
Precision pan head tapping screws eliminate internal tap debris that can cause circuit shorts. Fine-pitch threads provide high pull-out resistance in cast zinc, aluminum extrusions, and thin polycarbonate housings.
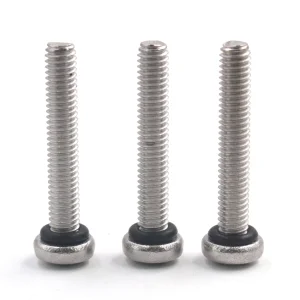
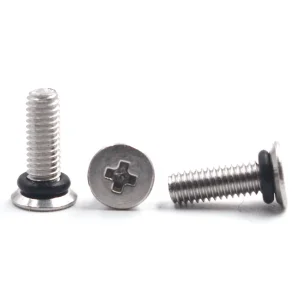
With IATF 16949 audit compliance, fasteners incorporate micro-encapsulated thread lockers or integrated EPDM/nylon washers, enduring high-frequency automotive vibration without backout.
Severe outdoor installations demand A2-70 / A4-80 stainless steel or advanced Delta-Protekt coatings, preventing galvanic corrosion in humid, coastal, and chemical environments over multi-decade lifespans.
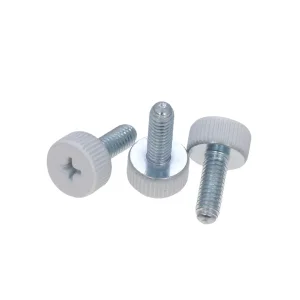
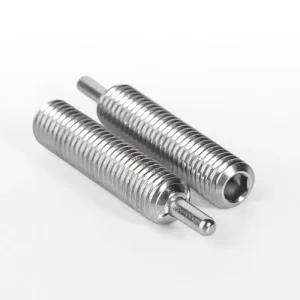
Explore our specialized production lines, including knurled thumb screws, SEMS assemblies, spring plungers, and vibration-resistant coatings.

Direct answers to core queries from procurement directors, mechanical engineers, and quality assurance leads.
Type A features a coarse thread with a sharp gimlet point designed for thin sheet metal (0.4–0.8 mm). Type AB has finer threads and a tapered gimlet point, offering lower driving torque in fragile brittle plastics and sheet metal up to 1.5 mm. Type B uses blunt tapered points for heavier sheets, plastic bosses, and die castings to avoid over-penetration hazards.
For case-hardened screws (1022A, Grade 8.8 equivalent) that undergo electro-galvanizing or acid pickling, hydrogen embrittlement poses catastrophic shear risks. Our facilities mandate immediate de-embrittlement baking at 200°C–220°C for a minimum of 4–8 hours immediately after plating, verified by destructive stress-durability testing.
Yes. As an IATF 16949 certified manufacturing group, we routinely supply Production Part Approval Process (PPAP) Level 3 packages. This includes Process FMEA, Control Plans, IMDS reporting, Gage R&R studies, Material Mill Certifications, Full Dimensional Inspection Reports (DIR), and Salt Spray Chamber validations.
Pan heads offer an optimal compromise between head surface area and low clearance profile. The flat underhead bearing surface distributes clamp loads evenly across sheet surfaces without countersinking, while slightly rounded contours prevent catching. Truss heads have a broader, lower profile, but pan heads handle significantly higher dynamic installation torques.
