

Factory-direct high precision metric hardware engineered to eliminate cam-out, ensure repeatable preload, and fulfill airtight IP67/IP68 sealing standards across harsh industrial environments.

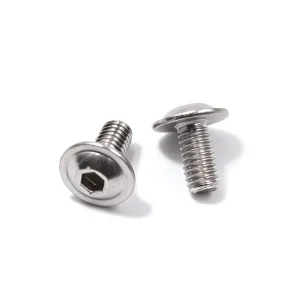

An analytical overview of structural tension distribution, automated feed compliance, and cross-recess mechanical integrity in high-throughput assembly lines.
Pan-head machine screws provide a wider, low-profile bearing area compared to round or fillister heads. This geometric signature uniformly distributes clamping force across soft non-ferrous alloys, sheet metals, and injection-molded plastics without localized surface crushing.
Modern high-speed robotic assembly demands strict adherence to dimensional concentricity. Our fasteners undergo 100% optical grading to secure drive recess depth, avoiding magnetic pickup failure, misaligned blow-feeding, and production jamming.
From EV powertrain electronic control units (ECUs) to consumer telemetry devices, pan-head fasteners serve as the core mechanical joint. Combining Class 8.8/10.9 tensile capabilities with localized locking elements ensures complete anti-loosening confidence.
Review our application-specific technical matrices tailored to solve thermal divergence, electrolytic corrosion, and continuous mechanical shock.
| Sector / Application | Material & Strength Class | Surface Treatment / Coating | Drive & Head Attributes | Engineering Benefit |
|---|---|---|---|---|
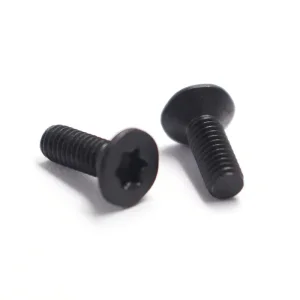
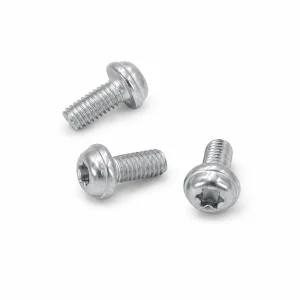
| Automotive Electronics (ECU / ADAS) | AISI 304 / 316 / SCM435 (Gr 8.8 / 10.9) | Geomet, Dacromet, Zinc-Nickel (720h+ NSS) | Torx (6-Lobe) Pan Head with Micro-Nylon Patch | Zero cam-out; resists road vibration and galvanic degradation. |
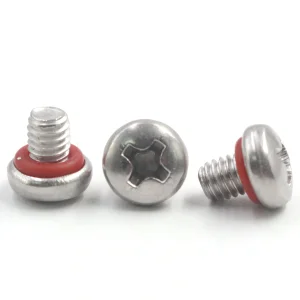
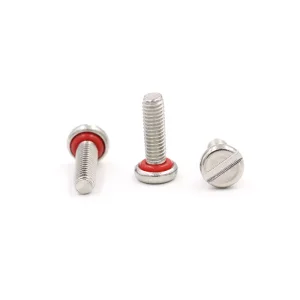
| Telecommunications & Outdoor 5G | Austenitic Stainless Steel 316 (A4-70) | Chemical Passivation, Electropolished | Pan Head with Integrated Fluorosilicone O-Ring | Certified IP68 sealing; impervious to atmospheric salt spray. |
| PCB & Computing Infrastructure | Carbon Steel 1018 / 1022 / SUS304 | Bright Nickel / Trivalent Zinc (RoHS compliant) | Cross-Recessed Phillips Pan Head with Captive Sems | Uniform grounding conductivity; prevents dropped hardware on PCB. |
| Thermoplastic Enclosures | Case Hardened 1022 Carbon Steel | Black Oxide, Zinc Yellow Passivated | Pan Head PT Thread Forming Geometry (30° profile) | Minimizes radial stress in bosses; prevents boss cracking/bursting. |
| Heavy Automation & Robotics | Medium Carbon Alloy Steel (Class 10.9 / 12.9) | Manganese Phosphating + Oil Impregnation | Hex Socket / Torx Plus Pan Head | Maximum clamp torque absorption under recurring cyclic shear forces. |
How advanced metallurgy, precision cold-forming kinematics, and sustainable electro-coatings are transforming the global fastener landscape.
By transitioning toward multistation high-speed progressive cold-heading machines, we guarantee uninterrupted grain-flow lines along the screw shank, radius, and pan head junction. This completely eliminates internal void formulation, enhancing cyclic fatigue life by over 38% compared to standard machined alternatives.
Aligned with stringent EU Reach and RoHS directives, our metallurgical laboratories have eliminated hexavalent chromium completely. Next-generation multi-layer nanostructured zinc-flake and ceramic-infused electro-coatings achieve 1500+ hours neutral salt spray resistance while maintaining negligible hydrogen embrittlement risk.
To support global automated factory floors that operate at near-zero human supervision, our production line implements high-frequency laser telemetry and multi-angle optical sorting machines. Fasteners are verified for shank thread pitches, head concentricity, recess depth, and plating uniformity at over 800 units per minute.
Delivering engineering authority, predictable lead times, and frictionless cross-border distribution from Dongguan, Shaoguan, and Wuhan to international hubs.
Yu-Huang operates rigorous full-process quality governance across its manufacturing hubs. From spectral material verification of incoming wire rods to in-process dimensional control and comprehensive lot traceability, every shipment complies strictly with ISO 9001, ISO 14001, and IATF 16949 standards.
Exporting to more than 60 countries across North America, Europe, and Southeast Asia, our logistics architecture incorporates buffer-stock management programs (VMI/Kanban) to insulate tier-1 procurement pipelines against global maritime schedule variances.
Explore additional precision fastening architectures including sealing screws, socket caps, flat countersunk variants, and heavy-duty thread-cutting screws.
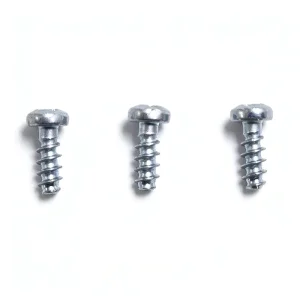
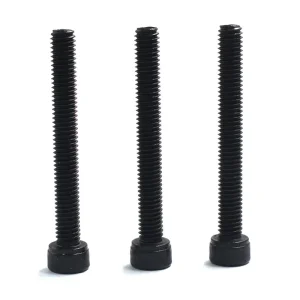
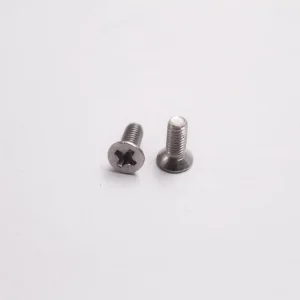


In-depth technical answers regarding dimensional standards, drive recess specifications, and metallurgical performance.
While all three specifications designate cross-recessed pan-head machine screws, their head diameters, head heights, and radius curvature vary significantly. DIN 7985 generally possesses a higher head profile and larger outer head envelope than ISO 7045. JIS B 1111 screws are designed with slightly lower head profiles and specific cross-recess dimensions tailored for Japanese standard driver bits to eliminate cam-out. Yu-Huang manufactures according to all standard matrices and maintains custom cold-heading dies to manufacture exact dimensional profiles from buyer drawings.
Cam-out occurs when axial insertion force is insufficient or the cross recess possesses excessive clearance. We solve this by (1) maintaining strict header punch lifecycle controls to keep recess geometry within micron-level tolerances; (2) recommending 6-lobe Torx (ISO 10664) or Torx Plus drives for torque-critical joints, which offer a 0-degree drive angle that removes the vertical ejection component entirely; and (3) supplying matched hardened drive bits and keys manufactured from high-grade alloy tool steel.
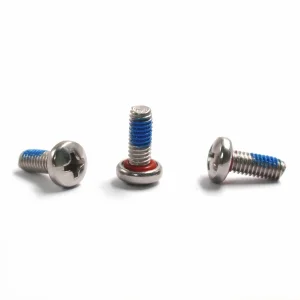
We provide three primary anti-loosening technologies: (1) Pre-Applied Nylon / Polyamide Patches: Applied 360° or 180° around the threads to provide continuous prevailing torque via interference fit; (2) SEMS Pre-Assembled Washers: Captive helical spring washers, external-tooth, or conical Belleville washers rolled onto the screw blank before threading to retain mechanical clamp force; and (3) Micro-Encapsulated Chemical Adhesives: Anaerobic adhesives that activate under shear pressure upon threading, delivering permanent thread-locking capabilities.
For standard corrosive environments, AISI 304 (A2-70) stainless steel with chemical passivation is specified. For salt-spray or chemically aggressive environments, marine-grade AISI 316 (A4-70/A4-80) stainless steel is utilized. For high-tensile carbon steel applications requiring extreme protection, we apply specialized multi-coat Zinc-Nickel (Zn-Ni) electroplating or non-electrolytic zinc flake coatings (such as Geomet or Dacromet), achieving in excess of 1,000 to 1,500 hours neutral salt spray (ASTM B117) exposure without red rust formation.
Every production batch includes complete quality documentation: Mill Test Certificates (chemical composition and tensile properties), Initial Sample Inspection Reports (ISIR / FAIR), Coating Thickness Measurement Reports (X-ray fluorescence), Salt Spray Test Verification, Hardness Test Results (HV/HRC), and RoHS/REACH compliance declarations. For automotive OEM clients, full Production Part Approval Process (PPAP) Level 3 packages are available upon request.