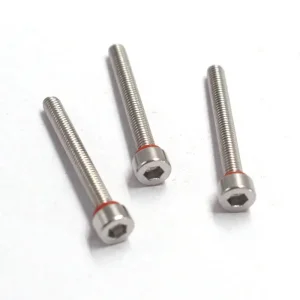
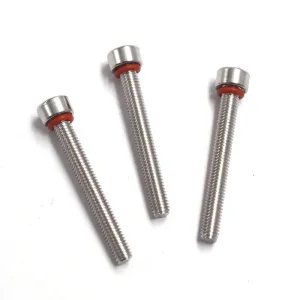
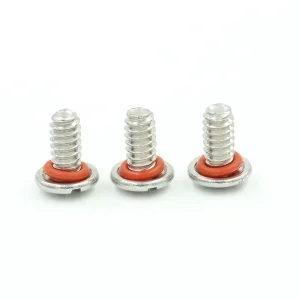
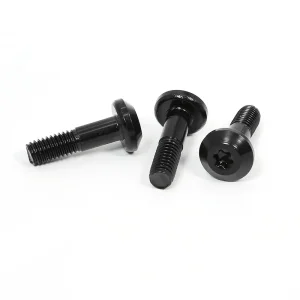
Explore standard, self-sealing, and anti-loosening thread-forming assemblies engineered with uniform micron-level zinc passivations for high mechanical pull-out strength.
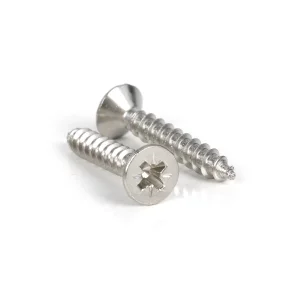
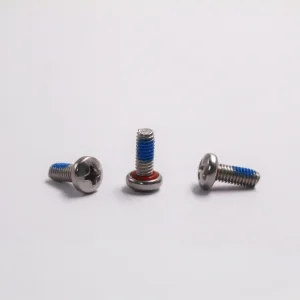



A technical deconstruction of case-hardening mechanics, thread-forming torque profiles, and corrosion barrier optimization for Tier-1 industrial applications.
Controlled carbonitriding in continuous mesh belt furnaces delivers a localized surface hardness of HV 450–750 while maintaining a ductile core (HV 270–390). This prevents premature shearing under excessive driving torque during tapping.
For high-tensile carbon steel tapping screws (tensile strength ≥ 1000 MPa), immediate thermal de-embrittlement baking is conducted at 200°C–220°C for 4 to 8 hours post-electroplating to eliminate interstitial hydrogen risks per ISO 15330 standards.
Hexavalent-free (Cr3+) electroplating incorporates clear, blue, or yellow passivation, augmented by inorganic nano-sealers. This composite layer provides sacrificial galvanic protection lasting from 72h to 1000h NSS without red rust.
Combining Dongguan's rapid precision tooling ecosystem with expansive high-volume cold-heading production lines across Shaoguan and Wuhan.
Our Dongguan technical center engineers proprietary tungsten carbide heading dies and thread-rolling blocks in-house, cutting custom drawing turnaround from 4 weeks to 7 business days.
Direct strategic supply partnerships with major domestic mills (e.g., Baosteel, Xingcheng Special Steel) guarantee heat-traceable 1018A, 1022A, 10B21, and SUS304/316 wire rod without supply volatility.
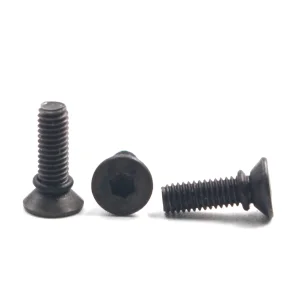
Equipped with 2-die 4-blow and multi-station forming machinery capable of holding complex undercut heads, captive washer assemblies, and precision Torx recesses to ISO 4759-1 Class A tolerances.
Every batch passes automated 360-degree high-speed optical inspection sorting tables verifying head diameter, recess depth, thread pitch integrity, and plating coverage at rates exceeding 800 pcs/min.
Comprehensive metallurgical, mechanical, and electroplating parameters supporting international OEM assembly standards.
| Parameter Category | Technical Baseline | Optional High-Performance Grades |
|---|---|---|
| Nominal Diameters | M1.2 – M8.0 (#0 to 5/16") | Micro-fasteners (sub-M1.0) and special multi-stage stepped shanks |
| Base Substrates | Low/Medium Carbon Steel (AISI 1018A, 1022A) | Boron Steel (10B21), Alloy Steel, Stainless Steel (SUS302, SUS304, SUS316) |
| Thread Profile Geometry | Type AB, Type B, DIN 7970, ISO 1478 Space Threads | 30° Flank Plastite/PT Profile, High-Low Thread, Trilobular Thread-Rolling |
| Zinc Coating Formulations | Cr3+ Blue/White Zinc (5–8 µm), Clear Passivation | Yellow Zinc Chromate, Black Zinc, Zinc-Nickel Alloy (12–15% Ni, 1000h NSS) |
| Mechanical Properties | Surface: min. 450 HV / Core: 270–390 HV | Through-hardened Grade 8.8 / 10.9 equivalents with pre-applied anaerobic adhesives |
| Compliance Clearances | RoHS 2.0 (2011/65/EU), REACH (EC 1907/2006) | ELV Directive (2000/53/EC), IMDS registration, conflict-free mineral verification |
Analyzing critical functional deployment zones where zinc-plated tapping screws reduce assembly stages and assure mechanical joint integrity.
Deployed within battery management enclosures (BMS), charging module heat-sinks, and interior chassis panels. Features non-conductive zinc under-head coatings and prevailing torque nylon micro-encapsulations to resist constant harmonic road vibrations.
Micro zinc-plated PT screws designed specifically for thin-walled thermoplastic casings (ABS, PC-ABS, Nylon 66). The reduced 30° flank angle alleviates internal boss hoop stress, eliminating casing cracking and optimizing stripping-to-driving torque ratios.
Heavy-duty self-drilling and thread-tapping assemblies for galvanized ducting, architectural facade brackets, and outdoor chassis. Incorporates elastomeric EPDM vulcanized sealing washers and 12-micron high-density zinc coatings to resist acid rain and condensation.
Addressing shifts in global inventory modeling, carbon transparency, and the replacement of secondary assembly steps.
Global manufacturing lines prioritize fasteners that form or cut clean internal threads in unthreaded extruded holes. This consolidation cuts cycle time, eliminates tap wear maintenance, and prevents chip contamination across electronic subsystems.
European and North American procurement teams enforce strict bans on hexavalent chromium and restricted phthalates. Direct factory documentation, including IMDS entry and XRF testing verification for each plating barrel, is now non-negotiable.
Multi-national enterprises demand consolidated supply from vendors operating redundant manufacturing sites. Our tripartite footprint (Dongguan, Shaoguan, Wuhan) guarantees dual-source risk mitigation against localized operational interruptions.
In-depth engineering answers covering thread geometries, plating thickness tests, and hydrogen embrittlement control protocols.
Engineered sealing hardware, DIN-standard sheet-metal fasteners, and custom mechanical retention assemblies for rigorous global installations.