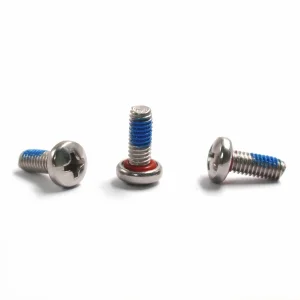
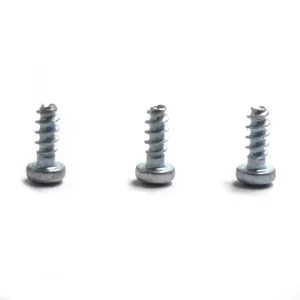
Explore standard, non-standard, and application-customized pan head, self-tapping, and machine threaded structural components manufactured under IATF 16949 quality protocols.
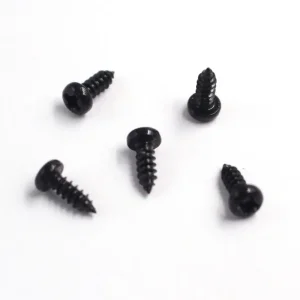
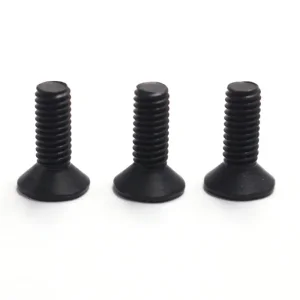


Transitioning from traditional mechanical joining to chip-free, thread-forming fasteners optimized for automated high-torque assembly lines.
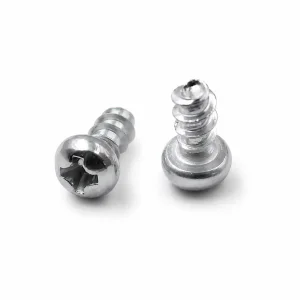
In modern industrial mechanical design, the stainless steel pan head self-tapper has evolved far beyond an ordinary threaded hardware part. In high-volume production environments across automotive electronics, marine computing, and green-energy infrastructure, the demand for eliminating pre-tapping operations has made the self-tapping fastener a cornerstone of structural engineering. Traditional assembly relied heavily on two distinct steps: tapping an internal female thread in a prepared pilot hole using machine taps, followed by driving a standard machine screw. This approach created substantial bottlenecks, chip contamination risks, and increased labor expenditures.
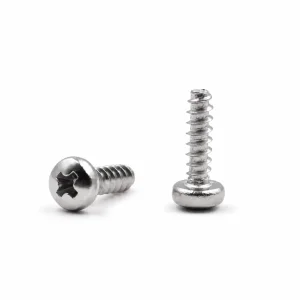
State-of-the-art cold-forged austenitic stainless steels (such as cold-work-hardened AISI 304/A2-70 and molybdenum-stabilized AISI 316/A4-80) now enable OEM self-tappers to displace mating material plastically rather than cutting it. The resulting cold-worked internal thread displays superior tensile retention and fatigue life because the grain flow of the host component is preserved intact. Furthermore, engineering the head style into an optimized pan head geometry balances high clamping surface distribution with a low profile, offering broad load bearing without cutting into sensitive lightweight plastic or sheet metal substrates.
Austenitic stainless steels cannot be hardened via standard quench-and-temper thermal methods. YH Fastener utilizes precision multi-station work-hardening during wire drawing and heading to achieve tensile strengths exceeding 700 to 800 MPa, delivering durable core ductility alongside rigorous thread performance.
Standard tapping screws (DIN 7981 / ISO 7049 Type C/F) are engineered for thin sheet metal, whereas trilobular cross-sections and 30° flank angle PT screws are designed specifically for engineering thermoplastics (e.g., PA66-GF30, PBT, Polycarbonate), minimizing radial hoop stress and preventing boss bursting.
The engineered pan head configuration delivers a broad bearing diameter ($d_k$) that distributes clamping force uniformly across enlarged through-holes. This mitigates surface embedding and prevents joint relaxation under cyclic temperature extremes and high dynamic vibration.
A persistent vulnerability of stainless steel self-tappers is friction-induced galling (cold welding) caused by micro-asperities tearing when high driving speeds interface with metal or composite pilot walls. YH Fastener incorporates dry-film synthetic micro-wax coatings, MoS2 anti-friction dispersions, or specialized passivation baths that reduce the dynamic coefficient of friction to $\mu = 0.08 - 0.14$. This ensures a broad process window between thread-forming torque ($T_{form}$) and torsional failure torque ($T_{fail}$).
How Chief Procurement Officers and Design Engineers evaluate Total Cost of Ownership (TCO), supplier manufacturing capability, and global trade compliance.
Enterprise procurement teams in North America, Europe, and the Asia-Pacific region no longer assess fastener purchases solely on unit price per thousand pieces. In continuous automated assembly lines running at hundreds of cycles per minute, a single defective fastener jamming a robotic screw feeder can incur thousands of dollars in line downtime. Consequently, top-tier buyers evaluate manufacturers based on comprehensive process stability and metallurgical traceability.
| Evaluation Parameter | Legacy Low-Cost Sourcing | YH Fastener Tier-1 OEM Protocol | Downstream Operational Value |
|---|---|---|---|
| Raw Material Provenance | Recycled, secondary melting wire without heat verification | 100% virgin austenitic coil with mill test certificates (EN 10204 3.1) | Eliminates internal voids, head snapping, and brittle fracture |
| Dimensional Dispersion | Manual vernier sampling; Cpk < 1.0 | Multi-gate CCD optical inspection; Process Cpk ≥ 1.67 | Guarantees 100% seamless feed in automated screwdriving bowls |
| Corrosion Resistance | Untreated or basic nitric acid rinse; rapid flash rusting | Controlled citric/nitric passivation; 1000+ hrs neutral salt spray (NSS) | Compliance with IP67/IP68 enclosures and extreme outdoor exposure |
| Quality Certification | Basic ISO 9001 baseline only | Automotive IATF 16949, ISO 14001, IMDS registered, PPAP Level 3 | Immediate qualification for automotive and high-reliability aerospace/EV |
| Drive Recess Accuracy | Shallow punch depth, fast bit slippage and recess wear | High-precision cold heading dies matching Torx/Phillips gauges exactly | Extends assembly driver bit lifespan by 400%, zero head reaming |
By eliminating manual hole tapping, cleaning, and broken tap extraction, YH pan head self-tappers reduce overall joint fabrication cost by 35% to 50% across large-scale industrial assembly programs.
With three major production hubs in Dongguan, Shaoguan, and Wuhan covering over 20,000 square meters, we mitigate geographic risks, providing dependable volume production and multi-plant backup capacity.
Full documentation packs including FMEA, Control Plans, Dimensional Results, Material Test Reports, and Gage R&R studies are provided to speed up OEM engineering sign-offs.
Addressing structural load bearing, environmental exposure, and vibration stability across specialized industrial sectors.
Lithium-ion battery enclosures require lightweight casing joints, high shock resistance, and anti-loosening safeguards. We supply PT thread self-tappers engineered with pre-applied nylon patches or under-head sealing washers to resist high road vibration and maintain IP67 battery compartment isolation.
Outdoor micro-base stations and PCB chassis demand uncompromised non-magnetic characteristics alongside atmospheric corrosion immunity. Austenitic 304/316 pan head self-tappers prevent eddy current losses while securing shielding gaskets against EMI/RFI interference.
Exposed to severe UV radiation, acid rain, and broad temperature swings (-40°C to +85°C), solar racking junction boxes rely on marine-grade AISI 316 pan head self-tappers paired with vulcanized EPDM bonded washers to block water ingress and maintain mechanical joint tension.
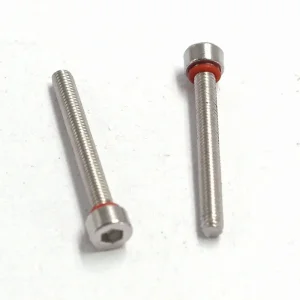
Direct contact between austenitic stainless steel fasteners ($E^\circ \approx -0.08\text{ V}$) and lightweight aluminum housings ($E^\circ \approx -0.75\text{ V}$) can induce galvanic corrosion in humid or coastal operating environments. YH Fastener provides specialized isolation barriers, including zinc-nickel hybrid platings, organo-mineral passivations, and integrated non-conductive elastomeric O-rings that prevent metal-to-metal galvanic coupling while preserving full mechanical torque transfer.
A look at the multi-stage quality control gates that keep defect escape rates below 50 PPM across millions of cold-headed fasteners.
Every incoming batch of wire rod undergoes X-ray fluorescence (XRF) spectrometry to verify critical elemental ratios (Chromium 18-20%, Nickel 8-10.5%, Molybdenum 2-3% for 316), alongside tensile yield tests prior to cold heading release.
Multi-station headers feature continuous acoustic sensors and micro-switches that identify tool chipping, punch misalignments, or concentricity runout during heading and thread rolling operations in real time.
Finished screws pass through rotary glass turntable optical sorters equipped with high-resolution telecentric lenses that measure head diameter, thread pitch, drive recess depth, and plating defects at rates up to 800 pcs/min.
| Standard Ref. | Head Style / Description | Drive Recess Options | Thread Type Specification | Common Industrial Use |
|---|---|---|---|---|
| DIN 7981 | Pan Head Tapping Screws | Cross Recess (Type H / Phillips) | Type C (Pointed) / Type F (Flat Point) | European machinery, control cabinets, white goods |
| ISO 7049 | Cross-recessed pan head tapping screws | Phillips / Pozidriv / Torx | Form A (Coned) / Form B (Flat end) | International industrial & automotive systems |
| ISO 14585 | Hexalobular socket pan head tapping screws | Torx (6-Lobe / Tamper-Resistant Pin) | Thread-forming Type C / Type F | Automated automotive robotic screwdriving |
| ASME B18.6.3 | Slotted & Recessed Pan Head Tapping | Type I (Phillips) / Type IA (Pozidriv) | Type AB (Fine Pitch) / Type B (Blunt) | North American HVAC, aerospace interiors & appliances |
| JIS B 1122 | Cross-recessed pan head tapping screws | JIS Cross Recess (Anti-Camout) | 1st / 2nd / 3rd Class Threads | Japanese consumer electronics, camera lenses, robotics |
Strategic engineering initiatives driving the next decade of structural connection performance across smart industrial ecosystems.
Adopting non-linear finite element modeling (DEFORM-3D) to predict grain flow during heading, preventing internal micro-cracks in high-strength austenitic stainless wire alloys.
Scaling precision heading capabilities down to M0.6 - M1.2 pan head micro self-tappers for augmented reality (AR) wearables, hearing instruments, and compact medical electronics.
Replacing conventional nitric baths with bio-based citric acid and closed-loop ultrasonic passivation, cutting wastewater output by 92% and achieving pristine cleanroom purity.
Integrating micro-etched 2D Data Matrix codes directly on pan head peripheries to enable individual fastener traceability across safety-critical automotive chassis assemblies.
In-depth responses to pilot hole sizing, material selection, galling prevention, and mechanical testing standards for fastener applications.
Austenitic stainless steels (AISI 304/A2 and AISI 316/A4) offer exceptional corrosion protection due to their high Chromium (18-20%) and Nickel (8-14%) content, with 316 containing 2-3% Molybdenum for resistance against chlorides and marine atmospheres. However, austenitic grades cannot be hardened through heat treatment; their strength comes purely from strain hardening during cold forging. In contrast, martensitic stainless steel (AISI 410) has lower chromium and negligible nickel, allowing it to be quenched and tempered to high hardness (HRC 38-45). 410 can tap into harder structural sheet steels, but provides markedly lower corrosion resistance compared to 304 and 316.
In thermoplastic boss designs, the nominal pilot hole diameter ($d_h$) is generally sized between 0.80 and 0.85 times the screw nominal outer diameter ($d$), dependent on the flexural modulus and ductility of the plastic:
$$d_h \approx (0.80 \sim 0.85) \times d$$
For filled, rigid materials like PA66-GF30, hole sizing leans toward the upper limit (0.85d) to avoid boss cracking from excessive hoop stress. For unfilled, ductile materials like ABS, Polypropylene, or PE, hole sizes closer to 0.78d-0.80d ensure higher thread engagement and pull-out resistance ($F_{pull-out}$). In all cases, the boss outer diameter should equal at least 2.0 to 2.5 times the screw diameter.
Phillips drives (ISO 7049 Type H) feature angled sidewalls originally designed to push the driver bit up and out (cam-out) at high torques to prevent over-tightening. In modern, precision torque-controlled electric screwdriving spindles, cam-out causes driver slippage, damaging screw plating, generating airborne metallic debris, and wearing driver bits prematurely. A Torx (ISO 10664) drive maintains vertical drive walls with a 15° engagement angle, transferring torque purely through radial drive surfaces rather than axial downward pressure. This provides zero cam-out, reduces operator fatigue, and extends driver bit service life up to 10-fold.
Galling occurs when friction breaks down the passive chromium-oxide surface film, resulting in localized friction welding under high contact pressure. Key countermeasures include: (1) Applying dry-to-the-touch fluoropolymer, wax, or MoS2 micro-coatings; (2) Maintaining controlled automated rundown speeds (under 400-600 RPM) to minimize interfacial heat build-up; (3) Utilizing trilobular thread-rolling geometries that form threads through intermittent contact peaks rather than continuous 360° circumferential friction.
Yes. Approximately 60% of our production volume comprises non-standard, custom-engineered components. We design and grind heading dies in-house to accommodate modified pan head diameters, ultra-low profile wafer heads, security drives (Torx pin, triangle, one-way), custom undercut sealing channels, and SEMS assemblies with pre-installed captive Belleville, wave, or rubber-backed sealing washers.
Every commercial export order includes an Inspection Certificate conforming to EN 10204 3.1. This details chemical composition via optical emission spectrometry, mechanical tensile and torsional strength, Vickers micro-hardness profiles, coating thickness (X-ray fluorescence), salt-fog corrosion test logs (ASTM B117), and dimensional inspection records. Full PPAP Level 3 documentation packages are readily provided for Tier-1 automotive and safety-critical industrial programs.
Precision-threaded, sealing, fine-pitch, and countersunk structural components manufactured to international industrial standards.