Explore engineered cold-headed components configured to withstand dynamic cyclic loads, chemical electrolytes, and severe outdoor atmospheric corrosion.
The global transition to zero-emission infrastructure imposes unprecedented mechanical and electrochemical requirements on joint fasteners. Yu-Huang delivers precision cold-headed hardware built to meet the rigorous failure-prevention metrics defined by international clean energy benchmarks.
Battery enclosures, busbar distribution plates, and inverter modules require micro-vibration resistance and non-magnetic, spark-resistant metallurgy.
Utility-scale photovoltaic farms face intense UV exposure, thermal cycling delamination, and corrosive C4/C5 marine environments.
Grid-scale Battery Energy Storage Systems and wind turbine nacelles demand hermetic ingress sealing and structural fatigue endurance.
Yu-Huang Electronics Dongguan Co., Ltd. combines advanced multi-station cold-forming automation with closed-loop process telemetry across a 20,000 m² footprint in Dongguan, Shaoguan, and Wuhan.
High-speed 5-die and 6-die heading machines shape intricate geometries from premium alloy wire without severing the internal grain microstructure, yielding superior tensile strength.
High-resolution CCD optical sorters run 360-degree telemetry on thread pitch, concentricity, head recess depth, and plating uniformity, keeping PPM defects near zero.
Direct supply contracts with top-tier steel mills provide complete metallurgical melt heats, chemical spectroscopy reports, and mechanical lot-level traceability.
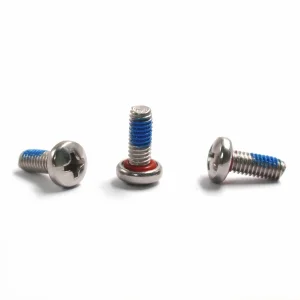
Integrated automated micro-encapsulation and nylon spray coating lines allow fine control over torque friction coefficients (µ 0.10 - 0.16) per ISO 16047.
Global procurement directors require absolute adherence to quality, delivery schedules, and audit accountability. Our quality management framework delivers full traceability from wire drawing to end-of-line verification.
Every batch follows strict APQP, FMEA, Control Plan, and MSA procedures. Complete Level 3 PPAP documentation—including IMDS material reporting, dimensional layout logs, and gage R&R calculations—is supplied with pre-production approval runs.
Our testing facility verifies clamp loads, tensile limits, micro-Vickers case depth, core hardness (HRC/HV), plating thickness via X-ray fluorescence, and hydrogen embrittlement relief bake verification per ISO 4042.
All finished coatings and raw alloys comply with EU Directives (RoHS 2011/65/EU and REACH (EC) 1907/2006). Chemical composition reports verify products remain free of SVHCs (Substances of Very High Concern) and responsibly sourced raw inputs.
As operating voltages in new energy equipment jump from 400V to 800V/1000V+ and battery power densities rise, fastening hardware must evolve beyond basic mechanical clamping.
Integrating micro-piezoelectric thin-film sensors and miniature RFID markers directly into fastener bolt heads enables real-time acoustic clamp-load telemetry across utility wind nacelles and automated battery exchange stations.
Aligning with Scope 3 carbon reduction metrics through scrap-fed Electric Arc Furnace (EAF) wire-rod alloys. We run dedicated low-carbon lines that maintain ASTM/DIN tensile and shear strength while minimizing embodied emissions.
Transitioning from standard electroplating to composite zinc-graphene and ceramic silane topcoats. These finishes deliver >3,000 hours of neutral salt spray protection while preserving Class 6g/6h thread clearances.
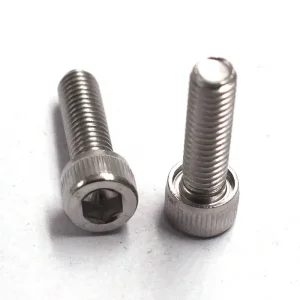
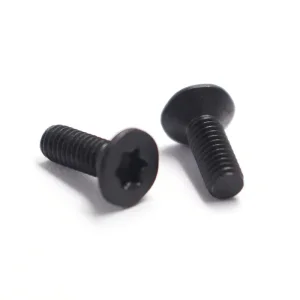
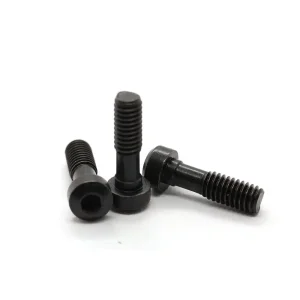
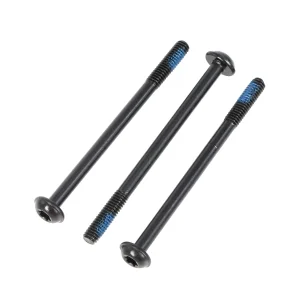
Browse our proven inventory of cold-headed and precision-turned screws engineered for electrical chassis, structural frameworks, and outdoor enclosures.
Key design considerations, material selection guidelines, and compliance requirements for renewable energy fastening hardware.