Engineered cold-headed and Swiss CNC-machined retention components manufactured to DIN, ISO, ANSI, and custom OEM drawings with strict 100% optical sorting.



A deep-dive technical analysis into captive fastener mechanics, retention geometry, and international regulatory directives governing mission-critical chassis designs.
In contemporary industrial equipment, telecommunications chassis, high-voltage battery enclosures, and aerospace avionics housings, enclosure captive screws represent an indispensable class of retention fasteners. Unlike standard machine fasteners that separate completely from the mating cover upon loosening, a captive screw remains permanently affixed to the primary panel or enclosure sheet metal even when fully disengaged from its mating tapped hole or threaded insert. This captive behavior eliminates lost hardware, accelerates field maintenance cycles, and crucially prevents foreign object debris (FOD) from falling into live electrical busses, rotating machinery, or dense printed circuit board assemblies.
The engineering topology of an enclosure captive screw centers around an undercut or reduced-diameter shank positioned between the threaded segment and the screw head or retained collar. Governed by international mechanical standards like DIN 7964 (wafer shank captive screws) or proprietary OEM spring-loaded press-fit designs, the screw diameter along this reduced neck ($d_3$) is intentionally turned or cold-headed down to slightly below the minor diameter of the external thread ($d_1$). When paired with a captive washer, a rolled sheet-metal flange, a swaged retention ferrule, or an internal retaining ring, the screw gains axial floating freedom while being physically barred from extracting through the panel mounting hole.
Loose fasteners falling onto energized DC busbars or high-density surface mount components can trigger cataclysmic short circuits, arc flash events, or mechanical jamming. Enclosure captive screws provide permanent mechanical capture, assuring 100% fail-safe compliance during field service operations.
Under the European Union Machinery Directive 2006/42/EC (Section 1.4.2.1) and EN ISO 14120, fixed guards and access panels required to be removed periodically for operational maintenance must remain attached to the guard or machinery chassis via permanent retention fastening systems.
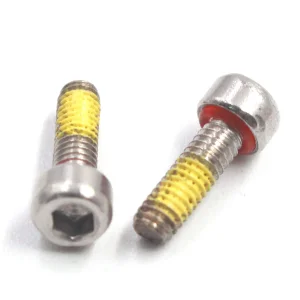
Harsh operating profiles in rolling stock (EN 61373), defense vehicles (MIL-STD-810G), and seismic-rated telecoms racks demand screws that will not back out under resonance. Captive spring mechanisms and pre-applied polyamide patches absorb extreme harmonic displacement.
When engineering multi-point captive screw arrangements on large sheet metal or die-cast aluminum doors, tolerance stack-up between mounting holes can cause thread binding. Specifying floating captive screw assemblies with 0.8mm to 1.5mm radial float prevents galling, compensates for thermal expansion differentials, and permits effortless hand-starting.
Harnessing the world's most concentrated precision tooling, cold-forming, and metallurgical finishing ecosystem across Yu-Huang Electronics' 20,000m² manufacturing infrastructure.
Founded on three decades of cold-heading research, precision tool & die making, and global OEM export experience.
Integrated manufacturing campuses situated across Dongguan headquarters, Shaoguan branch, and Wuhan branch.
Zero-defect optical sorting machines verifying thread pitch, shank runout, head height, and plating thickness.
Supplying Tier-1 electrical equipment builders across North America, Germany, Japan, Scandinavia, and APAC.
Global procurement directors increasingly choose Dongguan, China as the focal point for their precision hardware sourcing. The Greater Bay Area delivers an unparalleled cluster advantage: wire drawing mills, specialized cold-heading machinery builders, vacuum heat treatment providers, and automated trivalent passivation lines all reside within a 50-kilometer industrial radius. At Yu-Huang Electronics Dongguan Co., Ltd. (YH Fastener), we leverage this geographical supply chain velocity to compress design-to-prototype cycles from standard weeks down to mere days.
Our captive screw manufacturing lines combine multi-station cold-heading machines capable of producing the complex stepped-shank geometries of captive fasteners at speeds exceeding 120 parts per minute, integrated with secondary CNC Swiss-type automatic lathes for ultra-tight tolerance micro-finishing ($\pm 0.015\text{ mm}$). This hybrid approach allows us to deliver cold-formed high mechanical strength (achieved through continuous unbroken grain flow) combined with precision CNC ferrule retaining grooves and under-head O-ring sealing channels at a fraction of Western domestic production costs.
| Captive Screw Retention Architecture | Typical Fastener Materials | Mounting Method | IP Seal Rating Compatibility | Typical Industrial Enclosure Application |
|---|---|---|---|---|
| Spring-Loaded Retractable Assembly | SUS304 / 316 Screw, Aluminum Ferrule, Music Wire Spring | Press-Fit (Self-Clinching) or Flare-In | IP65 (with external wiper seal) | 19-inch Server Rack Drawers, Blade Servers, Telecom Modules |
| Wafer Reduced Shank (DIN 7964) | A2-70, A4-80 Stainless, Grade 8.8 / 10.9 Alloy Steel | Retaining Washer or Threaded Sheet Panel | IP67 / IP68 (with integrated under-head O-Ring) | Cast Aluminum Junction Boxes, NEMA 4X Enclosures, EV Inverters |
| Snap-In Plastic Grommet Style | Passivated Stainless Steel with Polyamide 66 Sleeve | Manual Toolless Snap-In into Punched Sheet | IP54 / Dust Resistant | Consumer Electronics, Vending Kiosks, White Goods Panels |
| Floating Self-Aligning Captive Screw | High-Tensile Carbon Steel (Zinc-Nickel Plated), Brass Bushing | Floating C-Clip or Swaged Panel Collar | IP66 (with dynamic silicone seal) | Railway Rolling Stock Doors, Mining Control Consoles, Seismic Cabinets |
Eliminating geopolitical supply friction through stringent material traceability, internationally accredited testing laboratories, and bilingual application engineering.
For Tier-1 automotive and industrial electrification customers, YH Fastener provides comprehensive Production Part Approval Process (PPAP) submission packages. Every mass-production run is validated through formal dimensional inspection reports, Material Test Reports (MTRs), Gage R&R studies, Failure Mode and Effects Analysis (FMEA), and Process Control Plans.
Global environmental safety is verified via third-party SGS/TUV batch testing. All trivalent passivated coatings ($Cr^{3+}$), zinc-nickel deposits, black oxide finishes, and stainless alloys are 100% compliant with EU RoHS Directive 2011/65/EU and REACH Regulation (EC 1907/2006). Automotive components are submitted directly to the International Material Data System (IMDS).
Our sales engineering team provides seamless CAD modeling reviews (STEP, IGES, DXF) with a guaranteed 24-hour turnaround on technical feasibility. Shipments are handled via bonded DDP air freight, consolidated sea freight, and regional consignment hubs across Europe and North America to shield clients from supply disruptions.
Strategic procurement evaluations must look beyond unit purchase cost ($C_{unit}$). In mission-critical enclosures, Total Fastener Cost is defined as: $TCO = C_{unit} + C_{install\_labor} + C_{loss\_scrap} + C_{field\_failure\_risk}$. Standard screws carry high lost-hardware downtime and assembly line drop rates (up to 4%), whereas pre-assembled enclosure captive screws slash assembly labor duration by 35% and completely eliminate catastrophic field warranty claims caused by loose parts.
From automated robotic assembly lines to IP68 waterproof battery modules, examine how custom captive screws address rigorous 21st-century mechanical environments.
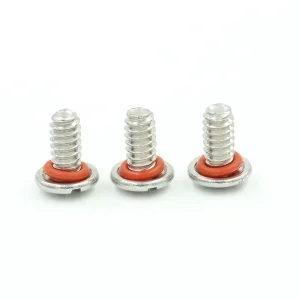
Remote radio units (RRU) and data center edge compute enclosures require rapid modular hot-swapping under severe weather. Our captive screws with Fluorosilicone O-rings deliver 1,000-hour salt-spray resistance while locking in IP68 submersion protection.
EV pack enclosures demand flame retardant (UL 94V-0) sealing combined with high thermal shock endurance. YH Fastener produces custom captive sealing bolts with captured EPDM/NBR washers capable of sealing pressurized cooling chambers against dielectric fluid leakage.
Aircraft cockpits and train signaling units are subject to continuous harmonic vibration. Our titanium and A286 superalloy spring-loaded captive screws comply with stringent weight-reduction quotas while guaranteeing captive security under 30G shock loads.
Medical centrifuges, MRI consoles, and diagnostic chambers require non-magnetic, corrosion-free Grade 316L stainless steel captive fasteners. Electropolished surfaces with blind head cavities prevent microbial entrapment and endure harsh autoclave sterilization washdowns.
As smart manufacturing sweeps through tier-1 OEM plants, assembly line automation is revolutionizing how captive screws are presented and seated. Traditional loose fasteners easily jam automated blow-feeder chutes. Next-generation enclosure captive screws are engineered with precision lead-in pilot points (dog points) and customized head flanges matched to automated vacuum pick-and-place magnetic robotic tooling. In parallel, automotive and defense applications are exploring micro-threaded captive fasteners with surface-laser-etched 2D Data Matrix codes for component lifecycle serialization, enabling 100% digital traceability from raw wire rod ingot to the disassembly of recycled electric vehicles.
Direct technical answers from YH Fastener application engineers regarding tolerances, retention mechanisms, custom tooling, and global supply logistics.
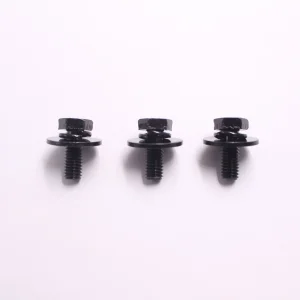
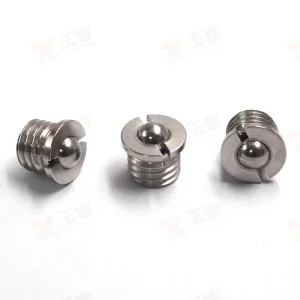
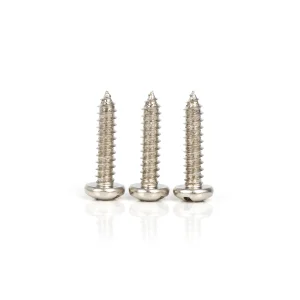
Complementary hardware solutions including sealing bolts, partial-thread frame screws, and precision spring-ball plungers for industrial equipment assembly.

Connect directly with Yu-Huang Electronics' chief mechanical engineers. Provide your 2D engineering drawings (PDF/DXF) or 3D STEP models, and receive a comprehensive DFM (Design for Manufacturability) review, material recommendation, and formal quotation within 24 hours.
