Explore our calibrated DIN standard & custom metric machine screws engineered for structural integrity, vibration dampening, and hermetic sealing across high-stress assemblies.

Class 8.8/10.9 high-tensile steel coarse thread designed for rigorous structural industrial framing.
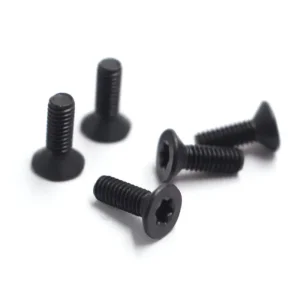
Austenitic 304/A2 stainless steel countersunk fasteners optimized for flush electronics assembly.

Anti-rust precision engineered self-tapping screw for sheet metal, ductile plastics, and composites.
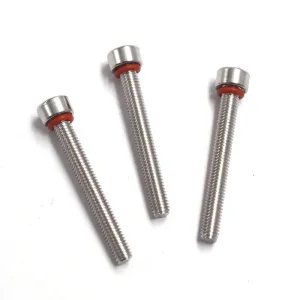
Under-head silicone/Viton elastomeric seal for marine electronics and rugged telecommunication boxes.
Black oxide treated headless set fasteners with precision cross drives for concealed precision assemblies.
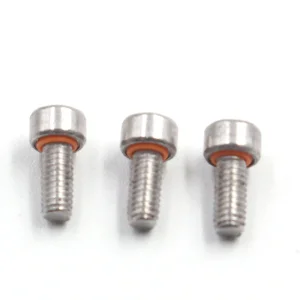
Engineered for high-torque new energy battery enclosures requiring hermetic isolation against moisture.

Dual-performance design combining dynamic vibration anti-loosening threading with dynamic O-ring seals.
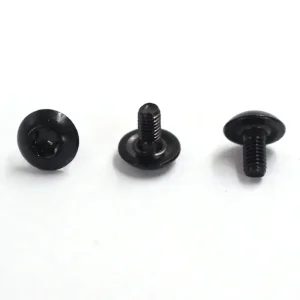
Multi-drive internal socket and Phillips combination bolts offering exceptional clamp preload uniformity.
An engineering evaluation of metric standardization, dimensional conformance under DIN/ISO norms, and how structural micro-fasteners determine operational lifespan in automated ecosystems.
The modern industrial landscape relies entirely on deterministic mechanical parameters. DIN (Deutsches Institut für Normung) standards—such as DIN 7985, DIN 965, DIN 912, and DIN 84—serve as the foundation for interchangeability across automated manufacturing plants worldwide. While ISO standards provide global guidelines, legacy DIN specifications continue to dominate capital-intensive industries in DAX-region equipment, robotics arms, and high-frequency vibratory machinery. A metric machine screw is not merely a passive fastener; it serves as a dynamically calculated tension element that balances axial preload against shear force fatigue.
High-speed automated assembly lines operate at feed rates where single-digit PPM (Parts Per Million) failure thresholds are strictly non-negotiable. Substandard drive recess depth, slight head eccentricity, or burrs in coarse/fine metric threading cause immediate pneumatic robotic feed line jams, resulting in production stoppage costs. As an OEM DIN machine screw manufacturer, Yu-Huang Fasteners enforces 100% optical sorting and tight concentricity controls, ensuring that high-throughput pneumatic feeding arms seat every fastener safely to target torque limits without stripping.
The risk of hydrogen embrittlement in electroplated high-tensile machine screws (Grade 8.8, 10.9, 12.9) represents one of the largest failure vectors in mission-critical enclosures. We apply thermal de-embrittlement baking at 200°C–230°C within 4 hours of electroplating, alongside automated passivation baths for austenitic grades (AISI 304/A2-70, AISI 316/A4-80). This safeguards dynamic micro-fasteners against sudden, delayed intergranular cracking caused by residual mechanical stresses and diffused hydrogen ions.
How custom engineered DIN metric fasteners are deployed within demanding physical sectors, maintaining structural stability under extreme environmental conditions.
Automotive battery enclosures, power electronics converters, and high-voltage busbars require IP67/IP68 sealing machine screws combined with pre-applied non-conductive or nylon locking patches (DIN 267-28) to resist road-vibration harmonics and thermal cycles.
Robotic joints and servo-actuator housings demand Torx (six-lobe) pan head DIN 7985 fasteners with precision rolled micro-threads down to M1.2. The high surface contact area eliminates cam-out and ensures consistent, long-term clamp preload retention.
Outdoor 5G base stations and marine radar housings use 316 A4-80 stainless machine screws paired with fluorosilicone O-rings. These resist salt-spray corrosion (tested over 1,000 hours per ASTM B117) and galvanic reactions against aluminum castings.
Precision surgical instruments and smart home wearables require DIN 965 flat countersunk heads with tamper-resistant triangular or pin-in-Torx drives, maintaining flush industrial surfaces, clean cleanroom finishes, and strict anti-tamper security.
Cross-reference table: Mapping common DIN machine screw designations to international equivalents, functional tolerances, and typical torque ranges.
| DIN Standard | ISO Equivalent | Head Geometry | Drive Recess | Standard Diameters | Tensile Property Classes |
|---|---|---|---|---|---|
| DIN 7985 | ISO 7045 | Pan Head (Raised Cheese) | Cross (Phillips / Pozidriv) / Torx | M1.6 – M10 | 4.8, 8.8, SS A2-70, SS A4-80 |
| DIN 965 | ISO 7046 | Countersunk (Flat) Head | Phillips / Slotted / Six-Lobe | M1.4 – M10 | 4.8, 8.8, 10.9, SS A2-70 |
| DIN 912 | ISO 4762 | Cylindrical Socket Head | Hexagon Socket (Allen) | M1.4 – M36 | 8.8, 10.9, 12.9, SS A2/A4 |
| DIN 84 | ISO 1207 | Cheese Head (Slotted) | Linear Slotted Drive | M1.0 – M10 | 4.8, SS A2-50, Brass (CuZn) |
| DIN 7991 | ISO 10642 | Countersunk Socket Head | Hexagon Socket | M3 – M20 | 8.8, 10.9, 12.9, Stainless Steel |
| DIN 933 | ISO 4017 | Hexagon Head (Full Thread) | External Hex Flange / Socket | M3 – M64 | 5.6, 8.8, 10.9, SS 304 / 316 |
How our 20,000 m² multi-site footprint in Dongguan, Shaoguan, and Wuhan mitigates global logistical risks and scales delivery cycles for tier-level manufacturers.
Unlike assemblers relying on fragmented third-party subcontractors, YH Fastener completes wire drawing, spheroidized annealing, cold heading, thread rolling, heat treatment, patch dispensing, and optical packaging entirely within controlled facilities. This direct control eliminates multi-tier logistical delays and keeps standard custom runs within 15–20 days.
Our quality lab utilizes Mitutoyo 2.5D optical measuring projectors, Vickers micro-hardness testers, Fischer X-ray fluorescence plating thickness analyzers, and automated torque dynamometers. Full SPC statistical process tracking ensures our custom DIN machine screws meet strict automotive CPK > 1.67 criteria.
Operating plants in both coastal Guangdong (Dongguan, Shaoguan) and central transportation hubs (Wuhan) gives our production network balanced supply resilience. Buyers maintain uninterrupted delivery schedules across volatile sea freight and raw-wire commodity markets through dynamic manufacturing allocation.
How Yu-Huang Fasteners approaches advanced metallurgy, digital traceability, and sustainable surface chemistry for the upcoming industrial generation.
Transitioning toward hexavalent-chromium-free zinc-nickel (Zn-Ni) and eco-friendly mechanical geodur/geomet coatings. These thin films (<8µm) survive 1,500+ hour neutral salt spray tests while preserving precision metric thread tolerances without retapping.
To support miniaturized edge-computing and optical transceiver modules, our cold-forming lines now process ultra-micro machine screws down to M0.6–M1.0, preserving precise drive geometry and preventing head shearing under micro-servomotor torques.
We are establishing digitized batch genealogies spanning raw wire heat numbers through automated heading, heat treatment profiles, and sorting logs. This architecture will support full, instant 3.1 material test certificate verifications across customer ERP networks.
Comprehensive testing protocols, environmental certifications, and technical support frameworks backing our international supply operations.
All manufactured machine screws fully satisfy European Directive 2011/65/EU (RoHS 3) and Regulation (EC) No 1907/2006 (REACH SVHC). Chemical declarations and test reports are kept current with biannual SGS laboratory validations.
For Tier-1 automotive and aerospace subcontractors, we prepare standard Production Part Approval Process (PPAP Level 3) packages, including Process FMEA, Control Plans, Dimensional Measurement Results, and material certifications.
Our bilingual senior application engineers review 2D/3D CAD files (STEP, IGES, DWG) within 24 hours, advising on cold-heading manufacturability, draft angles, and raw material optimization to reduce tooling costs.
Insights into cold heading parameters, torque calculations, plating coatings, and custom production timelines.
While both reference pan head cross-recessed machine screws, subtle differences exist in head radius curvature, head diameter tolerances, and recess engagement depths. DIN 7985 specifies slightly higher head height allowances in specific small metric sizes (such as M2.5 and M3), whereas ISO 7045 standardizes dimensions internationally to align with ISO metric driver bit depths. Our manufacturing plant provides certified tooling for both standards depending on drawing callouts.
Cold heading reshapes raw wire rod plastically at room temperature, preserving continuous material grain flow along the screw profile. This yields significantly higher shear strength, fatigue life, and tensile capacity compared to cut-thread CNC machining. Moreover, cold heading operates at production speeds up to 150–350 pieces per minute with near-zero material scrap, significantly lowering unit costs for mid-to-high volume OEM programs.
To eliminate hydrogen embrittlement risks, all high-tensile components (hardness exceeding 320 HV / 32 HRC) are transferred to de-embrittlement baking ovens within a strict 4-hour window following electroplating. Parts undergo thermal treatment at 200°C–230°C for 4 to 8 hours to allow atomic hydrogen to diffuse harmlessly out of the steel crystal matrix.
We work with Austenitic Stainless Steels (AISI 304, AISI 316, 316L), Martensitic Stainless Steels (410, 430), Brass (CuZn37, CuZn39), Phosphor Bronze, Titanium alloys (Ti Gr2, Gr5), and specialized aluminum grades (Al 6061, 7075). For extreme marine duty, we offer SS316 fasteners passivated per ASTM A967 with optional fluoropolymer coatings.
Custom cold heading tooling, punch dies, and thread-rolling dies are fabricated in-house within 7 to 10 working days. First-article inspection samples along with full dimensional reports are typically shipped within 12 to 15 days, followed by mass production runs upon drawing sign-off.
Explore additional specialized cold-headed fasteners from our manufacturing floor, engineered for high preloads and hermetic isolation.
Designed for thin-walled plastic enclosures and precision telecommunications brackets.
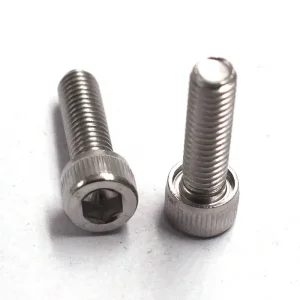
Austenitic stainless steel hex socket bolts providing high tensile clamp force in machine frames.

Features an integrated groove containing an elastomeric ring for dynamic fluid sealing.

Precision-rolled machine threads engineered for consistent sealing in cast electrical housings.
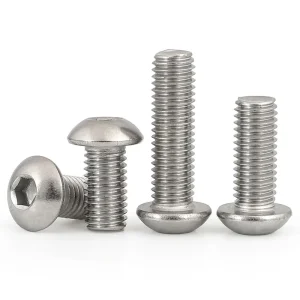
Wide-flange truss geometry spreads clamping pressure across sheet steel structures.
Color-coded grounding fastener with captive serrated washer for positive electrical earth bonding.
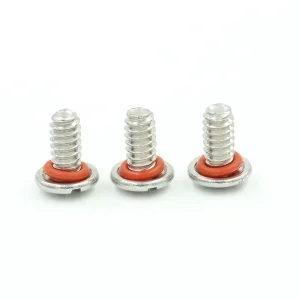
Class 10.9 heat-treated carbon steel sealing screw for automotive battery pack perimeter sealing.
Corrosion-proof, self-sealing fastener engineered for solar inverter cabinets and wind nacelles.
