Cold-headed metric and customized self-tapping architectures offering superior pull-out strength, zero tapping swarf, and enhanced anti-loosening torque resistance.



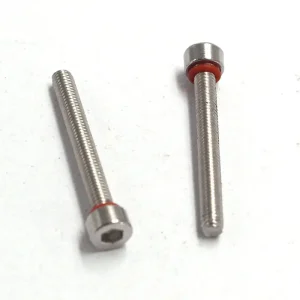
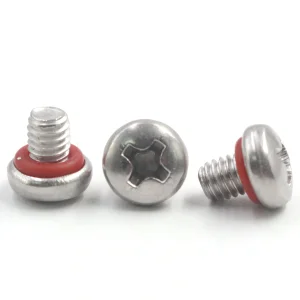
Addressing the fundamental tribological challenge of stainless steel galling, work hardening, and localized ductility during rapid automated installation.
Traditional machined screws sever grain lines, introducing micro-fissures. Our multi-station progressive cold-heading forces austenitic wire grain to flow continuously around the head contour, boosting fatigue resistance by up to 34% in SUS304 and molybdenum-fortified SUS316.
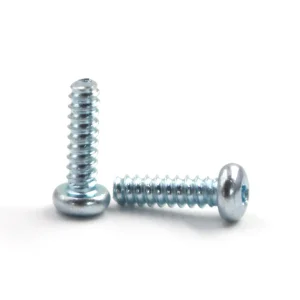
Self-tapping fasteners are structurally divided into Trilobular™ thread-forming geometry and fluted thread-cutting screws. In ductile thermoplastics and extruded aluminum sheets, our trilobular flank design eliminates tapping chips while compressing structural grain to prevent micro-cracking.
Austenitic stainless steels are naturally prone to friction galling (cold welding) at drive speeds over 400 RPM. We incorporate dry-film solid lubricants, micro-encapsulated fluoropolymers, and specialized organic sealants to regulate friction coefficients between 0.10 and 0.15.
From electric mobility drive systems to hermetic surgical instrumentation, our engineered fasteners resolve critical mechanical fastening constraints.
Electric vehicle (EV) battery module casings and inverter busbars require non-magnetic fasteners resistant to galvanic corrosion when joined with lightweight 6000-series aluminum chassis.
Micro-sized self-tapping screws ranging from M0.8 to M2.0 designed specifically for glass-filled liquid crystal polymers (LCP), PEEK, and polycarbonates in wearables and medical sensors.
Automated articulating robotic arms require continuous high-speed cycloidal torque transmission under dynamic vibration, where screw loosening induces catastrophic calibration drop.
Pole-mounted 5G massive MIMO antennas and centralized photovoltaic string inverters face heavy acid-rain, UV radiation, and severe ambient thermal oscillations (-40°C to +85°C).
Anticipating the downstream assembly demands of 2026–2030 through ongoing material innovation, nano-coatings, and sensorized fastening ecosystems.
| R&D Vector | Current Baseline (Standard) | YH Fastener Advanced Tier (2025–2026) | Next-Gen Horizon (2027+) | Engineering Benefit |
|---|---|---|---|---|
| Alloy Metallurgy | Standard Austenitic SUS304 / SUS316 Wire | Precipitation-hardened 17-4PH & Lean Duplex 2205 | Custom High-Entropy Nitrogen-Strengthened Alloys | Yield strength exceeding 1100 MPa while maintaining austenitic non-magnetic permeability (µr < 1.01). |
| Thread Profile Synthesis | Standard ISO Type AB & Type B Thread Geometry | Asymmetric Variable Pitch (30°/60° Dual Flank) | AI-Computed Biomorphic Load-Distribution Flutes | Triples pull-out load in low-density engineering plastics with 50% reduced radial crack risk. |
| Surface Functionalization | Standard Chemical Passivation (ASTM A967) | Plasma Assisted Chemical Vapor Deposition (DLC Coating) | Self-Lubricating Graphene-Matrix Nanocomposite Film | Eliminates galling without liquid oils; survives 3,000+ hours neutral salt spray testing. |
| Assembly Verification | Static Torque Wrenches / Optical Sorting | Angle-Monitored Automated Electric Drivers | Fasteners with Laser-Etched 2D DPM Data Matrix QR Codes | Individual lot traceability back to wire ingot melt batch, supporting critical aerospace/medical audits. |
Yu-Huang Electronics Dongguan Co., Ltd. operates a synchronized production triangle across Dongguan, Shaoguan, and Wuhan spanning over 20,000 m².
Equipped with 1-die-2-blow and ultra-precise 4-die-4-blow multistation cold formers from Taiwan and Japan. Capable of producing up to 350 fasteners per minute per machine with continuous shank concentricity monitoring.
Every critical batch destined for high-volume automated assembly lines undergoes glass-dial optical inspection checking head diameter, recess drive depth, thread flank integrity, and foreign object presence at sub-50 PPM defect rates.
Dispersed production across South and Central China insulates tier-one supply chains from localized power grid curtailments, regional freight delays, or raw material spikes through centralized ERP raw wire buffer reserves.
Navigating complex international regulatory frameworks with fully auditable documentation packages provided alongside every production release.
For OEM automotive customers, we provide comprehensive Production Part Approval Process (PPAP) Level 3 packages including Design FMEA, Process FMEA, Control Plans, Gage R&R studies, and Full Dimensional Measurement Reports.
All raw wire rod (austenitic, martensitic, ferritic) and plating treatments are tested via ICP-OES spectroscopy to ensure complete absence of SVHC (Substances of Very High Concern), Hexavalent Chromium (Cr⁶⁺), Lead, Cadmium, and Mercury.
Eliminate third-party inspection lag. Our internal mechanical testing department validates fasteners in accordance with ISO 898-1, ASTM F593, and DIN EN ISO 3506 specifications before container sealing.
Answers to common mechanical, metallurgical, and procurement questions encountered during DFM reviews and volume purchase transitions.
High-torque drive designs, ultra-thin profiles, custom multi-material joinery, and corrosion-resistant fasteners engineered for specialized OEM requirements.


Send your 2D engineering drawings (PDF, DWG, DXF) or 3D CAD step files. Our applications team confirms thread engagement ratios, head feasibility, and quotes volume tier pricing within 24 hours.
