Explore our certified cold-formed, thread-rolled stainless steel fasteners, waterproof self-sealing screws, and prevailing-torque locking assemblies.
Strategic perspectives on metallurgical selection, joint mechanics, micro-fastening trends, and automated assembly economics.
The global industrial fasteners market is projected to surpass $120 Billion by 2030, driven by the massive electrification of automotive architectures, industrial IoT automation, and clean-tech renewable installations. Pan head machine screws remain one of the most widely specified geometries across precision mechanical bills of materials.
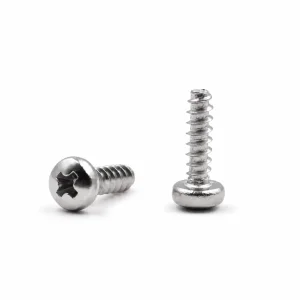
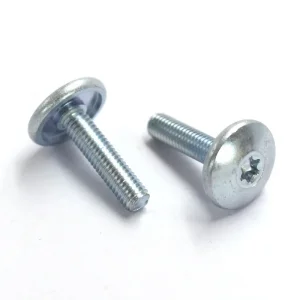
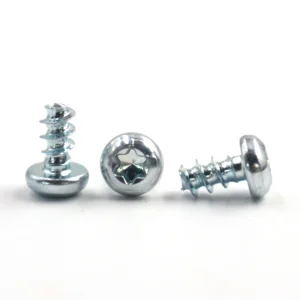
Pan head fasteners feature a wide, slightly rounded surface profile with high vertical edges. This geometric design delivers a superior bearing surface area, distributing clamping preload evenly across fragile housing materials (die-cast aluminum, magnesium alloys, polycarbonates) without causing surface countersink stress fractures.
Specifying 304 (18-8, A2-70) vs 316 (A4-80) stainless steel balances corrosion resistance, yield strength, and cold-heading ductility. Grade 316 provides critical resistance to pitting in chloride-dense marine and medical chemical sterilization environments, supported by continuous ultrasonic passivation.
| Alloy Grade | Tensile Strength (MPa) | Yield Strength (0.2% MPa) | Passivation Standard | Primary Industrial Use-Cases |
|---|---|---|---|---|
| AISI 304 / A2-70 | 700 min. | 450 min. | ASTM A967 Nitric 2 | Automotive sensors, control panels, computing, white goods |
| AISI 316 / A4-80 | 800 min. | 600 min. | ASTM A380 Citric IV | Marine hardware, chemical metering pumps, medical diagnostic gear |
| AISI 410 Hardened | 850 min. | 650 min. | AMS 2700 Method 1 | High-hardness self-drilling machine joints, industrial HVAC |
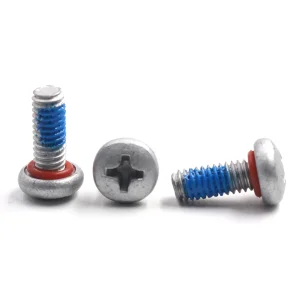
| 304 with Blue Patch | 700 min. | 450 min. | IFI-124 / DIN 267-28 | High-vibration drivetrain housings, robotic end-effectors, e-mobility |
Combining vertically integrated cold-heading ecosystems, automated tooling agility, and strict IATF 16949 automotive quality gates.
Our rapid-prototyping toolshop in Dongguan designs and discharges tungsten carbide cold-heading dies and thread-rolling blocks in as little as 3-5 working days. This rapid turnaround cuts standard design cycles by up to 60% compared to Western manufacturing hubs, supporting agile hardware engineering teams.
Zero-defect commitments are maintained via multi-camera automated laser-vision inspection machines. Every batch of pan head screws is checked for thread pitch integrity, head eccentricity, recess depth, and plating defects at rates exceeding 800 parts per minute, ensuring down-to-50-PPM quality delivery.
Situated within the Greater Bay Area hardware cluster, our manufacturing base leverages direct procurement of high-purity Japanese and domestic wire rod, localized vacuum heat-treatment kilns, and state-of-the-art non-electrolytic passivating facilities within a 30-mile operational radius.
From hermetically sealed electronics enclosures to automotive radar sensors and automated robotic grippers.
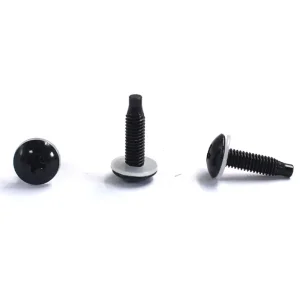
LiDAR, camera housings, and battery management (BMS) busbar enclosures demand non-magnetic 304/316 stainless pan head fasteners fitted with captive silicone O-rings to deliver long-term IP67 ingress protection against road grime and salt-spray corrosion.
Fluid handling cassettes and clinical point-of-care analyzers rely on precision-ground M1.6–M3 pan head machine screws with clean chemical passivations, resisting aggressive enzymatic cleaners and preventing thread galling during regular autoclave cycles.
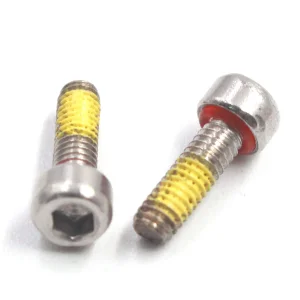
Rackmount cloud computing enclosures, switches, and edge computing units require anti-vibration pan head fasteners with micro-encapsulated polyamide thread-locking patches, preventing loosening from continuous high-frequency cooling fan harmonics.
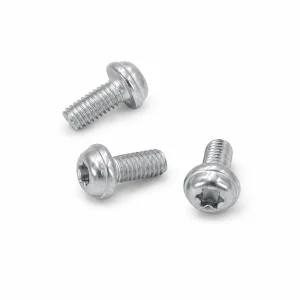
Compact high-torque servo drives and SCARA articulation segments use custom Torx and tamper-resistant security pan head screws, delivering high torsional installation drive efficiency without cam-out damage on fast automated assembly lines.
How automation, decarbonization, and smart assembly are reshaping industrial procurement requirements worldwide.
Global assembly lines are rapidly transitioning from legacy Phillips and slotted drives to Torx (6-lobe) and Torx Plus systems. These profiles deliver near-zero radial stress and zero cam-out, eliminating airborne particulate generation in cleanroom assembly settings and extending automated driver bit lifespans by up to 400%.
Manual thread-locking fluid dispensing is being phased out in modern manufacturing. OEM engineers increasingly require fasteners delivered with microencapsulated anaerobic pre-coatings (e.g., DIN 267-27) or reusable 360-degree polyamide patches, ensuring calibrated breakaway torque without messy on-line chemical handling.
Tier-1 procurement mandates comprehensive pedigree tracking. From raw material melt heats to cold-heading tonnage profiles and optical sorting verification, digital mill certificates (EN 10204 3.1) and Full PPAP Level 3 documentation are now standard requirements for mission-critical assemblies.
Technical guidance from senior application engineers on metallurgy, galling prevention, tolerance controls, and supply chain execution.
A pan head machine screw features a flat bearing surface with slightly chamfered or rounded outer vertical sides. Unlike a countersunk flat head, it sits entirely above the mating surface. Compared to a rounded or button head, the pan head delivers a significantly broader bearing surface contact area. This reduces localized compressive stress, making it the preferred choice for clamping plastics, thin-gage sheet metals, and composite enclosures without surface deformation.
Austenitic stainless steels (304, 316) have a natural tendency to gall when torqued at high speeds under load. Our manufacturing facility counters this by: (1) maintaining thread pitch tolerances to 6g/6h standards, (2) applying micro-thin dry-to-touch wax/lubricant coatings (e.g., molybdenum disulfide, PTFE, or synthetic waxes), and (3) recommending matched thread engagement speeds and calibrated torque drivers during customer assembly operations.
Yes. Our in-house engineering group specializes in custom ODM/OEM solutions. We regularly manufacture custom screws from CAD prints (STEP, DWG, PDF) incorporating captive shoulder steps, dog points, pilot tips, self-tapping PT threads for thermoplastics, special under-head sealing grooves for O-rings, and proprietary tamper-proof security drives.
Operating under ISO 9001, ISO 14001, and IATF 16949 accreditations, we provide Full Material Mill Test Certificates (EN 10204 3.1), salt-spray corrosion test logs (ASTM B117), dimensional measurement reports via Keyence optical systems, torque/tensile failure reports, and full automotive PPAP Level 3 documentation packages upon request.
For standard catalog configurations, MOQs start from 10,000–50,000 units depending on thread diameter. For custom drawing-based ODM orders requiring dedicated cold-heading tooling, pilot tooling samples are typically dispatched in 7–10 days, with full-scale production runs completed in 15–20 working days. Blanket order stocking agreements (JIT/Kanban) are also supported for global assembly operations.
Specialized non-standard screws, high-torque industrial fasteners, thread-forming fasteners, and IP67 sealing fasteners.