
Engineered cold-formed fasteners integrated with high-performance elastomer seals, captive configurations, and precision thread geometries for mission-critical joints.



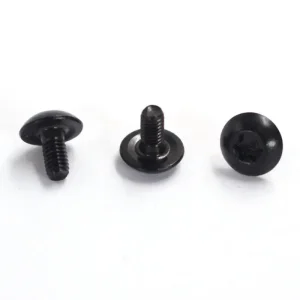
A systematic technical review of how structural sealing fasteners evolved from conventional flat gasket assemblies to precision cold-headed cap screws with integrated undercut O-rings.
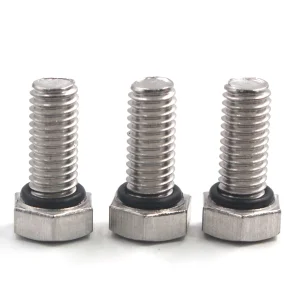
Traditional industrial sealing relied heavily on external cut washers or liquid anaerobic threadlockers. Under extreme thermal expansion, cyclical shock, and internal gas pressures, chemical sealants experience creeping and washer assemblies suffer asymmetric cold deformation. The modern ODM O-ring cap screw integrates a precisely machined or cold-rolled annular undercut groove immediately below the fastener head. This design restricts rubber volumetric swelling, achieving hermetic IP67/IP68 isolation with metal-to-metal contact.
The acceleration of automotive electrification, remote IoT telemetry nodes, and subsea renewable robotics has exposed standard hardware to aggressive operating environments. Global engineering teams specify custom O-ring cap screws manufactured from Austenitic Stainless Steel (SUS304, SUS316) or high-tensile Alloy Steel paired with Fluorocarbon (FKM), Nitrile (NBR), or Medical-Grade Silicone rings capable of sustaining pressure thresholds up to 6,000 PSI (413 bar) across temperatures ranging from -60°C to +200°C.
Modern automated pick-and-place lines and robotic multi-spindle screwdriving equipment leave zero tolerance for dimensional variation, head eccentricities, or damaged O-rings. Tier-1 automotive and consumer electronic OEMs demand 100% optical sorting, stringent CpK ≥ 1.67 process capabilities, and full lot traceability directly from the wire rod mill down to the elastomer vulcanization lot.
Leveraging deep industrial cluster integration, vertically controlled cold heading, and in-line automated sealing insertion to deliver agility, scale, and cost optimization.
By conducting raw material spheroidized annealing, wire drawing, multi-station cold heading, CNC thread rolling, specialized undercut forming, and automated O-ring pre-assembly in-house across Dongguan, Shaoguan, and Wuhan facilities, we eliminate third-party logistics latency and guarantee rigorous quality control across every production gate.
Custom undercut profiles require precise tooling radii to avoid stress concentrations in cold-forged stainless steel or high-tensile carbon steel. Our tool-and-die department manufactures custom carbide dies in-house, compressing initial prototyping cycles from the industry-standard 4–6 weeks down to just 7–10 days.
Operating under certified IATF 16949, ISO 9001, and ISO 14001 quality management frameworks, every production lot is issued full material certification (EN 10204 3.1), RoHS and REACH declarations, IMDS reporting, and multi-axis optical dimension validation reports.
Real-world engineering environments where custom O-ring cap screws provide mechanical clamping, environmental sealing, and vibration resistance.
Lithium-ion power modules and high-voltage power conversion inverters require IP67/IP69K sealing to prevent moisture ingress, internal thermal runaway, and catastrophic electrical flashover. O-ring cap screws maintain pre-load clamping under prolonged chassis harmonic vibration while preventing electrolyte vapor escape.
Subsea instrumentation, naval sensors, and autonomous marine drones face continuous hyperbaric water pressure and aggressive chloride salt attack. Marine screws feature undercut pan or socket cap geometries that mechanically compress a silicone or fluorosilicone O-ring against die-cast aluminium or composite housings.
Unmanned aerial vehicles (UAVs) and aircraft avionic pods operate across extreme atmospheric pressure gradients. Sealing screws prevent internal cabin decompression or optical fogging caused by rapid condensation during climb and descent cycles, maintaining zero leakage across wide thermal swings.
A technical guide for design engineers on groove geometry, elastomer squeeze ratios, and clamping mechanics.
| Thread Diameters & Pitch | Metric: M1.4 through M16 (Coarse & Fine Pitch). Imperial: #0-80 UNF to 5/8"-11 UNC. Precision rolled threads conforming to ISO 965 / ASME B1.1. |
|---|---|
| Undercut Groove Geometry | Engineered dovetail, semi-circular, or stepped rectangular undercut designed with calculated clearance volume to allow 25%–35% elastomer compression without ring extrusion. |
| Base Fastener Materials | Stainless Steel (AISI 302, 304, 316, 410); Carbon Steel (Class 4.8, 8.8, 10.9, 12.9); Brass (C3604); Aerospace Titanium (Grade 5 / Ti-6Al-4V); Monel 400. |
| Elastomer Ring Formulations | Nitrile (Buna-N / NBR); Fluorocarbon (FKM / Viton®); Silicone (VMQ - FDA / USP Class VI); Ethylene Propylene (EPDM); Fluorosilicone (FVMQ); Neoprene (CR). |
| Recess & Head Styles | Head Styles: Pan Head, Socket Cap, Flanged Hex, Truss, Flat Countersunk (with custom counterbore collar). Recesses: Hex Socket, Torx (6-Lobe), Security Tamper-Proof Pin-in-Torx, Phillips. |
| Plating & Surface Treatments | Electro-Zinc (Clear, Yellow, Black); Eco-friendly Trivalent Zinc-Nickel; Electroless Nickel; Black Oxide; Chemical Passivation (ASTM A967); Dacromet / Geomet anti-corrosion coatings. |
| Quality & Testing Protocols | Helium mass-spectrometry vacuum leak testing, hydrostatic pressure burst testing, salt spray chamber testing (ASTM B117), optical vision sorters (PPM < 20), optical profile projectors. |
Strategic purchasing insights, technical shifts toward automated assembly, and modern supplier qualification benchmarks.
Manual assembly of loose O-rings onto miniature screws on factory floors introduces high labor costs, inconsistent seating, ring twisting, and part damage. Tier-1 multinational procurement teams have shifted to factory-assembled O-ring screws. Integrated cap screws arrive pre-fitted and seated, ready for automatic blow-feed assembly screwdrivers, cutting assembly line cycle times by up to 40%.
Semiconductor fabrication fixtures, cleanroom automation, and hermetic camera sensor packaging demand sealing hardware with minimal volatile organic compounds. Global procurement teams require low-outgassing silicone and medical-grade fluoropolymer O-rings certified to ASTM E595, cleanroom degreased fasteners, and particle-free vacuum packaging.
International buyers seek stable Chinese manufacturing partners with mature multi-factory footprints that mitigate localized supply shocks. Partnering with suppliers operating manufacturing facilities across Dongguan, Shaoguan, and Wuhan provides the dual security of continuous scale production and reliable export delivery routes.
Technical guidance compiled by our application engineers addressing joint dynamics, tolerances, and custom ODM manufacturing.
Explore additional cold-forged screws, specialized sealing hardware, and custom thread-forming solutions designed for automated robotic assembly lines.

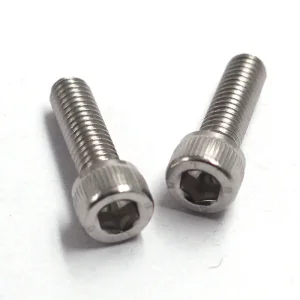

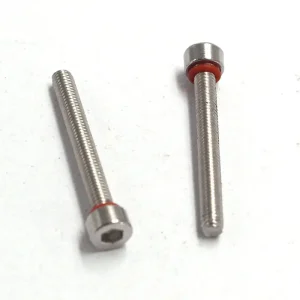
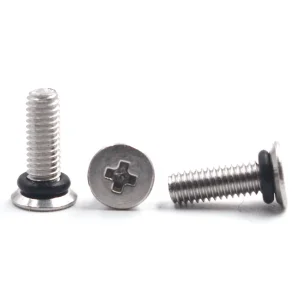
Send your 2D engineering drawings or 3D CAD files. Our senior fastener application engineers provide complete Design for Manufacturability (DFM) reviews, torque-tension calculations, and sample lead times within 24 hours.