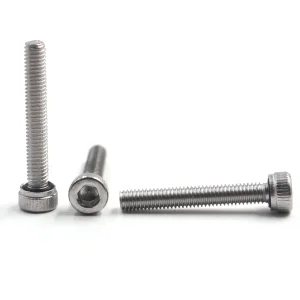
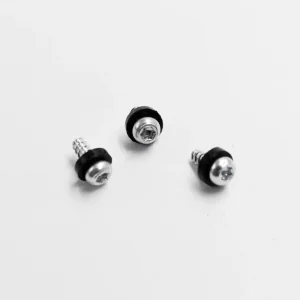
Engineered cold-formed fasteners featuring precision under-head O-ring seating, specialized thread geometry, and advanced anti-corrosion barrier coatings.
From passive mechanical clamping to multifunctional hermetic sealing: Analyzing macro shifts across electric mobility, industrial IoT, outdoor microelectronics, and harsh-environment architectures.
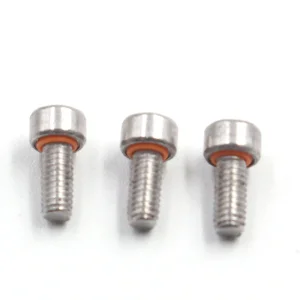
Modern electrical enclosures in automotive powertrain controllers, battery management systems (BMS), and aerospace sensors undergo rapid temperature swings from -40°C to +150°C. Standard elastomeric perimeter gaskets frequently suffer micro-channel leak paths due to uneven joint deflection. Integrated under-head sealing screws isolate every fastener penetration point, ensuring continuous hermetic sealing to IP68 and ISO 20653 IP69K ratings even under aggressive thermal expansion differentials.
Traditional flat washers deform unevenly under clamp load, causing elastomer squish, tear, or compression set over operational lifetimes. Modern ODM cold-heading engineering integrates a precision-machined or cold-formed annular groove beneath the screw head. This recess maintains controlled 25%–30% elastomer volumetric compression, preventing radial over-squeeze while facilitating metal-to-metal contact to establish stable tightening torque and clamp force retention.
With smart cities, surveillance optics, wearable diagnostics, and edge-computing nodes shrinking internal footprints, fasteners must scale down to micro-diameters (M1.0, M1.2, M1.6, M2.0) without sacrificing mechanical tensile yield or ingress barrier integrity. Yu-Huang utilizes progressive multi-station cold heading and optical sorting to hold concentricity tolerances within ±0.03 mm for miniature silicone, fluorosilicone, and Viton O-ring integrations.
Tier-1 procurement teams and mechanical hardware leads enforce stringent QA verification pipelines before qualifying waterproof mechanical housing fasteners.
Automotive electronics and mission-critical hardware demand comprehensive Advanced Product Quality Planning (APQP). We provide full Production Part Approval Process (PPAP) Level 3 documentation, including DFMEA/PFMEA, Control Plans, Process Capability Studies (Cpk ≥ 1.67), Gage R&R, Material Test Reports (MTR), and ballooned dimensional inspection prints.
Procuring separate loose O-rings and screws results in line assembly errors, missed seals, rolled rings, and doubled handling labor. Pre-assembled, captive-bonded, or undercut-trapped sealing screws eliminate field leaks, slash line takt times by up to 40%, and streamline procurement Bills of Materials (BOM) into a single traceable SKU.
For automated feeder bowl presentation, head burrs, thread nicks, or off-center O-rings trigger costly automated screwdriving line shutdowns. Yu-Huang deploys high-speed 360-degree glass plate automated optical sorting machines (AOI), inspecting thread profile, pitch diameter, recess depth, plating thickness, and seal positioning down to <20 PPM defect rates.
Global supply chain volatility requires redundant manufacturing resilience. Across our 20,000 m² production footprint spanning Dongguan, Shaoguan, and Wuhan facilities, we house redundant multi-station heading machines, thread rollers, continuous heat-treatment furnaces, and proprietary O-ring assembly cells to guarantee uninterrupted global deliveries.
Solving complex challenges in galvanic corrosion, torque-tension consistency, and polymer aging across harsh industrial, marine, and outdoor environments.
| Engineering Challenge | Underlying Failure Mechanism | Yu-Huang ODM Fastener Architecture | Target Standard / Compliance |
|---|---|---|---|
| Galvanic Corrosion in Aluminum & Magnesium Enclosures | Stainless steel fasteners (SUS304/316) in contact with die-cast aluminum (ADC12, A380) or magnesium (AZ91D) create an electrochemical galvanic couple, causing catastrophic galvanic pitting in humid or coastal environments. | Engineered inorganic non-electrolytic zinc-flake coatings (Geomet, Dacromet), high-adhesion fluoropolymer barriers, or electroplated zinc-nickel (12%–16% Ni) providing galvanic voltage isolation and eliminating dissimilar metal corrosion. | ASTM B117 (≥1500h NSS without red rust) ISO 10683 / DIN 50021 |
| Radial O-Ring Extrusion & Torque Loss | Conventional flat-bottom screws pinch elastomeric washers outward upon reaching final torque, leading to torn seals, variable clamp preload, and loss of hermetic containment over vibration cycles. | Precision cold-formed under-head annular undercut (trapped pocket design). Ensures metal-to-metal seating contact to carry clamp load while trapping the elastomer within a 90%–95% contained gland volume. | IP67 / IP68 (1.5m, 24h submersion) ISO 20653 IP69K dynamic spray |
| Vibrational Loosening in Heavy Machinery & EV | Transverse cyclic vibration induces microscopic slip on thread flanks, eroding thread friction and resulting in screw back-out and joint separation. | Integration of pre-applied micro-encapsulated chemical threadlockers (DIN 267-27, Precote, Loctite) or high-resilience 360°/180° polyamide (nylon) patches (DIN 267-28), establishing reusable prevailing locking torque. | DIN 65151 Junkers Vibration Test ISO 2320 Prevailing Torque |
| Thermoplastic Boss Cracking in Molded Enclosures | Standard machine threads or aggressive self-tapping profiles exert excessive radial hoop stress during thread formation, inducing micro-cracks and boss ruptures in ABS, Polycarbonate, or PBT. | Optimized 30° / 45° flank angle PT / TP thread-forming profiles. Reduced radial stress vectors combined with deep thread engagement provide high stripping torque, low driving torque, and crack-free installation. | VDI 2230 Systematic Calculation UL 94-V0 Flammability Enclosures |
We match the under-head sealing compound to the application environment: NBR (Buna-N) for standard oils and water (-30°C to +100°C); EPDM for ozone, steam, and outdoor weatherability (-40°C to +135°C); FKM (Viton) for aggressive fuels, acids, and elevated temperatures (-20°C to +200°C); and Fluorosilicone (FVMQ) for low-temperature military and aerospace avionics down to -60°C.
By forming the screw head, drive recess, and under-head seal groove via multi-station progressive cold heading rather than CNC material removal, the internal metal grain structure flows uninterrupted along the external geometry. This increases shear fatigue endurance by 25%–35%, prevents stress concentrations at the head-to-shank fillet, and guarantees dimensional stability across million-part runs.
Fastener clamp load consistency hinges on a tightly calibrated coefficient of friction (μ = 0.10–0.15). We apply integrated topcoats containing dry micro-lubricants, ensuring automated screwdrivers achieve repeatable clamping force without over-torquing the O-ring or under-clamping the mechanical gasket.
Comprehensive regulatory verification, material traceability, and tailored logistics frameworks serving engineering teams across North America, Europe, and Asia-Pacific.
All raw wire rod, elastomer vulcanizates, and electroplated finishes are 100% compliant with EU RoHS Directive 2011/65/EU and 2015/863, REACH Regulation (EC) No 1907/2006 (SVHC list), California Proposition 65, and Dodd-Frank Section 1502 Conflict Minerals reporting. Certified third-party SGS/TÜV test documentation is cataloged per manufacturing lot.
To eliminate production downtime for contract manufacturers (EMS), we establish customized inventory buffer programs, Kanban pull systems, and bonded warehouse fulfillment across key logistical hubs in the United States, Germany, Japan, and Southeast Asia, guaranteeing rapid dock-to-stock replenishment.
Our senior application engineering team reviews custom 2D drawings (DWG, DXF, PDF) and 3D CAD models (STEP, IGES) with complete DFM (Design for Manufacturability) feasibility reports within 24 hours. From rapid tool prototyping to full cold-heading sample delivery in 10–14 days, we accelerate your NPI cycle.
Pioneering innovations in liquid silicone direct over-molding, smart RFID asset tracking, and micro-scale ultra-deep waterproof architecture.
Transcending conventional loose or mechanically trapped O-rings, our next-generation manufacturing utilizes multi-cavity injection tooling to directly chemical-bond Liquid Silicone Rubber (LSR) onto the cold-headed screw undercut. This creates an unseparable, flash-free, molecularly bonded sealing gasket that cannot be lost or misaligned during high-speed robotic assembly.
For critical infrastructure such as offshore wind nacelle enclosures, high-speed rail junction housings, and utility energy storage containers, Yu-Huang is prototyping integrated micro-passive RFID sensors into the fastener head. Technicians can scan the joint to instantly verify part pedigree, torque history, batch provenance, and maintenance intervals without disassembling sealed housings.
As smart AR glasses, wearable biosensors, and submersible micro-cameras proliferate, conventional sealing screws reach their dimensional limits. Our advanced micro-cold-heading technology enables sub-millimeter (M0.8 to M1.4) sealing screws featuring micro-groove geometries capable of withstanding 5 ATM (50m depth) immersion pressures while maintaining total serviceability.
In-depth technical answers addressing fastener design parameters, O-ring groove engineering, and environmental testing protocols.
Explore our extended series of cold-headed industrial screws, anti-tamper Torx fasteners, flush-mount hardware, and positioning plungers.