Engineered for direct-feed automated tooling, precision electrical grounding, and multi-metal structural joints. Explore our factory-direct cold-headed hardware solutions.


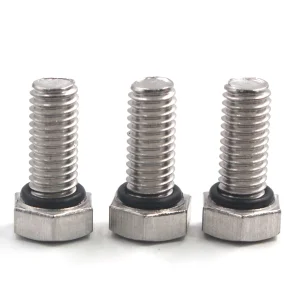

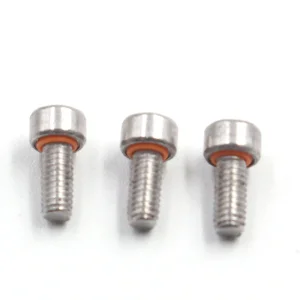
Why modern automotive platforms, tier-1 industrial electronics, and renewable energy arrays are transitioning entirely from loose multi-piece fastener assemblies to integrated SEMS architectures.
Procurement calculations based solely on unit purchase price miss 70% of downstream assembly overhead. When operators handle loose flat washers, Belleville discs, or helical spring washers separately, robotic feeder jams surge by up to 22%, and manual assembly takt times balloon. Hex Flange SEMS screws eliminate discrete SKU handling, reduce stock-keeping units in ERP systems, and prevent operator fatigue errors on multi-station assembly lines.
In electric vehicle battery modules and high-voltage junction systems, an uninstalled lock washer leads directly to micro-arcing, clamp load dissipation under thermal cycling, or catastrophic loose-part electrical shorts. SEMS engineering involves captive washer placement prior to thread roll forming. Once rolled, the thread crest major diameter physically prevents washer disengagement, guaranteeing absolute joint compliance in mission-critical applications.
Modern Industry 4.0 factories utilize continuous automated bowl feeders and high-speed multi-axis robotic screwdriving spindles. Hex flange geometry provides superior surface drive engagement compared to internal drive heads alone, eliminating cam-out failure, extending drive-bit life by up to 300%, and enabling exact torque-angle rundown monitoring in ISO/TS regulated production environments.
YH Fastener provides full-spectrum custom engineering across metric (M2 to M16) and unified (UNC/UNF #4 to 5/8") fastener profiles, optimizing grain flow metallurgy through high-speed multi-station progressive headers.
| Dimensional Parameter | Standard Range & Custom Tolerances | Material & Metallurgical Choices | Engineering Function & Application Benefits |
|---|---|---|---|
| Head Design & Flange Geometry | Indented Hex, Hex Washer, Hex Flange Serrated, Hex with Cross/Torx recess. Outer Flange Ø from 4.5mm to 32.0mm. Concentricity within ±0.05mm. | 1018, 1022A, 10B21, SCM435, Stainless SUS304, SUS316, A2-70, A4-80. | Spreads clamp load across thin sheet metal, aluminum housings, and plastic frames; prevents embedment into delicate substrates. |
| Captive Washer Combinations | Belleville Conical Springs, Split Helical Spring Lock, Curved Wave Washers, External/Internal Tooth Serrated, Heavy DIN 6902 / DIN 6903 Flat Washers. | Spring Steel 65Mn, 50CrV4, Phosphor Bronze, SUS301, 304 Hardened. | Maintains residual preload under severe thermal vibration; teeth pierce non-conductive anodized coatings to guarantee continuous ground bonding. |
| Thread Profile Options | Standard Metric Coarse/Fine (ISO 965-2 6g), Trilobular Thread Forming (PT / Taptite compatible), Thread Cutting, Hi-Lo Thread for Plastics. | Case Hardened Core: 28-38 HRC, Surface: 450-750 HV0.3; Class 8.8, 10.9, 12.9 properties. | Direct driving into pre-drilled or cored holes without pre-tapping; lowers insertion torque while maximizing strip-out and pull-out resistance. |
| Advanced Surface Passivations | Micro-layer thickness: 5µm to 15µm. Controlled friction coefficient (μ = 0.12 - 0.18) via integrated torque-tension topcoats. | Zinc-Nickel (12-15% Ni), Geomet / Magni / Dacromet Zinc Flake, Trivalent Clear/Black/Yellow Cr3+, Electroless Nickel, EPDM Sealing bonded. | Zero risk of hydrogen embrittlement via controlled 8-hour de-embrittlement baking at 200°C; provides up to 2,000 hrs ASTM B117 neutral salt spray resistance. |
How tier-1 engineering teams specify hex flange SEMS screws across demanding high-stress industries to maintain joint integrity under severe vibration and dynamic loading.
New Energy Vehicles experience intense cyclic shock along axes X, Y, and Z. Our indented hex flange screws with pre-assembled high-deflection Belleville conical washers deliver continuous axial compensation as copper and aluminum busbars expand and contract under high charge currents (150A to 600A), preventing catastrophic thermal runaway caused by loose electrical resistance joints.
Precision six-axis articulated arms and automated pick-and-place gantry systems produce dynamic centrifugal shear forces. SCM435 alloy Grade 10.9 hex flange SEMS with captured double-serrated tooth washers bite mechanically into mating steel castings, passing continuous 3,000-hour Junker transverse vibration testing (DIN 65151) without thread loosening or loss of initial clamp tension.
Deployed in coastal solar farms and desert micro-grids, outdoor electrical enclosures demand dual-action defense: IP68 hermetic ingress protection and ISO 12944 C5-M extreme marine corrosion endurance. We supply hex flange SEMS integrated with bonded vulcanized EPDM stainless steel washers that create an impervious fluid barrier against torrential moisture, salt fog, and sand ingress.
How Yu-Huang Electronics (YH Fastener) harnesses the world's most concentrated precision hardware ecosystem to outpace Western lead times by 65% while providing unparalleled cost efficiency.
Direct strategic contracts with domestic top-tier steel mills (Xingcheng Special Steel, Baosteel) guarantee immediate supply of cold-drawn, spheroidized-annealed alloy wire rods with pristine grain boundaries and certified chemical heats.
Our dedicated CNC wire-cutting, slow-feeding EDM, and tungsten carbide die grinding workshop reduces custom tooling lead times from the industry-average 35 days down to just 7 to 10 working days for rapid prototyping validation.
Multiple high-speed glass plate 360-degree vision sorting machines inspect 100% of finished lots at 800 pcs/min. Every screw is checked for thread pitch, recess depth, washer retention, and surface chips to achieve zero-defect delivery.
With our main manufacturing headquarters in Dongguan (20,000 m²) backed by sister plants in Shaoguan and Wuhan, YH Fastener guarantees continuous production continuity, immune to local grid fluctuations or logistical bottlenecks.
How YH Fastener R&D is evolving hardware interfaces to meet future demands for weight reduction, autonomous assembly feedback, and ultra-high tensile performance.
Replacing conventional multi-layer electroplating with ultra-thin (3-6µm) zinc-nickel ceramic composite matrices. These next-generation coatings deliver extraordinary cathodic protection exceeding 3,000 salt-spray hours without generating micro-cracking during thread deformation, while eliminating conductive interference in sensitive electronics.
To optimize cycle times for autonomous factory floor robots, our future hex flange SEMS configurations integrate MAThread® style elliptical clearing points and steep feeder lead-in chamfers. This virtually eliminates cross-threading errors, even when automated pneumatic spindles engage the fastener at up to 7 degrees of angular misalignment.
Pioneering induction-hardened boron steels that achieve ultimate tensile strengths exceeding 1,220 MPa with elongation parameters > 9%. Coupled with clean vacuum heat treatment processes, our high-strength SEMS bolts eliminate internal atomic hydrogen mobility, ensuring absolute safety in extreme structural chassis joints.
Ensuring friction-free integration across Tier-1 automotive and global OEM supply chains with uncompromising quality documentation and cross-border engineering support.
Every custom hex flange SEMS project is supported by complete AIAG-compliant Production Part Approval Process (PPAP Level 3) dossiers, including Process Flow Charts, PFMEA, Dimensional Results (ballooned drawings), Material Mill Certifications, Salt Spray Tests, and direct Material Data System (IMDS) registration numbers.
All electroplating, chemical passivation, and thread-locking compounds are strictly certified by third-party testing labs (SGS / TUV) to be compliant with EU RoHS Directive 2011/65/EU (and amendment 2015/863) and free of Substances of Very High Concern (SVHC) under EU REACH Regulation (EC) No 1907/2006.
We provide Vendor-Managed Inventory (VMI) frameworks, safety consignment stocking, and customized barcoded kanban packaging for OEM plants across North America, Europe, and Southeast Asia, guaranteeing continuous 48-hour replenishment to prevent line-down emergencies.
Broadening your bill-of-materials procurement with direct manufacturing integration. High-precision thumbscrews, countersunk heads, mechanical spring detents, and sealing fasteners.


Answers to critical questions regarding metallurgy, torque-tension calculation, washer captive dynamics, and custom tooling parameters.
The captive assembly is formed through a strictly staged cold-forming sequence: the blank screw shank is cold-headed with an unthreaded cylinder that features an outside diameter precisely matched to the thread pitch diameter (d2). The pre-punched washer (with an inner diameter slightly larger than the blank shank diameter but smaller than the eventual thread major diameter) is automatically seated against the under-head flange. When the part passes through the thread rolling dies, material displacement pushes the thread crests outward to the full major diameter (d). Because this rolled crest diameter exceeds the inner hole diameter of the washer, the washer is permanently captured, rotating freely without binding while remaining entirely captive.
A standard hex flange screw has an integral, rigid flange forged as a solid part of the head during heading. While it expands bearing surface area, it lacks axial flexibility. A Hex Flange SEMS screw incorporates both the solid forged upper flange AND one or more separate, captured dynamic spring elements (such as a Belleville spring washer, wave washer, or tooth-lock ring). This dual action provides both broad load distribution across delicate surfaces and dynamic elasticity to compensate for plastic creep, paint settling, and extreme thermal contraction.
Tightening torque (T) is governed by the Kellermann-Klein or VDI 2230 formula: T = F_M × [0.159 × P + 0.578 × d2 × μ_th + 0.5 × D_b × μ_b]. In SEMS assemblies, the effective under-head friction diameter (D_b) changes because contact occurs between the washer underside and the joint interface, while secondary friction occurs between the screw flange and washer face. To eliminate torque-tension uncertainty, our plating lines integrate friction-modifying topcoats (such as Gleitmo or Torque'N'Tension) calibrated to achieve a narrow overall friction coefficient (μ_tot) of 0.12 to 0.18, minimizing clamp force scatter during automated rundown.
Hydrogen embrittlement (HE) is a major catastrophic hazard for fasteners treated above 320 HV / 1000 MPa tensile strength when exposed to atomic hydrogen during acid pickling and electroplating. We eliminate this through three layers of defense: 1) Non-acid mechanical grit blasting or dry cleaning prior to plating; 2) Mandatory post-plating hydrogen baking at 200°C ± 5°C for 8 to 14 hours within 4 hours of electrodeposition; and 3) Utilization of non-electrolytic zinc flake coatings (such as Geomet, Dacromet, or Delta-Protekt) that are completely free of hydrogen generation during bath immersion.
For custom designs requiring bespoke tooling (special washer profiles, non-standard flange widths, or unique driver broaching), tooling fabrication takes 7 to 10 working days. First Article Inspection (FAI) samples with comprehensive CMM dimensional measurement reports are completed within 3 to 5 days following tooling qualification. Full mass production runs generally ship within 20 to 25 working days, with expedited 14-day production tracks available for critical automotive ramp-ups.
Send our senior engineering department your 2D CAD prints (PDF/DWG) or 3D models (STEP/IGES). Receive a complete manufacturability review, tolerance optimization assessment, and factory-direct commercial quotation within 24 hours.
