Explore our flagship OEM/ODM industrial fasteners developed for zero-defect automation lines. Built to withstand multi-axis dynamic shear, extreme temperature shifts, and aggressive galvanic environments.

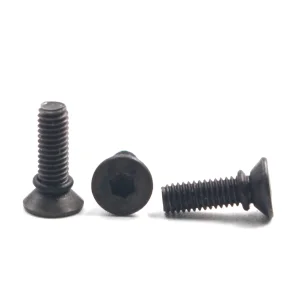
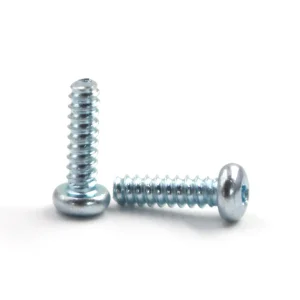
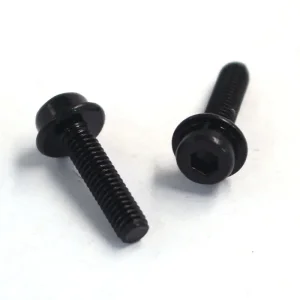
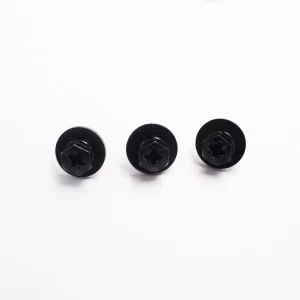

At Yu-Huang Electronics (YH Fastener), our 30-year evolutionary track record spans a 20,000 m² modern infrastructure anchored across primary high-precision cold-heading clusters in Dongguan, Shaoguan, and Wuhan. By consolidating wire spheroidizing annealing, multi-die cold extrusion, precision thread profile rolling, atmosphere-controlled case hardening, and optical inspection under one roof, we eliminate intermediate subcontracting bottlenecks and secure total trace-level metallurgical control.
Multi-station cold headers operate at tolerances within ±0.015 mm. Unlike turned or cut fasteners, unbroken grain lines follow the external contour of the head-to-shank transition, bolstering fatigue endurance and tensile load ratings by up to 28% under cyclic mechanical stress.
Proprietary rolling dies form standard DIN 7500, ISO 14585, and specialized 30° flank PT threads without cutting parent fiber structures. Surface finish drops below Ra 0.4 µm, drastically suppressing driving torque requirements while elevating ultimate strip-out thresholds.
High-speed rotary glass plate vision machines inspect 1,200 fasteners/min using multi-angle telecentric lenses. Critical parameters—including thread pitch, flank angle, head concentricity, recess depth, and plating continuity—are verified before automated packaging.
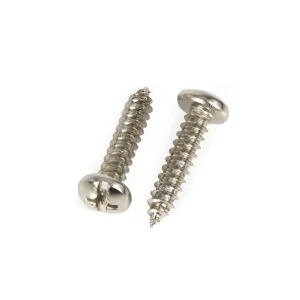
Specifying a self tapping screw requires understanding joint mechanics, material plasticity, insertion torque ($T_{drive}$), and strip-out torque ($T_{strip}$). For automotive-grade robotic assembly, achieving an engineering ratio of $T_{strip} / T_{drive} \ge 3:1$ is paramount to prevent thread stripping and assembly line stoppages.
High-tensile carbon steel self-tapping screws (Class 8.8, 9.8, 10.9) subjected to acid pickling and electro-galvanization require mandatory post-plating heat treatment. YH Fastener strictly executes thermal de-embrittlement baking at 200°C–220°C for 4 to 8 continuous hours within two hours of electroplating, satisfying automotive ASTM F1941 and ISO 15330 stress durability standards.
| Thread Architecture | Optimal Substrate | Flank Angle & Geometry | Drive-to-Strip Torque Ratio | Vibration & Loosening Immunity |
|---|---|---|---|---|
| PT Thread Forming (Trilobular) | Thermoplastics (ABS, PC, PA66-GF30, PBT) | 30° Sharp Flank Angle | > 3.8 : 1 (Max Safety Margin) | High radial springback friction prevents back-out without inserts |
| Type F & DIN 7500 Thread Rolling | Die-cast Zinc, Magnesium, Cast Aluminum | 60° Flank with Trilobe Cross-Section | > 3.2 : 1 (Controlled Flow) | Eliminates chip debris; zero risk of short-circuits in electronics |
| Type AB / B Thread Cutting | Sheet Metal (< 2.5 mm), Plywood, Resins | Gimlet / Blunt Tapered Entry | > 2.5 : 1 (Standard Fit) | Moderate; recommended with locking serrations or patch |
| Pre-Applied Microencapsulated Nylon Patch | High-Vibration Metal Enclosures & Powertrain | Metric Machine Thread (DIN/ISO Standard) | N/A (Prevailing Torque Spec) | Maintains clamping preload under severe DIN 65151 Junkers test cycles |
| Captive Sealing Head (O-Ring / Silicone) | Waterproof IP67/IP68 Electronic Housings | Undercut Head with Integrated Elastomer | > 3.0 : 1 with Controlled Torque Stop | Hermetic liquid/gas isolation with zero seal extrusion under torque |
To prevent hoop stress cracking and premature weld-line failure in glass-filled polymers, boss outside diameter ($D_B$) should equal $2.0 \times d_1$ (nominal screw diameter), with pilot hole diameter ($d_h$) calculated as $d_h = 0.8 \times d_1$, allowing full engagement without inducing excessive radial tensile strain.
From trivalent clear/yellow zinc to nickel plating, micro-crack black oxide, and zinc-nickel (Zn-Ni) coatings, we maintain friction coefficient windows ($\mu_{tot} = 0.12 - 0.18$) capable of exceeding 1,000 to 1,500 hours in ASTM B117 neutral salt spray tests without white or red rust inception.
R&D allocations are dedicated to ultra-light titanium Ti-6Al-4V micro self-tapping screws for wearable biomedical sensors, precipitation-hardened 17-4PH stainless steel for hyper-corrosive marine electronics, and conductive copper-alloy grounding fasteners for high-voltage EV battery modules.
Fasteners represent less than 1% of total bill-of-materials cost, yet account for more than 70% of unexpected catastrophic field failures. We design domain-specific joint architectures tailored to stringent end-use environments.
Our trilobular thread-rolling fasteners deliver chip-free, secure assembly into thin-walled extruded aluminum frames and fiberglass-reinforced battery covers. Resists harmonic vibration, thermal shock from -40°C to +125°C, and galvanic corrosion under IATF 16949 production quality controls.
Precision cold-heading down to M0.8 diameter with Torx/Six-Lobe recesses engineered to eradicate driver cam-out during robotic automatic feeding. Anti-static packaging and burr-free microscopic tolerances ensure clean integration across smartphones, drones, and telemetry equipment.
Designed with precision under-head O-ring channels vulcanized with fluorosilicone or EPDM gaskets. Eliminates leak paths across IP67/IP68 outdoor telecom distribution boxes, commercial PV combiner units, and harsh chemical instrumentation panels.
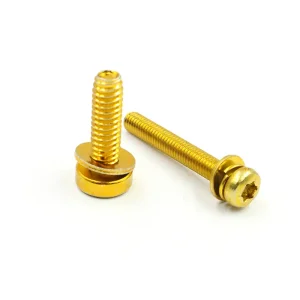
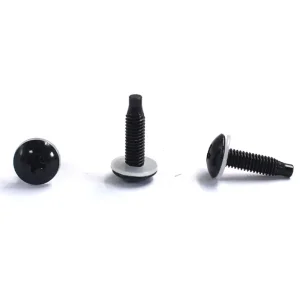
Integrated captive washer combination assemblies (SEMS) eliminate loose components on automated production lines. Coupled with factory-matched L-keys, ball plungers, and indexing pins, YH Fastener equips global machinery manufacturers with complete mechanical positioning ecosystems.
Navigating tier-1 OEM audits requires end-to-end documentation, uncompromising environmental compliance, and predictable logistics pipelines. YH Fastener operates as a verified global partner delivering comprehensive data transparency for international supply managers.
Full Production Part Approval Process (PPAP Level 3) packages provided, including Control Plans, Process FMEA, Dimensional Layouts, Gauge R&R, and direct material entry into the International Material Data System (IMDS).
100% compliant with EU Directive 2011/65/EU (RoHS 3), Regulation (EC) No 1907/2006 (REACH SVHC list), and California Proposition 65. Sourced raw materials undergo spectral composition verification against mill certs.
Submit 2D prints (.dwg, .pdf) or 3D CAD (.step, .iges). Our bilingual application engineers evaluate undercut radiuses, drive recess fit, and head volume ratios within 24 hours to accelerate prototyping cycles.
Exporting to 60+ countries across North America, Europe, and Asia. We support Vendor Managed Inventory (VMI), safety buffer warehousing, and door-to-door Delivered Duty Paid (DDP) multimodal transit.
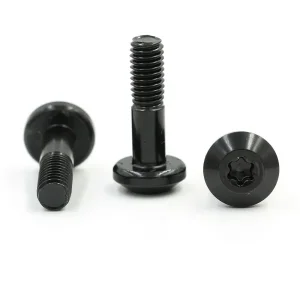
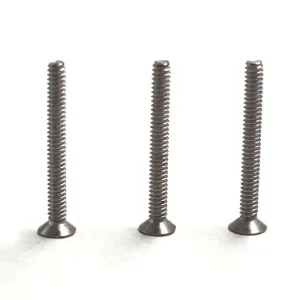
Precision fasteners configured for structural frames, PCB mountings, instrument housings, and specialized mechanical dampening. Custom head geometries and non-standard thread configurations produced to exact OEM specifications.

Direct answers to core mechanical engineering, procurement, and quality control questions frequently submitted by manufacturing systems engineers and sourcing directors.
Connect directly with YH Fastener’s senior cold-heading and metallurgical engineering team. Send 2D manufacturing drawings, 3D CAD files, or performance targets to receive complete DFM optimization, pilot sample tooling plans, and transparent factory-direct commercial terms within 24 business hours.
