Explore our standard-compliant and application-specific industrial fasteners manufactured with high-speed automated assembly lines.
Analyzing the metallurgical advantages, preload retention capabilities, and manufacturing processes of pre-assembled washer-and-screw units.
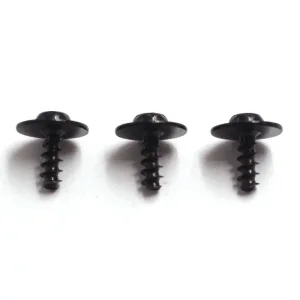
Engineering Definition: The term SEMS originates from "pre-asSEMbled" washers and screws. In high-tensile carbon steel SEMS fasteners, the washer (helical spring, external tooth, conical Belleville, or flat) is slipped onto the blank before the threads are rolled. Thread rolling cold-forms the crests beyond the washer's internal diameter, permanently capturing it while allowing free axial rotation. This eliminates manual washer placement, mitigates foreign object damage (FOD), and standardizes clamped tension across high-volume assembly lines.
We utilize premium drawn wire rods spanning Low Carbon (AISI 1018/1022) for self-tapping SEMS screws up to Medium Carbon Alloy (AISI 1045, 4135) achieving Class 8.8, 9.8, and 10.9 hardness. Controlled continuous quench-and-temper ensures uniform martensitic core structures without decarburization.
Whether pairing conical Belleville washers to absorb dynamic thermal relaxation or serrated/toothed rings to pierce non-conductive powder coats for electrical grounding, our tooling guarantees free rotation under the screw shoulder without binding before final tightening torque is applied.
To resolve hydrogen embrittlement risks in property classes ≥ 8.8, all electroplated fasteners undergo mandatory thermal de-embrittlement baking within 4 hours. We offer RoHS-compliant trivalent zinc, zinc-nickel plating (12-16% Ni), and mechanical Geomet/Dacromet flake finishes.
Operating from the industrial manufacturing cluster of Dongguan, Shaoguan, and Wuhan, YH Fastener integrates every stage of fastener cold-heading and heat treatment under one roof.
Immediate local access to cold-heading grade wire rods (Baosteel, Xingcheng Special Steel) enables custom alloy stocking and shorter extrusion lead times compared to fragmented western supply chains.
Equipped with precision CNC spark erosion and mirror-finishing die processing, custom punches and washer-feeding tracks are engineered within 7 business days, shortening ODM prototyping cycles.
Production complies with automotive APQP/PPAP requirements. From multi-stage cold header monitoring to laser image screening, every fastener meets automotive defect targets before dispatch.
Multiple high-speed glass disk optical sorting machines measure shank straightness, thread pitch, head concentricity, and washer assembly integrity at rates up to 800 pieces per minute.
Where vibration resistance, fast automated cycling, and consistent joint seating are critical engineering prerequisites.
High-tensile Grade 8.8 and 10.9 carbon steel SEMS with captive split lock or conical spring washers maintain clamp load on automotive oil pans, intake manifolds, and chassis bracketry subjected to engine vibrations.
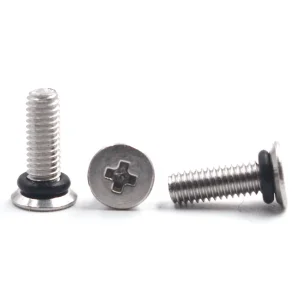
Combining under-head captive rubber elastomeric seals or conductive toothed washers ensures reliable IP67 moisture exclusion alongside grounding continuity across lightweight aluminum-to-steel joints.
M1.6 to M4 miniature carbon steel SEMS screws configured with external tooth lock washers prevent ground-connection loosening in washing machines, refrigeration compressors, and telecom server chassis.
| SEMS Configuration | Washer Dynamics | Primary Mechanical Advantage | Typical Industrial Assembly |
|---|---|---|---|
| Screw + Split Spring Lock Washer | DIN 127B / Helical Spring | Prevents complete back-off under initial relaxation | General Machinery, White Goods Frame Mounts |
| Screw + Conical (Belleville) Washer | DIN 6796 High Load Disc | Sustains constant preload through thermal expansion cycles | EV Battery Terminals, Exhaust Flanges |
| Screw + Toothed (Serrated) Washer | DIN 6798A / 6798J Internal/External | Penetrates paint, provides low-resistance electrical grounding | Control Cabinets, Audio Enclosures, Inverters |
| Screw + Double Washer (Flat + Spring) | Plain Washer + Spring Washer | Even load distribution across softer substrates with anti-loosening | HVAC Enclosures, Industrial Automotive Brackets |
How modern OEM procurement teams are mitigating geopolitical risks, automating torque control, and standardizing fasteners.
As robotic auto-feed drivers dominate modern tier-1 plants, standard screws risk dropped washers or bent feed tubes. Captive SEMS units offer smooth, jam-free passage through automated pneumatic feed mechanisms.
Procurement calculations now weigh total operational cost over unit purchase price. Sourcing SEMS cuts two discrete part numbers down to one, halving inventory handling, PO lines, and lost-parts scrap.
Modern EV battery and powertrain lines require tightening to target yield points. Fastener suppliers must supply controlled friction coefficients (μtot = 0.12 - 0.18) via specialized waxes and integrated topcoats.
Precision-manufactured threaded solutions engineered to international standards and custom drawing specifications.
Detailed answers covering manufacturing tolerances, washer combinations, and quality compliance for engineering teams.
During SEMS manufacturing, the washer has an internal hole diameter larger than the screw shank blank diameter, but smaller than the finished major thread diameter. When the blank passes between thread rolling dies, cold flow forces displacement of metal outwards to form threads. This expands the outer diameter past the washer's aperture, locking it beneath the head permanently while still allowing it to spin freely.
For carbon steel grades with tensile strength exceeding 800 MPa (Class 8.8, 10.9) that undergo acid pickling and electroplating, atomic hydrogen can migrate to grain boundaries under stress. We mitigate this through controlled low-acid cleaning processes combined with mandatory de-embrittlement baking at 200°C–220°C for 4 to 8 hours immediately post-electroplating, verified per ISO 15330 stress durability testing.
Yes. Our automated feeding assemblies can stack both a flat washer (to span oversized clearance holes and distribute clamp load) and a helical spring or conical disc washer (to retain tension). Both washers are captured in sequence beneath the cold-headed screw head prior to thread rolling.
We provide trivalent clear/yellow zinc (Cr3+), Zinc-Nickel (ZnNi) alloy plating offering over 1,000 hours to red rust per ASTM B117, and non-electrolytic zinc flake coatings (such as Geomet, Dacromet, or Magni). Coatings can be integrated with PTFE or synthetic wax lubricants to guarantee tight torque-tension coefficients.