Industrial-grade carbon-steel tamper-resistant fasteners manufactured with proprietary tooling, strict thread-rolling metrics, and high-tensile core integrity.


In high-torque, vandal-resistant enclosures, standard austenitic stainless screws frequently succumb to drive recess shearing and galling. Our carbon-steel alloys bridge the strength gap.
Utilizing cold-heading grade carbon steels (1018, 1022, 10B21), our screws undergo carburizing or neutral hardening, achieving surface hardnesses exceeding HV 450–750 and core hardnesses up to HRC 32–39. This eliminates drive-socket round-out during high-torque power driver installations.
Tamper-resistant heads (Pin-in-Torx, Security Hex, Snake-Eye Spanner, Tri-Wing, One-Way) require microscopic dimensional adherence. Micro-forged on multi-station header dies, our recess drive walls maintain zero draft angles, preventing cam-out and preserving recess longevity.
Compared to expensive nickel-alloys or 316 stainless steels, engineered carbon steel provides an optimal strength-to-cost ratio for massive OEM production runs. Combined with eco-friendly zinc-nickel or Geomet finishes, it delivers equivalent corrosion defense at scale.
Direct supply-chain vertical integration from the Pearl River Delta: 20,000 m² across three manufacturing facilities in Dongguan, Shaoguan, and Wuhan.
Our in-house EDM and tool-and-die center produces bespoke security-drive punch pins in under 72 hours. With over 200 multi-station high-speed cold headers, we achieve rapid dimensional adaptation for bespoke proprietary drives.
All finished fastener series comply fully with European RoHS 3 (Directive 2015/863) and REACH SVHC regulations. Mill test reports (MTR), full chemical analysis, and PPAP Level 3 documentation are available on demand for tier-1 supply chains.
Equipped with computerized high-speed multi-laser optical sorting machines, we inspect 100% of fastener batches for head diameter, recess pin concentricity, thread pitch integrity, and plating coverage, guaranteeing <50 PPM delivery standards.
Comprehensive engineering benchmarks for procurement managers, structural engineers, and quality assurance specialists.
| Alloy Specification | Heat Treatment Type | Surface Hardness | Core Hardness | Protective Coating Options | Corrosion Resistance (SST) |
|---|---|---|---|---|---|
| AISI 1018 / 1022 | Case Hardened (Carburized) | HV 450 – 650 | HRC 28 – 34 | Trivalent Zinc (Clear / Yellow) | 48 – 96 Hours to White Rust |
| AISI 10B21 (Boron Steel) | Quenched & Tempered (Neutral) | HV 550 – 720 | HRC 33 – 39 | Zinc-Nickel Alloy (Zn-Ni) | 720 – 1,000+ Hours to Red Rust |
| AISI 1035 / 1045 | Through Hardened Class 8.8 / 10.9 | HV 480 – 600 | HRC 32 – 38 | Black Oxide + Corrosion Oil | 24 – 48 Hours to Red Rust |
| SCM 435 Alloy Steel | High-Strength Class 12.9 | HV 650 – 780 | HRC 39 – 44 | Geomet® / Dacromet® Flake | 1,000 – 1,500 Hours to Red Rust |
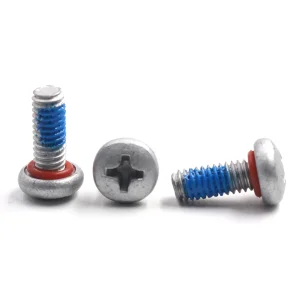
| Pre-Applied Nylon Patch | Prevailing Torque Polyamide | Operational Range | -50°C to +150°C | DIN 267-28 Locking Mechanism | Reusable (Up to 5 Install Cycles) |
Engineered for mission-critical installations where physical hardware tampering, IP theft, and unauthorized access must be structurally prevented.
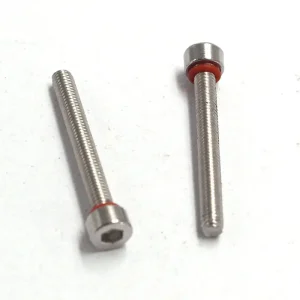
High-voltage battery packs, PCS conversion boxes, and highway DC superchargers utilize high-tensile carbon steel anti-tamper fasteners with sealing O-rings, providing IP67 sealing alongside strict unauthorized access prevention.
Financial transaction machines and smart metering equipment deploy security torx and triangle-drive screws to prevent skimming-device installations and housing breaches, compliant with PCI-PTS hardware security mandates.
Outdoor 5G microcell towers and distributed power distribution transformers demand heavy-duty Class 8.8+ anti-theft bolts with multi-year salt-spray corrosion protection to thwart component vandalism in remote facilities.
How automation, zero-hydrogen embrittlement treatments, and custom drive keys are defining modern fastening engineering.
High-tensile carbon steels (Grade 10.9+) are vulnerable to atomic hydrogen absorption during acid pickling and electroplating. Modern production enforces immediate 4-to-8 hour de-embrittlement baking at 200°C–220°C, ensuring zero delayed brittle failures under preload.
Public standard security drives (Torx Tamper TR, Snake Eye) can now be unlocked with widely available commercial bit sets. Tier-1 manufacturers increasingly produce proprietary asymmetric drives, issuing uniquely coded driver keys exclusively to authorized enterprise teams.
Global environmental mandates (RoHS/WEEE) have rendered Cr6+ obsolete. Production is fully converted to thin-film non-electrolytic zinc flake (Dacromet/Geomet) coatings, yielding over 1,000 salt-spray hours without risk of acidic hydrogen introduction.
Direct technical answers addressing mechanical specs, tooling lead times, and global shipping assurances.
Advanced anti-vibration nylon locking, captive spring-plunger detents, and specialized surface-mounting fasteners directly from our manufacturing bays.