Engineered anti-tamper profiles, pre-assembled combination hardware, and sealing socket cap screws verified across high-stress industrial applications.

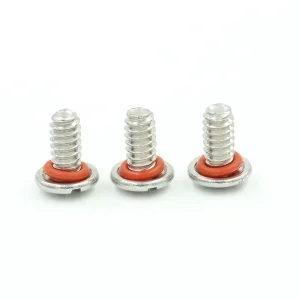
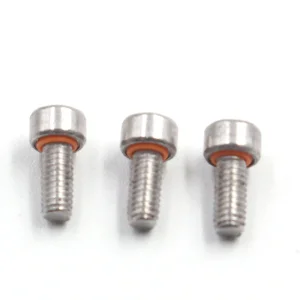

Analyzing structural resistance, torque transmission kinematics, and the worldwide surge in anti-tamper hardware adoption across tier-1 manufacturing supply chains.
Modern security fasteners have evolved beyond rudimentary one-way slots. Today's mission-critical hardware relies on cylindrical socket cap profiles integrated with post-recess geometries (Pin-in-Hex, Pin-Torx, Tri-Groove, and non-concentric drive keys). These designs resist high-torque extraction attempts with off-the-shelf tools, eliminating unauthorized tampering while maintaining consistent assembly clamping loads for industrial field service.
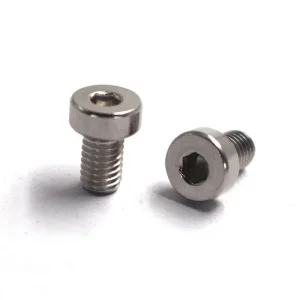
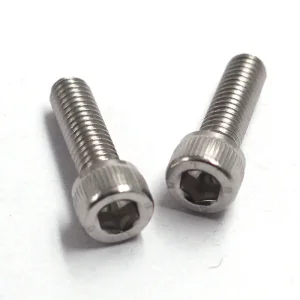
Traditional flat and countersunk security fasteners frequently suffer from driver cam-out under high-speed automated torquing. Cap head security screws (DIN 912 / ISO 4762 variant standards) provide a deep engagement socket that concentrates radial forces perpendicular to the tool interface. This minimizes bit slippage, extends driver tooling lifespan, and prevents catastrophic recess wall strip-out in automated robotic assembly.
The pronounced cylindrical shoulder and flat bearing surface of cap head configurations maximize load dispersal across adjacent structural substrates. Unlike countersunk fasteners that introduce lateral wedge stresses, cap head geometry distributes uniform compressive loads. When engineered with integrated under-head O-ring seals, these security screws provide hermetic IP67/IP68 ingress protection against fluid, dust, and galvanic chemical corrosion.
How multi-station progressive cold heading and integrated regional supply ecosystems outperform traditional European and North American machining models.
Consolidated workshops across Dongguan, Shaoguan, and Wuhan plants.
Laser profile verification and automated optical eddy current sorting.
Continuous cold forming R&D since 1998 for international OEMs.
Chemical spectrometer analysis, micro-hardness, and salt spray testing.
Traditional European and US manufacturers often machine specialized security recesses via secondary milling, CNC rotary broaching, or EDM cutting. Yu-Huang Electronics deploys high-speed multi-station progressive cold headers. By forming the cap head, internal drive recess, and security center pin in a single continuous impact sequence, grain boundary flow remains uninterrupted. This yields 28% higher shear and tensile yield strength while reducing cycle times from minutes to fractions of a second.
Security screw manufacturing is heavily constrained by punch wear; anti-tamper center pins cause localized thermal stress that fractures conventional punches. Our Dongguan tool center engineers proprietary tungsten carbide cold-heading punches coated with physical vapor deposition (PVD) titanium aluminum nitride (TiAlN). This proprietary tooling architecture maintains micro-tolerances within ±0.01mm over continuous production runs exceeding 500,000 units per die set.
The Greater Bay Area manufacturing cluster allows Yu-Huang to source audited wire rod (304, 316, SCM435, 10B21), perform spheroidizing annealing, high-precision thread rolling, continuous vacuum heat treatment, and electrolytic surface plating within a 40-kilometer radius. This hyper-dense industrial base compresses typical 16-week international non-standard fastener lead times down to 18-25 business days from tooling sign-off to overseas dispatch.
Analyzing high-reliability environments that depend on custom cap head security hardware to safeguard intellectual property, electrical enclosures, and life-safety systems.
Electric vehicle battery enclosures, DC-DC converter housings, and onboard charging units require secure fastening that prevents end-user tampering with lethal 800V DC busbars. Custom cap head security screws featuring integrated fluorosilicone or EPDM O-rings provide IP68 water sealing while their proprietary pin-drive profiles prevent unauthorized disassembly in non-certified repair centers, preserving vehicle safety certifications.
Utility-scale solar arrays and commercial battery energy storage systems (BESS) are situated in remote, unmonitored outdoor environments. Stainless steel 316 and Geomet-coated alloy security cap screws secure exterior junction boxes, combiner cabinets, and inverter access panels against opportunistic copper theft, weather ingress, and vandalism while enduring 1,500+ hours of ASTM B117 neutral salt spray exposure.
Public infrastructure assets—such as automated fare collection gates, roadside LiDAR sensor pods, surveillance radar units, and passenger information displays—demand fasteners that cannot be removed by standard Allen wrenches or screwdrivers. Cap head security screws provide structural clamping that resists vibration-induced back-off caused by passing trains and heavy truck traffic.
Factory automation systems, collaborative robotic arms, and edge computing enclosures require compact yet strong hardware. The cylindrical socket cap head profile allows screws to sit flush inside precision counterbored recesses, conserving valuable clearance in tight mechanical envelopes while shielding internal optical and PCB assemblies from unauthorized hardware modifications.
Precision laboratory hardware, diagnostic analyzers, and surgical equipment incorporate calibrated optical and fluidic paths. Custom cap head security screws produced in medical-grade austenitic stainless steel ensure maintenance is restricted strictly to factory-certified technicians, protecting machine calibration, medical data accuracy, and patient safety.
Pole-mounted 5G massive MIMO antennas and remote radio heads (RRHs) face intense wind-load buffeting and severe thermal cycling. Security screws equipped with microencapsulated thread-locking adhesives (nylon patches or 3M chemical lock) prevent micro-vibration loosening while locking down valuable telecommunications components against tower vandalism.
Comprehensive material classification, mechanical proof load thresholds, and surface conversion chemistry engineered to satisfy international ISO, DIN, and ASTM standards.
| Material Class | Common Grades | Tensile Strength (MPa) | Yield Strength (MPa) | Vickers Hardness (HV) | Primary Industrial Use Cases |
|---|---|---|---|---|---|
| Austenitic Stainless | AISI 304 (A2-70), AISI 316 (A4-80) | 700 – 800 | 450 – 600 | 210 – 260 | Marine, cleanrooms, outdoor telecommunications, solar hardware |
| Medium Carbon Alloy | SCM435, 10B21 (Class 8.8) | 800 – 830 | 640 – 660 | 250 – 320 | General machinery, consumer appliances, structural cabinetry |
| High-Strength Alloy | 40Cr, SCM440 (Class 10.9 & 12.9) | 1040 – 1220 | 940 – 1100 | 320 – 440 | Automotive chassis, powertrain mounts, high-vibration robotics |
| Corrosion-Proof Brass | H62, H65, C3604 | 400 – 520 | 200 – 300 | 110 – 150 | Non-magnetic electrical switchgear, precision fluid instrumentation |
| Lightweight Titanium | Grade 2, Grade 5 (Ti-6Al-4V) | 895 – 1000 | 825 – 920 | 310 – 360 | Aerospace sensors, racing suspension assemblies, portable medical devices |
To eliminate reliance on separate spring washers that can deform the bearing face, Yu-Huang applies precision 360-degree polyamide patches (DIN 267-28) or microencapsulated anaerobic adhesives (DIN 267-27). Upon thread engagement during torque-down, microcapsules rupture and polymerize, sealing thread roots against fluid migration and securing joint clamp load under harmonic vibration.
For high-corrosion industrial environments, we deliver non-electrolytic zinc flake coatings (Geomet 321/500, Dacromet) that provide zero hydrogen embrittlement risk on high-tensile 10.9 and 12.9 fasteners. Standard finishes include trivalent clear/black zinc plating (RoHS and REACH compliant), electroless nickel plating for wear resistance, and multi-stage chemical passivation for stainless series.
Consistent clamping force requires tightly controlled thread coefficient of friction (µtot between 0.10 and 0.16). By formulating custom wax and fluoropolymer topcoats, our factory stabilizes torque-tension relationships. This prevents over-stretching during automated assembly torquing while ensuring the security cap screw achieves its calculated clamping force every cycle.
How automation compatibility, smart RFID integration, proprietary drive geometries, and lightweight alloys are redefining the next generation of security hardware.
Modern high-volume manufacturing lines reject fasteners that lodge in vibratory feeder tracks. Traditional security screws with asymmetrical heads often tangle in automated chutes. The uniform cylindrical cap head architecture, paired with precision-chamfered head tops and stabilized shank-to-head center of gravity, ensures smooth movement through automated pneumatic blow-feed tooling at assembly speeds exceeding 60 cycles per minute.
Off-the-shelf Pin-Torx or Pin-Hex bits are increasingly accessible to consumers through retail channels. Tier-1 enterprise customers now partner directly with Yu-Huang to engineer proprietary drive patterns—such as custom 5-lobe non-symmetrical keyways, parabolic curve recesses, and multi-depth step geometries. Tooling bit sets are controlled under NDA and distributed exclusively to authorized OEM service channels.
Next-generation cap security hardware incorporates micro-engineered head cavities designed to accept color-shifting pressure indicators or microscopic RFID/NFC chips. These tamper-evident features visually indicate unauthorized torque disruption or fracture when subjected to uncalibrated maintenance tools, protecting OEM warranty governance from invalid claims.
A structured technical assessment matrix for global procurement teams vetting OEM/ODM cold-heading fastener manufacturers.
Global automotive and energy enterprises require complete Advanced Product Quality Planning (APQP) validation. Yu-Huang provides comprehensive Production Part Approval Process (PPAP) Level 3 packages, including Process FMEA, Control Plans, Gage R&R studies, 100% Dimensional Inspection Reports, Raw Material Mill Certificates, and Full IMDS / RoHS / REACH compliance declarations prior to mass dispatch.
Manual batch sampling cannot ensure automated assembly line continuity. Our factory lines incorporate dual-glass-plate high-speed optical inspection machines capable of checking 800 parts per minute. Cameras inspect major/minor thread diameters, head runout, pin recess concentricity, and under-head radius, while eddy current testing detects sub-surface metallurgical fractures and incomplete heat treatment.
Batch integrity is maintained by barcoded ERP tracking at each stage: wire descaling, multi-station cold heading, thread forming, heat treatment, plating, and final packing. Every export box contains heat code tracking numbers, allowing cross-referencing against chemical spectrometers, tensile rupture graphs, and furnace temperature logs for a minimum of 10 years.
Direct answers from Yu-Huang's fastener engineering team on tooling, drive geometry, material selection, and procurement logistics.
Precision-rolled metric threads, stainless steel machine fasteners, and specialty vibration-resistant hardware directly from our Dongguan production plants.
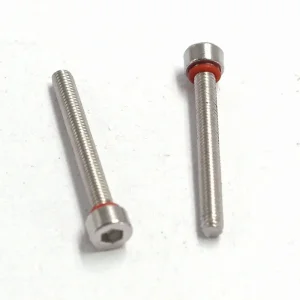


Submit your 2D/3D part drawing, material callout, target torque requirement, and volume forecast. Our senior cold heading application engineers will review tooling feasibility, cost-optimization opportunities, and provide formal quotation within 24 hours.
