High-precision cold heading engineering, customized drive profiles, and industrial-grade surface protection for global OEM automotive, green energy, and precision electronics assemblies.
Factory-direct micro and industrial fasteners engineered with low installation torque, high pull-out resistance, and certified corrosion barriers.
Truss head self tapping screws (also recognized as mushroom head or broad-bearing fasteners) provide the optimal load distribution profile required for modern structural assemblies. By combining an oversized, low-profile dome with aggressive thread geometry, these fasteners eliminate separate washers, reduce assembly steps, and prevent sheet metal tearing.
The low-profile extra-wide dome generates a surface contact radius up to 40% larger than conventional pan or round heads. This design prevents localized surface crushing and dimpling on thin sheet metal, composite brackets, and molded polymer enclosures.
Engineered to accommodate high-productivity automated lines. Available in deep Phillips, Torx (6-lobe), combination cross/slot, and tamper-resistant security pins, eliminating cam-out failures while maintaining tool bit longevity.
Precision thread-forming geometries (Type AB, Type B, and spaced PT-style thread banks) generate robust mating internal threads in unthreaded pilot holes, significantly cutting production cycle times and eliminating secondary tapping lubricants.
Fastener selection impacts warranty costs, automated cycle times, and mechanical reliability under extreme shock, vibration, and thermal cycling.
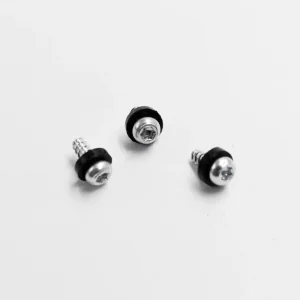
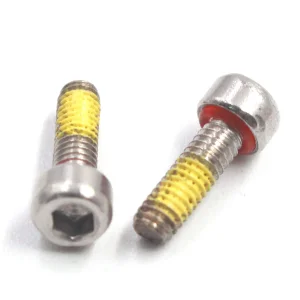
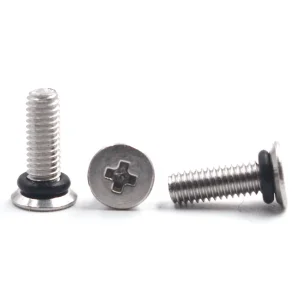
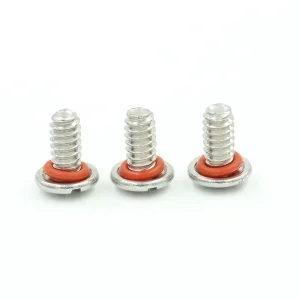
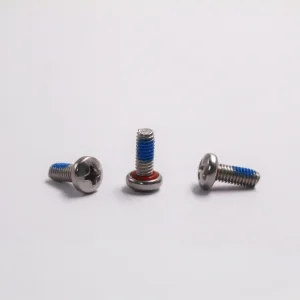
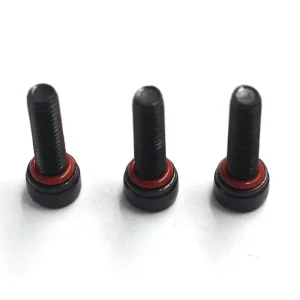
Electric vehicle battery packs, electronic control units (ECU), and interior trim call for lightweight fasteners that resist severe vibration. We supply modified truss head screws equipped with micro-encapsulated thread lockers or integrated EPDM/O-ring sealing washers to preserve IP67/IP68 ingress ratings under harsh operating road profiles.
Rooftop and commercial PV tracker frameworks require external corrosion resilience surpassing 1,000 to 2,000 hours in neutral salt spray testing (ASTM B117). We deploy austenitic 304/316 stainless steels, zinc-nickel plating, and multi-layer organic mechanical coatings that avoid hydrogen embrittlement while retaining clamp load over 25+ year outdoor design lifespans.
Miniaturized servers, network communication racks, and smart home modules leverage ultra-thin truss heads to maximize internal design clearance. Controlled lead-ins and razor-sharp threads minimize radial bursting stresses inside thin-walled injection molded resins (ABS, Polycarbonate, Nylon), delivering consistent seating torques.
Every batch complies with rigorous geometric dimensional tolerances (GD&T) verified via automated laser sensors and optical sorting machines before shipment.
| Design Parameter | Technical Capability & Options | Engineering Standards |
|---|---|---|
| Nominal Diameter Range | M1.2 to M10 (#0 to 3/8" inch series) | DIN 7981, ISO 7049, ASME B18.6.3, JIS B1122 |
| Head Geometries | Standard Truss Head, Modified Ultra-Low Truss, Wide-Wafer, Sems Combo | Customized prints via multi-die cold heading |
| Thread Profile Options | Type AB, Type B, Type A, Spaced PT Thread (for Plastics), Tri-Lobular | Thread-forming, Thread-cutting, and High-Low thread types |
| Raw Materials | Carbon Steel (1018, 1022A), Stainless Steel (304, 316, 410), Brass, Aluminum | Full material certs (MTR) & spectrometry verification |
| Surface Finishes | Eco Zinc Plated (Blue/Yellow/Black), Nickel, Electrophoresis Black, Dacromet, Ruspert | RoHS / REACH compliant; 24h to 2000h Salt Spray (ASTM B117) |
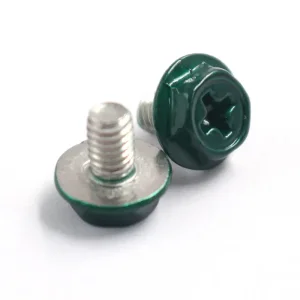
| Secondary Additions | Nylon patch locking (blue/yellow), pre-assembled captive washers, sealing O-rings | DIN 267-28 prevailing torque locking standards |
Our 20,000 m² manufacturing sites in Dongguan, Shaoguan, and Wuhan ensure multi-point redundancy, rapid prototyping, and end-to-end trace control.
Quality assurance starts with validated wire coil suppliers. We execute continuous SPC tracking during cold heading and thread rolling, complete batch hardness profiling, core microstructure analysis, and micro-Vickers depth verification to ensure high shear strength without risk of brittle head separation.
Exporting direct to 60+ countries across North America, Europe, and Asia Pacific. All production batches are strictly documented with Full Material Declarations, PPAP Level 3 capabilities (on demand), and certificates of compliance with European RoHS, REACH, and Dodd-Frank conflict mineral guidelines.
We offer full-cycle application support, including CAD review, finite element pilot hole analysis, and rapid sample prototyping within 3 to 5 working days. Our senior engineering response team addresses customer inquiries within 24 hours.
Adapting cold forming methodologies to meet the demands of automated assembly lines, ultra-light alloys, and low carbon requirements.
To support vehicle lightweighting and energy efficiency, we are scaling high-tensile 6000/7000-series aluminum and titanium alloy cold heading, providing a 40% weight reduction compared to carbon steel while retaining adequate clamping load.
Modern factory automation relies on high-speed blow-feed systems. We refine head symmetry, deburring methods, and driver recess depths to achieve sub-50 PPM sorting reliability, eliminating sorting bowl jams on high-speed robotic assembly arms.
Developing scrap-free heading sequences alongside closed-loop heat treatment facilities that use renewable electrical induction, reducing embodied carbon per million fastener units in accordance with Scope 3 ESG supply chain requirements.
Key mechanical differences, design calculations, and purchasing queries answered by our manufacturing team.
The primary differentiator is head diameter and surface bearing area. A truss head features a lower profile dome combined with a broader flat underside. This spreads the clamping force across a larger surface area, mitigating the risk of sheet metal deformation, hole pull-through, or composite cracking without needing a separate flat washer.
Type A features a coarse pitch with a gymlet-pointed tip, commonly applied in light wood or thin sheets. Type B is characterized by a blunt end with finer thread pitches, designed for heavier metal sheets and die castings. Type AB incorporates the sharp gymlet pilot tip of Type A with the refined thread pitch of Type B, making it the preferred standard for thin metal stamping pilot holes.
For high-tensile carbon steel self tapping screws (hardened to HRB 90+ or case hardened to 450-550 HV for sheet penetration), electroplating can introduce atomic hydrogen. We follow strict baking protocols: within 4 hours post-acid de-rusting and plating, fasteners are baked at 190°C–210°C for 4 to 8 hours to eliminate trapped hydrogen and prevent catastrophic delayed head snapping.
Yes. Our engineering shop produces custom cold heading dies and punches. We frequently develop customized combinations such as ultra-low wafer truss heads, security pin drives (tamper-proof Torx, Tri-Wing, Snake Eye), under-head serrations for grounding/anti-loosening, and customized integrated captive elastomer assemblies.
Explore specialized anti-loosening, sealing, and precision positioning assemblies manufactured across our production network.