Explore our flagship precision screws, indexing spring plungers, and mating drive components engineered for automated OEM production lines and rigorous vibration resistance.



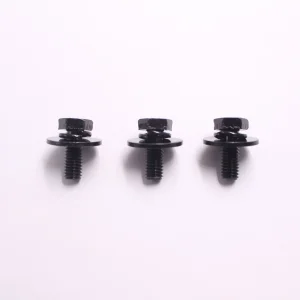
Understanding the mechanical kinematics, contact geometry, and metallurgical requirements governing modern T10 internal hexalobular drive tooling.
Unlike traditional cruciform Phillips or slotted drives that naturally push the driver outward as torque increases, the ISO 10664 T10 hexalobular geometry maintains a 15-degree drive angle. This near-zero radial separation force eliminates cam-out, reduces worker fatigue, and prevents devastating head stripping on high-speed automated lines.
The T10 Torx profile provides elliptical lobes that transfer torque over a broad contact area rather than concentrated single-point corner edges typical of standard hexagon keys. This dramatically lowers Hertzian contact stress, preserving both the tool tip and the fastener recess across hundreds of disassemblies.
At YH Fastener, our China manufacturing lines grind T10 keys to strict across-lobes dimensioning (2.74 mm ± 0.02 mm) with pin-center tolerances within 0.015 mm for tamper-proof T10H variations. This precision fit ensures absolute engagement with minimal play and predictable torque transfer coefficients.
Selecting the correct metallurgical substrate is the single largest determinant of tool lifecycle, torsional deflection, and plastic deformation prevention in critical OEM applications.
| Performance Parameter | Industrial S2 Tool Steel (YH Standard) | Chrome Vanadium (CR-V 6150) | Standard Carbon Steel (Grade 45) |
|---|---|---|---|
| Rockwell Core Hardness (HRC) | HRC 58 - 62 (Atmospheric Quenched) | HRC 52 - 56 (Oil Quenched) | HRC 42 - 48 (Surface Induction) |
| Yield Strength (MPa) | 1,950 - 2,150 MPa | 1,450 - 1,600 MPa | 650 - 850 MPa |
| Torsional Fatigue Endurance | > 25,000 cycles at 75% max load | ~ 12,000 cycles at 75% max load | < 3,500 cycles (Prone to twist) |
| Ductility / Brittleness Transition | Cryogenic tempered: Zero shattering | Standard toughness: Rare brittle fracture | Moderate: Prone to plastic shear rounding |
| Surface Protection Treatments | Manganese Phosphate, TiN, Satin Chrome, Electrophoresis | Bright Chrome, Zinc Plating, Black Oxide | Standard Blackening, Light Zinc |
| Primary Target Application | Automated robotics, high-torque industrial line assembly | Maintenance toolkits, general mechanical repair | Low-cost DIY retail consumer packs |
Discover how YH Fastener combines multi-facility capacity across Dongguan, Shaoguan, and Wuhan with intelligent MES automation to de-risk tier-one international supply chains.
Our distributed production ecosystem across Dongguan (HQ & cold heading center), Shaoguan (secondary high-tonnage forming), and Wuhan (assembly & regional stocking) prevents supply chain bottlenecks and protects global clients from localized disruptions.
Every critical batch of T10 Torx keys and matching security machine screws undergoes 360-degree automated glass-disk optical inspection. Cameras verify hexalobular flank height, tamper pin concentricity, and thread lead pitch at speeds exceeding 600 pcs/minute.
Operating rigorously under IATF 16949 (automotive supply chains), ISO 9001 (quality management systems), and ISO 14001 (environmental sustainability), YH Fastener provides PPAP Level 3 documentation, full material heat-number tracing, and lot certificate packages.
Located in the heart of the Greater Bay Area hardware cluster, we source certified Japanese and Taiwanese alloy wire coils with 24-hour lead times. Secondary surface treatment plants (nickel, zinc-nickel alloy, trivalent chrome) operate within a 15-kilometer radius.
T10 hexalobular systems are critical across micro-assembly and heavy industrial components where zero fastener loosening and rapid serviceability are uncompromising mandates.
Modern laptops, smartphones, drone gimbals, and telecommunication switchboards rely heavily on M2.5 to M3.5 screws paired with T10 drive recesses. The high torque transmission prevents screw head stripping during delicate automated assembly, while security pin-in-torx (T10H) patterns prevent unauthorized consumer tampering.
Under IATF 16949 production standards, our T10 wrenches and mating screws serve electric vehicle battery enclosure seals, infotainment dashboard assemblies, and inverter casing joints. Tight dimensional tolerances prevent vibration loosening under severe road harmonic excitation.
Diagnostic imaging equipment, laboratory peristaltic pumps, and surgical robotic arms require non-shedding, corrosion-resistant fastening interfaces. We produce passivated 304/316 stainless steel and vacuum-coated T10 drivers that withstand aggressive autoclaving and chemical sterilization cycles.
Explore our active engineering R&D pathways designed to anticipate the micro-fastening, low-friction, and ESG decarbonization demands of future automated industries.
By integrating diamond-like carbon (DLC) and physical vapor deposition (PVD) titanium carbo-nitride (TiCN) coatings onto our cold-forged S2 T10 drivers, surface friction is cut by 68%. This yields a microscopic surface hardness exceeding 3,000 Vickers, drastically extending automated continuous driver-bit life.
Capitalizing on our cold-heading and EDM wire-cut die technologies, we have expanded our tooling matrices down to sub-millimeter scales (T1, T2, T3, T4, T5) to support next-generation augmented reality smart eyewear, implantable medical sensors, and nano-satellite payload integration.
In accordance with the EU Carbon Border Adjustment Mechanism (CBAM), YH Fastener is introducing low-carbon annealed alloy wire rods melted using electric arc furnace (EAF) technology. Our Dongguan finishing line utilizes closed-loop water reclamation and zero-hexavalent-chromium zinc-nickel solutions.
Streamlining customs clearance and supply reliability for global procurement directors through comprehensive regulatory certifications and customized replenishment contracts.
All finished screws, L-keys, flag-type drivers, and spring plungers strictly comply with EU Directive 2011/65/EU (RoHS 3) and Regulation (EC) No 1907/2006 (REACH SVHC). Full CFSI CMRT documentation certifies tin, tantalum, tungsten, and gold are 100% ethically sourced.
We support tier-one manufacturers through flexible VMI agreements, blanket order call-offs, and localized warehouse buffer stocks in Rotterdam, Chicago, and Singapore. Minimum 60-day safety stock buffers protect your production schedules from ocean freight volatility.
For automotive powertrain and chassis assemblies, our engineering team supplies Production Part Approval Process (PPAP) packages including Design FMEA, Process Flow Charts, Control Plans, Gage R&R studies, and Full Dimensional Measurement Reports.
Why leading Fortune 500 procurement executives analyze holistic assembly yield, bit wear rates, and automated uptime rather than nominal unit purchase price alone.
| Evaluation Factor | YH Fastener Engineered Solution | Generic Commodity Supplier | Impact on Overall TCO |
|---|---|---|---|
| Driver Profile Engagement | 100% matched to ISO 10664 cold-heading tooling | Mismatched broaching tolerances | Eliminates micro-burrs and stripped screws during final assembly |
| Batch Hardness Uniformity | Computer-controlled continuous vacuum furnace (± 1.5 HRC) | Manual salt-bath quenching (± 4 HRC) | Prevents sudden tool shatter during torque-gun cycle spikes |
| Pre-Applied Locking Options | Automated 360° or 180° nylon patch (DIN 267-28) | Secondary liquid threadlock (applied manually) | Saves $0.08–$0.14 per joint in manual labor and messy cleanups |
| Traceability & Certification | Heat-number tracking stamped on export packaging | Generic uncertified box tags | Prevents costly customs holds and warranty chargebacks |
Answers to complex engineering, material specification, and international logistics questions submitted by global industrial procurement managers.
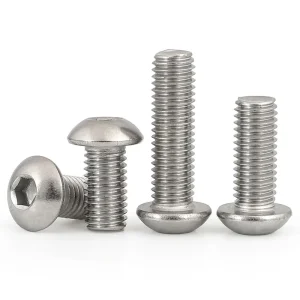
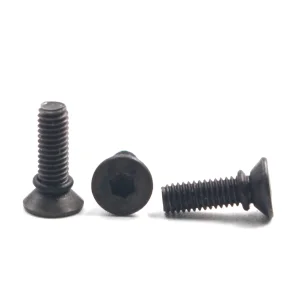
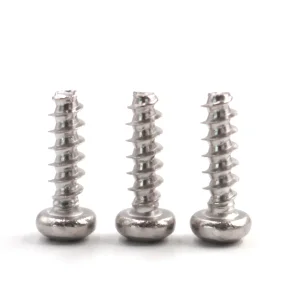
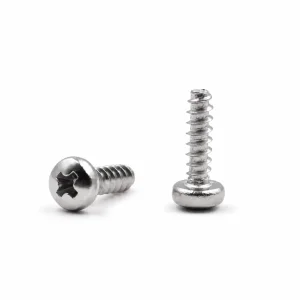
Browse our certified industrial fastening components, anti-loosening PT thread configurations, waterproof sealing fasteners, and positioning ball plungers.

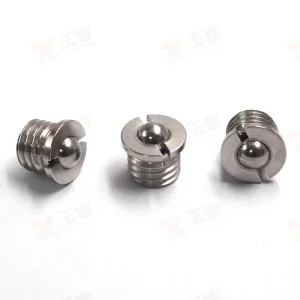
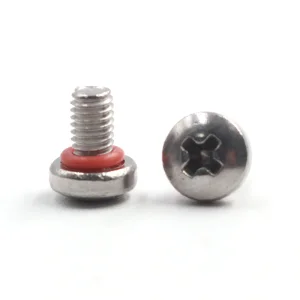
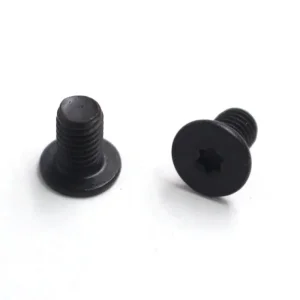
Upload your 2D/3D part drawings (.STEP, .IGS, .DWG) or custom fastener specifications. Our senior metallurgical and tooling engineers will provide full feasibility analysis, quote matrices, and rapid prototyping within 48 to 72 hours.
Initiate Technical RFQ Review