Explore factory-direct SEMS combinations, sealing machine screws, and precision threading solutions engineered across our Dongguan, Shaoguan, and Wuhan facilities under rigorous IATF 16949 parameters.




A rigorous examination of captive SEMS washer mechanics, preload tension retention, and dynamic load dissipation under continuous operational vibration.
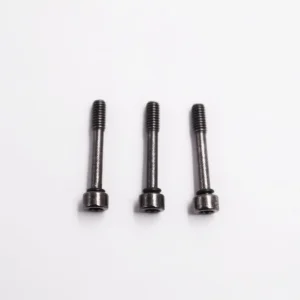
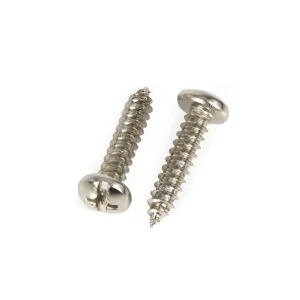
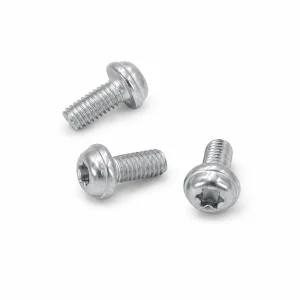
In automated industrial manufacturing, assembly screw failure is rarely a catastrophic tensile snap; it is predominantly a gradual loss of preload caused by cyclic transverse vibration, thermal relaxation, and embedment relaxation. An industrial hex assembly screw—commonly integrated as a SEMS unit (Screw and Washer Assemblies) under DIN 6900, DIN 7985, or ASME B18.13 standards—permanently captures single or dual washers (flat, conical/Belleville, spring, or toothed) under the cold-headed hexagon or hex-washer flange head before thread rolling. By cold-rolling threads after washer installation, the major thread diameter is enlarged past the internal diameter of the washer, securing it permanently while allowing free rotational clearance. This eliminates washer omission errors, standardizes under-head friction coefficients, and accelerates assembly throughput by up to 34% on high-speed robotic lines.
Preload force ($F_M$) stability governs bolted joint reliability. When tightened, hex assembly screws convert tightening torque ($M_A$) into axial tension through thread mechanics and under-head contact surfaces. By integrating captive Belleville conical washers or serrated wave washers, the joint introduces elastic spring deflection that dynamically compensates for micro-yield embedment and gasket creep across fluctuating temperature zones (-40°C to +150°C).
Under ISO 16047 torque-tension testing, unexplained variations in the total friction coefficient ($\mu_{ges}$) cause severe clamp load scatter—resulting in either joint loosening or thread stripping during automatic driving. YH Fastener employs proprietary lubricant topcoats and high-precision electrolytic finishes to maintain consistent friction windows ($\mu = 0.10 - 0.16$), delivering predictable clamping loads within ±6% across high-speed driver RPMs.
Standard fasteners subjected to Junker vibration tests (DIN 65151) often experience total preload decay within 300 cycles. Industrial hex assembly screws engineered with micro-encapsulated chemical patches (DIN 267-27) or captive double-spring lock washers preserve over 85% residual clamp force past 2,000 harmonic cycles, resisting transverse shear stress in powertrain, chassis, and heavy reciprocating compressor blocks.
How specialized hex assembly screws perform within mission-critical sectors spanning electric mobility, renewable infrastructure, heavy industrial automation, and micro-electronic enclosures.
Within battery pack trays, hex assembly screws with integrated non-conductive EPDM sealing collars or ground-piercing toothed washers ensure IP68 hermetic isolation against moisture while sustaining structural integrity during vehicle curb impact tests.
End-of-arm tool changers and 6-axis articulated robotic linkages utilize Grade 10.9 & 12.9 alloy hex socket assembly screws with thread-forming trilobular shanks, resisting cyclical torsional snap under sudden acceleration reversal.
Photovoltaic slewing drives and offshore nacelles expose fasteners to salt spray and thermal shocks. Austenitic 316 and Duplex stainless steel hex SEMS parts treated with multi-stage passivation withstand over 1,500 hours of continuous ASTM B117 salt fog exposure.
5G base station outdoor housings require high EMI shielding and IP67 weather-proofing. Hex washer head sealing screws with embedded silicone O-rings form a complete gas-tight seal directly upon seating, preventing galvanic corrosion across aluminum cast walls.
Evaluating total cost of acquisition, supply chain resilience, and precision cold-heading infrastructure in the Greater Bay Area and Central China manufacturing corridors.
Global original equipment manufacturers (OEMs) demand rock-solid supply continuity. Operating three synchronized production hubs in Dongguan (Guangdong HQ), Shaoguan, and Wuhan allows YH Fastener to decouple regional logistics risks, scale batch capacities to hundreds of millions of units monthly, and provide emergency production failover without re-tooling delays.
Unlike regional assemblers reliant on imported tooling, China's mature fastener ecosystem permits rapid, in-house fabrication of specialized carbide heading dies, transfer fingers, and thread-rolling cylindrical dies within 5 to 7 days. This compresses custom prototype lead times by over 60% compared to Western European or North American standard timelines.
The business case for pre-assembled hex assembly screws goes far beyond unit purchase price. Quantifiable savings include: zero assembly line downtime caused by uncoupled washer mishandling, reduced procurement SKUs (one part number replaces two or three), and automated optical sorting guarantees under 20 PPM (parts per million) defect rates on high-speed feeds.
| Dimensional Metric / Feature | Cold Heading Standard Range | High-Precision Extended Capability | Compliance / Reference Standard |
|---|---|---|---|
| Nominal Thread Diameter | M1.6 – M12 (#0 to 1/2") | M0.8 Micro to M20 Heavy Structural | ISO 965-1, DIN 13, ASME B1.1 (2A/6g) |
| Shank Lengths Under Head | 3.0 mm – 120 mm (1/8" to 5") | Up to 250 mm for special pass-throughs | DIN EN ISO 4759-1 Class A |
| Integrated Washer Architectures | Flat, Split Spring, Helical, Wave | Conical Belleville, External/Internal Tooth, EPDM | DIN 6900 Series, ASME B18.13 SEMS |
| Material Classifications | Low/Med Carbon Steel (Class 4.8, 8.8, 10.9) | SCM435 Alloy (12.9), A2-70, A4-80, Brass | ISO 898-1, ASTM A193, ASTM F593 |
| Surface Protection & Finishing | Clear/Yellow Cr3+ Zinc, Black Oxide | Geomet, Dacromet, Zinc-Nickel (1500h Salt Fog) | RoHS, REACH, ISO 4042, ASTM F1941 |
Bridging metallurgical research with automated manufacturing to meet emerging demands in autonomous transport, renewable energy, and low-carbon assembly.
As automotive sustainability standards phase out hexavalent chromium completely and demand resistance to extreme chemical washdowns, our advanced continuous barrel Zn-Ni coating lines achieve 12%–15% nickel content. This micro-crystalline barrier resists red corrosion beyond 1,500 hours without risk of cathodic blister delamination.
Integrating piezo-electric acoustic emission sensors within our 4-die and 5-die progressive cold formers allows real-time monitoring of heading force curves. Tooling micro-cracks, blank short-feed, or wire inclusion defects are detected and automatically rejected at 250 pieces per minute, preventing compromised lots from reaching thread-rolling stations.
For high-strength Class 10.9 and 12.9 fasteners, hydrogen embrittlement represents a serious silent failure mode. Our closed-loop mesh-belt carburizing and tempering furnaces feature continuous dew-point atmospheric tracking, immediately followed by mandatory 4-to-8 hour de-hydrogenation baking cycles at 200°C–220°C per ISO 4042 specifications.
Exceeding international standards through rigorous metallurgical verification, APQP frameworks, and complete PPAP Level 3 documentation packages.
For automotive Tier-1 programs, YH Fastener provides comprehensive Production Part Approval Process (PPAP) Level 3 documentation: Design Records, Process Failure Mode and Effects Analysis (DFMEA / PFMEA), Process Flow Charts, Control Plans, Gage R&R repeatability studies, and International Material Data System (IMDS) declarations.
Our quality control laboratories house advanced metallurgical testing systems: Spectrometers for chemical grade verification, Vickers & Rockwell digital micro-hardness testers, computerized Tensile & Proof Load machines, X-Ray fluorescence (XRF) coating thickness analyzers, and automated computerized torque-tension analyzers complying with ISO 16047.
Our dedicated application engineering group works across European, American, and Asia-Pacific time zones to review 2D CAD prints and 3D STEP models, identify potential DFM (Design for Manufacturability) cost drivers, optimize head style geometries, and deliver comprehensive formal engineering quotes within 24 hours.
Direct answers from our metallurgical engineers on thread forms, captive washer integrity, friction management, and custom prototyping.
Complete your Bill of Materials (BOM) with precision pan washer heads, EPDM self-sealing fasteners, and metric socket screws built for demanding mechanical environments.
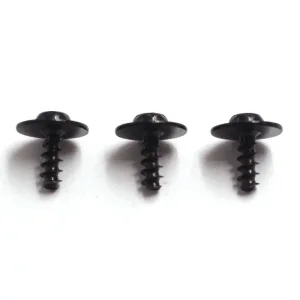
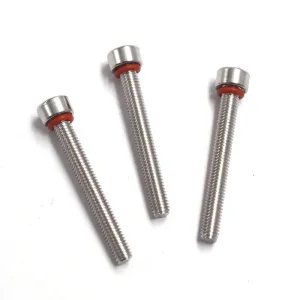

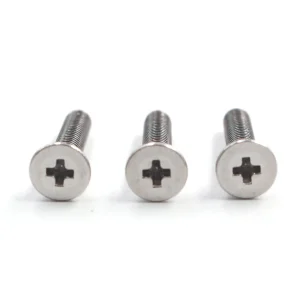
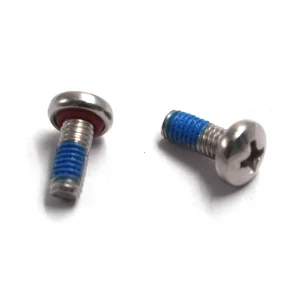
Submit your 2D engineering drawings (PDF / DWG) or 3D models (STEP / IGES). Our senior application engineering team reviews thread profile geometries, friction coatings, and clamping parameters, returning complete feasibility feedback and volume quotations within 24 hours.
