
Explore production-grade fastening components engineered in Dongguan, Shaoguan, and Wuhan facilities under ISO 9001 and IATF 16949 certified manufacturing controls.



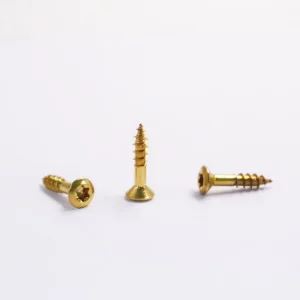
Headless set screws (also recognized as grub screws, blind screws, or socket set screws) generate pure torsional compressive clamping force without an external protruding head geometry, enabling zero-clearance, high-speed rotating mechanical unions.
Engineered with a thin annular edge that cuts deep into the mating shaft under high installation torque. Cup points maximize resistance against severe torsional slippage and axial shock loads in pulleys, gears, collars, and motor couplings where controlled surface deformation is acceptable.
Cone points transfer extreme axial holding power by seating into machined detents or v-grooves, facilitating permanent pivot hinges and fine-tuning alignments. Dog points and half-dog profiles feature cylindrical non-threaded ends configured to pilot into keyways, preventing rotational migration without galling outer threads.
Flat points (DIN 913 / ISO 4026) seat securely against ground flats, thin-walled tubing, or surface-hardened shafts without introducing localized micro-cracking or marring. For violent cyclic reversal environments, our knurled cup points provide mechanical interlock cutting edges to overcome harmonic loosening.
| Dimensional & Mechanical Parameters | Standard Specification Range | Automotive / Precision Custom Grade |
|---|---|---|
| Nominal Diameter Range | M1.2 to M24 (Metric) | #0 to 1" (UNC/UNF Imperial) | Micro-diameters from M0.8 (Precision Watch & Medical Optic standards) |
| Internal Drive Profiles | Hexagon Socket (Allen), Slotted, Torx / Six-Lobe (ISO 10664) | Tamper-Resistant Pin-in-Torx, Spline, Custom Internal Polygon Drive |
| Raw Material Composition | Carbon Steel (45H, 12.9 Grade), Alloy Steel SCM435, SS 304 (A2-70) | Stainless Steel 316L (A4-80), Brass H59/H62, Titanium Gr2/Gr5, 17-4PH |
| Surface Engineering & Coatings | Black Oxide, Zinc Cr3+ Passivation, Nickel Electroplating | Electrophoresis Black, Dacromet, Zinc-Nickel (1500h NSS), PTFE Micro-coatings |
| Anti-Loosening Pre-Applied Patches | Optional Top Coat Liquid Sealant | 360° or 180° Blue Nylon Patch, Dri-Loc Microencapsulated Adhesive (DIN 267-27) |
In global industrial hardware procurement, navigating lead-time volatility and raw material pricing demands an integrated manufacturing ecosystem capable of multi-station high-speed cold processing.
With high-tonnage production sites established across Dongguan (Guangdong HQ), Shaoguan, and Wuhan, YH Fastener cushions overseas supply lines against localized supply disruptions while accessing China’s premier industrial steel rod reserves.
By forming headless set screws via progressive multi-station cold headers instead of high-scrap screw-machining, we optimize crystalline grain flow along the screw body, producing superior tensile properties while slashing scrap rates by up to 68%.
In-house continuous vacuum carburizing, quenching, tempering, passivating, and blue nylon pre-coating ensure every lot remains under strict traceability, preventing the hydrogen embrittlement failures frequently triggered by third-party plating shops.
Automotive assembly demands absolute pedigree. We support global tier-1 automotive, aviation, and medical accounts with complete PPAP Level 3 documentation, Material Test Reports (MTR 3.1), IMDS declarations, and RoHS/REACH compliance files.
A failed M3 headless set screw can halt a multi-million-dollar robotics line. YH Fastener bridges Chinese manufacturing economies with seamless localized western procurement expectations.
Every fastener batch passes six controlled inspection stages: raw wire optical spectrum analysis, dimensional laser micrometer inspection during heading, pitch-diameter checking post-thread rolling, micro-hardness Rockwell profiling, salt spray corrosion endurance testing, and final CCD automatic optical screening.
Our bilingual sales engineering squad offers real-time DFM (Design for Manufacturability) critiques on non-standard fasteners within 24 hours. We evaluate socket wall thickness, drive recess depth ratios, and raw material work hardening behaviors to preempt torque failure before tooling creation.
Certified to ISO 9001:2015, ISO 14001:2015, and automotive standard IATF 16949:2016. Every export shipment complies strictly with EU RoHS Directive 2011/65/EU and REACH (EC 1907/2006) chemical constraints, reinforced by barcoded lot tracing down to raw melt charges.
Engineered without bulky heads, socket set screws seat flush within tapped holes to prevent interference in tight tolerances, rotating shafts, and hermetic assemblies.
Ultra-small headless screws (M1.0 - M2.5) secure precision camera zoom modules, drone gimbal armatures, wearable sensors, and PCB mounting rails, where weight limitations and extreme spatial constraints prohibit standard machine screw heads.
Utilized extensively in EPS (Electric Power Steering) shafts, window regulator mechanisms, shift lever linkages, and sensory encoder collars. Vibration resistance is reinforced via pre-applied microencapsulated adhesives to endure automotive temperature profiles (-40°C to +150°C).
Flat and dog point grub screws lock linear guide rail stops, pneumatic cylinder stops, and rotary bearings onto ground drive spindles. Paired with hardened hex keys, they ensure rapid maintenance field adjustments without burring or recess deformation.
Machined from marine-grade 316 stainless steel, monel, or passivated A4 alloys, headless fasteners secure control valve handles, underwater instrumentation, and food processing machinery subject to regular chemical caustic washdowns.
The global precision hardware sector is shifting away from commodity pricing toward functional engineering, intelligent defect detection, and automated assembly ergonomics.
Because headless set screws lack a natural physical shoulder or protruding head, automated robotic bowl feeders frequently struggle with orientation. The latest trend combines internal hex recess orientation sensors with asymmetrical point designs (like dog points or micro-stepped tapers) to facilitate flawless robotic pick-and-place assembly at 300+ parts per minute.
Environmental standards in Europe and North America have triggered the complete elimination of hexavalent chromium coatings. Next-generation fastener treatments rely on high-thickness zinc-nickel electro-alloys sealed with organic silane topcoats, delivering upwards of 1,500 hours of neutral salt spray (ASTM B117) without causing red rust or degrading thread tolerances.
To achieve Zero-PPM targets for automotive and medical clients, modern Chinese facilities employ high-speed glass disk optical sorting machinery driven by neural-network vision systems. Every individual headless screw is screened at 800 pieces per minute for hex socket depth, thread pitch integrity, plating clumping, and point geometry.
Review our extended series of standard and drawing-based fasteners manufactured for precision performance, rapid automated assembly, and high-vibration duty cycles.

Direct technical answers to the most common engineering, metallurgical, and international logistics questions handled by our sales engineering department.
These international specifications refer exclusively to the terminal point geometry of hexagon socket headless set screws. DIN 913 is a flat point designed for flat mating faces. DIN 914 features a sharp cone point for locating into detents. DIN 915 features a cylindrical dog point to fit inside keyway grooves, while DIN 916 is a cup point engineered to bite into shafts for maximum torsional lock.
Socket stripping (cam-out) is typically caused by inadequate socket depth, poor cold-heading punch concentricity, or under-tempered core hardness. We hold internal hex tolerances within ±0.015mm, use high-carbide tooling, and ensure through-hardening to 45HRC (for alloy steel), ensuring high bit engagement without wall fracture.
Yes. We offer fully integrated in-house coating systems, applying 90°, 180°, or full 360° blue nylon patches (yielding prevailing torque per IFI 124 / DIN 267-28), as well as microencapsulated chemical adhesives (such as 3M Scotch-Grip and precote) that automatically polymerize upon thread engagement.
For standard metric/inch set screws held in our stock library, dispatch takes 3–5 working days. For custom prints requiring bespoke heading dies or special point geometries, tooling development and initial FAI (First Article Inspection) samples are typically delivered within 10–14 working days, followed by mass production within 2–3 weeks.
High-tensile fasteners (Class 10.9 and 12.9 / 45H) are vulnerable to atomic hydrogen absorption during acid pickling and electroplating. We mitigate this through strictly monitored mechanical cleaning alternatives and a mandatory post-electroplating de-embrittlement bake at 200°C–220°C for 4 to 8 hours within 4 hours of plating completion.
Every commercial export consignment ships with comprehensive traceability paperwork: EN 10204 Type 3.1 Material Test Reports (MTR), dimensional CMM inspection certificates, heat treatment hardness curves, plating thickness test reports, and RoHS/REACH compliance documentation. Automotive orders can be fully backed with PPAP Level 3 documentation packages.