Explore our precision-manufactured production lines featuring cold-headed sealing geometries, thread-locking polymers, and corrosion-resistant alloys for global Tier-1 industrial applications.
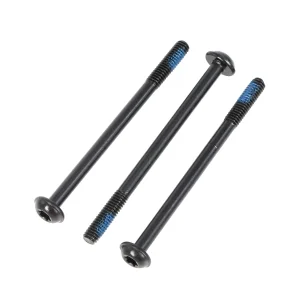
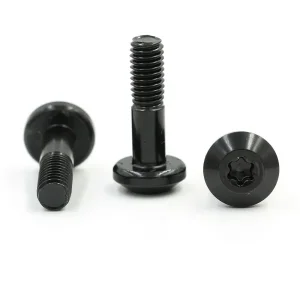
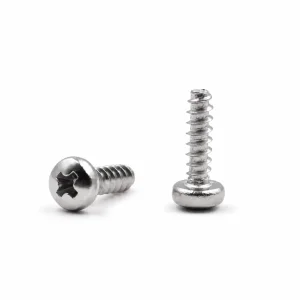
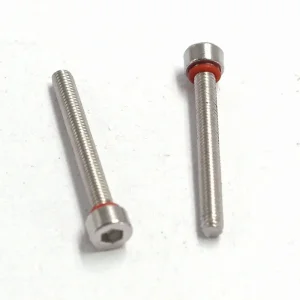

In mission-critical industrial hardware, fluid containment and ingress prevention require precision cold heading, optimized under-head groove kinematics, and high-performance elastomeric cross-sections.
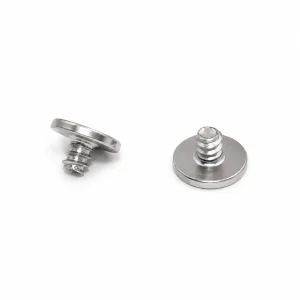
Standard mechanical fasteners rely purely on frictional tension across mating thread flanks, leaving micro-voids vulnerable to helical leakage paths. Precision sealing screws incorporate an engineered undercut groove positioned beneath the bearing surface. By matching the annular cavity volume to 90–95% of the elastomeric cross-section, the O-ring flows under axial preload without extruding beyond the head perimeter, ensuring 360-degree metal-to-metal seating and hermetic isolation up to 6,000+ PSI.
Choosing the correct polymer matrix is essential to prevent embrittlement, swell, and compression set. Yu-Huang integrates medical-grade Silicone (-60°C to +200°C), Fluorocarbon (Viton/FKM) for hydraulic fuels and synthetic oils, Nitrile (Buna-N) for universal petroleum applications, and EPDM for automotive brake fluids and outdoor ozone resistance. Integrated vulcanization options prevent ring separation during high-speed bowl feeding on automated assembly lines.
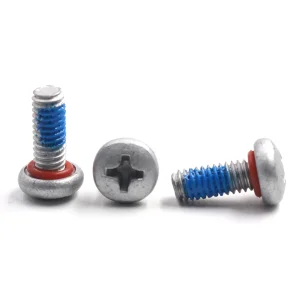
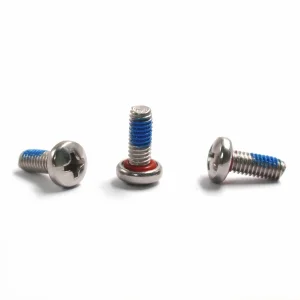
When dynamic mechanical vibrations or thermal oscillation occurs, under-head elastomeric containment must be augmented by thread locking. Pre-applied micro-encapsulated anaerobic adhesives (e.g., Dri-Loc/3M) and resilient nylon/polyamide patches provide secondary fluid dams while maintaining prevailing torque resistance. This dual barrier eliminates fastener back-out and capillary weeping across threaded blind holes and through-tapped assemblies.
Over three decades, Yu-Huang Electronics has established an agile, vertically integrated manufacturing framework that addresses structural risks in global supply chain procurement.
Unlike trading intermediaries, our 20,000 m² production facilities house raw wire spheroidizing annealing, wire drawing, cold heading, secondary CNC groove profiling, high-speed thread rolling, heat treatment, optical sort filtering, and automated elastomeric assembly under a unified quality system.
We source prime austenitic stainless steels (304, 316, 316L), duplex alloys, high-tensile carbon steels (Grade 8.8, 10.9, 12.9), and aerospace titanium (Grade 5). Every inbound wire lot undergoes spectrographic chemical analysis, tensile testing, and metallographic grain structure validation before cold forging.
Our precision die fabrication shop delivers custom heading dies, groove tools, and threading rolls within 5–7 working days. First-article samples backed by complete CMM dimensional reports enable rapid R&D turnaround for new electric vehicle, aerospace, and medical device platforms.
With primary operations in Dongguan and sister plants in Shaoguan and Wuhan, Yu-Huang provides multi-regional redundancy against localized supply disruptions. High-capacity operations ensure scalable deliveries exceeding tens of millions of precision fasteners monthly.
Select the optimal balance of elastomer properties, fastener substrate, drive recess, and environmental resistance to meet exact operating conditions.
| Elastomer / Feature | Operating Temp | Media Compatibility | Fastener Substrates | Drive Recesses | Ingress Rating |
|---|---|---|---|---|---|
| Fluorocarbon (FKM / Viton) | -20°C to +205°C | Synthetic lubricants, hydraulic oils, fuels, mild acids | 316/316L SS, A2-70, 10.9 Alloy Steel | Torx Security, Hex Socket, Pan Cross | IP68 / Subsea |
| Silicone (VMQ / Medical) | -60°C to +200°C | Ozone, weather exposure, pure water, alcohols | 304/302 SS, Titanium Gr5, Brass | Phillips, Slotted, Torx Plus, Flat Head | IP67 / Cleanroom |
| EPDM (Ethylene Propylene) | -45°C to +150°C | Brake fluid, hot water, phosphate esters, steam | 304 SS, Zinc-Plated Carbon Steel | Hex Flange, Sems Double Washer, PT Pan | IP67 / Automotive |
| Buna-N (Nitrile / NBR) | -40°C to +120°C | Petroleum oils, water, silicone greases | Case-Hardened Carbon Steel, 304 SS | Trident Tamper, Torx Pin, Hex Socket | IP66 / Enclosures |
| Pre-Applied Nylon Patch | -50°C to +125°C | Engine vibration, thermal cycling, thread weeping | Stainless Steel 304/316, Class 8.8/10.9 | All Machine & PT Tapping Recesses | DIN 267-28 Anti-Vibe |
International OEMs require strict regulatory alignment and verification. Our quality infrastructure ensures dependable compliance and documentation from raw billet to finished joint.
Our manufacturing ecosystem operates strictly under IATF 16949 automotive guidelines. Every production campaign incorporates Advanced Product Quality Planning (APQP), Process Failure Mode and Effects Analysis (PFMEA), and comprehensive Statistical Process Control (SPC) with Cpk > 1.67 targets for critical dimensions.
We provide complete Production Part Approval Process (PPAP Level 3) packages for automotive, rail, and medical platforms. Deliverables include Dimensional Results, IMDS (International Material Data System) filings, Material 3.1 Certifications, Gage R&R reports, and salt spray test certifications up to 1,500 hours without red rust (ASTM B117).
All surface plating and passivation treatments—including trivalent zinc, zinc-nickel alloys, passivated stainless steel, and fluoropolymer topcoats—fully comply with EU RoHS Directive 2011/65/EU and REACH (EC 1907/2006) SVHC. Dodd-Frank section 1502 Conflict-Free Smelter documentation is maintained across all raw material suppliers.
As power density increases and environments become harsher across clean energy, subsea, and automation markets, sealing fasteners are evolving beyond simple hardware into multifunctional engineered systems.
Next-generation direct-contact dielectric immersion cooling requires hermetic sealing against synthetic dielectric hydrocarbons at operating pressures up to 3.5 bar, driving rapid adoption of integrated fluorosilicone and Viton sealing fasteners.
Compact outdoor smart vision, LiDAR modules, and IoT compute units require sub-miniature M1.2 to M2.5 sealing fasteners that maintain an IP68 hermetic barrier without cracking thin-wall die-cast magnesium or aluminum housings.
Gaseous hydrogen containment creates severe embrittlement and micro-permeation risks. Modern sealing fasteners utilize specialized A286 or 316L stainless steel substrates paired with low-permeability EPDM elastomers to prevent atomic leakage.
High-speed robotic screwdriving demands captive O-ring systems that cannot dislodge during centrifugal sorting or pneumatic feed tubes. Chemically bonded or mechanically staked rings eliminate costly assembly line downtime.
Engineered for harsh operating environments where fastener degradation or seal failure can cause major equipment downtime or safety incidents.
ADAS cameras, millimetric-wave radar covers, and EV traction inverters require sealing fasteners that endure thermal shock (-40°C to +125°C), road salt spray, and pressure jet washing without loss of clamping force or moisture ingress.
Masthead radio units face decades of ultraviolet degradation, wind-driven downpours, and temperature extremes. Our weather-resistant silicone and fluorosilicone sealing screws ensure maintenance-free hermetic enclosures over multi-year service lives.
Dialysis systems, in-vitro diagnostic analyzers, and surgical equipment require biocompatible 316L stainless steel screws with non-outgassing silicone O-rings that resist aggressive chemical washdowns and repeated autoclave sterilization.
Straightforward technical guidance addressing torque calculations, reuse limitations, pressure thresholds, and custom tooling parameters.
The screw features a cold-forged or precision CNC-machined annular undercut channel positioned directly below the bearing surface of the head. When torqued into position, the metal shoulder makes full contact with the mating surface, limiting compressive force on the elastomer to its ideal 25–30% deflection range. The elastomer fills the engineered channel without being crushed, enabling pressure containment up to 6,000+ PSI.
Yes. Because the elastomeric seal is seated within an engineered undercut cavity rather than clamped flat across the joint interface, it avoids destructive extrusion. As long as the joint is torqued within specified engineering limits and the O-ring shows no mechanical tears or chemical swelling, the screw can typically be retightened through multiple maintenance cycles.
Bonded seal washers require separate handling, increase vertical stack height, and can slip out of alignment during automated assembly. Integrated sealing screws incorporate the elastomer directly into the cold-formed fastener head, resulting in a single component that fits flush, reduces bill-of-materials count, and operates smoothly in automated bowl feeding systems.
Yes. Yu-Huang manufactures custom fasteners ranging from micro-metric M1.0 up to M12, alongside imperial sizes from #00 to 1/2". Available drive styles include Torx (6-lobe), Torx Plus, tamper-resistant pin-Torx, triangular, slotted, cross-recess, and hex socket combinations. Tooling for custom profiles is produced in-house within 5 to 7 days.
Shipments can be provided with full quality documentation: EN 10204 3.1 Material Test Reports, dimensional inspection data, optical sorting certifications, salt spray test reports (ASTM B117), RoHS and REACH certificates of compliance, and complete PPAP Level 3 documentation packages upon request.
Explore our broader range of custom machine screws, anti-loosening nylon patch solutions, tamper-resistant security designs, and sub-assembly combinations.