Verified structural hardware deployed across high-vibration and structural joints globally.
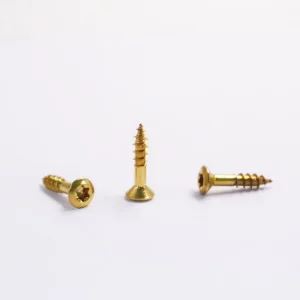
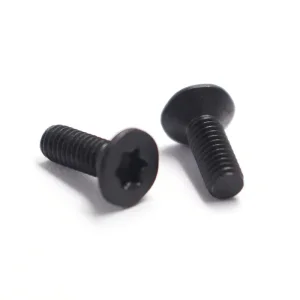
Addressing structural load distribution, zero-pre-drilling requirements, and dynamic micro-movement in mass timber engineering.
Global architectural standards require specialized coarse deep-thread geometries with high pull-out capacity to replace traditional lag bolts in Cross-Laminated Timber (CLT) assemblies without pilot drilling.
Transition from Phillips and Pozi drive systems to deep-seated Torx (Star drive) recesses to mitigate bit slip, lower axial installation force, and eliminate cam-out failure during high-torque machine installations.
The proliferation of composite woods, MDF, and HDF requires aggressive cutting notches (Type 17 points) that ream timber grain without causing substrate swelling, lateral splitting, or surface blowout.
Calibrating shank design, knurling reamers, and alloy ductile strength across specific microclimates and industrial assemblies.
Requires double-thread structures with reverse top threads to sink timber flush, treated with Class 3 or 4 Ruspert coatings capable of surviving 1,000 to 1,500 hours of neutral salt spray testing.
Flat countersunk heads with under-head cutting nibs that machine their own seating hole into particle boards and melamine surfaces without tearing laminated edges or demanding post-assembly reaming.
Structural timber framing applications in high-shear coastal zones demanding optimized case-hardening depths (0.10–0.25 mm) to combine surface hardness with a ductile, bendable core (minimum 45° bend angle).
Specialized austenitic A2-70 (AISI 304) and A4-80 (AISI 316) screws passivation-treated for teak, oak, and chemically treated wood where tannic acids and chlorides accelerate galvano-chemical deterioration.
A multi-site manufacturing footprint across Dongguan, Shaoguan, and Wuhan delivering unified, agile cold-heading output.
Our operations cover over 20,000 square meters. Production integrates internal wire drawing, continuous high-speed multi-station cold heading, high-precision thread rolling, and fully controlled atmospheric mesh-belt furnace heat treatment.
Holding IATF 16949, ISO 9001, and ISO 14001 credentials. Utilizing advanced automated optical screening machinery that executes dimensional tolerance and surface defect sorting down to 50 PPM thresholds.
Equipped with an internal R&D tooling laboratory. We deliver CAD/CAM modifications, produce non-standard wood fastener molds in-house within 7 working days, and provide verified sample batches within 15 days.
Comprehensive engineering matrices cross-referencing head configurations, metallurgic grades, and structural load values.
| Category | Material Alloy | Surface Hardness | Corrosion Shielding | Primary Industrial Use |
|---|---|---|---|---|
| Type 17 Cut Point | AISI 1022A Carbon Steel | 550–650 HV 0.3 | Zinc Yellow / Eco-Zinc (Cr3+) | Solid Hardwood Joinery, Softwood Frameworks |
| Countersunk Torx Timber | 10B21 Boron Steel | 600–700 HV 0.3 | Multi-Layer Ceramic / Ruspert 1500 Hrs | Structural CLT Jointing, Modular Frame Systems |
| Austenitic Stainless | AISI 304 (A2) / 316 (A4) | Core 210–260 HV | Passivated Acid Wash / Delta Seal | High-Tannic Cedar, Exposed Marine Boardwalks |
| Waxed Low-Torque Series | Case-Hardened Carbon | 500–580 HV 0.3 | Waxed Zinc Plating | High-Speed Automated Industrial Cabinetry Lines |
Application of sub-micron dry waxing technology directly to timber threads to lower insertion torque requirements by 35%, extending cordless battery lifecycles on mass job sites.
Advanced dual-heat processing yielding ultra-hard thread crowns (preventing thread burn) merged with an elastic, highly ductile central core built to flex during structural timber deflection.
Total phase-out of hexavalent/trivalent chromates in favor of zero-VOC inorganic silicate dip-spin matrices exceeding 2,000 hrs ASTM B117 salt spray endurance without risk of hydrogen embrittlement.
Complete traceability documentation, certified testing procedures, and environmental compliance for global markets.
Testing for European structural timber components covering characteristic yield moment, withdrawal parameters, head pull-through capacity, and minimum tensile strength limits.
Direct third-party lab documentation (SGS, TÜV Rheinland) certifying the absence of hazardous elements, heavy metals, or toxic plasticizers across all zinc, phosphate, and polymer finishes.
Provision of certified inspection documents (3.1 inspection certificates) matching incoming steel coil heats, case carburization records, mechanical shear data, and plating batch audits.
In-depth responses from our application engineering division on fastener design and material performance.
Explore the full spectrum of our cold-formed industrial fasteners, O-ring sealing assemblies, and precision thread-forming products.