

Precision Cold-Heading Engineering, Sub-Micron Thread Profiling, and Global Industrial Procurement Solutions for High-Stress Assembly Systems
Explore our certified batch-manufactured self tapping pan heads, precision thread-forming screws, and dynamic sealing solutions engineered for international OEM production lines.





Strategic analysis of multinational supply chain architectures, total cost of ownership (TCO) optimization, and manufacturing risk mitigation.
Global original equipment manufacturers (OEMs) and contract electronics manufacturers (CEMs) face escalating supply volatility. Enterprise sourcing strategies now mandate tier-1 fastener manufacturing partners capable of vertically integrated production: from wire rod drawing and cold heading to automated optical screening and multi-stage anti-corrosion passivation.
The acceleration of Industry 4.0 robotic insertion lines demands tighter geometric tolerances. Pan head self tapping fasteners must maintain absolute concentricity and strict drive recess recess depth consistency (Phillips, Torx, Pozi) to eliminate cam-out, bit slippage, and downtime within high-speed automated feed systems.
In safety-critical sectors like automotive powertrain control and medical electronics, fastener failure incurs astronomical warranty liabilities. Procurement contracts require comprehensive PPAP (Production Part Approval Process) Level 3 documentation, full material heat-number traceability, and sub-15 PPM sorting capabilities.
How bespoke pan head thread geometry resolves unique operational stresses across mission-critical application domains.
Engineered for lightweight plastic structural sub-assemblies and aluminum battery casing lids. Type C / F thread-cutting points deliver high stripping torque to driving torque ratios, resisting vibration under severe cyclic loading.
Micro-fastener engineering (M1.2–M3.0) using 304 and 316 austenitic stainless steel. The broad pan head profile ensures optimal load distribution across ultra-thin polycarbonate or ABS housings without causing stress crazing.
Integrating pre-assembled under-head elastomeric sealing washers or micro-encapsulated thread sealants to maintain IP67/IP68 environmental integrity against moisture, dust ingress, and dielectric degradation.
Thread-forming PT-style screws designed with 30° flank angles to reduce radial stress within thermoplastic materials, boosting pull-out resistance and maintaining clamping force over long-term thermal cycling.
Comprehensive metallurgical properties, geometric standards, and testing verifications executed at our Dongguan, Shaoguan, and Wuhan facilities.
| Dimensional / Metrological Parameter | Standard Metrics (Metric & Imperial) | Validation / Metrology Protocol | Industrial Application Significance |
|---|---|---|---|
| Nominal Diameter Range | M1.2 to M10 (#0 to 3/8") | High-Precision Micrometer, Keyence Optical Profiler | Enables use in micro-optics, electronics, and structural frames |
| Thread Profile Geometries | Type AB, Type B, Type F, PT 30° / 48° Thread-Forming | Shadowgraph 50X Contour Analysis | Controls displacement vs. cutting action across varying substrate hardness |
| Alloy Metallurgy Options | Carbon Steel (1018, 1022A, 10B21), SS304, SS316, A2/A4 | Spectrometric Chemical Heat Composition Audit | Matches environmental corrosion limits and ultimate shear strength goals |
| Surface Hardness & Case Depth | Vickers HV 450–750, Case Depth 0.05–0.18mm | Micro-Vickers Hardness Indentation Tester | Guarantees mating thread formation without core brittleness risks |
| Drive Recess Types | Phillips, Torx (6-Lobe), Pozidriv, Hex Socket, Tamper-Proof | Go/No-Go Gauge Blocks, Digital Depth Probes | Prevents cam-out and optimizes robotic automated torque transfer |
| Corrosion Resistance Passivation | Black Zinc, Eco-friendly Geomet, Zn-Ni Plating, Blue Ruspert | ASTM B117 Neutral Salt Spray Testing (24h to 1000h+) | Protects fasteners in harsh marine, chemical, and outdoor installations |
Addressing the shifting engineering frontiers: ultra-high-strength micro fasteners, composite joining mechanisms, and sustainable decarbonized supply systems.
Traditional tapping screws cause delamination in composite structures. Our R&D is scaling modified parabolic thread-forming roots that compact rather than sever internal matrix fibers, eliminating the need for brass inserts.
Upgrading automated manufacturing lines with 360-degree laser telecentric cameras tied to neural networks to detect micro-cracks, incomplete plating coverage, and thread burrs down to single-digit micron tolerances.
Achieving carbon-neutral cold-heading lines through 100% post-industrial steel scrap circular loops, bio-based cold-heading lubricants, and non-cyanide, low-energy electrolytic bath chemistry.
Providing seamless, fully documented regulatory pathways for worldwide cross-border delivery across Europe, the Americas, and the Asia-Pacific region.
Every fastener batch is certified to RoHS, REACH (SVHC), and Conflict Minerals regulations. Complete full-substance declaration data sheets (IMDS records) can be integrated directly into your automotive compliance systems.
To shield clients from unexpected demand surges, we manage Vendor-Managed Inventory (VMI) and buffer safety-stock agreements at regional staging centers, guaranteeing on-time line replenishments under JIT (Just-In-Time) setups.
Our bilingual sales engineering teams in Dongguan deliver 24-hour drawing evaluations, design-for-manufacturability (DFM) reports, and tooling simulations before production begins.
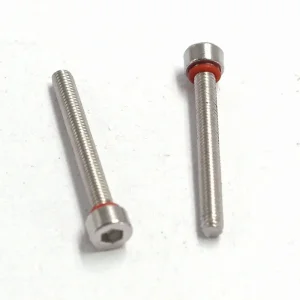
Complementary hardware solutions including spring plungers, custom socket cap screws, and high-tensile machine components manufactured directly by YH Fastener.
In-depth responses covering mechanical specifications, tooling schedules, material traceability, and custom OEM manufacturing workflows.
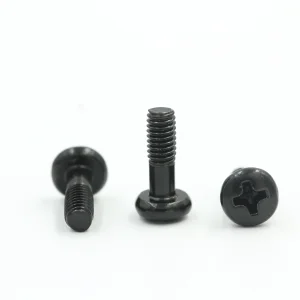
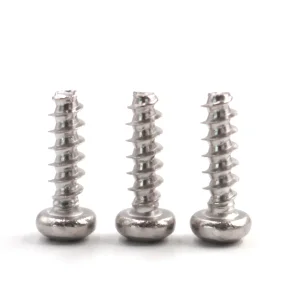
Pan heads feature a broad, flat bearing surface combined with low-profile rounded outer edges. This design maximizes clamping pressure distribution over a wider surface area without gouging delicate parent materials such as thin-gauge sheet metals, polymers, and PCBs. Unlike countersunk fasteners, pan heads require no chamfered preparation, reducing tooling costs, preserving joint structural integrity, and supporting automated optical orientation checks on assembly lines.
Thread-cutting screws (e.g., Type 1, Type F, Type 23) incorporate specialized flutes or cutting slots that remove parent material as chips, generating clear mating threads within hard plastics and metals. Thread-forming screws (e.g., PT screws, trilobular geometries) yield and deform the parent material into thread flanks under compressive displacement. Thread-forming fasteners generate zero debris, provide higher back-out torque retention, and create an interference fit that resists vibration-induced loosening.
Standard quality documentation packages include full Material Mill Test Reports (MTR / EN 10204 3.1 certification), complete dimensional inspection reports (CMM / 2D optical profiles), Vickers / Rockwell case hardness depth gradients, and Salt Spray Corrosion Test Logs per ASTM B117. For automotive-tier and medical accounts, our facilities supply complete PPAP Level 3 documentation, including DFMEA/PFMEA records, control plans, and Gage R&R repeatability audits.
Yes. Our in-house tool and die facility produces bespoke tooling for non-standard head heights, modified collar under-cuts, non-traditional thread pitches, captive washer grooves (SEMS designs), and specialized drive configurations (security pin-in-Torx, triangular heads, micro-slotted). Rapid prototype samples are typically delivered within 7 to 10 working days upon 2D/3D drawing sign-off.
During the acid pickling and electroplating processes (such as zinc or zinc-nickel coatings), atomic hydrogen can migrate into high-strength carbon steels (especially parts heat-treated above 320 HV). We mitigate hydrogen embrittlement by immediately transferring coated lots into continuous baking ovens at 200°C–220°C for 4 to 8 hours. Batches undergo subsequent sustained-load testing to verify mechanical core ductility before packaging.