Direct factory-manufactured cold-formed fastening components featuring tight tolerance thread pitches, anti-loosening chemical patches, and high-integrity surface plating solutions.



While metric hardware dominates European and Asian consumer electronics, the Unified Thread Standard (UTS)—encompassing Unified Coarse (UNC), Unified Fine (UNF), and Unified Extra Fine (UNEF) profiles—remains the fundamental structural backbone of North American aerospace, heavy automotive, defense systems, and fluid-power automation.
Machine screws designed under ASME/ANSI B18.6.3 mandate meticulous head proportions, recess depths, and root radius controls. Cold forging dies are engineered to impart continuous metallurgical grain flow through the critical head-to-shank junction, vastly mitigating catastrophic shear failures under high dynamic fatigue.
For standard assembly efficiency, Unified Class 2A external threads allow an intentional clearance allowance to accommodate industrial surface plating (zinc, cadmium, nickel). For critical mil-aero or medical instruments, Class 3A eliminates this allowance to maximize thread engagement and preload consistency.
Rather than severing grain structures through lathe cutting, YH Fastener utilizes multi-die cold thread rolling. This work-hardens the flank and root of the screw thread, delivering up to 25% higher fatigue strength and smoother surface finishes (Ra 0.4 µm) that prevent galling.
Navigating global tariff shifts, domestic reshoring policies, and the Total Cost of Ownership (TCO) in tier-one and tier-two industrial assembly operations.
Modern procurement executives can no longer rely on single-region production. While North American OEMs demand inch fasteners (such as #2-56, #4-40, #6-32, #8-32, #10-24, 1/4-20, and 3/8-16), domestic manufacturing capacity remains constrained by high tooling changeover costs and labor shortages. Our multi-plant operational model across Dongguan, Shaoguan, and Wuhan provides the critical capacity, precision heading speed, and export scalability needed to maintain continuous inventory buffers.
The cost of a fastener is rarely its invoice unit price; it is the cost of downtime on automated assembly lines caused by stripped drive sockets, eccentric heads, or defective threads. Implementing fully automated multi-sensor laser and CCD vision sorting ensures defect rates under 15 PPM, protecting automotive robot cells and high-speed feeder systems from mechanical jam-ups.
| Nominal Size | Major Dia. (Inch) | Coarse (UNC TPI) | Fine (UNF TPI) | Tensile Stress Area (sq in) | Recommended Drive System | Standard Material Grades |
|---|---|---|---|---|---|---|
| #2 (.086) | 0.0860" | 56 TPI | 64 TPI | 0.00370 sq in | Phillips #1 / Torx T6-T8 | 304 / 316 SS Grade 2 Carbon |
| #4 (.112) | 0.1120" | 40 TPI | 48 TPI | 0.00604 sq in | Phillips #1 / Torx T8-T10 | 18-8 SS Case Hardened 1022 |
| #6 (.138) | 0.1380" | 32 TPI | 40 TPI | 0.00909 sq in | Phillips #2 / Hex Socket 7/64" | Grade 5 Alloy 316L SS |
| #8 (.164) | 0.1640" | 32 TPI | 36 TPI | 0.0140 sq in | Phillips #2 / Torx T15 | Grade 8 (High Tensile) |
| #10 (.190) | 0.1900" | 24 TPI | 32 TPI | 0.0175 sq in | Phillips #2 / Hex Socket 1/8" | A2-70 / A4-80 Grade 5/8 |
| 1/4" (.250) | 0.2500" | 20 TPI | 28 TPI | 0.0318 sq in | Phillips #3 / Torx T25-T30 / Hex | SAE J429 Gr 8 316 Marine SS |
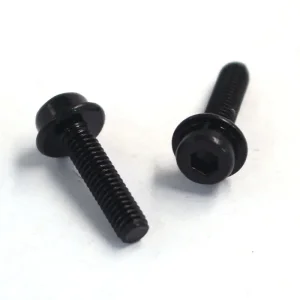
| 5/16" (.3125) | 0.3125" | 18 TPI | 24 TPI | 0.0524 sq in | Hex Flange / Socket Head 1/4" | Structural Heat-Treated |
Real-world mechanical performance depends on matching drive geometry, base alloy, thread pitch, and surface protection to the specific environmental operating stress.
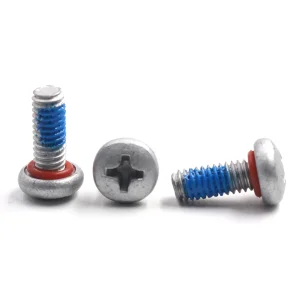
Unified inch screws such as 10-32 UNF and 1/4-28 UNF are standard across North American flight decks, avionics rack trays, and actuator housings. Formed from vacuum-melt 316 stainless steel or A286 high-temperature superalloys, these screws incorporate mil-spec Class 3A thread tolerances and pre-applied blue/yellow polyamide locking patches to resist acoustic and rotational loosening under extreme G-force vibration.
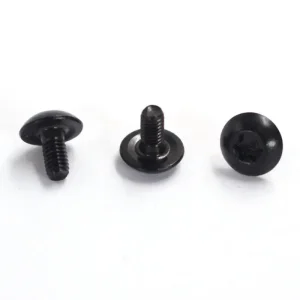
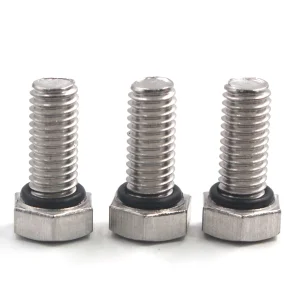
Electric vehicle (EV) battery packs and charging enclosures require specialized pan-head and truss-head screws with under-head fluorosilicone sealing rings (O-rings) to achieve IP67/IP68 ingress protection against moisture and electrolytic fluid. Pre-assembled SEMS washer assemblies cut assembly cycle times in half, preventing internal mechanical short-circuits during high-speed robotic chassis integration.
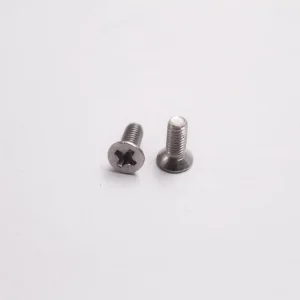
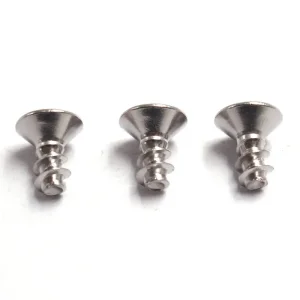
Micro-inch machine screws (#0-80, #2-56, #4-40) in 82-degree countersunk flat-head styles provide flush mounting for printed circuit boards, aluminum front plates, and handheld military diagnostic tools. Non-magnetic austenitic 304 stainless steel guarantees zero electromagnetic interference (EMI) with high-frequency RF transmission boards.
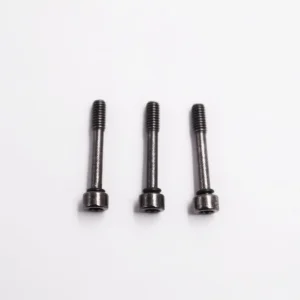
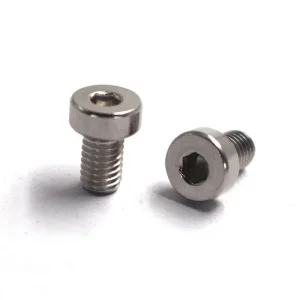
In harsh CNC machining centers, stamping dies, and industrial hydraulic valves, Grade 8 and alloy steel socket-head cap machine screws withstand elevated torque settings without head stripping. Integrated spring plungers and hardened locator detents allow rapid modular retooling without losing centerline datum alignment.
B2B fastener procurement requires complete traceability, material test reports (MTR), and adherence to statutory international environmental directives.
Every cold-heading and thread-rolling lot is subjected to Statistical Process Control (SPC) charting. Pre-production Part Approval Process (PPAP Level 3) packages, including Failure Mode and Effects Analysis (FMEA) and Control Plans, are routinely provided to tier-one global suppliers.
All electroplated finishes, passivations, and base alloys comply strictly with EU RoHS Directive 2015/863 and REACH SVHC regulations. Raw wire materials are verified 100% free from conflict-region minerals, backed by verifiable 3.1 chemical analysis inspection certs.
Our in-house metrology lab executes neutral salt spray testing (ASTM B117) exceeding 1,000+ hours without red rust for zinc-nickel and Dacromet coatings. Destructive torsional yield testing, Rockwell/Vickers hardness checks, and optical comparator contour analysis ensure flawless joint reliability.
How advanced cold-forging digital twins, nanotechnology coatings, and integrated micro-positioning elements are driving next-generation hardware designs.
Eliminating trial-and-error tooling modifications by simulating continuous metal flow, effective strain, and heading die stress concentrations. This delivers sub-micron concentricity tolerances on non-standard custom head designs while lowering tooling lead times by 40%.
Transitioning from traditional hexavalent passivations to inorganic micro-zinc flake coatings and trivalent black sealants. These achieve exceptional salt-spray longevity while maintaining pitch diameter tolerances on ultra-fine inch threads (#2-56 and #4-40) without requiring tap re-threading.
Pioneering micro-recess RFID tagging and acoustic preload validation for critical infrastructure and offshore renewable equipment, allowing real-time clamp force monitoring without manual torque wrench verification.
Critical technical and logistical insights addressing unified thread standards, custom cold-heading tooling, and volume OEM purchasing.
Explore our specialized portfolio of Torx-drive, countersunk, sealing O-ring, and micro-inch industrial hardware built for demanding environments.