
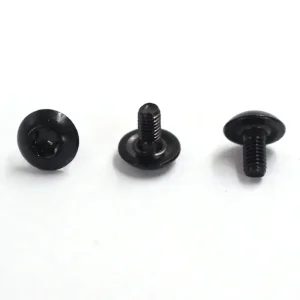
Manufactured under stringent IATF 16949 and ISO 9001 protocols with full microstructural and torque verification.
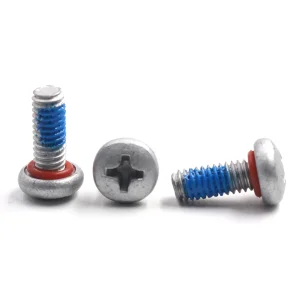

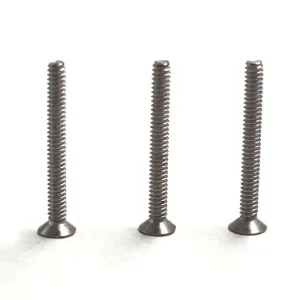
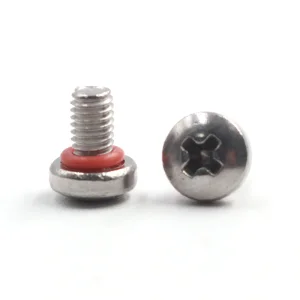

A comprehensive examination of metallurgical optimization, advanced surface passivation, and automated robotic assembly dynamics.
Modern cold-forging leverages low-carbon cold-heading quality (CHQ) AISI 1022A boron-enhanced wire rod. Controlled case-carburizing yields an exceptionally hard outer surface layer (HV 450–650) to penetrate sheet metals seamlessly, while retaining a ductile core (HV 270–390) that prevents catastrophic shear failure under dynamic torsional loads.
Global environmental mandates (RoHS, REACH, and ELV) have driven the transition from hexavalent coatings to Cr3+ trivalent zinc, zinc-nickel alloy platings, and organic-inorganic zinc flake treatments (Geomet/Dacromet). These eco-friendly coatings reliably withstand 480 to 1,500 hours of neutral salt spray testing (ASTM B117) with zero hydrogen embrittlement.
Industry 4.0 automated screwdriving robotic systems demand zero cam-out and tighter drive recess tolerances. The industry has shifted significantly toward deep Phillips-drive and 6-lobe Torx/Hexalobular geometries, minimizing bit slippage, reducing axial seating thrust, and prolonging robotic drive-bit lifecycles over multi-million-cycle production runs.
Addressing the critical supply-chain vulnerabilities of OEM/ODM industrial buyers across Europe, North America, and APAC.
Global manufacturing procurement mandates continuous supply with guaranteed multi-plant redundancy. With manufacturing hubs in Dongguan, Shaoguan, and Wuhan covering over 20,000 m², YH Fastener ensures complete insulation against localized line interruptions and regional geopolitical constraints.
Procurement directors optimize working capital via Just-In-Time (JIT) releases and Vendor-Managed Inventory (VMI) frameworks. Pre-allocated raw material buffers and scheduled production runs support rapid 24-hour engineering dispatch and compressed bulk fulfillment cycles.
Mission-critical deployments require comprehensive documentation: Production Part Approval Process (PPAP) Level III, Initial Sample Inspection Reports (ISIR), Material Mill Certificates (EN 10204 3.1), and chemical compliance testing for every cold-heading production heat.
Engineered thread configurations calibrated for sheet metal, polymer substrates, and electrical assemblies.
| Target Sector | Material & Head Spec | Thread Geometry | Recommended Coating | Functional Performance Advantage |
|---|---|---|---|---|
| Automotive Electronics | AISI 1022A Carbon Steel, Pan Head, Torx Plus | Type F / Trilobular Thread Forming | Zinc-Nickel (12–15% Ni) + Clear Topcoat | Eliminates chips; resists extreme under-hood vibration and temperature cycling (-40°C to 150°C). |
| Telecommunications & 5G | Low Carbon Steel, Ultra-Low Pan Head | Fine Machine/Tapping Thread Class 6g | Black Trivalent Zinc Passivation | Optimized low-clearance envelope inside antenna modules; minimizes RF harmonic interference. |
| Industrial HVAC & Enclosures | Case-Hardened Carbon Steel, Phillips Pan | Type AB High-Low Coarse Pitch | Zinc Flake (Geomet 321 / 500) + EPDM Washer | Zero water/moisture capillary action; over 1,000 hrs ASTM B117 salt spray protection. |
| Consumer Appliances | High-Ductility Carbon Steel, Phillips Pan | PT Thread (30° Flank Angle) for Plastics | Eco-Friendly Bright Zinc Plated | Reduces radial boss bursting in polycarbonate/ABS mouldings while maximizing strip-to-drive torque ratios. |
| Power Infrastructure | Grade 8.8 Equiv. Heat-Treated Carbon Steel | DIN 7981 / ISO 7049 Standard Tapping | Hot-Dip Galvanized / Mechanical Zinc | Withstands high electrical grounding contact pressure without head shearing or surface galling. |
Combining rigorous institutional certifications with rapid on-site and technical engineering diagnostics.
Our operations follow ISO 9001, ISO 14001, and IATF 16949 automotive quality management certifications. From cold heading and slotting to carburizing and surface deposition, every run undergoes strict Statistical Process Control (SPC) with automated Cpk evaluation.
All finished fasteners adhere to international environmental and chemical restrictions, fully verified against RoHS Directive 2011/65/EU and REACH (EC 1907/2006) SVHC declarations. Conflict-mineral-free assurances are certified on every raw metal delivery.
Senior fastener application specialists provide drawing evaluations, FEA clamping load analyses, and joint failure troubleshooting within 24 hours. We help calculate optimal pilot-hole diameters to prevent boss cracking and strip-out issues.
Forecasting manufacturing intelligence, AI quality assurance, and lightweight structural joining through 2030.
Integrating high-speed 360-degree machine-vision sorters capable of analyzing thread pitch consistency, head concentricity, and drive recess depth at speeds exceeding 1,200 parts/min, reducing zero-defect field allowances below 5 PPM.
Next-generation thread-rolling topologies tailored for hybrid aluminum-to-composite and thin-gauge multi-metal sheets. Flow-drilling-assisted point geometries create internal extruded collars without requiring pre-punched pilot holes.
Emerging graphene-modified thin-film conversions and dry-lubricant micro-encapsulations optimize thread-engagement friction coefficients (μ = 0.10–0.15), preventing thermal stick-slip during high-speed robot assembly.
Precision-threaded, custom-engineered components available for volume supply contracts and custom OEM runs.




Authoritative guidance addressing common specification challenges, failure modes, and production lead times.