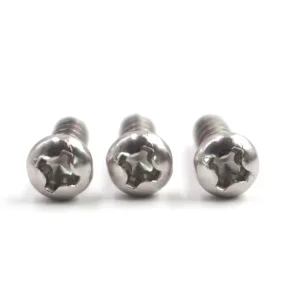
Engineered cold-formed fasteners precision-manufactured under IATF 16949 / ISO 9001 certified operations for automotive, electronics, and precision robotics platforms.
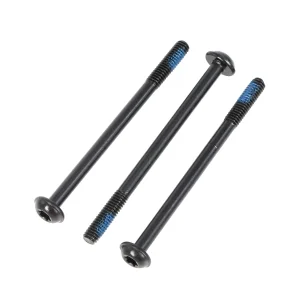

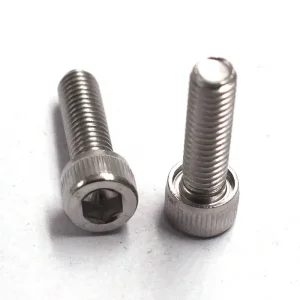

Why Tier-1 OEM assemblers are transitioning away from cross-recess drives to ISO 14583 Torx pan-head systems to guarantee torque transmission integrity and eliminate assembly fatigue.
Traditional Phillips recesses were engineered during early industrial eras specifically to force driver disengagement to avoid over-tightening. In automated CNC and robotic assembly cells, this cam-out mechanism is catastrophic—causing metallic shavings, tool wear, and surface marring. The six-lobe Torx drive generates zero cam-out axial force, preserving driver bit lifecycle up to 10× longer.
Unlike hex socket systems that present a 60-degree contact angle subject to rapid corner rounding under high clamp-loads, hexalobular geometries transfer torque across a virtually perpendicular 15-degree driving angle. This geometric alignment radically curtails radial outward bursting stress inside the screw head, enabling higher preload tightening without head fracture or recess deformation.
The standard pan head profile (ISO 14583 / DIN 7985) offers an optimized under-head bearing surface area. This wide surface distributes axial clamp loads uniformly across delicate substrates like aluminium enclosures, PCBA assemblies, and composite brackets, effectively mitigating localized galling, material deformation, or creep relaxation across dynamic thermal cycles.
In high-speed robotic screwdriving operations, torque-to-tension conversion is heavily impacted by head frictional diameter. The pan head design standardizes the contact diameter relative to nominal thread pitch, resulting in an exceptionally narrow torque scattering coefficient (k-factor variance within ±0.03 when coupled with specialized lubricating topcoats).
Navigating tier-1 supply chain constraints, automated production yield metrics, and end-to-end metallurgical traceability from raw billet to factory delivery.
Global procurement directors recognize that fastener purchase price accounts for less than 15% of total assembly cost. The remainder is consumed by feeder misfeeds, bit replacement, robotic stoppages, and thread rework. Precision Torx machine screws with concentricity tolerances under 0.05mm provide significant bottom-line operational savings.
With blow-feed and vacuum-pick automated systems in smart factories, any dimensional flash, head-to-shank misalignment, or metal burr can cause catastrophic line halts. Our cold heading dies undergo strict optical wear monitoring, paired with 100% automated eddy-current and optical sorting machines to assure strict zero-defect PPM benchmarks.
Automotive and high-reliability aerospace systems mandate comprehensive documentation. We deliver complete Advanced Product Quality Planning (APQP) packages, including Process Flow Charts, Design/Process FMEA, Dimensional Results, Material Test Certifications (MTR EN 10204 3.1), and Initial Sample Inspection Reports (ISIR).
Enterprise resilience hinges on seamless inventory coordination. We support customized EDI connectivity, Vendor-Managed Inventory (VMI) frameworks, safety stock buffers in localized fulfillment hubs, and barcode/QR lot serialization down to each specific packaging carton for rapid traceability.
Comprehensive comparative matrices for OEM project engineers, product designers, and procurement managers specifying Torx pan-head machine screws.
| Feature Parameter | ISO 14583 (Metric Standard) | DIN 7985 (Historical Torx/Cross) | ASME B18.6.3 (Inch Unified) |
|---|---|---|---|
| Nominal Range | M1.6 to M10 (Custom Micro M0.8+) | M2.0 to M8.0 | #0-80 through 3/8"-16 UNC/UNF |
| Head Diameter Profile | Optimized cylindrical radius profile | Slightly wider crowned profile | Engineered pan head contour |
| Drive Engagement | Hexalobular Internal (T5 to T50) | Hexalobular or Type H/Z Cross | Torx Size T6 to T45 / Torx Plus |
| Thread Classes | ISO 965-2 6g medium fit | Medium tolerance Class 6g | Class 2A standard / Class 3A tight |
| Tensile Strength Options | Class 4.8, 8.8, 10.9, 12.9; A2-70, A4-80 | Class 4.8, 5.8, 8.8; A2, A4 | Grade 2, 5, 8; 18-8, 316 Stainless Steel |
| Corrosion Protection | Zinc-Nickel (1000h NSS), Geomet 500, Passivated | Electro-zinc plating, Cr3+ passivated | Zinc Clear/Yellow, Black Oxide, Magni |
Selecting the ideal alloy matrix ensures maximum fatigue life, prevents galvanic corrosion, and maintains clamping force in extreme operating environments.
Standard for consumer electronics, household appliances, and light automotive assemblies. Excellent general corrosion resistance with non-magnetic properties when properly cold worked and solution-annealed. Yield strength typically exceeding 450 MPa.
Formulated with 2-3% Molybdenum content to resist pitting from chlorides and industrial chemical washdowns. Widely deployed in marine electronics, outdoor 5G base stations, and medical diagnostic instrumentation where zero surface oxidation is tolerated.
Class 8.8, 10.9, and 12.9 quenched and tempered alloy steels. Engineered for structural machine elements, heavy engine bays, and powertrain mountings where exceptional clamp-loads, high shear resistance, and structural joint stiffness are paramount.
How specialized OEM Torx pan-head machine screws resolve severe environmental, mechanical, and regulatory challenges across high-growth global sectors.
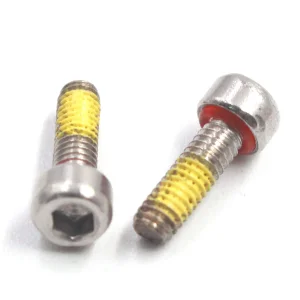
Electric vehicle battery packs experience harmonic vibration, rapid thermal cycles (-40°C to +85°C), and stringent flame-resistance requirements. Our solutions integrate SEMS lock-washers or micro-encapsulated thread-locking adhesives with ISO 14583 pan heads to maintain constant clamp force, eliminate thermal back-out, and prevent battery enclosure breach.
High-density rack servers require low-profile, clean fasteners free from volatile organic compounds or oil residue. Our ultra-clean passivation and ultrasonic solvent degreasing processes ensure particulate-free fasteners that preserve sensitive microcircuits, optical links, and electromagnetic shielding enclosures.
Joint assemblies on six-axis robotic arms demand micro-toleranced fasteners capable of resisting dynamic shear reversing loads. We manufacture custom shoulder and precision pan-head configurations with Torx Plus profiles that optimize stress transfer during high-acceleration kinematic reversals.
Exposed to extreme UV, oceanic salt mist, and sulfurous atmospheres, renewable energy hardware demands zinc-flake coatings (Geomet / Dacromet) exceeding 1,500 hours of salt spray testing without red rust formation, preventing galvanic degradation against aluminium framing.
Non-magnetic, bio-compatible stainless steels (316L / 1.4404) machined and cold formed in ISO Class 7 cleanroom environments. Precision electropolishing removes microscopic surface irregularities, inhibiting bacterial biofilm formation on surgical instruments and laboratory centrifuges.
High-volume consumer hardware requires ultra-miniature Torx pan-head machine screws (sizes M0.8 to M2.0). Deep-recess drive retention guarantees vacuum nozzle pickup alignment, accelerating unit throughput in automated electronics surface mounting.
Ensuring complete regulatory conformity across North American, European, and Asia-Pacific industrial manufacturing jurisdictions.
All finished fasteners are certified 100% compliant with RoHS Directive (EU) 2015/863 and REACH Regulation (EC) No 1907/2006 for Substances of Very High Concern (SVHC). Certified hexavalent chromium-free (Cr6+) surface finishes eliminate toxic ecological footprints in accordance with EPA and WEEE requirements.
Yu-Huang implements rigorous auditing following the OECD Due Diligence Guidance and Section 1502 of the Dodd-Frank Act. Raw wire rod sources are verified 100% conflict-free across 3TG elements (tantalum, tin, tungsten, gold), backed by complete annual CMRT declarations.
Fasteners with core hardness >320 HV (Class 8.8 and higher) undergo immediate de-embrittlement baking at 200°C–230°C within 4 hours post-acid pickling or electroplating, strictly adhering to ISO 4042 and automotive OEM engineering standards to prevent catastrophic delayed brittle failure under static load.
Yu-Huang Fastener maintains fully unified manufacturing capabilities across its Dongguan, Shaoguan, and Wuhan facilities spanning over 20,000 m². Every single production batch is serialized with full heat-number traceability back to raw wire rod coils, ensuring prompt, accountable root-cause resolution for engineering procurement teams.
Anticipating next-generation manufacturing breakthroughs, smart assembly integrations, and low-carbon metallurgical frameworks.
Adoption of elliptical rib profiles providing an authentic 0-degree drive angle, maximizing bit engagement life and enabling high-speed off-axis robot tool entry without mechanical jam.
Transition from liquid lock-thread compounds to dry, micro-encapsulated polyamide and reactive acrylic patches, eliminating outgassing inside sensitive optical and electronic sensor housings.
Micro-laser etched 2D matrix identifiers directly etched onto pan-head crowns for mission-critical aircraft and rail infrastructure, enabling lifetime maintenance and torque lifecycle auditing.
Adoption of ultra-low carbon footprint electric-arc furnace (EAF) wire rods derived from 95%+ recycled scrap, dropping the embedded carbon dioxide equivalent below 0.8 kg CO2e/kg finished fastener.
Integration of piezoresistive micro-thin film coatings beneath pan-head bearing collars that relay real-time clamping preload data wirelessly during high-stress structural operations.
Authoritative technical answers to common queries raised by quality assurance engineers, mechanical designers, and global procurement professionals.
Explore our specialized portfolio of self-sealing IP67 fasteners, custom stainless cold-forged screws, and high-strength industrial machine components.