Explore our cold-formed PT thread screws, integrated sealing fasteners, and micro-recessed machine assemblies manufactured to rigorous IATF 16949 automotive standards.
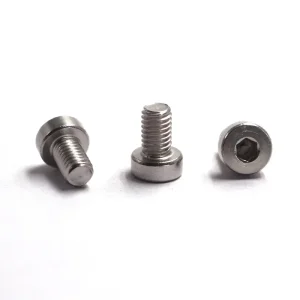

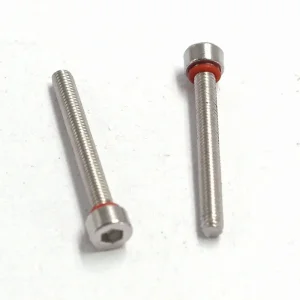
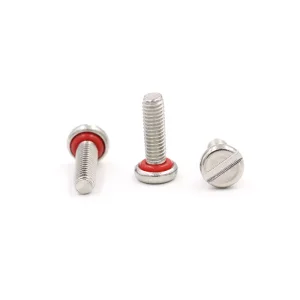
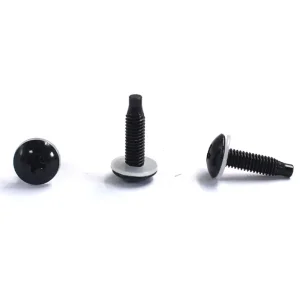
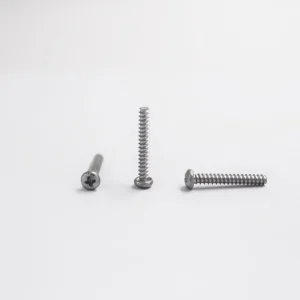

Why conventional 60° machine and sheet metal screws fail catastrophically in thermoplastic substrates, and how engineered 30° flank thread profiles deliver optimal clamp load retention.
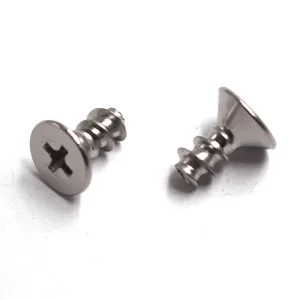
Standard tapping screws utilize a symmetrical 60° thread profile that generates excessive outward radial displacement force ($F_r = F_a \cdot \tan 30^\circ$). The PT screw features an optimized 30° included angle, drastically decreasing radial hoop stress by over 50%. This prevents plastic boss cracking, crazing, and dimensional wall distortion, even in thin-walled or low-ductility polymers.
By recessing the root diameter and expanding thread pitch, the PT design leaves a substantially greater volume of undisturbed thermoplastic between consecutive thread flights. This thick plastic shear zone resists tensile pull-out forces and dynamic creep, increasing stripped-to-drive torque ratios ($T_s / T_d$) safely past the 3:1 safety margin necessary for automated screwdriving lines.
The specialized thread-forming crest smoothly displaces polymer molecules via localized viscoelastic flow rather than destructive abrasive cutting. Friction-induced heat during high-speed automated assembly is controlled, minimizing thermal degradation of surrounding amorphous or semi-crystalline polymers like ABS, PBT, Polycarbonate, and Nylon 66.
In-depth technical parameters for structural fastening across mission-critical sectors. Compare design ratios, boss dimensions, and assembly criteria.
Modern industrial equipment design has shifted irreversibly from dense die-cast metal alloys to engineered engineering thermoplastics and composite blends. From lightweight Electric Vehicle (EV) battery management modules to hermetically sealed solar microinverters, engineers face a critical dilemma: preventing joint relaxation under thermal cycling without escalating production scrap caused by stripped plastic bosses.
As an OEM PT thread self-tapping screw manufacturer, Yu-Huang Electronics Dongguan Co., Ltd. (YH Fastener) provides empirical boss calculation support, custom thread pitch adjustments, and specialized micro-coatings that allow direct assembly into virgin and glass-filled thermoplastics without tapping inserts or brass ultrasonic grommets.
| Polymer Class & Trade Name | Common Industrial Application | Recommended Boss Ratio (d_b / d) | Recommended Pilot Hole (d_h / d) | Key PT Screw Characteristic |
|---|---|---|---|---|
| ABS / PC-ABS Alloy (Cycolac, Bayblend) | Consumer Electronics, Automotive Dashboards | 2.00 – 2.20 | 0.78 – 0.82 | Torx ultra-thin flat head; prevents housing seam gap under torque |
| PA66-GF30 (30% Glass Filled) (Zytel) | EV Battery Trays, Motor Housings, Engine Shrouds | 2.25 – 2.50 | 0.82 – 0.86 | Case-hardened 1022A / Zinc-Nickel; resists abrasive glass fibers |
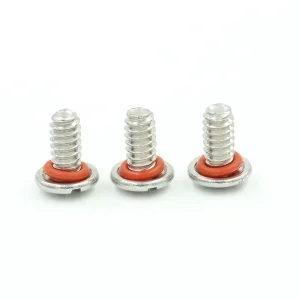
| PBT-GF20 / PBT-GF30 (Crastin, Valox) | Industrial Sensors, ECU Connector Enclosures | 2.10 – 2.35 | 0.80 – 0.84 | Pan head with captive O-ring; maintains IP67/IP68 hermetic seal |
| Polycarbonate (Unfilled PC) (Lexan, Makrolon) | Medical Diagnostic Shells, Transparent Covers | 2.30 – 2.55 | 0.82 – 0.85 | Passivated 304/316 Stainless; avoids notch stress cracking |
| Polypropylene (PP Copolymer) | Appliance Pumps, HVAC Duct Dampers | 1.90 – 2.10 | 0.72 – 0.76 | Coarse pitch PT profile; maximizes engagement against plastic creep |
| PEEK / PPS High-Performance (Victrex) | Aerospace Actuators, Surgical Handpieces | 2.40 – 2.65 | 0.84 – 0.88 | Precision cold-forged A2-70 / A4-80 Stainless Steel PT thread |
For custom polymer formulations, our laboratory calculates nominal pilot hole diameter using: d_h = c \times d, where $d$ represents major thread diameter and $c$ varies between 0.72 (soft polyolefins) and 0.88 (rigid high-modulus resins). Correct sizing guarantees full thread flank engagement without hydrostatic pressure buildup.
We advise integrating a shallow cylindrical counterbore ($d_c \approx 1.05 \times d$) at the entrance of the plastic boss. This relief zone eliminates upward material flash (crowning), ensures that flat under-head screw surfaces clamp squarely against mating components, and prevents stress concentration at the parting line.
Automated screwdriving lines operate efficiently only when the stripping torque ($T_s$) exceeds driving torque ($T_d$) by at least 300%. YH Fastener’s proprietary thread geometry and micro-wax lubricants widen this assembly process window, minimizing both motor stall rejections and stripped threads.
Mitigating supply chain risks through vertical in-house manufacturing, multi-site production facilities, and full material traceability.
In the contemporary B2B fastening marketplace, purchasing managers and engineering leads are caught between two distinct vulnerabilities: exorbitant price markups from multi-tier trading brokers, and unpredictable quality discrepancies from uncertified sub-contract workshops. Yu-Huang Electronics Dongguan Co., Ltd. solves this structural inefficiency through comprehensive internal integration across three high-capacity plants in Dongguan, Shaoguan, and Wuhan.
From initial carbide header die machining to multi-station heading and planetary thread rolling, all core tooling is engineered in-house. This cuts turnaround times on custom prototype batches from 8 weeks to under 12 business days, while maintaining tolerances down to $\pm 0.02\text{ mm}$.
Zero-defect commitments are backed by automated multi-camera glass turntable sorting systems. Every single PT screw is inspected at speeds up to 800 pcs/min for head diameter, recess concentricity, flank angle profile, thread integrity, and plating coverage prior to sealed packaging.
OEM buyers are paired directly with senior fastener application engineers. Whether analyzing broken boss samples via optical metallography or reviewing GD&T drawings, clients receive complete technical evaluations, FEA clamping models, and DFM recommendations within 24 hours.
Ensuring compliance with automotive, electronics, and environmental directives through rigorous testing protocols and certified chemistry.
Utilizing high-purity, vacuum-degassed AISI 1022A wire rod. Controlled atmosphere continuous mesh-belt furnace carbonitriding yields a surface hardness of HV 0.3 550–650 for clean thread forming in fiber-reinforced resins, paired with a ductile core hardness of HV 0.3 270–390 to eliminate brittle torsional shearing under dynamic shock.
Available in AISI 304 (A2) and AISI 316 (A4) austenitic grades for absolute corrosion resistance and chemical inertness in marine, pharmaceutical, and outdoor cleanrooms. For applications requiring both thread-forming capability and high hardness without electroplating embrittlement risks, AISI 410 martensitic stainless is heat-treated and passivated.
Finishes engineered to surpass ASTM B117 neutral salt spray standards:
• Black/Clear Zinc Plating: 96–168 hrs to white rust.
• Zinc-Nickel (Zn-Ni) Alloy: 1,200+ hrs to red rust, ideal for automotive under-hood.
• Geomet & Dacromet: Hydrogen-embrittlement-free thin-film barrier protection.
• Pre-Applied Nylon Patches: Locking torque resistance under continuous vibration.
Regulatory & Quality System Integrity: All YH Fastener manufacturing infrastructure operates in strict adherence to IATF 16949 (Automotive Quality Management), ISO 9001, and ISO 14001 environmental protocols. All shipments are accompanied by detailed Level 3 PPAP documentation, IMDS filings, dimensional CMM inspection reports, and full compliance certificates verifying adherence to RoHS Directive 2011/65/EU and REACH (EC 1907/2006).
Addressing the demands of high-frequency electronics, sustainable circular disassembly, and lightweight polymer-matrix composites.
As wearable IoT devices, AR/VR displays, and micro-medical implants miniaturize, plastic wall thicknesses shrink below 0.6 mm. Our cold-heading R&D team has realized micro-PT geometry in threads as small as M0.8 and M1.0, utilizing specialized Torx Plus (6-lobe) drive heads that allow automated micro-assembly without driver cam-out damage.
Traditional self-tapping screws cross-thread or strip after a single service removal. YH Fastener’s optimized thread crest and parabolic root design encourage true repeat engagement: the screw re-tracks into the original formed mating thread with negligible residual clamp loss over 5+ disassembly cycles, supporting global WEEE recycling directives.
Eliminate secondary manual O-ring fitting through cold-formed under-head annular undercut grooves that entrap EPDM, Silicone, or Fluoropolymer sealing rings. This delivers instantaneous IP67 / IP68 dust- and water-tight sealing directly against plastic enclosures in telecommunication and outdoor charging stations.
Direct answers from YH Fastener application engineers regarding plastic fastening design calculations, material validation, and production logistics.
Explore complementary OEM assembly hardware, including spring plungers, captive SEMS assemblies, and waterproof marine-grade structural screws.




Upload your 2D engineering drawings (PDF/DXF) or 3D CAD files (STEP/IGES). Receive a comprehensive manufacturing feasibility analysis, boss hole sizing consultation, and competitive direct-factory quotation within 24 hours.
