
Browse high-reliability self-tapping, sealing, and precision-engineered fastener hardware manufactured across our 20,000 m² clean facilities.


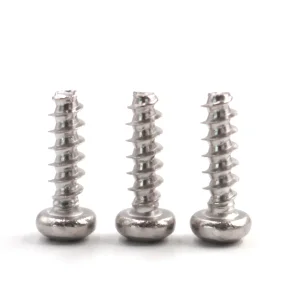
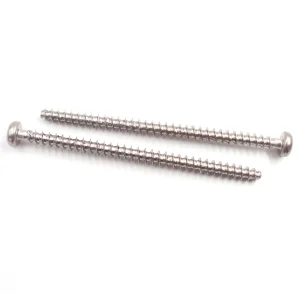
Traditional self-tapping screws utilize standard 60° thread angles originally engineered for ductile sheet metals. When driven into polymeric matrices, these legacy profiles exert massive circumferential bursting forces. PT thread geometry revolutionizes thermoplastic fastening.
Featuring a 30° profile angle rather than standard 60°, PT fasteners dramatically reduce radial expansion force during driving. This low displacement prevents cracking in thin-wall boss designs, enabling lightweight component miniaturization.
Shear Area OptimizationEnlarged thread pitch combined with an engineered core taper increases total plastic material flow between flanks. This deep inter-thread cavity accommodates material relaxation, maximizing pull-out load capacity even under elevated ambient heat.
Anti-Relaxation DynamicBy lowering driving torque while drastically elevating stripping torque thresholds, our PT fasteners ensure wide assembly safety margins. Automated screwdrivers can operate at peak cycle speeds without stripping plastic boss mating threads.
High Speed AutomationFrom automotive lightweighting to high-frequency 5G enclosures, PT thread-forming technology delivers reliable fastening into diverse crystalline and amorphous resins.
PBT+GF30 and PA66 enclosures subject to aggressive engine-bay thermal cycling benefit from PT thread stability, resisting micro-creep and dynamic harmonic loosening under road vibration.
ISO/TS Grade DurabilityIn smartphone internal chassis, AR/VR optical frames, and drone gimbals molded from Polycarbonate (PC) and ABS blends, ultra-miniature PT threads (M0.8 to M2.0) eliminate metal inserts.
Zero-Clearance JoiningBusbar support framing, flame-retardant polyamide tray lids, and battery cell housing assemblies use insulated or passivated PT fasteners to maintain structural rigidity without risk of conductive debris generation.
Dielectric Isolation ReadyCombined with custom under-head elastomeric washers and precision multi-stage cold formed collars, our PT screws deliver IP67/IP68 ingress seals on polyolefin and POM housings.
Sealed Environment CompliantReview the physical joint mechanics comparing our engineered PT profile to standard Type B tapping screws, cutting screws, and brass threaded heat-stake inserts.
| Evaluation Parameter | YH Fastener PT Screw | Standard Type B (60°) | Thread Cutting Screws | Brass Heat-Stake Inserts |
|---|---|---|---|---|
| Flank Profile Angle | 30° Low Radial Displacement | 60° High Burst Stress | 60° with Cutting Slot | N/A (Co-molded / Ultrasonic) |
| Radial Boss Expansion Stress | Minimal (Up to 45% lower) | Critical (High boss rupture risk) | Moderate (Debris generation) | Low (Residual heat stress) |
| Assembly Torque Ratio (Strip/Drive) | Optimal (> 2.5:1 Safety Margin) | Narrow (High stripping hazard) | Inconsistent | High (Requires threaded bolt) |
| Assembly Cost & Cycle Time | Direct Fastening (Lowest cycle cost) | Low cost, high scrap rate | Low cost, chip contamination | High tool cycle & insert expense |
| Disassembly & Re-usability | High (Maintains formed thread pitch) | Poor (Strip risk after 1-2 cycles) | Poor (Thread degradation) | Very High (Metallic thread) |
| Swarf / Particulate Generation | Zero (Pure cold plastic displacement) | Low to Moderate | Severe (Metallic/plastic shavings) | Zero |
Leverage Yu-Huang Electronics' vertically integrated supply system. Across 20,000 square meters of specialized production space, our cold heading lines operate around the clock.
Equipped with multistation automated headers and specialized high-speed PT thread rolling dies, our facilities churn out tight-tolerance micro-fasteners with zero grain boundary disruption, maximizing structural tensile resistance.
Multi-Die ProgressionContinuous mesh-belt carburizing furnaces guarantee uniform case depth and core ductility. Every PT screw undergoes controlled quenching and tempering to prevent hydrogen embrittlement while retaining case hardness for penetration.
Case Hardening RigorTo support automated assembly lines worldwide, our quality control architecture integrates 360-degree high-speed optical vision sorters, eliminating defect escapes for head diameter, recess wobble, thread runout, and foreign debris.
< 5 PPM Industrial QualityWe export engineered fasteners to over 60 industrial nations. Complete documentation, metallographic cross-sections, and environmental declarations accompany every lot.
Automotive grade traceability with Full Production Part Approval Process dossiers, including DFMEA/PFMEA support, dimensional layouts, Gage R&R, and international IMDS material uploads.
Automotive StandardCertified eco-friendly electroplating: Cr3+ trivalent clear/yellow zinc, black zinc, nickel, and ultra-high corrosion zinc-nickel coatings complying with EU Directives and SVHC lists.
Heavy Metal FreeOur Dongguan metrology lab provides application testing on your actual molded test bosses, offering empirical drive, seating, and stripping torque curves before mold sign-off.
Validation LaboratoryFlexible logistics programs including Vendor Managed Inventory, blanket purchase order stock agreements, and bonded warehouse clearance for zero line-stop guarantees across North America and Europe.
Just-In-Time AssuranceDiscover our comprehensive cold-forged catalog built for structural integrity, vibration isolation, and clean assembly.



As OEM requirements transition toward bio-polymers, composite lightweighting, and automated cleanrooms, our engineering team continuously innovates.
Pioneering hybrid thread forms capable of cleanly tapping into Carbon Fiber Reinforced Thermoplastics without shearing structural fibers, preserving high interlaminar composite strength.
Composite IntegrationEliminating wet lubricating oils on micro-fasteners. Developing PTFE/MoS2 matrix dry coatings that stabilize seating torques in Class 100 cleanroom medical and semiconductor settings.
Zero ContaminationPartnering with automated feed drive manufacturers to map real-time servo angle-torque curves, generating digital assembly certificates for automated production lines.
Industry 4.0 VerificationAuthoritative answers on boss design calculations, material pairings, stripping prevention, and factory ODM customization parameters.
The optimal pilot hole diameter typically ranges between 0.70x to 0.85x of the screw's nominal diameter, depending on whether the plastic is ductile (e.g., PP, PE) or rigid/filled (e.g., PA66+GF30, PPS). The outer boss diameter should typically equal 2.0x to 2.5x the screw diameter, with an entrance chamfer of 0.3-0.5 mm to aid thread engagement.
PT thread forming screws eliminate the separate ultrasonic or thermal installation step required for brass inserts, reducing manufacturing tooling, labor costs, and floor space. Moreover, PT screws offer exceptional vibration looseness resistance due to dynamic polymer spring-back directly into the 30° thread flanks.
We manufacture PT screws utilizing 1022A case-hardened carbon steel, 10B21 alloy steel, as well as AISI 304 and 316 austenitic stainless steels. Finishes include eco-friendly Cr3+ trivalent zinc, black zinc, Dacromet, Geomet, and electro-nickel, capable of withstanding neutral salt spray tests from 24 to 1,000+ hours.
Yes. Because PT threads form their mating interface via elastic-plastic deformation without cutting or splintering the plastic, the internal mating thread is preserved. By starting the screw counter-clockwise until it drops into the existing thread before driving, you achieve repeated disassembly cycles with minimal pull-out loss.
All high-tensile and case-hardened carbon steel PT screws undergo strict de-hydrogenation baking within 4 hours post-electroplating. Parts are soaked at 200°C–220°C for 4 to 8 hours depending on core hardness, followed by destructive stress rupture testing to verify ductility.
Tooling design, fabrication, and custom sample heading are typically completed in 7 to 10 business days. Standard production MOQs for custom configurations begin at 50,000 units (varying for micro sizes), backed by rapid 24-hour drawing reviews from our engineering staff.