
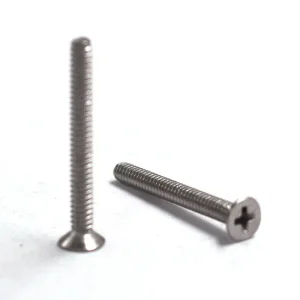
ODM Phillips Flat Head Machine Screws 304 Stainless Steel 82 Degree Countersunk M3 M4 For PCB Mounting Supplier, Factories
Request Technical CAD
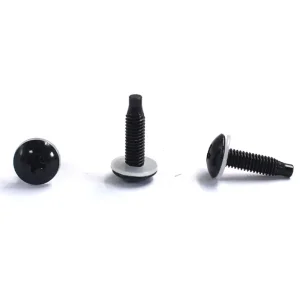
Precision cold-headed fasteners equipped with under-head captive O-ring grooves and anti-loosening technologies designed for electrical enclosures, powertrain housings, micro-electronics, and harsh marine environments.

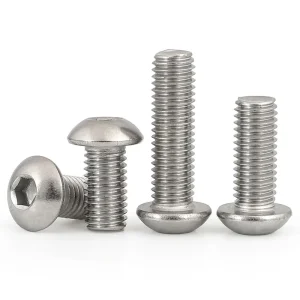
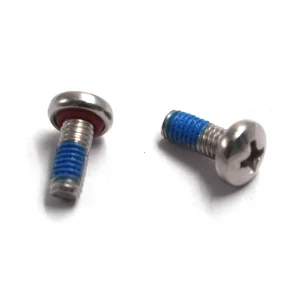
Conventional liquid threadlockers and standard external flat washers fail under dynamic thermal shock, vibration, and multi-axis hydraulic pressure. YH Fastener’s integrated rubber O-ring screws achieve hermetic, bi-directional sealing through precision CNC cold-formed undercut channels engineered to govern elastomer flow.
When a standard screw is torqued, an uncontained elastomeric washer tends to splay laterally, rupturing under shear and causing joint relaxation. Our proprietary under-head annular groove restricts lateral displacement.
Unlike soft-gasket assemblies that suffer from creeping preload decay, our self-sealing fasteners deliver precise metal-to-metal contact between the fastener bearing surface and the mating panel.
The trapped elastomer acts as an integrated internal hydraulic dampener, absorbing harmonic resonances that typically induce bolt rotation in mobile and vibrating machinery.
| Elastomer Material | Hardness Shore A | Operating Temp Range | Media Resistance Compatibility | Recommended Applications | Compliance Rating |
|---|---|---|---|---|---|
| Silicone (VMQ) | 50 - 70 Shore A | -60°C to +230°C | Ozone, weather, hot air, UV radiation | Avionics, medical hardware, outdoor telecom | FDA / UL94-V0 |
| Fluorocarbon (Viton® / FKM) | 70 - 90 Shore A | -20°C to +205°C | Fuels, synthetic lubricants, acids, aggressive solvents | Automotive powertrains, aerospace hydraulics | MIL-R-83248 / REACH |
| Nitrile (NBR / Buna-N) | 60 - 80 Shore A | -40°C to +120°C | Petroleum-based oils, hydraulic fluids, water | Industrial gearboxes, pneumatic cylinders, pumps | RoHS / ISO 3601 |
| Ethylene Propylene (EPDM) | 60 - 75 Shore A | -45°C to +150°C | Brake fluid, hot water, steam, polar solvents | EV battery cooling circuits, HVAC compressors | NSF / WRAS |
| Fluorosilicone (FVMQ) | 60 - 75 Shore A | -65°C to +175°C | Jet fuel, petroleum distillates, extreme low-temp | Military aerospace, radar systems, subsea exploration | MIL-DTL-5423 |
Modern engineering design cycles require robust fastener standardization. OEMs across North America, Europe, Japan, and Southeast Asia are replacing multi-component sealing stacks with monolithic O-ring screws to streamline bill-of-materials (BOM), reduce manual assembly error, and guarantee long-term field reliability.
Electric vehicle traction battery enclosures require IP67/IP69K sealing against moisture ingress while enduring thermal cycling and extreme road vibrations. Custom self-sealing screws eliminate the catastrophic risk of dielectric coolant escape or water-induced short circuits in battery management systems (BMS).
By consolidating the fastener and elastomeric seal into an integrated unit, automotive assembly lines reduce takt times by 35% compared to applying secondary anaerobic sealants.
Hyper-scale telecommunications base stations, outdoor optical distribution boxes, and mmWave transceivers operate under aggressive environmental conditions, including solar UV degradation, acid rain, and driving wind.
YH Fastener provides SS316 marine-grade screws coupled with ozone-resistant EPDM or fluorosilicone O-rings, preventing capillary liquid ingress through tapped blind holes and preserving sensitive micro-electronics across decades of maintenance-free service.
Industrial multi-axis articulated robots, servomotor end-effectors, and hydraulic manifold blocks encounter dynamic pulsating pressures and oil-mist exposure.
Our Viton-ringed high-tensile alloy steel (Class 10.9 and 12.9) screws provide rigid mechanical clamping while sealing up to 40 MPa internal hydraulic pressures, eliminating messy external fluid leakage and preserving sterile operating environments in cleanroom automation.
As smart electronic devices miniaturize and power densities surge, sealing hardware is transforming from passive mechanical components into multifunctional systems engineered for EMI shielding, chemical inertness, and automated smart-factory integration.
With the advent of autonomous driving radar and high-frequency 6G communications, conventional non-conductive rubber causes electromagnetic leakage paths through fastener holes.
YH Fastener’s engineering roadmap features silver-plated aluminum, nickel-graphite filled silicones, and conductive fluorosilicone O-rings integrated directly into screw under-heads. This produces concurrent IP68 fluid sealing and 80dB+ EMI attenuation up to 40 GHz across sensitive defense and automotive electronics enclosures.
Consumer electronics, smart wearables, and implanted biomedical devices require microscopic water-tight fasteners. Forming precision under-head seal retention channels on screws smaller than M1.6 has historically been deemed unfeasible through high-speed cold heading.
Through multi-station progressive carbide tooling and sub-micron EDM die finishing, YH Fastener mass-produces micro sealing screws down to M0.8 diameter with zero burr formation and strict +/-0.02mm undercut groove tolerances.
Semiconductor wet processing, atomic layer deposition (ALD), and petrochemical equipment demand resistance to plasma etching gases and supercritical solvents that degrade standard Viton and Silicone.
Integrating custom FFKM (Kalrez-equivalent) formulations within high-nickel alloys like Hastelloy C276, Inconel 718, and Titanium Grade 5 screws guarantees extreme temperature survivability up to 327°C and universal chemical immunity.
Quality assurance at YH Fastener is embedded directly into our production processes. From raw steel wire cold-heading to precision automated vulcanization and final packaging, every batch undergoes strict metallurgical, mechanical, and ingress testing.
Certified automotive-grade management framework ensuring strict PPAP Level 3 documentation, FMEA analysis, Control Plans, and full heat-lot raw material traceability.
High-speed multi-camera optical sorters inspect head concentricity, shank straightness, thread pitch, and O-ring seating to eliminate line-stopping assembly defects.
In-house vacuum decay and hydrostatic testing rigs verify underwater immersion performance down to 50 meters, along with high-pressure steam jet (IP69K) survivability.
Fully certified to EU RoHS Directive 2011/65/EU and REACH (SVHC free). Elastomeric elements meet FDA 21 CFR 177.2600 standards for food-contact and medical applications.
Our senior applications engineering team will evaluate your 2D/3D CAD files (STEP, IGES, DXF) to recommend the ideal groove geometry, elastomer durometer, and thread-locking parameters. We provide fast prototyping and technical DFM evaluations within 24 hours.
Browse our complete range of specialized industrial fasteners, tamper-proof security drives, spring positioning plungers, and hardened tooling designed to complement your production assemblies.


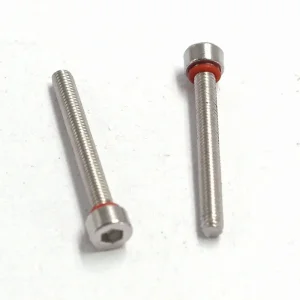
Key considerations for specifying, testing, and assembling high-performance custom O-ring sealing screws in mission-critical applications.
An external sealing washer rests loosely between the bolt head and the mating surface. Under torque tightening, the flat washer experiences uncontrolled compressive displacement, often extruding outwards, shearing, or creating localized leak paths. In contrast, YH Fastener’s self-sealing screws feature an undercut annular groove cold-formed directly into the underside of the head. This groove encloses the elastomeric O-ring on three sides, controlling compression to precisely 25%–35% while permitting direct, solid metal-to-metal contact between the screw head and the mating panel. This design maintains positive clamp torque without washer relaxation while sealing up to 6,000 PSI against vacuum, gas, and fluid penetration.
Yes, provided the fastener is installed according to the specified torque rating and the elastomer has not suffered chemical damage or thermal set. Because the O-ring is captured within an engineered groove, it avoids destructive over-compression during installation. For standard maintenance cycles in telecommunications and industrial equipment enclosures, YH Fastener sealing screws typically support multiple re-assembly cycles without degradation in IP67 or IP68 waterproof ratings.
For electric vehicle battery packs, Fluorocarbon (Viton® / FKM) and high-grade Ethylene Propylene Diene Monomer (EPDM) are the preferred materials. Viton offers resistance to battery electrolyte solvents, synthetic coolants, gear oils, and thermal excursions up to +205°C. For water-glycol immersion circuits, peroxide-cured EPDM is recommended due to its low compression set and stability in polar liquids from -45°C to +150°C.
When austenitic stainless steel screws (AISI 304 or 316) contact aluminum housings in the presence of an electrolyte (such as salt spray), galvanic cell corrosion can occur. YH Fastener mitigates this by providing functional barrier coatings, including specialized zinc-nickel plating (surpassing 1,500 hours of neutral salt spray without white or red rust), passivated fluoropolymer sealers, or pairing the fasteners with electrically insulating O-ring profiles to break galvanic continuity.
Our multi-station cold-heading equipment supports standard and custom configurations:
Head Styles: Pan head, button head, socket head cap, flat countersunk (with 82° or 90° sealing skirts), truss head, and hex washer head.
Drive Systems: Phillips, Torx (6-lobe), Torx Plus, tamper-resistant pin Torx, hex socket, slotted, and triangular anti-theft recesses.
Every production batch is backed by comprehensive quality records: EN 10204 3.1 Mill Material Inspection Certificates, dimensional inspection reports (CMM and optical), micro-Vickers hardness verification, plating thickness analysis via X-ray fluorescence (XRF), Salt Spray Test reports, and full automotive PPAP Level 3 documentation upon request. All fasteners comply with EU RoHS, REACH, and California Proposition 65 directives.
For custom-engineered sealing fasteners requiring proprietary cold-heading tooling or special elastomer molds, prototype batch sizes start from 5,000 to 10,000 pieces. Standard metric and imperial sizes from our active tooling library feature MOQs from 2,000 pieces. Rapid 3D prototyping and tooling development are typically completed within 7 to 10 working days, with mass production runs delivered in 15 to 25 working days.