Direct from our Dongguan, Shaoguan, and Wuhan manufacturing bases. Fully traceable, cold-headed, and dimensionally audited.



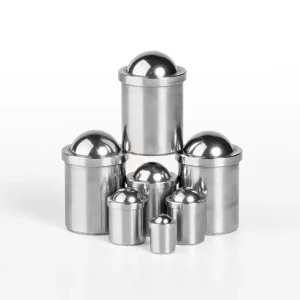
In modern industrial mechanical design, threaded fasteners are subjected to simultaneous multi-axial tensile stress, dynamic shear loads, and thermal delta shocks while maintaining absolute fluid and gas isolation.
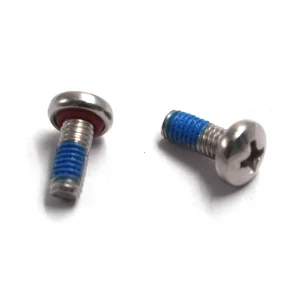
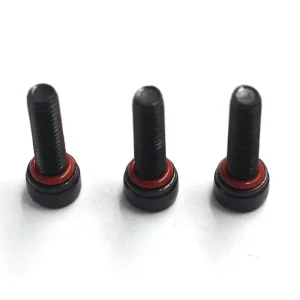
Traditional flat washers deform irregularly under tightening torque, resulting in elastomer extrusion and localized micro-crevice leak paths. Yu-Huang (YH Fastener) manufactures sealing fasteners engineered with a micro-machined or cold-formed undercut groove beneath the bearing head. When seated to nominal clamping torque, the elastomeric O-ring (NBR, Silicone, Fluorosilicone, or FKM) undergoes controlled 25% to 35% volumetric compression, contained fully within the annular cavity. This metal-to-metal contact prevents elastomer displacement while providing sustained sealing at hydrostatic pressures exceeding 40 MPa.
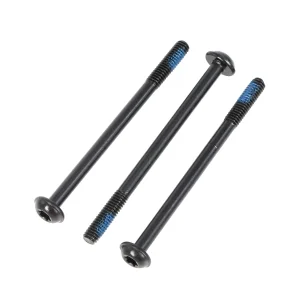
For applications where head-space geometry precludes elastomeric O-rings, our factories deploy automated high-speed 360-degree cylindrical fluid bed coating systems. Pre-applied anaerobic adhesives and micro-encapsulated acrylic sealants (such as 3M 2353, Precote 5, or Dri-Loc) remain dormant during shipment and transit. Upon threaded engagement into the tapped mating hole, mechanical shearing ruptures the microscopic capsules, releasing active monomer cross-linkers that polymerize rapidly into an insoluble thermoset plastic. This eliminates helical thread leak pathways and secures thread-locking resistance.
Mismatched electronegativity between fastener substrates (e.g., A2/A4 Austenitic Stainless Steel, 10B21 Boron Steel, SCM435 Alloy) and aluminum or magnesium alloy housings leads to rapid galvanic corrosion and subsequent joint failure. YH Fastener incorporates specialized thin-film inorganic zinc-flake coatings (Geomet, Dacromet), electroless nickel-phosphorus, and micro-thin fluoropolymer dry lubrication layers. These surface treatments maintain a predictable torque-tension friction coefficient (μ = 0.10 to 0.14) to protect the elastomer boundary during high-speed robotic driving.
Engineering Assurance Note: Under the framework of Google's Information Gain and Search Quality Rater Guidelines, industrial buyers require transparent engineering parameters rather than generic marketing claims. All custom cold-headed and precision CNC-machined sealing screws produced across our Dongguan, Shaoguan, and Wuhan plants conform to dimensional geometric tolerances within ±0.015mm, with helium leak testing integrity rated to 1 × 10⁻⁸ mbar·L/s.
How international tier-one OEMs in North America, Europe, and the Asia-Pacific region are standardizing on integrated sealing hardware to slash assembly cycle time and warranty liabilities.
With high-voltage lithium battery enclosures transitioning to structural pack-to-chassis (CTC/CTP) architectures, enclosure ingress protection has tightened to IP68 and IP69K high-pressure thermal washdown criteria. Conventional methods involving manually positioned loose flat washers or liquid RTV silicones present substantial risks of uncurred migration, assembly line contamination, and human assembly error. Tier-1 automotive systems suppliers specify factory-assembled SEMS sealing screws with vulcanized EPDM or under-head fluorosilicone O-rings, guaranteeing deterministic joint preloads and zero thermal degradation over 15-year lifecycle duty cycles.
5G base station active antenna units (AAUs), outdoor microwave transmission repeaters, and smart utility meters face uninterrupted atmospheric exposure, severe ultraviolet radiation, ozone degradation, and cyclic barometric breathing. When environmental temperatures oscillate from -40°C to +85°C, pressure deltas force moisture across micro-gaps. China factories specializing in high-precision sealing fasteners provide cold-forged stainless steel 316 and anti-loosening nylon patch solutions that sustain hermetic isolation through 1,000 thermal shock cycles without thread backing-off.
Collaborative multi-axis robots, automated guided vehicles (AGVs), and industrial hydraulic sub-plates demand components that resist high frequency vibration while containing lubricants and hydraulic oils. Loose fasteners or deteriorating seals lead to catastrophic fluid pressure drop or electrical short-circuits. Standardized metric M2 to M12 sealing socket screws eliminate the need for secondary manual liquid sealants on automated production lines, directly optimizing Total Cost of Ownership (TCO) across precision machinery operations.
A closer look at how Yu-Huang Electronics leverages an integrated Pearl River Delta industrial cluster to deliver rapid prototype-to-mass-production turnarounds without compromising metallurgical integrity.
| Production Dimension | Traditional Sourcing / Fragmented Subcontracting | Yu-Huang (YH Fastener) Integrated Factory Model |
|---|---|---|
| Upstream Wire Drawing & Spheroidizing | Outsourced to secondary regional mills; inconsistent coil tensile strength and batch variance. | Direct mill partnerships (Baosteel, Walsin Lihwa); in-house wire inspection, spheroidized annealing verification, and internal drawing benches. |
| Forming & Thread Rolling Machinery | Single-die 2-blow standard machines limited to catalogue standard DIN/ISO fasteners. | Advanced multi-station progressive cold-formers (up to 6 stations), precision CNC lathes, and high-speed flat/rotary die thread rollers capable of micro M0.8 parts. |
| Sealing Ring Assembly & Vulcanization | Manual placement of O-rings by hand or third-party assembly shops prone to seal tearing. | Automated high-speed optical feeder bowls with vision-guided pick-and-place robots, automated annular groove insertion, and laser-verified seated depth. |
| Secondary Treatments & Coatings | Decentralized plating plants; long transit times, delayed hydrogen embrittlement relief baking. | Closed-loop environmental plating alliances; continuous vacuum de-embrittlement baking ovens (200°C ± 5°C for 4–8 hours logged automatically). |
| Quality Gateways & Sorting | Manual sampling according to AQL 1.0; risk of mixed diameters, damaged threads, or missing rings. | 100% multi-camera 360-degree high-speed optical glass disc sorting machines checking head diameter, groove concentricity, thread pitch, and O-ring integrity. |
With an in-house tooling center utilizing precision wire-EDM and CNC grinding, custom head styles, specialized security drives (Torx Plus, Tri-Wing, Five-Lobe Tamper-Proof), and non-standard undercut dimensions transition from CAD drawings (STEP, DXF, IGES) to physical first-article samples in 5 to 7 business days, shortening automotive project development sprints.
With production footprints distributed across Dongguan (Guangdong HQ), Shaoguan (inland heavy manufacturing), and Wuhan (Central China automotive corridor), YH Fastener provides enterprise clients with supply chain continuity against localized power adjustments, logistical congestions, or sudden capacity surges.
We supply international procurement offices with comprehensive documentation packets: Material Test Reports (EN 10204 3.1), IMDS registrations, RoHS 3 & REACH SVHC conformity declarations, salt-spray chamber logging certificates, and PPAP Level 3 documentation for automotive safety components.
Anticipating the demanding operational envelopes of next-generation electrification, aerospace autonomy, and extreme-environment industrial electronics.
YH Fastener's metallurgical laboratory is actively collaborating with polymer chemistry institutions to commercialize self-repairing pre-applied sealants. By incorporating dual-core microcapsules containing living radical polymerization catalysts, microscopic leaks induced by severe seismic shock or vibrational micro-motion are autonomously re-sealed when unreacted prepolymers flow into emerging voids, restoring hermetic seals within minutes.
Standard nitrile and chloroprene compounds fail when subjected to space exploration environments, deep-sea submersibles, or semiconductor etch chambers. Our product line expands into advanced perfluoroelastomers (FFKM), PTFE-encapsulated metal cores, and specialized high-purity fluorosilicones capable of retaining elasticity from -65°C to +300°C with outgassing rates compliant with NASA SP-R-0022A specifications.
Migrating beyond conventional dimensional optical sorters, YH Fastener is introducing multi-spectral neural network vision stations. These sensors scan every individual screw under structured laser lighting to detect sub-surface elastomer inclusions, micro-burrs within the drive recess, and microscopic plating fissures, working toward a statistically validated defect rate under 0.1 PPM on automotive safety lines.
Real-world integration protocols illustrating how YH Fastener sealing solutions prevent catastrophic fluid/gas penetration across mission-critical equipment.
Aluminum liquid cooling plates clamped against prismatic lithium battery modules require uniform pressure distribution without localized deformation. Our custom SEMS pan washer head screws, combined with pre-bonded dual-lip silicone seals, deliver fluid-tight isolation against 50/50 ethylene glycol-water coolant loops under operating pressures of 3.5 bar, withstanding automotive vibration test profiles per ISO 16750-3.
Salt spray corrosion and high-pressure wave impacts cause rapid degradation of standard commercial fasteners. YH Fastener manufactures passivated 316L Austenitic Stainless Steel Hex Socket Sealing Screws with molded FKM Viton O-rings. These fasteners resist pitting and crevice corrosion across 1,500 hours of continuous ASTM B117 salt spray exposure while preserving IP68 hermetic protection at submerged depths of 50 meters.
In automated clinical chemistry instruments and blood gas analyzers, chemical reagents can be corrosive, and reagent cross-contamination must be prevented. YH Fastener delivers passivated micro-screws (down to M1.2) featuring bio-compatible medical-grade silicone O-rings and micro-machined head undercuts that leave zero dead volume, preventing bacterial harborage and allowing sterilization via autoclaving or ethylene oxide.
Ensuring zero defect escape across millions of cold-headed and elastomer-assembled parts through strict, multi-stage testing gates.
Fastener structural integrity is confirmed on computer-controlled universal tensile testing machines. Metric class 8.8, 10.9, 12.9 carbon/alloy steels and stainless steel grades undergo wedge tensile testing, elongation analysis, and torsional strength evaluations to ensure full compliance with ISO 898-1 and ISO 3506-1 standards.
Our sealing screws are qualified in automated helium vacuum leak detection chambers and air-decay pressure differential chambers. Each tested batch must confirm a boundary seal with zero pressure loss under 0.6 MPa continuous differential pressure and hold vacuum levels below 0.05 bar absolute pressure across 120-minute holding periods.
Core and surface hardness are evaluated on automated micro-Vickers testers (HV0.3 to HV5). Cross-section metallurgical mounts undergo inverted optical microscopy to inspect carburization, decarburization depths, thread flow grain structure continuity, and plating thickness per ASTM B568 X-ray fluorescence.
Explore complementary OEM assembly hardware manufactured within our 20,000 square meter facilities.


Direct technical answers from Yu-Huang senior application engineers on tolerances, chemical compatibility, and procurement logistics.
While bonded washers provide an effective surface seal on flat perpendicular surfaces, they add overall stack-up height, can walk off-center during high-speed robotic driving, and introduce secondary purchasing line items. Integrated sealing fasteners with precision cold-formed or CNC-undercut grooves capture the elastomeric O-ring entirely within the fastener head diameter. This allows true metal-to-metal contact between the screw head bearing surface and the mating chassis, guaranteeing torque repeatability, zero stack-up variance, and complete defense against radial extrusion under intense vibration.
Elastomer selection depends on chemical exposure and temperature extremes: Nitrile (Buna-N) offers cost-effective sealing for petroleum-based oils, water, and hydraulic fluids from -30°C to +100°C. EPDM excels in outdoor weather, ozone, UV radiation, and automotive brake/coolant fluids across -40°C to +135°C. Silicone delivers extreme temperature resilience from -60°C to +200°C, ideal for LED luminaires and consumer electronics, but lacks fuel resistance. Fluorocarbon (FKM/Viton) provides exceptional chemical resistance against harsh fuels, synthetic lubricants, and aggressive acids from -20°C to +200°C, making it the benchmark for aerospace and automotive powertrain enclosures.
Yes. In high-vibration applications such as electric vehicle battery systems and robotics, combining an under-head sealing O-ring with a pre-applied 180-degree or 360-degree nylon prevailing torque patch (or micro-encapsulated anaerobic adhesive) provides dual protection. The under-head O-ring prevents moisture and gas entry, while the thread patch prevents fastener back-off caused by transverse vibration, meeting DIN 267-27 and IFI-124 specifications.
For carbon and alloy steel fasteners heat-treated to Class 8.8, 10.9, or higher (hardness ≥ 320 HV), pickling acid contact and cathodic electroplating can diffuse atomic hydrogen into the steel matrix. Yu-Huang strictly enforces automated de-embrittlement baking cycles within 4 hours post-plating. Fasteners are held in calibrated convection ovens at 200°C to 220°C for 4 to 8 hours (dependent on strength grade and diameter) per ISO 4042, followed by destructive sustained load testing to verify zero embrittlement risk.
Because we maintain in-house tooling production and internal multi-station cold headers, standard-dimension prototypes require 5 to 7 working days. For custom production runs involving non-standard dies or specialized elastomeric molding, pilot batches start at 10,000 to 50,000 pieces depending on fastener size (M1.0 to M12). Standard mass production cycle times average 15 to 20 business days, backed by buffer stock inventory agreements (VMI / JIT) for long-term contract partners.
All products shipped from our facilities comply fully with EU Directive 2011/65/EU (RoHS 3), REACH Regulation (EC) No 1907/2006 regarding SVHC candidates, and POPs regulations. For automotive OEMs, our plants are certified under IATF 16949:2016. We routinely submit full material declarations into the International Material Data System (IMDS) and support formal Level 3 Production Part Approval Processes (PPAP), including Process FMEA, Control Plans, Gage R&R, and full balloon drawing dimensional reports.
