Explore standard, self-drilling, high-torque, and self-sealing fasteners directly fabricated from cold-heading lines.
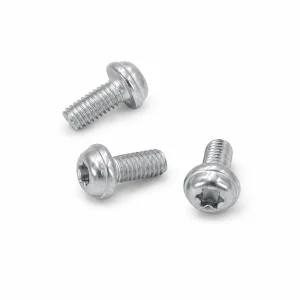


Strategic deployment of cross-recessed thread-forming fasteners across automated tier-1 manufacturing ecosystems.
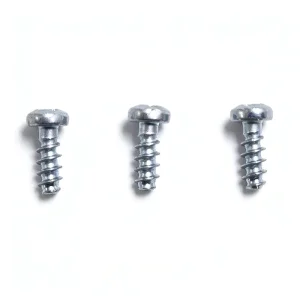
By engineering specialized lead-in pitch profiles (Type AB and Type B), our fasteners remove secondary tapping routines, saving capital tooling costs and cycle time in automotive and consumer electronics lines.
Optimized Phillips cross-recess (DIN 7981 / ISO 7049) featuring concentric driver alignment prevents cam-out and wobbling during multi-spindle automatic feed screwdriving exceeding 1,200 RPM.
Multi-layer zinc-nickel alloy, trivalent passivation, and fluorocarbon topcoats yield robust resistance against galvanic oxidation in EV battery enclosures, marine solar mounts, and telecommunications arrays.
Comprehensive metallurgical matrix showcasing case-hardened carbon steel and austenitic stainless steel material specifications.
| Material Designation | Core Hardness | Surface Hardness | Torsional Strength (M4 Ref) | Corrosion Shielding | Primary Industrial Sector |
|---|---|---|---|---|---|
| AISI 1022 Carbon Steel Case-Hardened | HRC 28 - 38 | HV 450 - 650 (Min. 0.05mm) | > 4.8 N·m | Cr3+ Galvanized / Eco-Zinc | Consumer Electronics, Industrial Enclosures |
| AISI 304 (A2-70) Austenitic | HRB 85 - 95 | Passivated Work-Hardened | > 3.9 N·m | Passivation (ASTM A967) | Precision Audio, Smart Home, Marine Sensors |
| AISI 316 (A4-80) Marine | HRB 90 - 100 | Passivated Anti-Corrosive | > 4.2 N·m | Grade 5 Marine Resistance | EV Charging Piles, Outdoor Photovoltaics |
| SCM435 Alloy Steel Grade 10.9 | HRC 32 - 39 | Carbonitrided Micro-Layer | > 6.2 N·m | Zinc-Nickel Alloy + Sealant | Automotive Powertrain, Actuators |
Addressing structural load distribution, localized micro-vibration, and thermal expansion across demanding assembly lines.
Micro Phillips self-tapping screws (M1.2–M2.5) with shallow pan heads prevent motherboard trace stress and PCB delamination. Controlled torque margins prevent thread stripping in soft ABS/PC boss towers.
Certified under IATF 16949 workflows, our high-clamp cross-recess fasteners join thin-gauge cold-rolled steel and aluminum alloy substrates without requiring blind rivets or cage nuts.
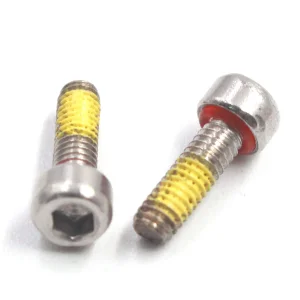
Featuring pre-applied microencapsulated threadlockers or serrated under-head bearing surfaces, these screws withstand sustained harmonics in solar inverters, commercial energy storage racks, and wind nacelle cabinets.
Three decades of manufacturing authority validated through ISO 9001, ISO 14001, and IATF 16949 verified testing regimens.
Electroplated carbon steel fasteners undergo 200°C–220°C de-embrittlement baking within four hours of acid processing for a minimum duration of 8 to 24 hours, guaranteeing zero catastrophic delayed fracture.
High-resolution glass-plate optical sorters screen every manufactured fastener for head height, recess depth, thread pitch, and total runout, safeguarding high-speed robotic assembly plants against jam errors.
Complete traceability from certified steel ingot mills to finished product. Full lab reporting includes heavy metal screening, SVHC disclosures, and IMDS documentation required by European and North American buyers.
Pioneering cold-heading innovations, automated AI optical calibration, and sustainable low-carbon manufacturing initiatives.
Integrating closed-loop scrap wire recycling and biodegradable cold-forging lubricating oils to lower Scope 1 and Scope 2 carbon footprints across Dongguan, Shaoguan, and Wuhan facilities.
Developing ultra-thin, low-friction micro-coatings that allow self-tapping screws to achieve equal clamp force with 25% lower driving torque, reducing wear on assembly line driver bits.
Providing OEM clients with finite element analysis (FEA) models to calculate ideal pilot hole diameter and wall thickness ratios across composite thermoplastics and light alloys.
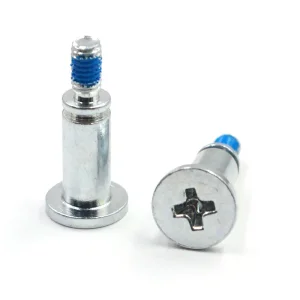
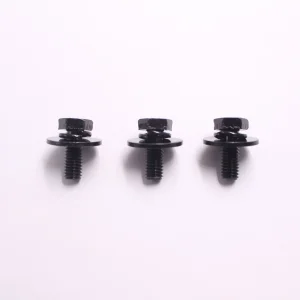
Specialty thread-forming screws, multi-component SEMS screws, and precision anti-loosening industrial hardware.
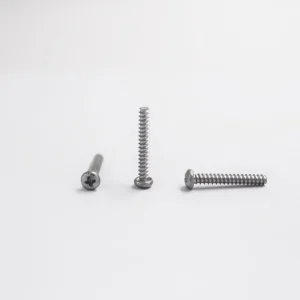


Expert answers covering thread designs, hole preparation, torque parameters, and OEM customization.
Thread-forming screws (e.g., DIN 7981 Type AB/B) displace mating material cold without cutting chips, generating internal threads with zero metallic debris—essential for cleanroom electronics. Thread-cutting screws feature flutes that broach mating internal threads in brittle plastics or heavy die-cast alloys.
We apply high-precision cold heading dies that yield strict Phillips recess depth and wing geometry per ISO 4757. For automated assembly requiring zero driver disengagement, we also supply Phillips-Square combination or matched Torx drive alternatives that distribute torque along vertical drive walls.
Austenitic stainless steels (304/316) cannot be case-hardened using standard heat treatments. They tap into aluminum, softer brass, or engineered thermoplastics. For carbon steel sheets exceeding 1.2mm, we supply 410 martensitic stainless steel with case hardening or bimetallic fasteners with hardened carbon steel drill points.
Every batch of electroplated Grade 8.8 and case-hardened tapping screws undergoes strict baking cycles (200°C–220°C for 8 to 24 hours) within 4 hours of electroplating. Lots are verified via stress-durability testing under 75% ultimate tensile load for 48 hours without cracking.
Standard samples ship within 24 to 48 hours from our inventory hubs. For custom-engineered drawings requiring new heading tooling and thread dies, tooling fabrication and pilot samples take 10 to 14 working days, followed by mass production delivery in 20 to 25 days with full dimensional and PPAP Level 3 documentation.
Our captive sealing screws feature precision-machined under-head annular recesses that contain an EPDM or silicone O-ring during installation. When torqued, the elastomeric element compresses into the metal groove, preventing water, dust, and hydraulic fluids from bypassing the thread interface.
