Mass-produced via high-speed multi-station cold formers, optical roller sorters, and continuous heat treatment belts.


Navigating supply chain volatility, decarbonization directives, and the transition toward automated, defect-free cold heading ecosystems.
Direct supply partnerships with Baosteel and Xingcheng Special Steel ensure strict control over raw wire rod chemical composition, decarburization depths, and grain structure uniformity before heading begins.
Transitioning from multi-step machining to high-speed multi-station cold heading reduces material scrap rates from over 52% down to under 3%, substantially lowering per-unit production expenditure.
Tri-regional operational redundancy across Dongguan (Guangdong HQ), Shaoguan, and Wuhan facilities guarantees zero production disruptions during localized logistical bottlenecks or regional industrial constraints.
In the contemporary industrial landscape, commercial fastener procurement has outgrown the traditional metric of simple per-thousand piece unit price. As tier-1 global equipment builders accelerate automated assembly cycles, a single misformed thread, hydrogen embrittlement failure, or microscopic burr can stall high-throughput robotic assembly lines, resulting in tens of thousands of dollars in assembly floor downtime. The modern industrial buyer demands Information Gain: an empirical understanding of wire rod draw ratios, cold-forming grain boundary continuity, multi-stage thread rolling dynamics, and statistical process control (SPC) data backed by comprehensive PPAP Level 3 documentation.
China remains the undisputed epicenter of precision fastener mass-production, accounting for more than 40% of the world's mechanical hardware production. However, leading manufacturers like Yu-Huang Electronics Dongguan Co., Ltd. (YH Fastener) represent the technological divergence from low-margin commodity hardware to high-precision engineering cold-formed solutions. With over 30 years of operational heritage, 20,000 square meters of dedicated production space, and tri-factory logistical capabilities, YH Fastener bridges the gap between massive scale economies and micro-tolerance aerospace/automotive stringency.
A deep dive into cold extrusion mechanics, thread rolling precision, and in-line thermal kinetics across our tri-plant manufacturing network.
Unlike conventional subtractive machining where metal fibers are severed, cold heading relies on high-pressure plastic deformation. By forcing annealed steel, brass, or austenitic stainless steel wire rod into carbide dies at room temperature, internal metallurgical grain lines flow continuously along the contours of the screw head, shank, and under-head fillets. This uninterrupted grain orientation generates superior shear, fatigue, and tensile properties, ensuring critical fasteners resist extreme cyclical stresses in vibrating automotive battery chassis and high-speed robotic limbs.
Our workshop houses over 250 high-precision multi-station cold heading machines, including high-speed 1-die-2-blow, 2-die-4-blow, and complex 4-die-4-blow transfer headers capable of forming micro-fasteners from nominal diameter M0.8 up to M12 structural bolts. Advanced in-line tooling monitoring instantly detects punch fractures, wire feed variances, or die wear, automatically rejecting non-conforming blanks at rates exceeding 350 pieces per minute.
Threading is executed strictly via rotary planetary or reciprocating flat-die thread rolling equipment. Rather than removing metal via chasing or tapping, the blank is compressed between hardened dies, cold-working the threads into existence. This burnishes the root radius and pitch flanks, increasing external thread surface hardness by 15% to 25% while leaving residual compressive stresses that defend against fatigue micro-cracking.
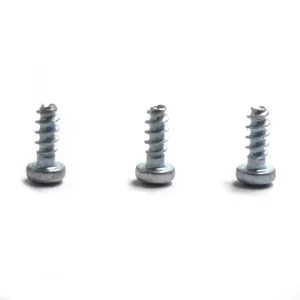
For demanding plastic assemblies (such as consumer electronics housings and automotive lighting), our proprietary PT® 30-degree thread profile drastically reduces radial expansion stress while maximizing axial pull-out resistance, eradicating the boss burst failures commonly observed with generic 60-degree sheet metal screws.
| Process Parameter | YH Precision Fastener Factory Specs | Standard Industry Norm | Engineering Benefit to Client |
|---|---|---|---|
| Diameter Capability | M0.8 to M12 (0.030" to 0.500" ANSI) | M2.5 to M10 | Enables micro-electronic integration & heavy structural chassis mounting |
| Length Range | 1.2 mm to 150 mm custom lengths | 6 mm to 60 mm | Accommodates deep blind-hole housings and thin sheet interfaces |
| Dimensional Tolerance | ±0.015 mm (down to ±0.005 mm on CNC specials) | ±0.05 mm to ±0.10 mm | Seamless compatibility with robotic vacuum feeders & automated drivers |
| Thread Profiles | Metric, UNC, UNF, BSW, PT-30°, Double-Lead, Trilobular | Standard Metric / UNC only | Optimized pull-out resistance across plastics, cast aluminum, & sheet steels |
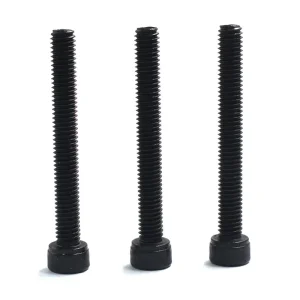
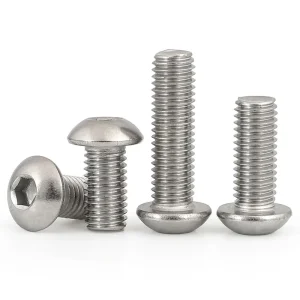
| Head & Drive Geometries | Pan, Flat, Truss, Socket, Torx (Six-Lobe), Tamper-Resistant, Sems | Standard Phillips / Slotted | High torque transfer, zero cam-out, anti-tamper security protection |
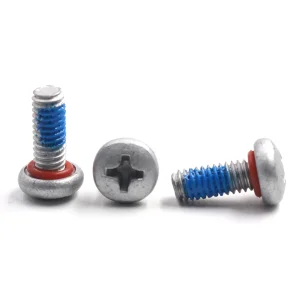
| Secondary Value-Add | In-line EPDM vulcanization, 360° Nylon patch, Micro-encapsulated epoxies | Outsourced third-party patch | One-stop warranty accountability with guaranteed 5-time reusability |
Tailoring mechanical fastening dynamics to the unique thermal, chemical, and physical stresses of mission-critical systems.
Use Case: EV battery pack module retainers, battery management system (BMS) busbar fasteners, and inverter enclosures.
Solution: Class 8.8 and 10.9 hardened alloy fasteners equipped with trivalent zinc-nickel electroplating and pre-applied micro-encapsulated locking patches. Certified to withstand 1,000+ hours neutral salt spray resistance and rigorous ISO 16750-3 automotive random vibration testing without loss of clamp load.
Use Case: PCB grounding, smartphone frames, drone gimbal stabilizers, and server blade chassis.
Solution: Austenitic stainless steel 304 and 316 micro-screws (M1.0 to M3.0) with wafer-thin head profiles and precision Torx drives. Non-magnetic treatments (relative permeability μr < 1.05) safeguard ultra-sensitive RF signals and compass modules from magnetic distortion.
Use Case: 5G outdoor base stations, solar inverter IP68 weather-sealed enclosures, and smart grid electric meters.
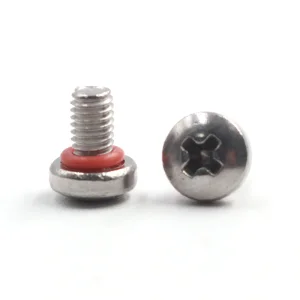
Solution: Custom EPDM bonded washer assemblies and under-head O-ring sealing screws. The elastomer vulcanization forms a hermetic seal against moisture, chemical wash-down, ozone, and UV radiation, maintaining IP67/IP68 ingress protection under continuous thermal cycling.
Operating under audited IATF 16949, ISO 9001, and ISO 14001 certifications to deliver verifiable trace-to-melt pedigree.
Every single mass-production production lot passing through our facilities is subjected to a rigorous 5-stage verification regimen. Our Dongguan metrology laboratory is outfitted with certified coordinate measuring machines (CMM), optical profilometers, micro-Vickers hardness testers, Fischer X-ray fluorescence (XRF) coating thickness analyzers, and dedicated tensile/shear test benches.
Securing global OEM approval requires full transparency. YH Fastener strictly complies with European Union RoHS Directive 2011/65/EU and REACH Regulation (EC 1907/2006), providing certified third-party SGS/TÜV test reports for every product batch. We provide comprehensive automotive PPAP Level 3 packages, including Process Failure Mode and Effects Analysis (PFMEA), Control Plans, Gauge Repeatability and Reproducibility (Gage R&R) studies, and full material registration inside the International Material Data System (IMDS).
Furthermore, our surface treatment chemistry complies with environmental standards: 100% free of Hexavalent Chromium (Cr6+), ensuring non-toxic, eco-compliant supply chains across North America, the European Union, Japan, and the Asia-Pacific region.
Pioneering lightweight metallurgical cold heading, digital twin traceability, and intelligent surface finishes.
Integration of piezoelectric acoustic emission sensors inside multi-station cold heading dies. By detecting instantaneous micro-fracture acoustic signals in the forming zone, machines self-adjust wire feed speeds or halt stroke cycles before defective threads or heads can be forged.
Continuous mesh-belt furnace atmosphere monitoring utilizing infrared pyrometry and digital twin thermal modeling. Carbon potential is micro-adjusted in real-time, completely preventing surface decarburization and eliminating the risk of delayed brittle fractures.
Expanding precision cold-forming methodologies to Grade 5 Titanium (Ti-6Al-4V) and high-strength 7075 Aluminum alloys. Delivers a 42% structural weight reduction for commercial aerospace, eVTOL drone platforms, and handheld medical diagnostic equipment.
Clear, technical answers to the most common queries raised by industrial fastener procurement directors.
Hydrogen embrittlement is a primary failure mode when acid pickling or electroplating introduces atomic hydrogen into hardened steel lattices. At YH Fastener, all carbon steel fasteners tempered above 320 HV (or Grade 8.8 and above) enter de-hydrogenation baking ovens within a strict 4-hour window following electroplating. The parts are baked at 200°C to 220°C for 8 to 24 hours depending on fastener diameter and core hardness, verified per ASTM F1940 and ISO 15330 stress durability testing.
For mass-production cold heading, typical MOQs range from 50,000 to 200,000 pieces depending on part geometry, wire material, and tooling complexity. For preliminary prototyping, our rapid CNC engineering center produces 500 to 2,000 pieces within 7-10 working days. Mass-production tooling design and die fabrication require 15 days, followed by initial sample inspection (PPAP samples) within 7 days, and full container-load delivery in 25-30 days.
Yes. We accept native SolidWorks, STEP, IGES, and DWG drawing formats. Our engineering team conducts comprehensive Design for Manufacturability (DFM) reviews within 24 hours, advising on optimal cold heading draft angles, under-head fillet radii to prevent stress concentrations, and optimal patch positioning (e.g. 3-5 threads from tip) to ensure smooth initial thread engagement during automated robot feeding.
For harsh marine, chemical, or automotive environments, we recommend high-performance Zinc-Nickel electroplating (12-15% Ni content) with trivalent clear or black passivations, which routinely achieves 1,000 to 1,500 hours without red rust per ASTM B117. Alternatively, non-electrolytic Zinc Flake coatings (such as Geomet® or Magni®) provide sacrificial galvanic protection with zero risk of hydrogen embrittlement and exceptional thermal stability.
We maintain Vendor-Managed Inventory (VMI) frameworks, blanket annual purchase order agreements, and rolling safety stock arrangements for qualified tier-1 clients. With multi-point dispatch ports across Shenzhen, Guangzhou, and Hong Kong, ocean shipments reach European and North American ports within 18-28 days, backed by express air logistics for emergency assembly replenishments.
High-precision specialized mechanical hardware engineered to exact DIN, ISO, and client specifications.



Upload your 2D/3D component drawings. Our senior fastener application engineers provide structural feasibility analysis, material recommendations, and formal quotation packages within 24 hours.
